丸ナイフのラップ量(オーバーラップ)設定:せん断力学、材質別適正値、およびアーバー精度制御

In continuous metal coil processing, achieving a clean, square, and burr-free edge is the primary benchmark of a well-calibrated slitting line. Behind every high-yield slitting run are two critical geometric parameters governing shear-cut quality: horizontal side clearance and vertical rotary knife overlap. While horizontal clearance dictates the stress concentration across the strip width, vertical knife overlap determines the exact depth of blade penetration required to transition the metal cleanly from plastic deformation into controlled fracture. The operational significance of rotary knife overlap cannot be overstated. Setting the correct vertical overlap minimizes burr height, preserves cut edge geometry, and dramatically extends blade working life. Conversely, incorrect overlap settings drive edge tearing, […]
スリッターのカエリ(バリ)低減:根本原因マトリックス・設定条件・検査プロトコル
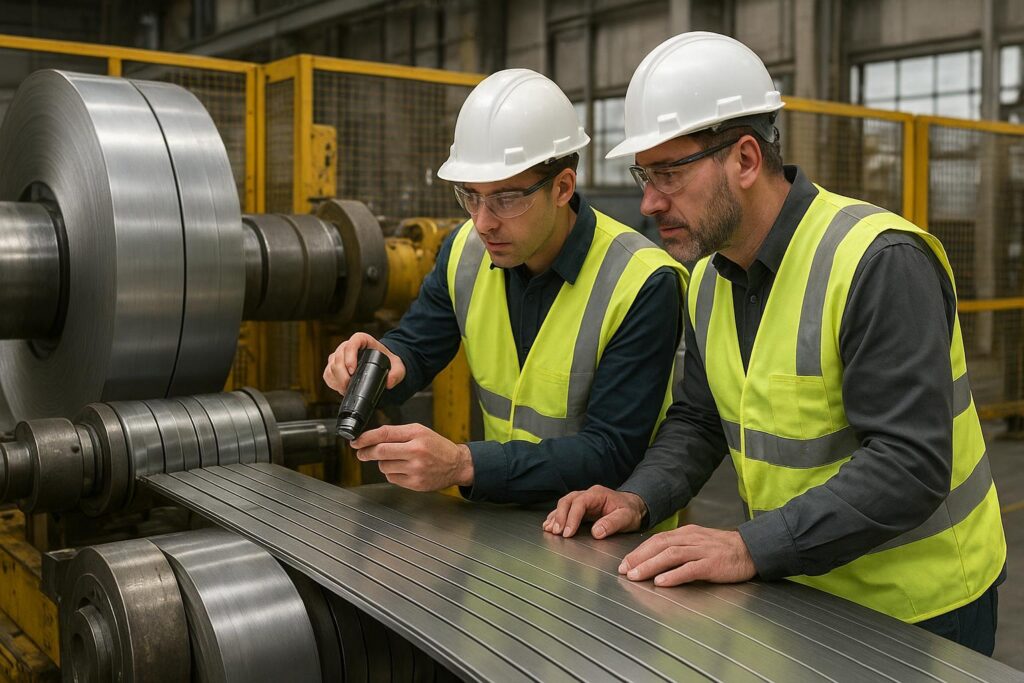
Slitting burr reduction is one of those “small edge” problems that becomes a big cost problem fast: burr drives customer complaints, creates downstream forming issues, and quietly shortens knife life. This handbook is compiled by Jerry Chu, Technical Support Specialist at Maxtor Metal, drawing on 10+ years of field troubleshooting experience across coil slitting lines processing carbon steel, AHSS, stainless, and aluminum. It is peer-reviewed by Maxtor Metal’s application engineering team and written in a practical, verification-first spirit where the winning approach is disciplined setup windows, fast root-cause isolation, and consistent measurement. If your line uses roller shearing blades (or equivalent slitter knife systems), the principles below still apply: treat the cut […]
高精度スリッター用スペーサー&ゴムリング:組込み剛性、刃先クリアランス、およびTIR(総合振れ精度)の完全制御

What readers will gain: tolerances, setup, verification, and ROI logging: concrete specs to ask for, checks to run before you clamp, and what to track so “better tooling” turns into measurable uptime. High-speed coil slitting doesn’t usually fail because the knives are “bad.” It fails because the clearance you thought you had is not the clearance the stack holds once it’s clamped, accelerated, heated, and pushed sideways by strip loads. That’s why constant axial side-clearance and stack stiffness are so tightly tied to burr height, edge wave, and early chipping. If your stack “breathes” under load—microns of spacer non-parallelism, a ring that takes a set, a nicked seating face—your clearance becomes a moving target. […]
ロータリースリッターナイフのROI:粉末ハイス(PM-HSS)vs 工具鋼のTCOモデル&刃先寿命分析

ロータリースリッターナイフは一見、小さな部品コストのように見えますが、それが影響を与える要素(段取り替え、スクラップ、バリの手直し、そしてラインがコイル全体にわたって公差を維持できるかなど)をモデル化すると、その重要性が明らかになります。本ガイドは、コイル切断・スリッティング操業におけるプロセス、設備、製造、および購買の責任者を対象としており、特に高価格帯のナイフセットが長寿命を謳っている場合に、選択肢を合理的に比較するための確実な方法を提供します。これは、より厳しいエッジ仕様、高強度グレード、またはより高速なライン速度へと移行する際に、多くのチームがMaxtor Metalのようなサプライヤーと行うROI(投資対効果)に関する議論と同様のものです。もし貴社の操業において、ロータリースリッティングと並行してローラーシャー設備を使用している場合、材料選定のロジック、クリアランス設計、および直接関係する故障モード診断は […]
OEMスリッターナイフの図面:スピンドル嵌合監査、ISO公差、TIRゲート

スリッターラインにおいて、優れた刃物鋼を使用していたとしても、内径とアーバーの嵌合部(ボア・アーバー界面)の仕様が不適切であったり、検証が不十分であったりすると、バリ、幅のズレ、早期チッピングなどの問題が発生します。このチェックリストは、エンジニアリング監査用として作成されています。OEMスリッター刃の図面を用意し、実際のスピンドルやアーバーの寸法と比較して、工具がコイルに接触する前に合否判定を記録します。お使いのラインで丸刃スリッターに加えてローラーシャー刃も使用している場合は、工具ファミリー全体で製品の形状と検査基準を統一してください。寸法公差、軸方向の振れ許容値、内径嵌合要件は、材質グレードやライン速度によって大きく異なります。エンジニアリングの全体像については、Maxtor Metalのロータリー[…]に関するガイドを参照してください。
スリッタースペーサーがバリ制御と裁断幅の精度を決定する仕組み
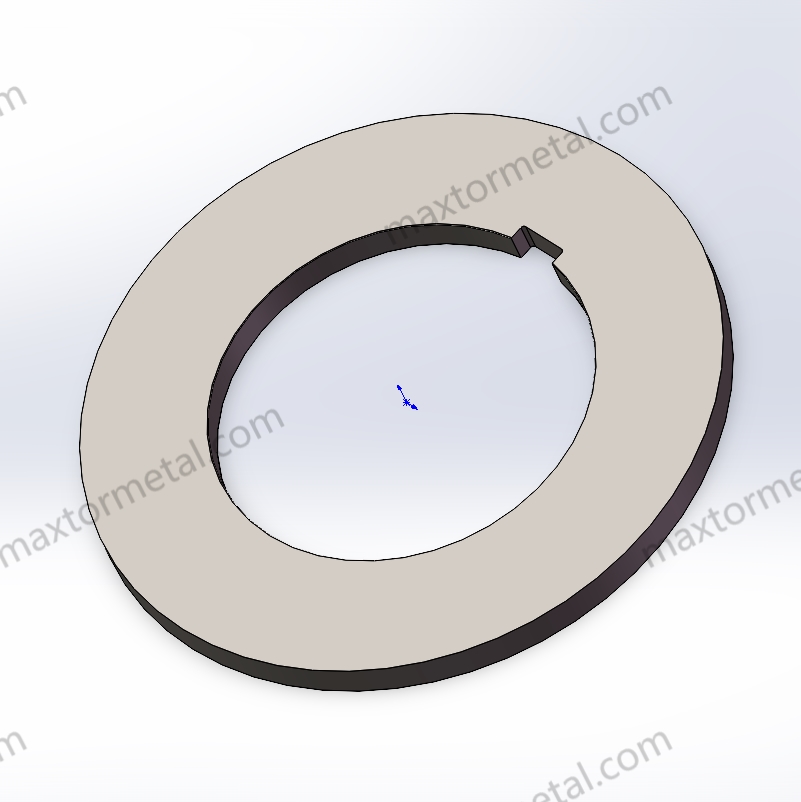
重要なポイント バリは単なる外観上の欠陥ではありません。フィルム、箔、繊維、コーティングされたウェブでは、粗いエッジが下流工程での破損、しわ、巻き取り不良、顧客からの苦情につながる可能性があります。金属では、バリが下流工程での取り扱い時の怪我、フィッティングの問題、早期摩耗を引き起こす可能性があります。スリット幅のずれも同様にコストがかかります。ロット間またはシフト間で幅を維持できない場合、仕様を広げる(不良品のリスクが下流工程に移る)か、再加工(時間と労力)を行う必要があります。どちらの場合も、OEEは低下します。停止回数が増え、検査回数が増え、段取り替え時間が長くなります。ナイフとスリッタースペーサーが共同でクリアランス、オーバーラップ、剛性を設定する方法 ナイフはせん断動作を生み出しますが、スペーサーはその動作が発生する場所と[…]
「安物買いの銭失い」の理由:プレミアムなロータリースリッターナイフの経済性を解明
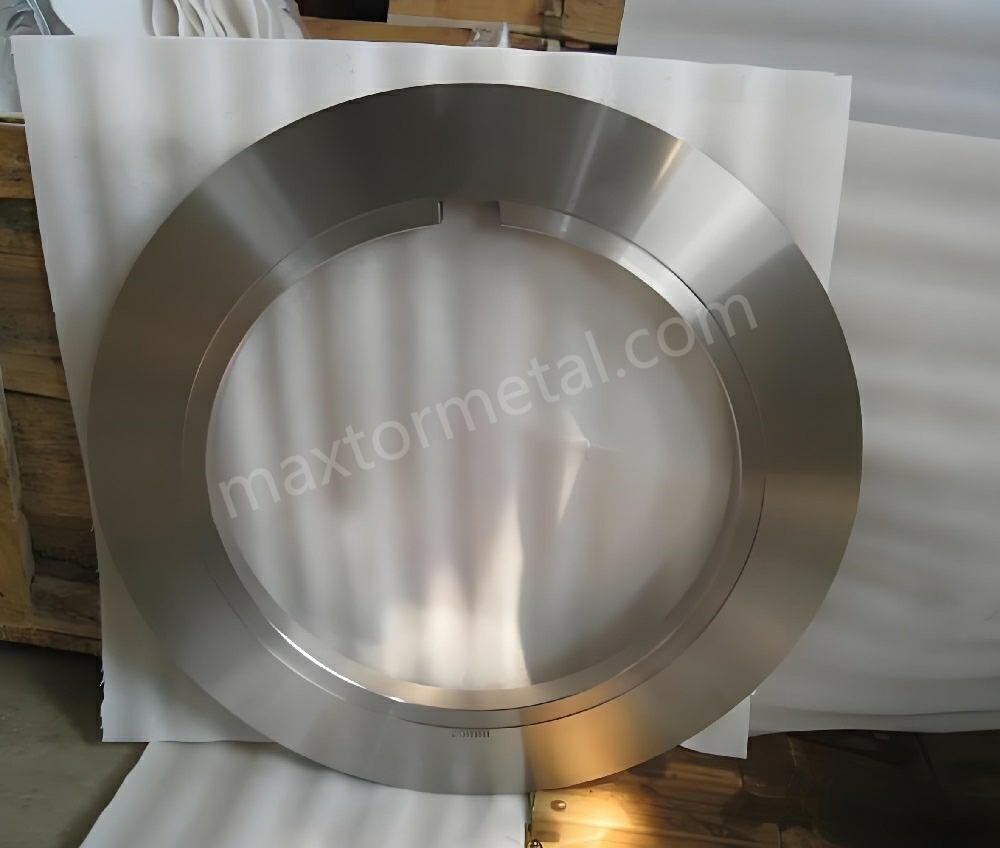
Verdict in 30 seconds: If you’re slitting stainless or high‑strength steels at moderate-to-high speeds—or your downtime costs run above roughly $50,000 per hour—premium Rotary Slitter Knives (HSS/PM‑HSS/Carbide, precision‑ground, coated) win on total cost of ownership. They cut scrap, stretch regrind intervals, and slash changeovers. If you’re a small shop on mild CR/HR steel with downtime under ~$10,000 per hour and conservative speeds, budget D2 or basic HSS can still be the economical choice. Our math anchors on three numbers: A) unplanned downtime $/h, B) total cost per changeover/regrind, and C) savings per 1% scrap‑rate reduction. Key takeaways Cheap vs premium Rotary Slitter Knives: the fast comparison (as of 2026‑01‑20) Below […]
AHSSの課題に挑む:自動車用高張力鋼(ハイテン)向けスリッターナイフの選
Automotive AHSS grades like DP, TRIP, and martensitic steels can turn a routine slit into a line-stopping headache. Burrs and micro‑chipping surge, edge ductility drops, and downstream formability (HER) suffers. This guide gives plant, process, and maintenance leaders practitioner-grade parameters—material and hardness ranges, coating choices, edge geometry targets, and clearance settings—plus a concise troubleshooting matrix. The goal: cleaner edges, fewer defects, and predictable performance when slitting AHSS. Key takeaways Why AHSS changes the rules AHSS combines high tensile strength with multiphase microstructures (martensite in ferrite), which raises cutting forces and amplifies sensitivity to parameter errors. Mechanical cutting reduces edge ductility; minimizing damage in the shear-affected zone is essential for better […]
鏡面仕上げの重要性:長寿命な円形スリッターナイフの製造方法
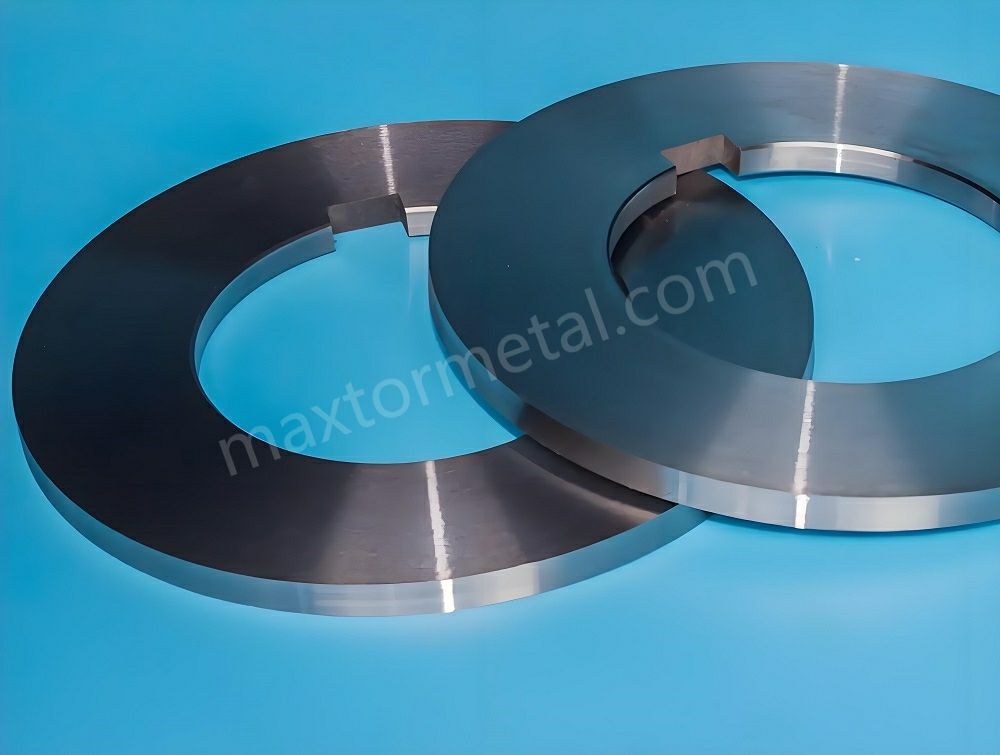
正確な切断を行うには、滑らかな表面が必要です。円形スリットナイフの鏡面研磨された刃先は、より良く、より速く切断するのに役立ちます。この仕上げは、作業を遅くするバリや摩擦を防ぎます。また、材料が刃に付着するのを防ぎます。材料が付着すると、刃を傷つけ、切断精度が低下します。南京Metal工業は、各刃を高度な技術で製造しています。彼らは常に、厳しい作業にも耐えうる高品質の製品を提供しています。重要なポイント 鏡面仕上げと切断精度 鏡面仕上げが重要な理由 刃は毎回きれいに切断したいものです。円形スリットナイフの鏡面仕上げは、これを実現するのに役立ちます。滑らかな表面により、刃は材料の上をスムーズに滑ります。つまり、[…]
セットアップの最適化:完璧なエッジのためにスリッターラインナイフとスペーサーがどのように連携するか

スリット加工において、常にバリのないシャープな切断面を得ることは極めて重要です。スリッターライン用刃物とスペーサーは、一体となって機能します。適切な材質と刃先形状を選択することで、刃物の性能を最大限に引き出すことができます。また、刃物間の隙間(クリアランス)は精密に調整する必要があります。適切なセットアップを行うことで、作業効率が向上し、機械によるスムーズなスリット加工を維持できます。 主なポイント スリッターライン用刃物:役割と特徴 スリット加工における切断機能 スリッターライン用刃物は、幅広の金属コイルを細いストリップ状に切断します。まず、アンコイラーにマスターコイルをセットします。金属材料は、所定の幅に設定された刃物の間を通過します。各刃物は、必要なストリップ幅に合わせて正確な位置に配置され、[…]
 English
 Spanish
 Italian
 French
 Portuguese
 Russian
 German
 Arabic
 Hindi
 Vietnamese
 Indonesian
 Japanese
 Korean