

Automotive AHSS grades like DP, TRIP, and martensitic steels can turn a routine slit into a line-stopping headache. Burrs and micro‑chipping surge, edge ductility drops, and downstream formability (HER) suffers. This guide gives plant, process, and maintenance leaders practitioner-grade parameters—material and hardness ranges, coating choices, edge geometry targets, and clearance settings—plus a concise troubleshooting matrix. The goal: cleaner edges, fewer defects, and predictable performance when slitting AHSS.
Principais conclusões
- Optimize clearance as a percentage of strip thickness by grade strength; AHSS typically needs 10–16% t, higher than mild steel.
- For knife materials, prioritize PM tool steels at 60–62 HRC for toughness + wear; add PVD coatings to control heat and adhesion.
- Use a micro-edge hone (10–30 µm typical) and polished faces to cut micro‑chipping and improve edge ductility.
- Validate with on-line checks: burnish/fracture zones, burr height trends, and targeted edge ductility tests for critical parts.
- Don’t chase maximum hardness; balance hardness with toughness to avoid brittle chipping, especially on martensitic grades.
Why AHSS changes the rules
AHSS combines high tensile strength with multiphase microstructures (martensite in ferrite), which raises cutting forces and amplifies sensitivity to parameter errors. Mechanical cutting reduces edge ductility; minimizing damage in the shear-affected zone is essential for better HER. Guidance from WorldAutoSteel notes that while mild steels may run at ~6–8% clearance (as % of thickness), AHSS grades—especially >1400 MPa—often require significantly larger clearances to reduce galling and stress at the cutting edge. See the slitting and clearance discussions in the AHSS portal for context in the industry’s own words in the AHSS Guidelines on slitting and clearance and the broader cutting guidance in WorldAutoSteel’s cutting and trimming overview.
Selecting Steel Slitting Knives for AHSS: material, hardness, coatings, geometry
Choosing the right combination prevents plastic deformation on one end and brittle chipping on the other. Think of it as balancing three levers—hardness, toughness, and friction/heat control.
- Materials and hardness
- PM tool steels (e.g., Uddeholm Vanadis 4 Extra, Vanadis 8; Böhler K390): run around 60–62 HRC (some up to ~64) for AHSS cutting, offering high wear resistance with better chipping resistance than conventional D2. Uddeholm’s AHSS tooling notes emphasize these PM grades for edge stability in severe applications; see Uddeholm’s AHSS tooling solutions e o Vanadis 4 Extra data.
- D2 (1.2379): workable at ~58–62 HRC but more prone to micro‑chipping in AHSS; consider PM alternatives for long runs or harsher grades.
- H13: tougher at ~52–56 HRC; useful where impact/shock dominates, but lower wear resistance may shorten intervals.
- Carbide or carbide‑tipped: consider for extremely abrasive or coated AHSS; ensure arbor support to manage brittleness.
- Coatings and surface treatments
- TiAlN/AlTiN: 1–4 µm PVD layers with high hot hardness and oxidation resistance; suited to dry or high-speed conditions typical of AHSS. See Oerlikon’s product pages on AlTiSiN/AlCrN families such as BALIQ TISINOS PRO.
- TiN/TiCN: 1–4 µm; TiN around ~2000–2500 HV; TiCN harder (~3000+ HV) but lower temperature ceiling; useful for adhesion reduction. Industry overviews provide representative ranges, e.g., TGW’s coating guide.
- DLC (ta‑C/a‑C:H): very low friction (COF <0.1 possible) and high hardness; useful when adhesive pickup/galling is the problem, including some coated steels. See Oerlikon’s DLC overview for cutting tools e Ionbond’s DLC technology page.
- Geometria e acabamento das bordas
- Micro‑edge hone: start with 10–30 µm for balanced AHSS, moving toward 20–50 µm if chipping persists on martensitic grades or where line shocks exist. Present these as validation ranges; direct standards are scarce. Uddeholm recommends polished faces for AHSS cutting tools; aim for fine finishes (e.g., Ra ≤0.2 µm on critical faces) to reduce notch initiation as outlined in Uddeholm’s AHSS guidance.
Summary table: material, hardness, coating, geometry (starting points)
| Choice | Typical working range | Where it helps | Cautions |
|---|---|---|---|
| PM tool steels (Vanadis 4 Extra, Vanadis 8, K390) | 60–62 HRC (some up to ~64) | High wear + chipping resistance for AHSS | Validate edge hone; excessive hardness without toughness can chip |
| D2 (1.2379) | 58–62 HRC | Baseline availability and cost | More chipping risk in AHSS; consider PM alternative for long runs |
| H13 | 52–56 HRC | Impact/shock, tough conditions | Lower wear resistance; shorter intervals |
| Carbide/carbidetipped | N/A (very high HRA) | Highly abrasive or coated AHSS | Brittleness; requires stable support |
| TiAlN/AlTiN PVD | 1–4 µm | Heat/oxidation resistance at speed | Regrind removes coating; plan recoat |
| TiN/TiCN PVD | 1–4 µm | Adhesion control; entry option | TiCN lower temp ceiling; validate |
| DLC | 0.3–1 µm+ | Low friction; galling control | May not suit high-heat spots; validate |
| Micro-edge hone | 10–30 µm (20–50 µm if chipping) | Reduces micro‑chipping; smoother entry | Too large hone can raise burr; trial |
| Acabamento da superfície | Target fine finish (e.g., Ra ≤0.2 µm) | Lower friction and notch sites | Requires careful grinding/polish |
Setup parameters that control burrs and HER
Clearance dominates burr formation and edge damage in AHSS. Start from strength- and thickness-based rules, then validate on line with edge-quality checks.
- Clearance as % of thickness (starting bands)
- Mild steel: ~6–8% t
- AHSS 600–980 MPa: ~10–14% t
- UHSS >1400 MPa: ~14–16%+ t
These align with the ranges discussed in the AHSS portal. For context and deeper explanation of how clearance shapes the shear‑affected zone, consult the AHSS Guidelines on clearance.
- Alignment, tension, and speed checklist
- Knife parallelism and arbor runout: verify before production. Misalignment adds uneven burr and accelerates wear.
- Tension: keep strip tension consistent; excessive tension increases edge tearing, while too little can cause wandering and knife marks.
- Speed: higher speeds can alter deformation zones; some studies on electrical steel show clearance and speed significantly affect burr and deformation. Treat speed changes as a controlled trial variable and re‑validate edge outcomes; see a peer‑reviewed overview in Szada‑Borzyszkowska et al. (2023) on shear‑slitting effects.
- Verification and HER awareness
- Inspect rollover, burnish, and fracture zones; in AHSS, burr height alone may not track wear predictably. The AHSS portal notes the need for broader edge-quality criteria in WorldAutoSteel’s slitting notes.
- For critical parts, run edge ductility checks: hole expansion testing (ISO 16630) or simple bend tests. SSAB provides context for edge ductility evaluation in SSAB’s insight on determining AHSS ductility.
Clearance quick table (validate per line)
| Strength/grade band | Thickness example | Starting clearance |
|---|---|---|
| Mild steel | 0.040 in (1.0 mm) | 6–8% t (0.0024–0.0032 in) |
| DP/TRIP 600–980 MPa | 0.040 in (1.0 mm) | 10–14% t (0.004–0.0056 in) |
| Martensitic/UHSS >1400 MPa | 0.040 in (1.0 mm) | 14–16%+ t (0.0056–0.0064 in) |
Troubleshooting matrix: AHSS slitting defects
Use the following as a first-response playbook; verify each change on a short coil segment before scaling.
| Sintoma | Causa provável | Ação corretiva | Prevenção |
|---|---|---|---|
| Rebarba alta ou borda irregular | Folga muito baixa/alta; gume cego; desalinhamento; detritos | Ajustar para 10–16% t para AHSS; reafiar; realinhar; limpar espaçadores/eixo | Calibrar a folga por classe; inspeções programadas; POP de limpeza |
| Micro-lascamento no gume da faca | Dureza excessiva ou aço frágil (ex: D2); afiação/acabamento de gume inadequado; choque por suporte deficiente | Mudar para aço PM a 60–62 HRC; adicionar micro-acabamento de 10–30 µm; verificar a rigidez do eixo e guias | Especificar classe PM + acabamento (hone); manter o hardware de suporte; evitar folgas excessivamente apertadas |
| Engripamento/adesão de material (galling) | Alto atrito com aços revestidos; superfícies da ferramenta ásperas; revestimento inadequado | Aplicar TiAlN ou DLC; polir a face de ataque/flanco; aumentar ligeiramente a folga; garantir lubrificação/limpeza | Adequar o revestimento ao trabalho; manter acabamentos finos; impor a limpeza entre bobinas |
| Deformação plástica/arredondamento do gume | Dureza da ferramenta muito baixa; sobrecarga; folga deficiente | Aumentar a dureza dentro dos limites de tenacidade; otimizar a folga; moderar a velocidade/tensão | Especificar o HRC correto; confirmar a folga; monitorar os indicadores de carga |
| Marcas de faca/ondulação de borda | Desalinhamento; tensão desigual; rolamentos desgastados | Realinhar as facas; estabilizar a tensão; fazer a manutenção dos rolamentos | Verificação de alinhamento pré-operação; controle de tensão; plano de manutenção preventiva |
As fontes para mecanismos e soluções incluem o portal AHSS e o guia de emparelhamento de ferramentas e revestimentos para AHSS da Uddeholm: consulte Visão geral de desgaste de ferramentas e matrizes da WorldAutoSteel e Guia de emparelhamento de PVD da Uddeholm.
Maintenance and lifecycle policy
Trate as lâminas de corte longitudinal como consumíveis de engenharia com um ciclo de vida documentado.
- Gatilhos de reafiação: em AHSS, a altura da rebarba pode não aumentar de forma constante com o desgaste; acompanhe também o crescimento do arredondamento, a consistência do brunimento/fratura e defeitos microscópicos no gume. As notas de corte longitudinal da WorldAutoSteel explicam o porquê. Consulte o Guia de corte longitudinal de AHSS.
- Plano de retificação e novo revestimento: preservar a geometria e o raio do micro-gume; reaplicar PVD após a retificação quando os revestimentos forem críticos para adesão/resistência ao calor, conforme Guia de revestimento da Uddeholm.
- Política de estoque sobressalente: manter uma rotação que suporte os tempos de retificação/revestimento sem forçar operações de emergência com facas cegas.
- Para checklists práticos de conservação e dicas de armazenamento/manuseio, revise os recursos neutros de manutenção da METAL, tais como dicas de manutenção de lâminas industriais.
Practical micro‑example: specifying a DP780 knife set (METAL)
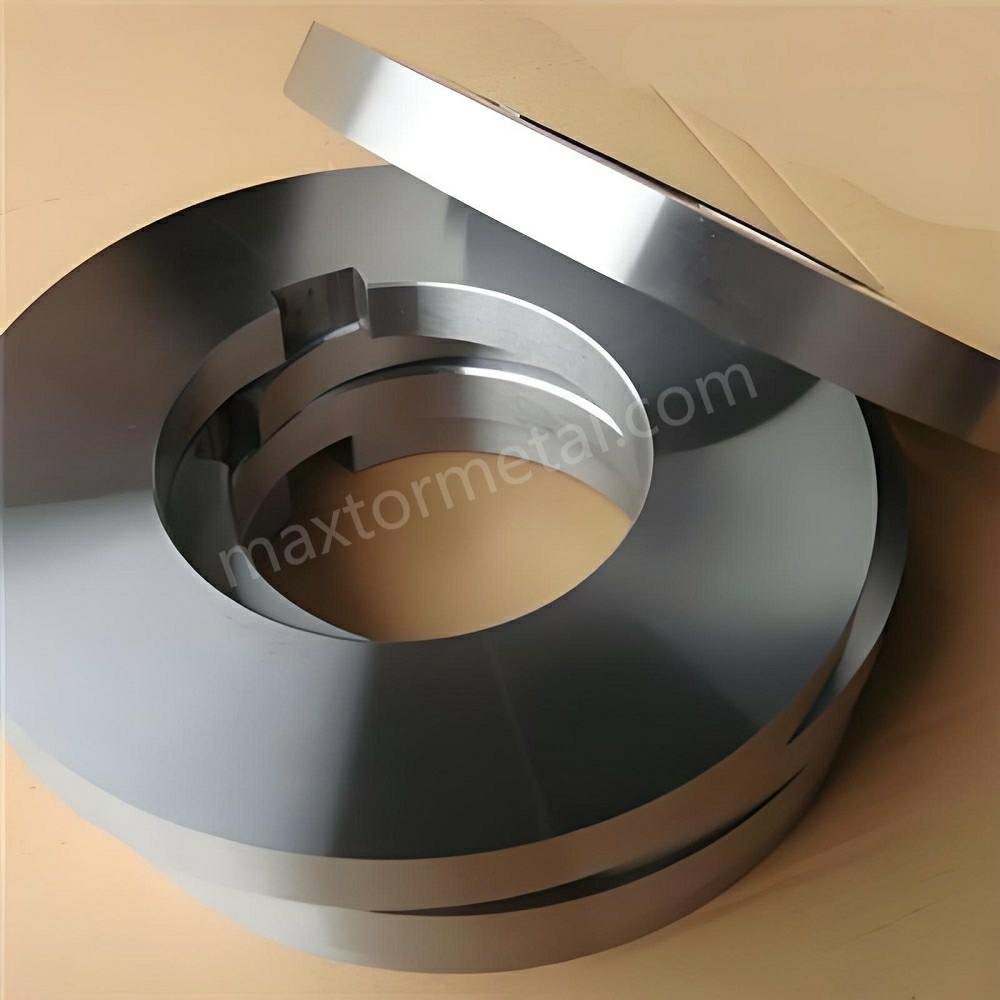
Divulgação: METAL é o nosso produto.
Para um AHSS automotivo comum como o DP780 a 0.040 in (1.0 mm), uma especificação inicial equilibrada pode ser assim para minimizar rebarbas e micro-lascamentos, preservando a ductilidade da borda:
- Material da faca: aço ferramenta PM comparável ao Uddeholm Vanadis 4 Extra, especificado em 60–62 HRC para um equilíbrio entre desgaste e tenacidade.
- Revestimento: TiAlN (1–3 µm) para gerenciar o calor e a oxidação em velocidades de linha típicas; considere DLC se houver adesão de material em bobinas revestidas.
- Preparação do gume: micro-acabamento (hone) de 15–25 µm; faces de ataque/flanco finamente polidas.
- Folga: 10–12% da espessura (0.004–0.0048 in para material de 0.040 in) como ponto de partida; validar com testes de curta duração.
- Verificação: inspecionar as proporções de brunimento/fratura e realizar testes pontuais de dobra/ductilidade de borda em peças críticas.
Para mais contexto sobre revestimentos e práticas de gestão de vida útil sem linguagem comercial, consulte a visão geral da METAL sobre revestimentos de lâminas de corte longitudinal e guia de durabilidade.
Referências e leituras complementares
- O portal AHSS da WorldAutoSteel oferece orientações sobre corte longitudinal, folga e corte que se conectam diretamente à ductilidade da borda/HER: consulte AHSS Guidelines on slitting and clearance e corte/blanking/cisalhamento/rebarbação.
- Os documentos orientados para profissionais da Uddeholm explicam por que os aços PM e as superfícies polidas e revestidas são importantes para ferramentas de corte de AHSS: Soluções de ferramentas para AHSS e Guia de emparelhamento de revestimento PVD.
- A SSAB fornece um contexto útil sobre a avaliação da ductilidade da borda em aços automotivos: Determinação da ductilidade do AHSS.
- Para uma discussão revisada por pares sobre como a folga e a velocidade moldam a deformação e a formação de rebarbas no corte longitudinal por cisalhamento (em aço elétrico), consulte Szada‑Borzyszkowska et al. 2023. As faixas de propriedades de revestimento e os casos de uso estão resumidos nas visões gerais neutras em relação ao fornecedor e nas páginas dos provedores de PVD citadas acima.
Próximos passos
Se você compartilhar o seu grau de aço alvo, espessura e limites atuais de rebarba/HER, podemos fornecer uma ficha de parâmetros simples (material, HRC, revestimento, preparação de aresta e folga) personalizada para a sua linha — e cotar as Facas de Corte Longitudinal para Aço exatas para atender a essas especificações.

 English
 Spanish
 Italian
 French
 Portuguese
 Russian
 German
 Arabic
 Hindi
 Vietnamese
 Indonesian
 Japanese
 Korean