

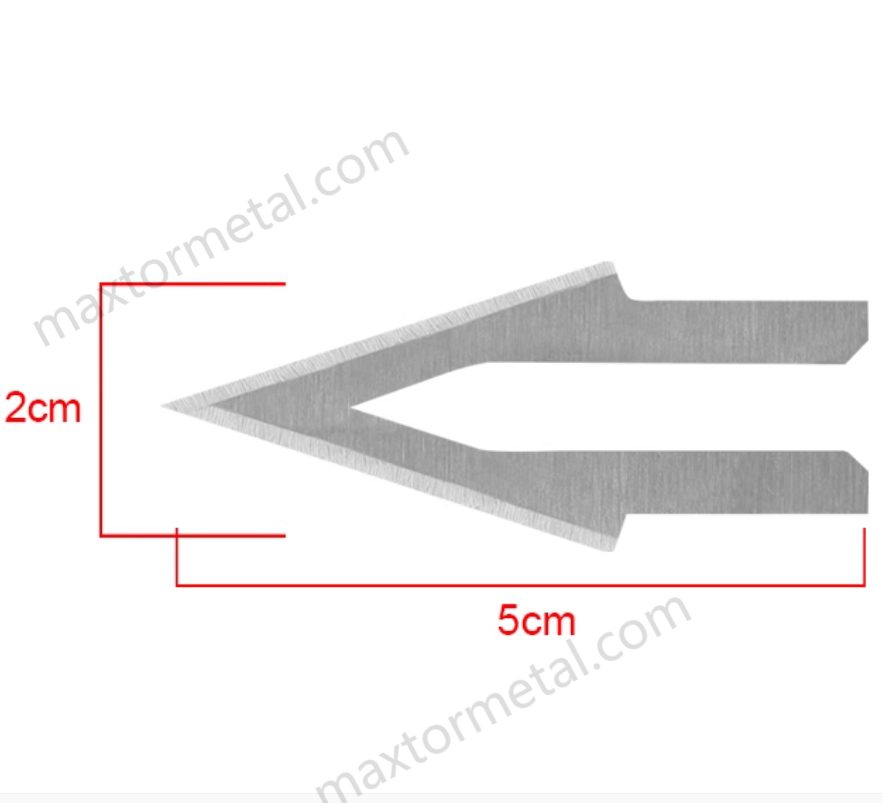
Introduction
Si vous utilisez la coupe thermique pour des sangles, des étiquettes, des chants ou de la mousse, le choix du matériau détermine discrètement vos limites en matière de temps de préchauffage, de dérive de température et de fréquence d'arrêt de la ligne pour le nettoyage ou le remplacement des pièces. Il s'agit d'une comparaison pratique visant des décisions que vous pouvez défendre : un temps de mise en service plus rapide, des coupes plus stables tout au long du poste de travail et un coût total de possession inférieur.
Ce guide est rédigé à l'intention des responsables d'équipements, de procédés, de production et des achats qui doivent concilier qualité de coupe, taux de rendement global (TRG), sécurité et continuité de l'approvisionnement. Nous comparerons le NiCr (nichrome 80/20) aux options courantes en acier inoxydable (304/316/420/440C) et, surtout, nous séparerons les exigences de l'élément chauffant des exigences de la lame/du tranchant exigences.
Auteur: Ingénieur procédé MAXTOR (anonyme)
Revue technique : Revu par l'équipe de fabrication et de contrôle qualité de MAXTOR METAL
Comment nous validons nos recommandations : Dans la mesure du possible, nous alignons la sélection des matériaux et les conseils de procédé sur le flux d'inspection et de vérification de MAXTOR METAL (inspection des matériaux entrants avec certifications, inspection du premier article, inspection en cours de fabrication et inspection finale), puis nous confirmons les résultats par des essais chez le client.
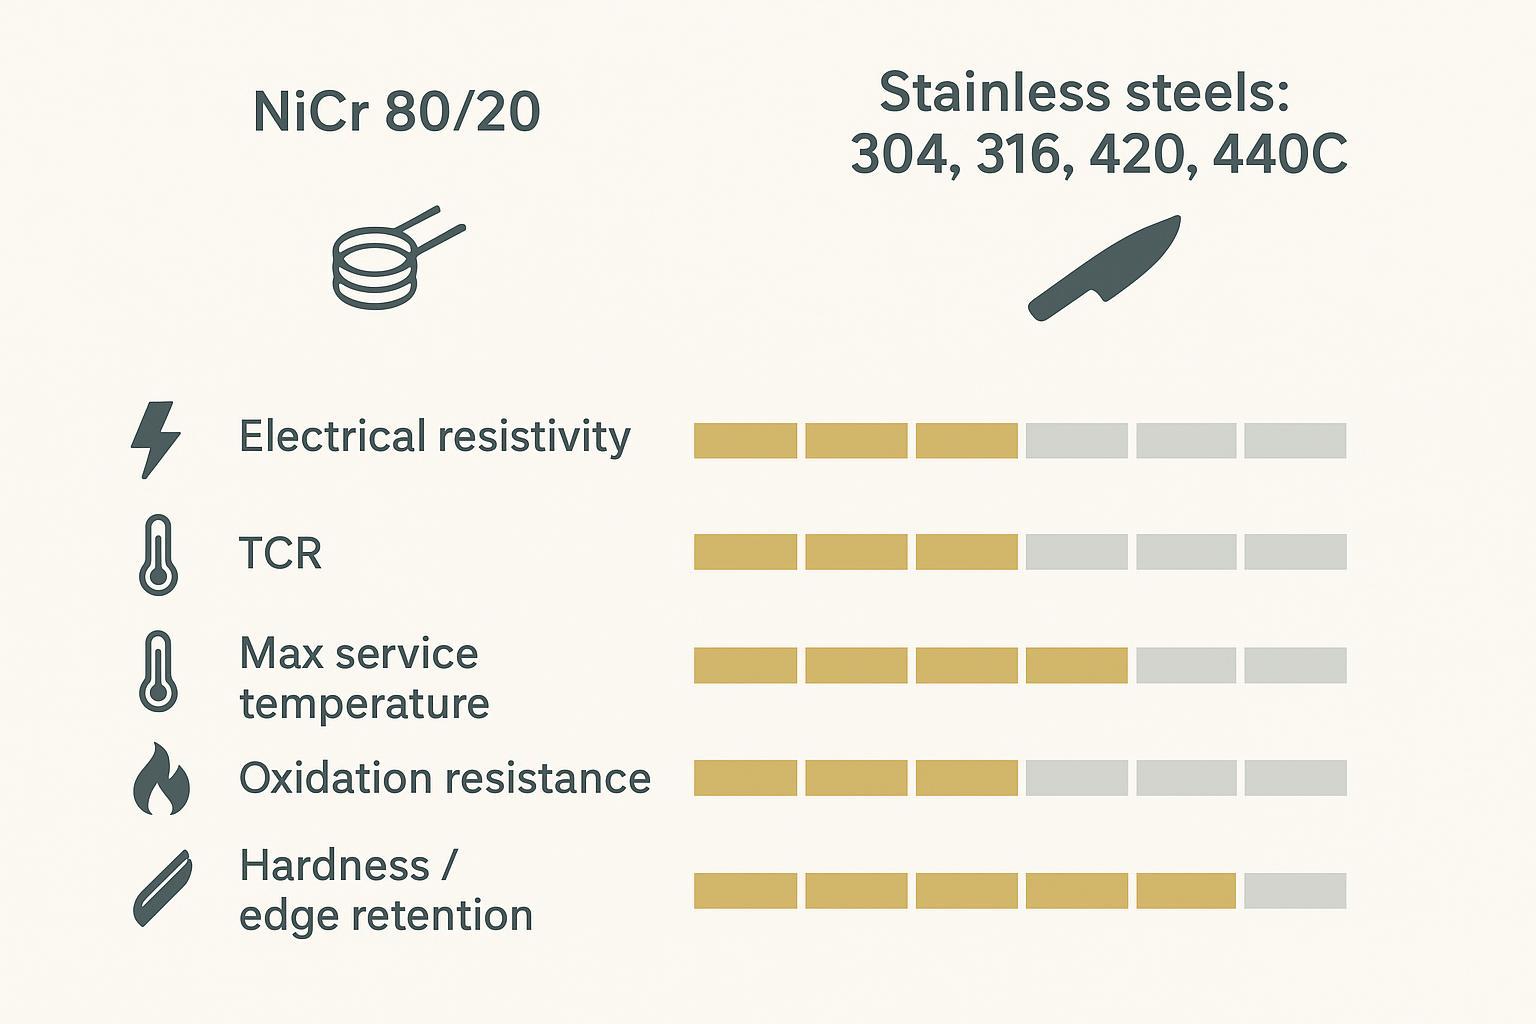
Propriétés des matériaux qui déterminent la performance (comparaison des matériaux pour thermocouteaux)
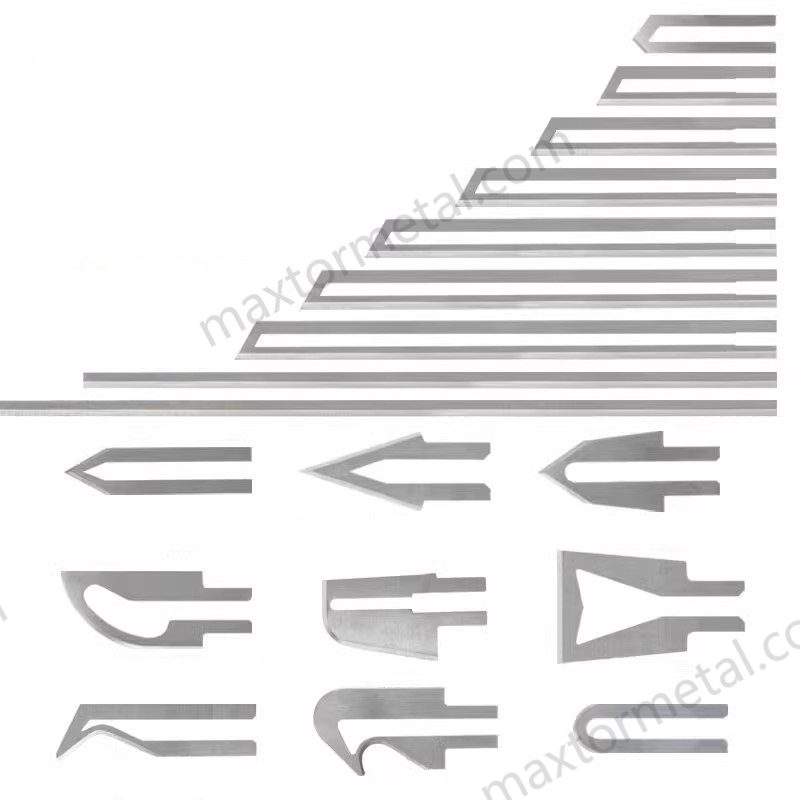
Les thermocouteaux tombent en panne de manière prévisible : préchauffage lent, chute de température lorsque le matériau entre en contact avec la lame, formation importante de bourrelets de fusion, noircissement/fumée et arrondissement rapide du tranchant. Ces résultats découlent généralement d'un nombre restreint de propriétés des matériaux.
Résistivité électrique et coefficient de température (TCR/Ct)
Un élément chauffant par résistance est une résistance contrôlée. Une résistivité électrique élevée facilite la génération de chaleur avec des tensions et des courants pratiques ; un coefficient de température de résistance (TCR) stable rend le contrôle plus prévisible à mesure que l'élément chauffe. En d'autres termes, c'est le cœur de la décision entre le NiCr et l'acier inoxydable pour l'élément chauffant.
Le NiCr (nichrome 80/20) est un alliage de résistance spécialement conçu pour les éléments chauffants, c'est pourquoi il domine dans les réchauffeurs industriels et l'outillage à fil chaud. En revanche, les aciers inoxydables peuvent conduire le courant, mais ils ne sont pas optimisés pour un chauffage par résistance stable et efficace à des températures élevées ; même les ingénieurs expérimentés préviennent que l'acier inoxydable ne peut pas “ se comparer au Nichrome ” une fois que les bobines deviennent chauffées au rouge, comme cela est abordé dans Eng-Tips : “ 304 Stainless Steel vs. Nichrome Heating Coils »".
Température maximale de service et comportement à l'oxydation
La température de service ne se résume pas à “ peut-il devenir chaud ? ”. Il s'agit plutôt de savoir “ s'il peut survivre aux cycles thermiques dans l'air sans calaminage, fragilisation et dérive de résistance ”. Le NiCr est conçu pour former une couche d'oxyde protectrice et tolérer des températures élevées prolongées dans l'air, c'est pourquoi il est décrit dans les références sur les alliages de résistance telles que l'aperçu des alliages de résistance de Tokkin comme étant adapté à une utilisation dans des éléments chauffants à haute température.
Les aciers inoxydables peuvent tolérer des températures modérément élevées, mais leur comportement à l'oxydation et leurs propriétés mécaniques changent avec la température et le temps. Si votre conception se situe près de la limite supérieure de ce que subit votre outillage, utilisez des données fiables sur les températures élevées spécifiques à chaque nuance (et validez-les avec votre fournisseur), telles que la plateforme de référence de la British Stainless Steel Association : «Propriétés physiques à haute température des aciers inoxydables".
Dureté, résistance au revenu et rigidité structurelle
Voici la distinction que la plupart des usines négligent :
- L'élément chauffant a besoin d'un comportement électrique stable et d'une résistance à l'oxydation.
- La lame/le tranchant a besoin de dureté, de résistance au revenu et de rigidité pour ne pas s'arrondir, se déformer ou “ pousser ” le matériau au lieu de le trancher.
C'est là que les nuances d'acier inoxydable martensitique (comme le 420 et le 440C) prennent toute leur importance : elles peuvent subir un traitement thermique pour obtenir un tranchant plus dur que le 304/316, améliorant ainsi la tenue de coupe et réduisant les changements d'outils —if à condition de gérer la perte de revenu à la température de fonctionnement (plus de détails à ce sujet dans la section de sélection).
| Matériau | Meilleur rôle dans un thermocouteau | Valeur(s) typique(s) pour guider les décisions | Source principale |
|---|---|---|---|
| NiCr 80/20 (Nikrothal® 80) | L'élément chauffant | Résistivité électrique 1,09 Ω·mm²/m (20°C) ; température maximale de fonctionnement continu dans l'air 1200°C | Fiche technique Kanthal : feuillard Nikrothal® 80 (ou fil Nikrothal® 80) |
| Acier inoxydable 440C (traité thermiquement) | Lame/tranchant pour la résistance à l'usure | Dureté après traitement thermique généralement de 58–60 HRC (selon l'application) | Fiche technique Carpenter Technology : CarTech® 440C Stainless |
| Acier inoxydable 420 (traité thermiquement) | Lame/tranchant lorsque la ténacité/le réaffûtage sont importants | Dureté après trempe généralement autour de 50 HRC (dépend du traitement thermique) | Fiche technique Atlas Steels : Stainless Steel 420 grade data sheet |
| Acier inoxydable 304 (recuit) | Structural parts, low-heat tooling bodies | Electrical resistivity at 24°C 19.9 μΩ·cm | BSSA reference: Elevated temperature physical properties of stainless steels |
| 316 stainless (annealed) | Fixtures/housings in humid or chloride environments | Electrical resistivity at 24°C 19.9 μΩ·cm | BSSA reference: Elevated temperature physical properties of stainless steels |
Notes: “Typical values” vary by product form, heat-treatment condition, and temperature. For engineering sign-off, pull the exact values from your heater alloy datasheet and your mill test certificate/COA (or supplier datasheet), then validate performance under your real duty cycle, geometry, and controls.
Des propriétés aux résultats du procédé
Once you separate “heater” from “edge,” the process outcomes become easier to predict—and to fix.
Field snapshot: NiCr vs 440C on a 20 mm polyester webbing line (anonymous)
The data below comes from an industrial trial on an automated continuous cutting line running 20 mm polyester webbing, comparing a NiCr 80/20 hot-knife approach versus a heat-treated 440C blade approach. Treat it as a directional benchmark—your geometry, power supply, sensor placement, and line speed will shift the exact numbers.
For context, supplier specs for automated webbing hot-knife cutting machines often list cutting rates on the order of ~60–200 cuts/min depending on cut length and setup (see example machine specifications such as chinafoxsew’s automatic polyester webbing cutting machine et un webbing cutting machine spec listing 200 cuts/min as an example at 50 mm length). Use this as a rationality check when you compare your own throughput.
- Warm-up to 350°C: NiCr 80/20 ~**15 s** vs 440C ~35 s
- Cut edge outcome (webbing): NiCr showed a flat sealed edge with minimal sticking; 440C performed excellently early on but could start “stringing” when temperature control drifted.
- Maintenance interval: NiCr ~**50,000 cuts** vs 440C ~120,000 cuts
- Typical failure mode: NiCr edges dulled mechanically and began under-sealing; 440C could soften over long high-temperature exposure and later chip once hardness dropped.
How to use this: if your process is dominated by heat delivery and stability, NiCr tends to win on time-to-ready and control margin; if it’s dominated by mechanical edge retention in thick/tough stock, heat-treated 440C often wins on wear and changeover interval.
*Data notes: the warm-up time is sensitive to heater resistance design (gauge/length), available voltage/current, PID/SSR behavior, and thermocouple location. For temperature measurement practice, cutting-temperature measurement methods generally emphasize placing the thermocouple junction as close as practical to the cutting edge/interface so it represents the real cutting zone (see review of cutting temperature measurement methods). Maintenance interval depends strongly on webbing construction, coatings/adhesives, edge geometry, and allowable seal quality.*
Heat-up speed and time-to-ready
Warm-up is a simple productivity lever: every restart, setup, and changeover has an “idle-to-ready” penalty. In practice, time-to-ready depends on how quickly the heater can deliver energy into the edge without needing excessive current, and how consistently the controller can hit setpoint without overshoot.
NiCr heaters typically shorten warm-up for a given power supply envelope because they’re designed to convert electrical power to heat efficiently and survive the temperature you actually need for sealing synthetics. If you’ve been compensating for slow warm-up with a higher setpoint “just to get it cutting,” that’s often what pushes you into blackening and heavy melt beads.
Temperature stability and drift under thermal cycling
Thermal cutting is a repeated disturbance: the blade dumps heat into the workpiece, then recovers, over and over. Hot knife temperature stability comes from three pieces:
- A heater material with predictable resistance change vs temperature
- A controller that can modulate power smoothly (SSR + PID is common)
- A temperature sensor mounted where it represents the cutting edge
Practical checklist (to make this reproducible on your line):
- Sensor placement: mount the thermocouple as close as safely possible to the cutting edge or the heat-transfer path that actually represents the edge temperature (not just the heater body).
- Controller output: SSR + PID works well for cycling loads; size SSR and wiring for your duty cycle and peak current.
- Overshoot control: if you see smoke/blackening at startup, reduce ramp rate or tune PID to soften the initial power burst before you raise setpoint.
- Stability criteria: judge stability by edge outcome (seal continuity, kerf, residue rate) and by whether the edge temperature recovers consistently after each cut.
When stability is poor, you see it as alternating under-seal and over-melt across a run. MAXTOR METAL describes these field symptoms—under-seal (fray), over-melt (distortion), and smoke/blackening—as common indicators that temperature, feed rate, and duty cycle aren’t matched, in their article “How a Synthetic Fabric Hot Knife Improves Yield and OEE”.
Element life, edge retention, and changeover frequency
Element life is mostly oxidation + thermal fatigue. Edge life is mostly hardness retention + contamination management.
A NiCr element that holds up to thermal cycling reduces heater failures and “mystery drift” where the tool needs more power over time to do the same work. For the blade, moving from 304/316 to a heat-treatable edge material (420/440C) can reduce how often you regrind or replace the blade—especially when cutting abrasive laminates, coated tapes, or foam with fillers.
Plages de fonctionnement : textiles, sangles, étiquettes, chants, mousses
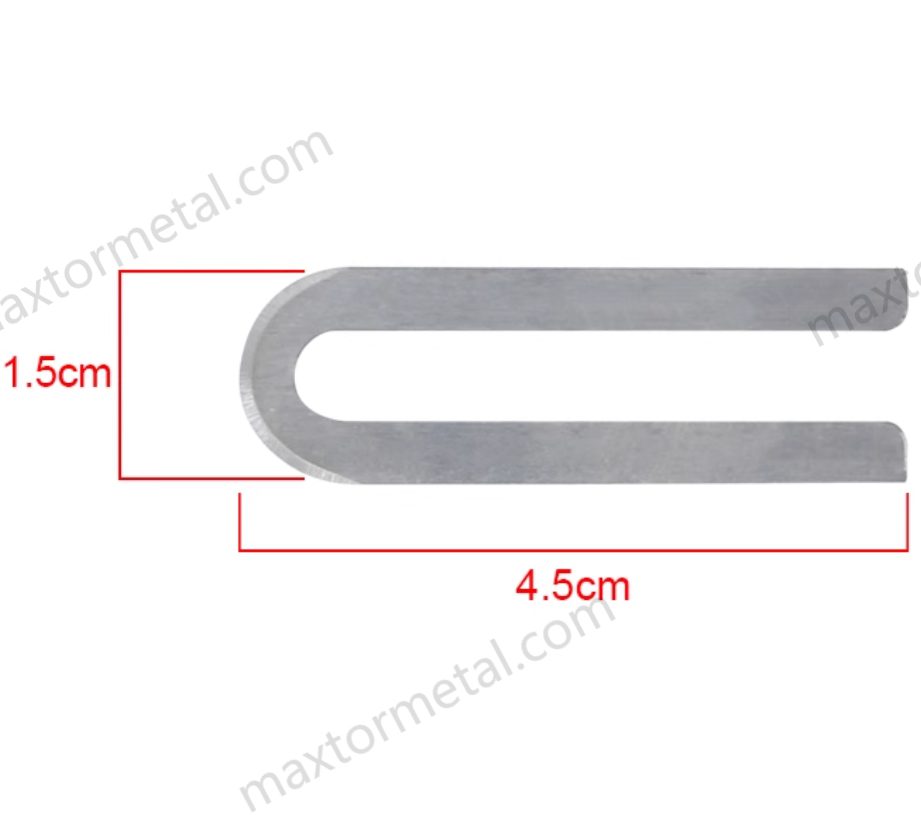
The right material choice narrows the gap between “works on the bench” and “holds a window on the line.” The window is set by edge temperature, power delivery, and how fast you move.
Method and scope notes (read before you copy setpoints)
- Capability vs. recommended settings: temperature ratings and example tools show what a system peut reach, not what you should run. Treat any number as a starting point, then qualify it on your own material and line speed.
- Validate locally: polymer family, coatings/adhesives, thickness, and airflow can change smoke, residue, and seal behavior. Always run a short, instrumented trial before locking parameters.
- Safety disclaimer: thermal cutting can release irritant gases, vapors, and particles. Use local exhaust ventilation and follow your site EHS requirements and applicable regulations.
Typical edge temperatures and setpoint ranges
Typical starting points depend on polymer family, thickness, and whether you’re sealing the edge or only separating.
- For many synthetic fabrics and webbings, hot knives are commonly rated to operate up to about 400°C, providing sealed cuts when motion and dwell are controlled.
- For foam tools, some industrial handheld cutters are designed to reach up to 500°C rapidly (for example, ATO’s handheld foam cutter listing (500°C capability)).
Treat these as capabilities and starting references, not universal setpoints. Your acceptance criteria should be edge quality (seal continuity, kerf, distortion) and fume level, not a target number alone.
Power matching, feed speed, and kerf/seal quality
Three practical rules keep you out of trouble:
- If you see fray or “hairy” edges (under-seal): raise temperature in small steps ou slow feed slightly ou improve tension/fixturing. Don’t jump straight to a much higher setpoint.
- If you see a big melt bead or edge shrink-back (over-melt): lower setpoint ou increase feed speed; consider changing blade geometry to reduce dwell and smear.
- If the cut is wavy or dimensions drift: your system is likely heat-soaking unevenly. Check rigidity (blade bending), sensor placement, and whether the heater is delivering uniform heat into the edge.
Those adjustments matter more when the heater material has stable behavior and the edge material keeps its shape; otherwise, you end up chasing the process all day.
Ventilation and fume considerations during thermal cutting
Thermal cutting makes fumes because you’re heating polymers at the edge. Even when the cut looks clean, ventilation is not optional in production.
Use local capture where practical, keep a record of materials cut (including coatings and adhesives), and treat smoke/odor changes as process signals—not “normal.” If you’re seeing persistent smoke or blackening, MAXTOR METAL’s process guidance is blunt: reduce temperature/dwell and clean the blade, rather than forcing the tool through contamination, as outlined in their yield/OEE hot knife note.
NIOSH’s Health Hazard Evaluations on high-heat plastic processes (including heat sealing) repeatedly emphasize capturing contaminants at the source—local exhaust ventilation at the point where the fume plume forms—because general ventilation alone is often not enough in real production conditions (see NIOSH HHE reports such as «Evaluation of Exposures and Symptoms from Heat Sealing…" et «Evaluation of Employee Exposures at a Plastic Bag Sealing Plant").
For example, OSHA’s welding/cutting/heat standards emphasize ventilation and fume control as core controls (see OSHA 29 CFR 1926.353 “Ventilation and protection in welding, cutting, and heating").
Analyse technique et ROI
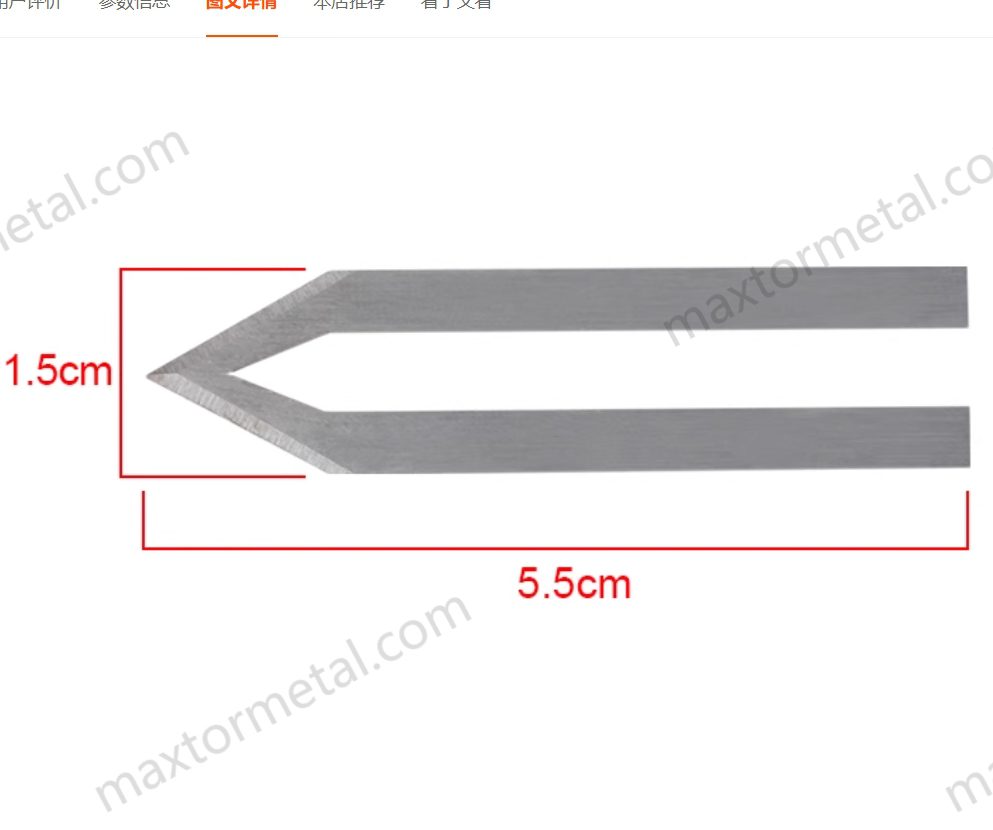
This is where material choice stops being a “preference” and becomes an engineering and cost decision.
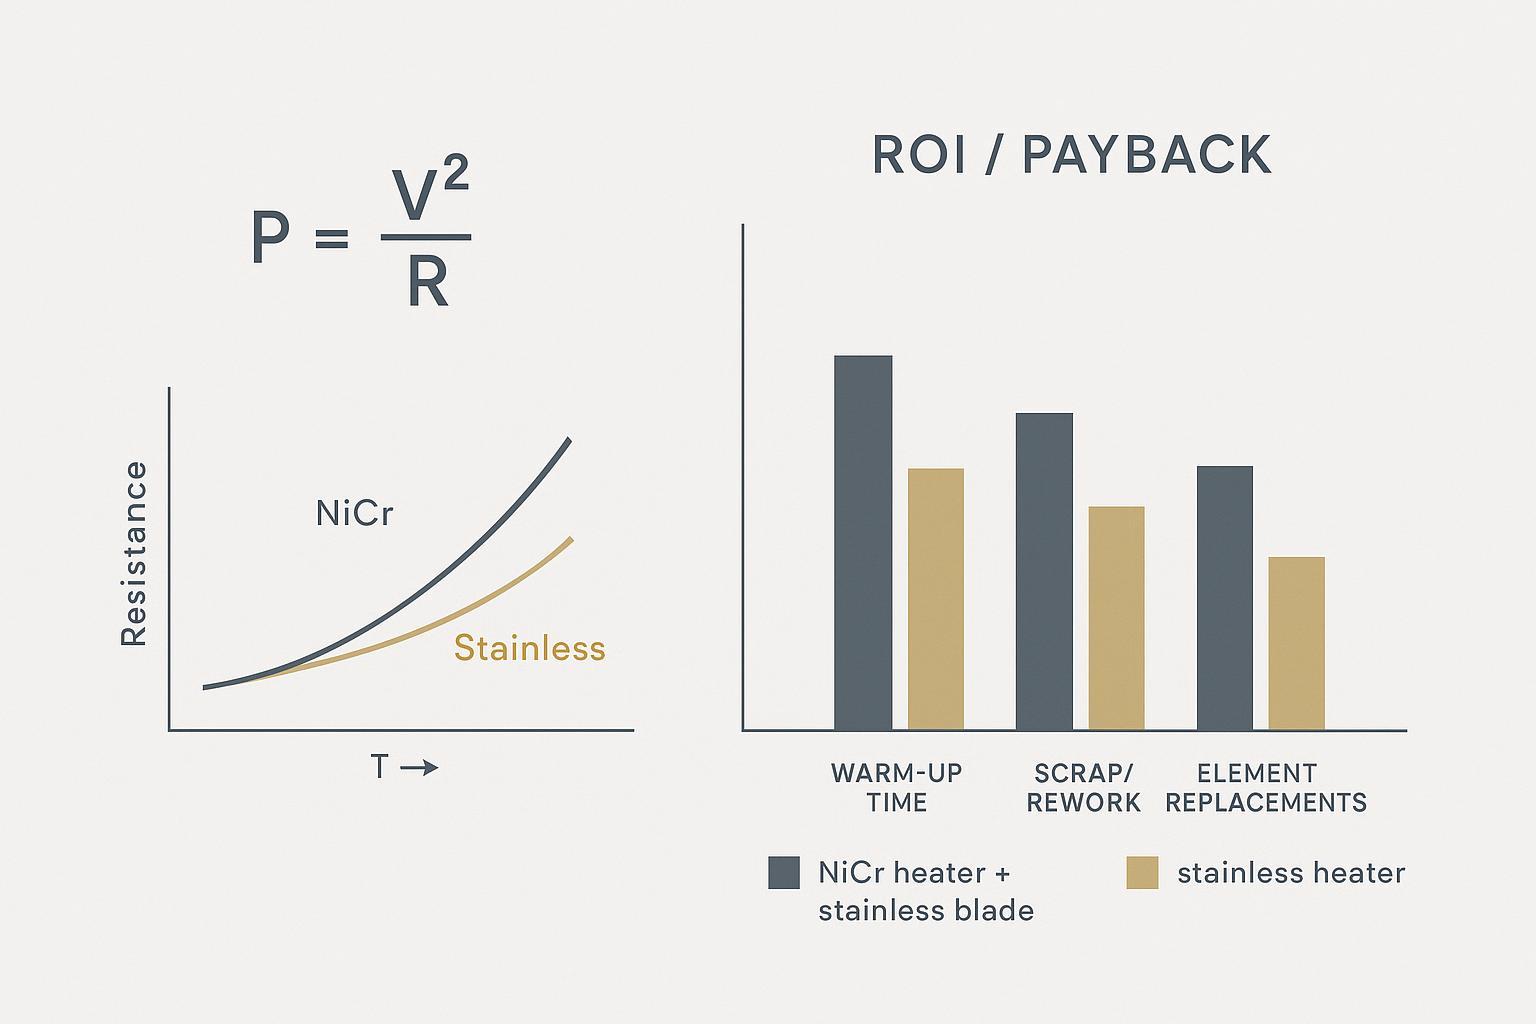
Linking P=V^2/R and TCR to warm-up and control accuracy
For a resistive heater:
- Pouvoir is approximately P = V² / R (at constant voltage).
- As the element heats, its resistance changes with its TCR.
Practical implication: if you choose a heater material with low resistivity or a large resistance swing vs temperature, you force either (a) higher current and heavier wiring/PSU, or (b) more aggressive controller duty cycling to maintain temperature. A heater designed for stable resistance heating makes it easier to reach setpoint quickly and hold it under load.
OEE/FPY gains from stability; energy and idle-to-ready savings
A stable hot knife improves OEE the same way stable extrusion or sealing does: fewer rejects, fewer micro-stops, and fewer “operator tweaks.” MAXTOR METAL frames the gain in terms of improved Quality (less scrap/rework from fraying) and improved Availability/Performance (less time fixing edge issues) in their hot knife yield and OEE article.
On the energy side, warm-up and idle-to-ready time is where factories quietly lose money: the line is waiting, the tool is heating, and you’re not shipping parts. Material choice that reduces warm-up time and stabilizes setpoint shrinks that non-productive window.
TCO: consumables, downtime, and quality-related scrap
A simple total cost of ownership model should include:
- Consumables: heater elements, blades/edges, insulation, fasteners
- Temps d'arrêt : planned changeovers + unplanned stops from drift or failures
- Quality losses: scrap, rework labor, and inspection holds
If you already track OEE and scrap by SKU, you can make the case quickly: the payback is often driven by fewer changeovers and fewer “bad edge” parts, not by the unit price of the element.
Guide de sélection par scénario
Heater element: when NiCr is preferred over stainless
Choose NiCr (80/20) as the heater element (a nichrome 80/20 heater element in many legacy designs) when:
- Vous avez besoin fast time-to-ready without overshooting into smoke/blackening.
- The process requires stable cutting across thermal cycling (start/stop, varying feed, thicker sections).
- You operate at elevated temperatures where oxidation life matters.
Stainless can be workable for low-temperature, short-duty prototypes, but for production thermal cutting it often becomes a control problem (current draw, drift, shorter life) rather than a cost saver.
Blade/edge: when 420/440C beats 304/316, with temper management
Choose 420 or 440C for the la lame/du tranchant when you need hardness and edge retention.
- 420 is typically the more forgiving choice when toughness and ease of resharpening matter.
- 440C is typically the better choice when wear resistance and edge retention dominate, and your setup avoids impact or edge chipping.
If your team keeps asking “440C vs 420 stainless blade edge?”, the practical answer is: pick 420 when abuse/toughness dominates; pick 440C when wear and longer intervals between regrinds dominate—then validate temper loss under your real setpoint and duty cycle.
Temper management matters because repeated heating can soften a hardened edge over time. Practical mitigations:
- Keep heat concentrated in the heater/edge zone; avoid heat soaking the whole blade body.
- Use insulation and geometry that reduces dwell and smearing.
- Validate edge retention under your real duty cycle (not just a short bench cut).
Humid/cleaning environments: roles for 316 structures plus NiCr heaters
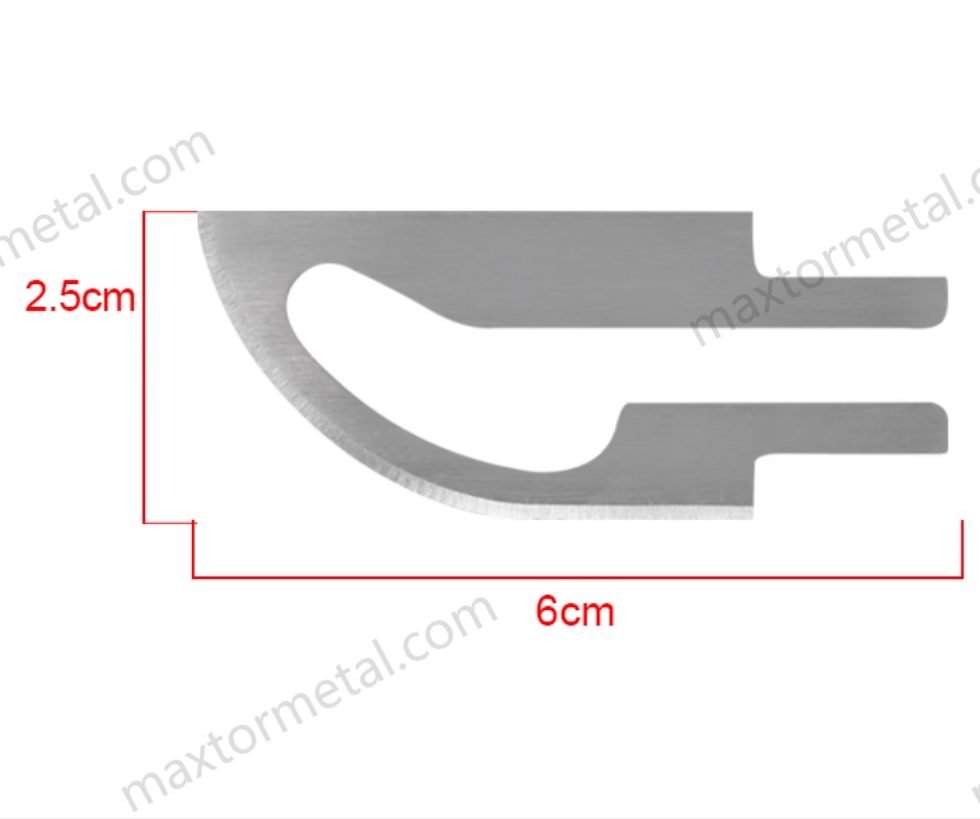
In washdown, humid, or chloride-prone environments, 316 is a strong choice for fixtures and housings, while keeping NiCr as the heater. MAXTOR METAL supports custom hot-knife blades and material selection (420/440C edges, 316 structures) and can help match a NiCr heater to your power and duty-cycle constraints.
Mise en œuvre et conformité
Verification checklist (what to confirm on your line)
- Materials & certificates: confirm heater alloy and blade steel match the specified grade and condition (e.g., heat-treated vs annealed) and review supplier datasheets plus your COA where available.
- Temperature measurement: verify the sensor location represents the cutting edge temperature (not only the heater body) and document the placement so results are repeatable.
- Controls: confirm power supply/SSR capacity matches peak current and duty cycle; tune PID to avoid overshoot (smoke/blackening at startup is a warning sign).
- Acceptance criteria: define pass/fail for seal continuity, kerf/dimensions, discoloration, residue buildup rate, and changeover interval.
- Ventilation: use local exhaust ventilation at the fume source and align with site EHS requirements and applicable OSHA/NIOSH guidance.
Trial protocol: instrumentation, ramp, and acceptance criteria
A trial should be short, instrumented, and repeatable:
- Instrument: record setpoint, actual edge temperature (thermocouple placement matters), power, and feed speed.
- Ramp and soak: define a warm-up time target and a soak time so the blade reaches a stable condition.
- Acceptance criteria (binary):
- edge seal continuity (pass/fail)
- kerf and dimensional stability (within your spec)
- discoloration/blackening (none allowed)
- residue buildup rate (cleaning interval target)
Keep the first-article approval explicit, then lock parameters per material.
Safety and air quality: capture, ventilation, and exposure controls
Treat thermal cutting as a fume-generating operation. Use local capture where feasible, document what materials/coatings are being cut, and train operators on symptoms that require action (smoke/odor change, irritation, residue buildup). If you need to defend your setup to EHS or a customer audit, the easiest win is a clear capture/ventilation plan plus records of setpoints and materials.
Power, controls, and CE/OSHA-aligned documentation
For controls, prioritize:
- Stable power delivery sized for your duty cycle
- Closed-loop temperature control with an SSR output where appropriate
- Documented setpoints, blade type, and acceptance checks per material
For documentation, keep wiring diagrams, control settings, and maintenance intervals in a single packet. It reduces troubleshooting time and makes compliance reviews faster.
Conclusion
The practical split is simple:
- NiCr (80/20) is the right default for heater elements when you need fast warm-up, stable temperature under load, and long oxidation life.
- 420/440C are the right defaults for cutting edges when you need hardness and edge retention—provided you manage temper loss and contamination.
- 316 earns its place in structures and fixtures where corrosion and cleaning matter.
Business impact shows up as faster warm-up, steadier temperatures, longer life between changeovers, and a lower TCO driven by fewer defects and fewer stops.
Next steps: run a short instrumented trial, lock setpoints and feed speeds per material, and document your safety/ventilation controls. If you’re building a custom blade or need help matching geometry and heater selection to your line, review MAXTOR METAL’s Lames pour Couteau Chauffant Électrique and their hot-knife process notes; for foam-specific considerations, see foam cutter blades for EPS/XPS.
À propos de l'auteur
Tommy Tang is a Senior Sales Engineer at Nanjing METAL Industrial with 12 years of experience supporting industrial cutting and hot-knife applications. His work includes application support for material selection and trial validation in webbing, textiles, and foam cutting. Certifications: CSE, CME, Six Sigma Green Belt, PMP.
Technical review
This article is reviewed internally by the MAXTOR METAL manufacturing & QC team. Review scope includes material certifications (when available), incoming inspection checkpoints, first-article inspection, in-process checks, and final inspection criteria that affect blade performance.
Dernière révision : 2026-04

 English
 Spanish
 Italian
 French
 Portuguese
 Russian
 German
 Arabic
 Hindi
 Vietnamese
 Indonesian
 Japanese
 Korean