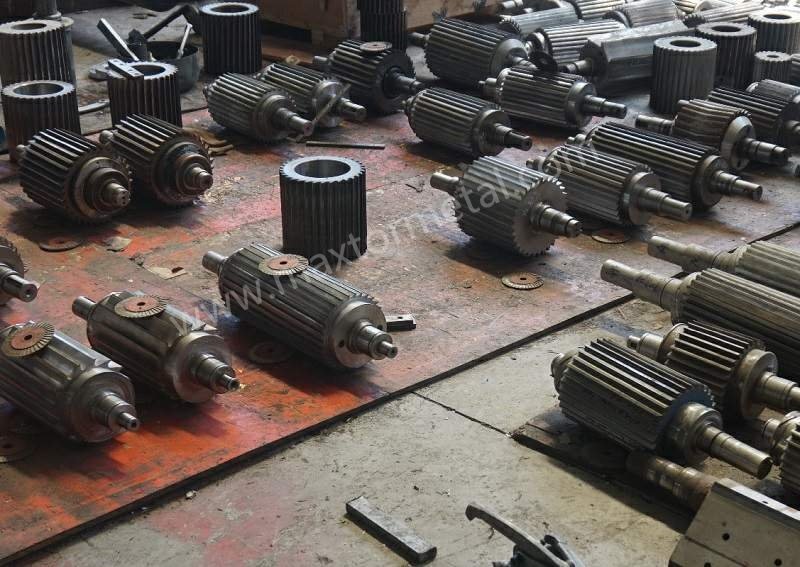
In strand pelletizing, polymer strands are guided into a rotary cutter that shears them against a fixed bed knife to create consistent pellets. A helical rotary cutter uses spiral knives rather than straight edges, so the cut occurs progressively along a helix instead of across the full width at once. At high RPM, this progressive shear spreads the cutting load over time, dampening force spikes that would otherwise excite vibration and tonal noise. Plants see practical wins from this mechanism: steadier pellet length distribution and edges, fewer fines, and longer service intervals when setup and maintenance are executed correctly.
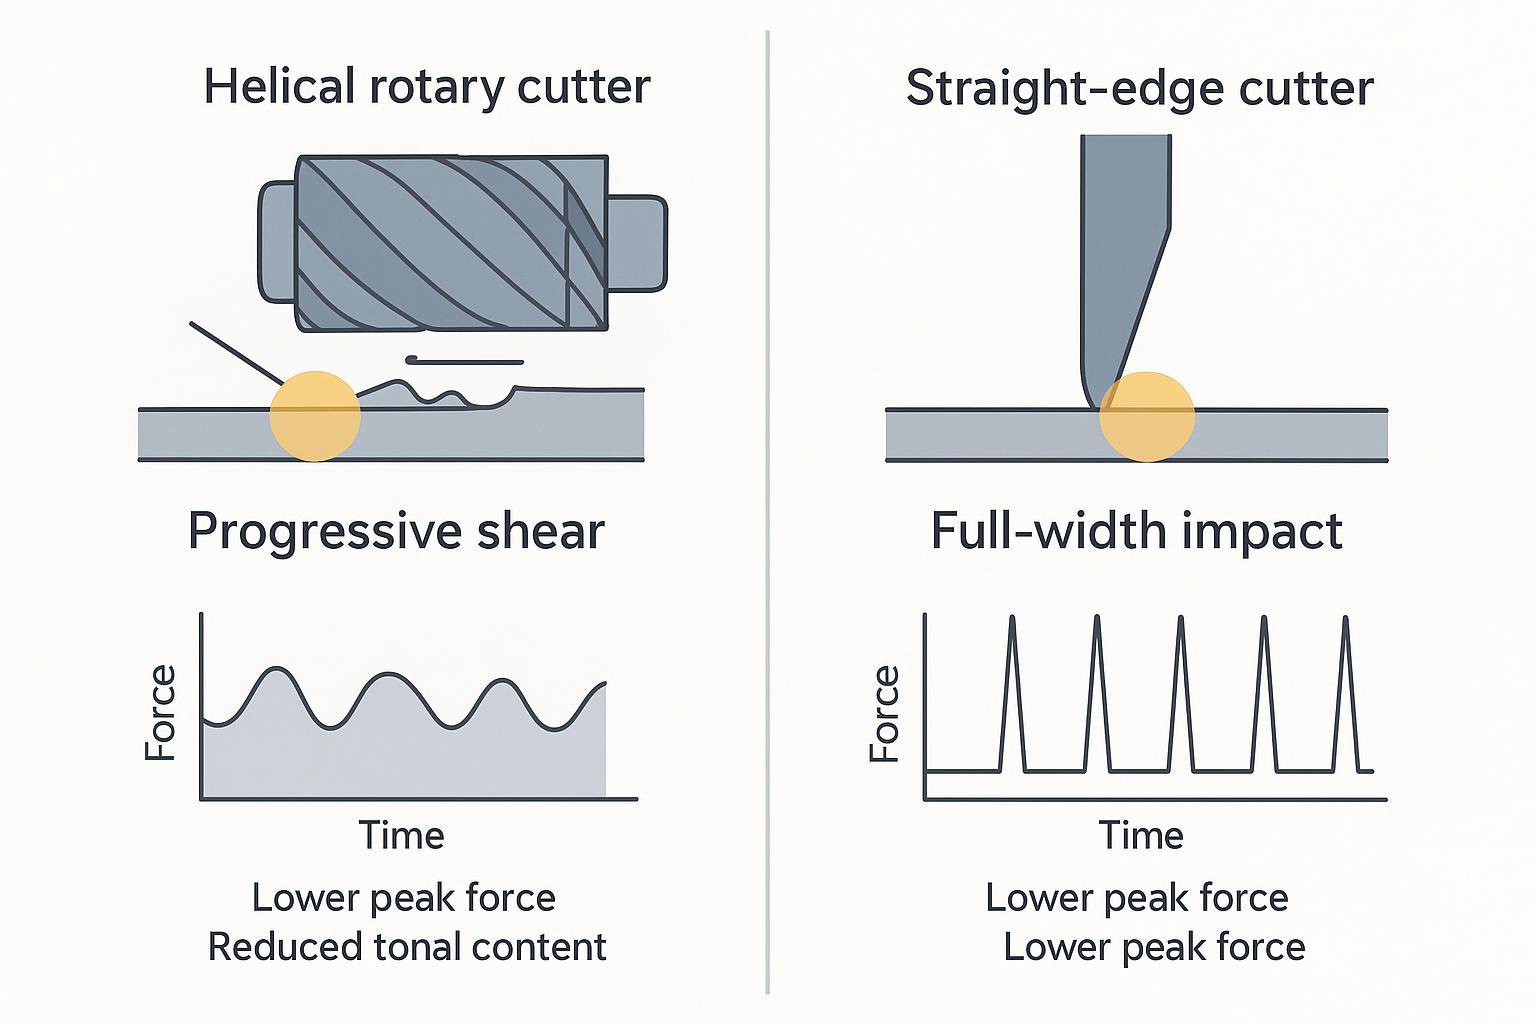
Why this matters for speed: when a cutter engages all at once, the motor and structure feel sharp impulses in a repeating pattern, which can line up with machine natural frequencies and produce a recognizable “whine.” By contrast, the helical engagement keeps the contact zone small and moving, which tends to smooth torque demand and reduce harmonic excitation. In short, quieter often follows from smoother force input.
According to public OEM documentation for premium strand and underwater systems, operator‑position noise targets are often kept below 85 dB(A) at the system level, with cutting‑gap accuracy called out as a key enabler. This is a reference point for what modern systems aim to achieve—not a statement of how much any single component (such as the rotor or knives) contributes. For context on noise expectations and the emphasis on cutting‑gap setting, see MAAG’s system brochure: MAAG M‑USG, operator‑position sound and cutting‑gap focus.
Safety note: Any work involving guards, knife settings, or speed changes should follow your OEM manual, local EHS procedures, and Lockout/Tagout requirements, and be performed by qualified personnel.
主なポイント
- Progressive shear spreads engagement over time, lowering instantaneous force and reducing tonal noise drivers at high RPM; this supports steadier pellets and fewer fines when the gap is controlled.
- Gap control is the daily lever: set a minimal, uniform knife‑to‑bed clearance per OEM guidance; verify cold and hot; re‑gap when pellet quality metrics drift.
- Balance and runout matter at speed: specify rotor balancing per ISO 21940 and keep assembly runout in micrometer ranges defined by your OEM to avoid forcing and chatter.
- Validate changes with KPIs you already track: dB(A) at operator position, fines percentage, and pellet length Cpk; log current ripple or vibration velocity if sensors are available.
- For abrasive or recycled feeds, choose wear‑resistant steels or coatings; pair regrind strategy with documentation so geometry and balance stay within limits over multiple cycles.
Mechanism & high-speed gains
Progressive engagement
A helical rotary cutter engages the bed knife along a moving line rather than a full‑width strike. At any instant, only a small portion of the edge is shearing. Think of it as “handing off” the work along the helix. The contact zone enters, does work briefly, and exits—avoiding the single, broad impulse that can excite structure‑borne noise and elevate motor amperage peaks. In strand pelletizing, this translates to a calmer cut on each strand and fewer opportunities for tails when the clearance is set correctly.
Force and harmonics
Cutting force is never truly steady, but its waveform can be shaped. With straight knives, the force can arrive in tall, periodic spikes as each edge strikes across the full face. With a helical edge, the energy is partitioned into smaller, staggered increments, reducing peak magnitude and concentrating less energy at a single tone. That shift in the force spectrum is why helical cutters often sound less “tonal” at speed. It also reduces the likelihood of coupling with machine natural frequencies.
If your facility measures motor current or vibration, you’ll often see smaller amplitude ripples with a well‑balanced helical rotor and a uniform, tight gap compared with an equivalent straight‑edge setup—all else equal. System‑level noise targets referenced by OEMs (for example, the MAAG reference above) are generally compatible with this mechanism when enclosure design, strand guides, and installation quality are also optimized.
Geometry basics
- Helix angle: Modest helix angles in polymer cutting help balance smooth shear against added axial (thrust) load. Higher angles tend to smooth engagement but can increase axial forces and edge stress. Select within your machine’s thrust capacity and polymer behavior per OEM guidance.
- Edge geometry: Edge land and included angle influence startup bite, fines generation, and life. Follow OEM or supplier recommendations for your resin family, fillers, and throughput.
- Knife count and wrap: More cutting events per revolution can raise base frequency but lower per‑event force; exact trade‑offs depend on rotor diameter, speed, and strand count.
For an accessible primer on progressive shear and pelletizer knife roles, see this educational overview: Masterbatch pelletizer blades guide (context).
Specification & setup
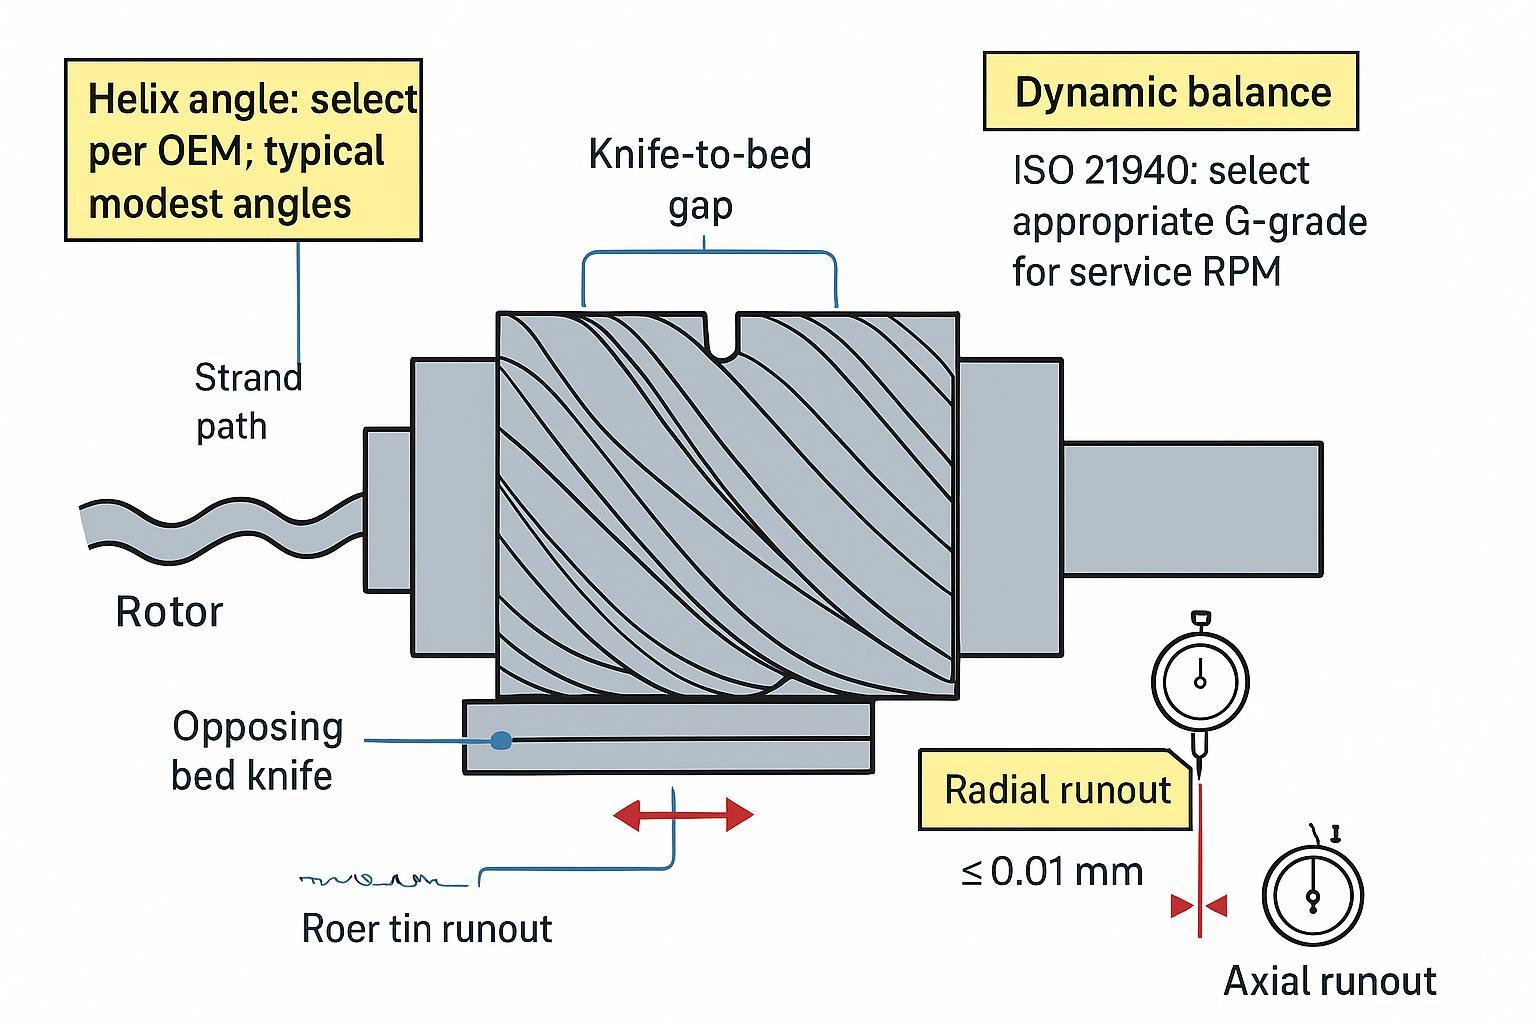
A quiet, stable helical installation is built on specification discipline and repeatable setup. That means defining the cutting gap, balance quality grade, assembly runout, and the regrind plan—and proving each with documentation.
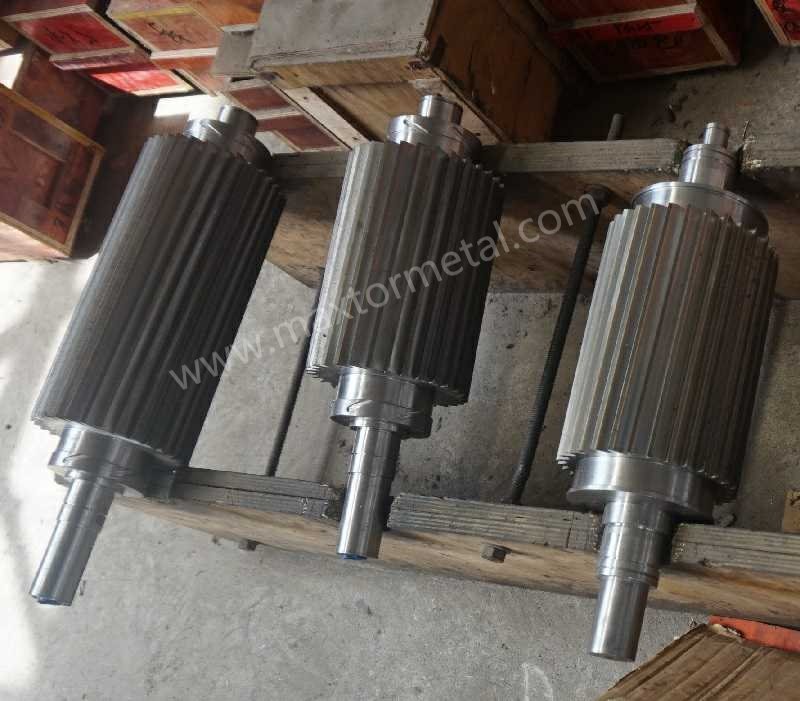
Suppliers that support production QA can simplify this work. For example, マックストールメタル can provide material and hardness data with dimensional inspection records and, upon request, balancing and runout test reports aligned to buyer acceptance criteria. Keep such documents with your line’s maintenance files to speed audits and troubleshooting.
Key specifications
- Knife‑to‑bed gap
- Target a minimal, uniform clearance per your OEM. Premium underwater/strand systems emphasize precise, repeatable gap setting to stabilize pellet quality and noise. Public documentation highlights the importance of “cutting gap setting” rather than prescribing a universal value; always defer to the machine manual. See the OEM perspective here: MAAG M‑USG, emphasis on cutting‑gap accuracy.
- Dynamic balance (ISO 21940)
- Specify rotor balancing to ISO 21940 with an appropriate G‑grade for the service RPM and sensitivity of your cutter/line. High‑speed, precision cutting applications commonly require tighter grades; confirm the grade and verification method with your OEM and supplier.
- Runout (assembly and installed)
- Control radial and axial runout to OEM‑specified micrometer limits. Measure on the rotor journals/knife faces with dial indicators and re‑verify after regrinds and reassembly. Even small increases in runout can widen effective gap, elevate fines, and add tonal content.
- Materials and coatings (for abrasive/recycled feeds)
- For glass‑filled or high‑recycle blends, consider powder‑metallurgy tool steels or carbide‑tipped knives, and coatings such as TiN/TiAlN or chromium to reduce friction and wear. Match hardness and coating to your coolant/wet environment as applicable. For an educational overview of blade materials in plastics service, see this context piece: Industrial blades for plastic processing.
Setup and gap control
A simple, repeatable SOP improves noise and quality as much as a new rotor. Below is a model‑agnostic procedure—adapt specifics (torques, gauges, target clearances) to your OEM manual.
- Preparation (Lockout/Tagout, cleanliness)
- Lockout the drive. Clean rotor and bed‑knife seating faces. Install matched, sharpened knives; verify fasteners and keys.
- Cold alignment and initial gap
- Set the bed knife using your OEM’s mechanism (commonly push/pull bolts on the bed‑knife holder, or eccentric adjustment depending on model). Aim for a minimal, uniform clearance. Check multiple positions along the cut line with feeler or leaf gauges appropriate to your model. Sweep parallelism with a dial indicator across the bed‑knife face; correct taper. For publicly available examples of these adjustment concepts, see Bay Plastics Machinery’s strand‑pelletizing training material (push/pull gap adjustment) and MAAG’s T200 series overview (eccentric rotor‑to‑bed adjustment): BPM Training PDF, MAAG T200 series.
- Balance/runout verification
- If the rotor was serviced, review the latest ISO 21940 balance certificate and measure installed radial/axial runout at specified points. Record values on the job traveler.
- Hot verification
- Warm the line to operating temperature and RPM under typical load. Stop safely and recheck accessible points (or use in‑situ gauges if designed) to account for thermal growth. Adjust per OEM guidance if a “hot” target clearance is specified.
- Acceptance checks
- Resume production and observe pellet edges, fines percentage, and motor current ripple. If tails, sudden fines, or tonal noise rise, re‑inspect for contamination under the bed knife, gap drift, or edge wear.
For background on system‑level expectations (operator‑position noise) and the importance of accurate cutting‑gap setting, see the MAAG reference cited earlier.
Troubleshooting quick matrix
| Symptom you see/hear | Likely cause (most common first) | What to do next (in order) |
|---|---|---|
| More fines / dusty pellets | Gap opened up, edge dulling, contamination under bed knife | LOTO → clean seating faces → re‑set gap cold → verify at multiple positions → inspect edge land/chips |
| Tails or inconsistent length | Gap non‑uniform (taper), runout increased, strand guide misalignment | Check parallelism with dial indicator → check runout at OEM points → correct taper → verify strand guides |
| Rising tonal “whine” at steady RPM | Balance drift after service, runout growth, resonance excited by forcing | Review last balance cert → measure vibration/current ripple trend → re‑verify runout → correct unbalance per ISO 21940 plan |
| Motor current ripple increases | Intermittent contact from runout or gap drift, uneven knife set | Confirm matched knife set and fastener torque → re‑gap hot if required → re‑check runout |
| Noise rises but pellets look OK | Enclosure/guide changes, airflow paths, measurement point changed | Confirm measurement position/time window → inspect guards/enclosure panels and strand guide section for looseness |
Always follow your OEM manual and EHS procedures; do not bypass guards or adjust settings on a running machine unless the equipment is explicitly designed for in‑situ adjustment.
Regrind and wear
Edge wear widens the effective gap and elevates fines and noise. Keep geometry within limits and document each cycle.
- Triggers: Regrind when fines and tails exceed your internal limits, when length Cpk trends down, or at the OEM’s edge‑land threshold.
- Balance after service: If mass was removed asymmetrically, rebalance the rotor per your specified ISO 21940 grade.
- Rotation strategy: Rotate knives/edges as prescribed to distribute wear.
- Records: Log hours/throughput, gap checks, geometry after grind, balance cert numbers, and runout readings. This history speeds root‑cause work if quality drifts.
Validation & procurement
KPIs and trials
Treat changes like engineering trials. Change one variable at a time, then measure in steady state.
- Noise: Measure dB(A) at operator position using your plant’s method aligned with the ISO 11200 family for machinery noise in situ; compare to your site targets and OEM expectations (e.g., modern systems often target <85 dB(A) at the operator position per MAAG M‑USG).
- Product quality: Sample fines percentage by sieving at timed intervals after warm‑up. For pellet length, compute Cpk from a defined sampling plan (e.g., multiple pulls over 30–60 minutes) and track alongside gap/balance notes.
- Machine health: Where available, log motor current ripple and vibration velocity (mm/s). Look for reductions in peak‑to‑peak and tonal components when gap/runout are tightened.
Documentation checklist
Provide and retain documents that prove what you specified is what you received and installed. The items below are commonly requested in audits and RFQs.
| Document | 目的 | Notes/Standard |
|---|---|---|
| Material test certificate | Confirms grade/chemistry and test results for the batch | Prefer EN 10204 3.1 for traceability; overview: TWI—material test certificates / EN 10204 context |
| Hardness report | Verifies HRC or HV at defined locations | Include method, location map, acceptance range |
| Dimensional inspection | 重要寸法、平面度、および平行度を確認 | 公差付き図面を添付。必要に応じて表面仕上げを記載 |
| 動バランス証明書 | 適用されたISO 21940等級および使用回転数(RPM)を記載 | 最終残留不平衡量および修正面を含める |
| 振れ精度レポート(組立時/取り付け後) | 指定点におけるラジアル振れおよびアキシャル振れを記録 | 測定セットアップおよびインジケータの位置を記録 |
| コーティング仕様(使用する場合) | コーティングの種類および膜厚を明記 | 処理プロセス(PVD/CVD/メッキ)および後処理を注記 |
| 再研磨・メンテナンス記録 | サイクルごとの形状、バランス、および寿命を追跡 | トレーサビリティのためのシリアル番号/ヒート番号への関連付け |
互換性およびリードタイム
事前に形状およびインターフェースを確認することで、予期せぬ不具合を回避します。.
- 形状およびインターフェース:OEMに基づくねじれ方向/角度、刃先形状、孔/スロットパターン、キー溝、および厚み/外径を確認します。管理図面を共有し、可能であればサンプルまたは詳細写真を提示してください。.
- バランス/振れ許容値:発注書(PO)にISO 21940 G等級、測定面、および振れ許容値を記載し、貴社現場での受入検査方法を明確にします。.
- 再研磨の運用ローテーション:稼働中の刃が交換基準に達した際、文書化された研磨済みの予備セットが常に用意されているよう在庫を計画します。サプライヤーのリードタイムをメンテナンス期間と同期させます。.
テスト記録用記入例(入力テンプレート)
A/Bテスト(例:「クリアランス絞り込みSOP」、「再研磨直後のナイフ」、「新規ヘリカルローター」)の1ページ記録としてご活用ください。テスト期間と測定方法は一定に保ってください。.
| Category | 記録項目 | 注記 |
|---|---|---|
| 騒音測定 | 測定位置(作業者位置)、距離、測定器/型式、周波数補正(A特性)、平均化/時間ウィンドウ、暗騒音に関するメモ | 貴社現場でISO 11200シリーズの手法を使用する場合は、EHSチームが準拠する具体的な手順を記載してください |
| 運転条件 | 樹脂グレード、フィラー/リサイクル率%、処理量、回転数(RPM)、冷却方法、ストランド数 | 実質的に変更された項目のみを記録 |
| 切断設定 | 固定刃と回転刃の間隙(常温時)、固定刃と回転刃の間隙(温調/定常状態時、該当する場合) | 単位と切断線上の測定位置を必ず記録してください |
| 装置の状態(マシンヘルス) | ラジアル/アキシャル振れ測定値(測定ポイント)、振動(mm/s、可能な場合)、モーター電流リップル測定法 | 毎回同じ測定ポイントを参照してください |
| 品質KPI | 微粉率%測定法(ふるい目/時間)、ペレット長サンプリング計画、ペレット長Cpk、外観不良(テール、欠け) | サンプリングシートがある場合は添付してください |
| メンテナンス記録 | ナイフセットID/シリアル、再研磨回数、主要寸法形状メモ、バランス証明書ID(ISO 21940)、振れレポートID | これにより、結果の監査可能性と再現性が確保されます |
結論
段階的なヘリカル噛み合い(連続剪断)により、ピーク切削力および高速運転時に構造体を共振させる周波数音を低減します。このメカニズムを厳格な仕様(適切かつ均一なクリアランス、正確なバランス、低振れ)と組み合わせることで、工場では作業者位置での体感騒音の低減、微粉発生率の減少、ペレット長Cpkの改善といった重要な成果を得ることができます。リスク管理は「期待」ではなく、明文化された仕様書、SOP、文書化された品質保証(QA)によって行われ、体系的なテストおよび定期的測定によって検証されます。.
研削性の高い原料やリサイクル原料を使用する場合は、使用環境の摩耗に耐えうる材質およびコーティングを選定し、再研磨サイクルごとにバランスと振れ精度を維持してください。「仕様規定、検証、記録、調整」のサイクルを確立することで、ストランドペレタイズラインが本来備えている静音かつ安定した高速切断性能を実現できます。.
About the author: Tommy Tangは、Nanjing METAL Industrialのシニアセールスエンジニアであり、産業用刃物アプリケーションのサポートにおいて12年の経験を有しています。保有資格:CSE、CME、シックスシグマ・グリーンベルト、PMP。.
手法および適用範囲: 本ガイドは、公開されているOEMドキュメント(例:MAAGシステムのパンフレットなど)、一般的な工場のKPI(dB(A)、微粉率%、ペレット長Cpk、電流リップル/振動)、および標準用語(例:バランス調整に関するISO 21940)を総合したものです。具体的なクリアランス、締め付けトルク、および許容限界値は、 装置のモデルによって異なります—OEMのマニュアルおよび貴社現場のEHS手順を優先的な基準としてご参照ください。.
 English
 Spanish
 Italian
 French
 Portuguese
 Russian
 German
 Arabic
 Hindi
 Vietnamese
 Indonesian
 Japanese
 Korean