

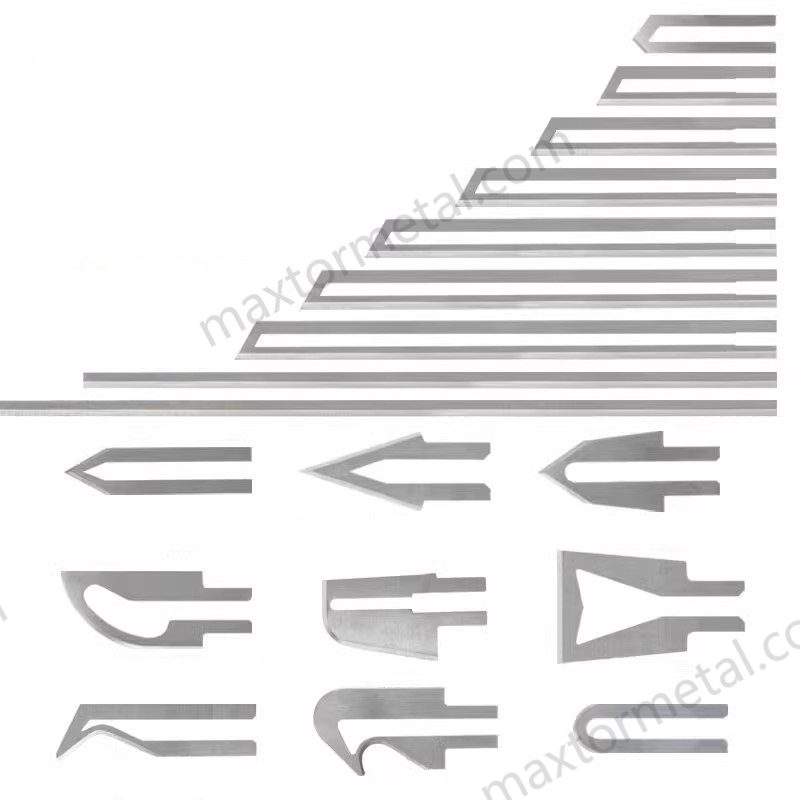
Hot knife blades work in the messy intersection of heat, polymers, and production pressure. When residue builds up, you don’t just get a dirty blade—you get unstable cut quality, more scrap, longer changeovers, and higher total cost of ownership (TCO) through unplanned downtime and premature regrinds.
In practice, “clean hot knife blades” means removing carbonized film, molten polymer smear, adhesive transfer, and dust without changing the blade geometry. Done right, cleaning restores consistent heat transfer and predictable cutting—without rounding the edge or attacking any non-stick or wear-resistant coatings.
In this guide, you’ll learn a safety-first hot knife maintenance SOP—a practical way to handle hot knife blade cleaning, choose compatible cleaners, and build habits that keep residue from becoming a weekly firefight.
Byline & review
Tác giả: Liang Chen, Senior Application Engineer (Industrial Hot-Cut Blades), MAXTOR METAL — 15+ years in custom, precision-ground industrial blades.
Đánh giá kỹ thuật: Reviewed by MAXTOR METAL Quality Team (materials inspection & in-process QC) — April 2026.
Questions or site-specific constraints? Contact our team: https://maxtormetal.com/
An toàn là trên hết
Safety & compliance note: This guide is for general maintenance planning and does not replace your facility’s lockout/tagout program, EHS requirements, or the cleaner manufacturer’s Safety Data Sheet (SDS). Always follow your site SOP first, confirm chemical compatibility with blade material/coatings, and consult SDS Section 7 (Handling & Storage), Section 8 (Exposure Controls/PPE), Và Section 13 (Disposal) before using or disposing of any solvent or contaminated wipes.
Lockout, cool, verify
Treat cleaning like maintenance, not housekeeping. De-energize the system, lock out the power source, and verify zero energy state before you touch the blade or holder. For program-level guidance, OSHA summarizes the intent of 29 CFR 1910.147—control of hazardous energy: prevent unexpected energization or release of stored energy during servicing and maintenance.
Cooling is non-negotiable. As Carolina Knife notes in its guide to maintaining an industrial hot knife (2025), cleaning should be done only after the tool has completely cooled.
Use a simple verification step before you start:
- Confirm the heater/controller is off and locked out.
- Wait for the blade to reach a safe-handling temperature.
- Verify with an IR thermometer or contact probe if your SOP requires it.
PPE and ventilation
Hot knife residue can include fine particulates, degraded polymers, and solvent vapors. PPE and ventilation aren’t optional—especially if you’re cleaning multiple blades per shift.
Minimum baseline:
- Cut-resistant gloves (appropriate level for your blade size and handling)
- Eye protection
- Respiratory protection if your solvent SDS or residue type requires it
- Local exhaust or well-ventilated work area
Solvent and waste handling
Choose cleaners that are compatible with your blade material and any coating. Use the solvent’s SDS as your rulebook for handling, ventilation, and disposal.
Keep the process controlled:
- Use small amounts on wipes rather than open-bucket soaking.
- Segregate solvent wipes and residue as process waste per your site rules.
- Don’t rinse solvents into drains unless explicitly permitted by the SDS and your EHS policy.
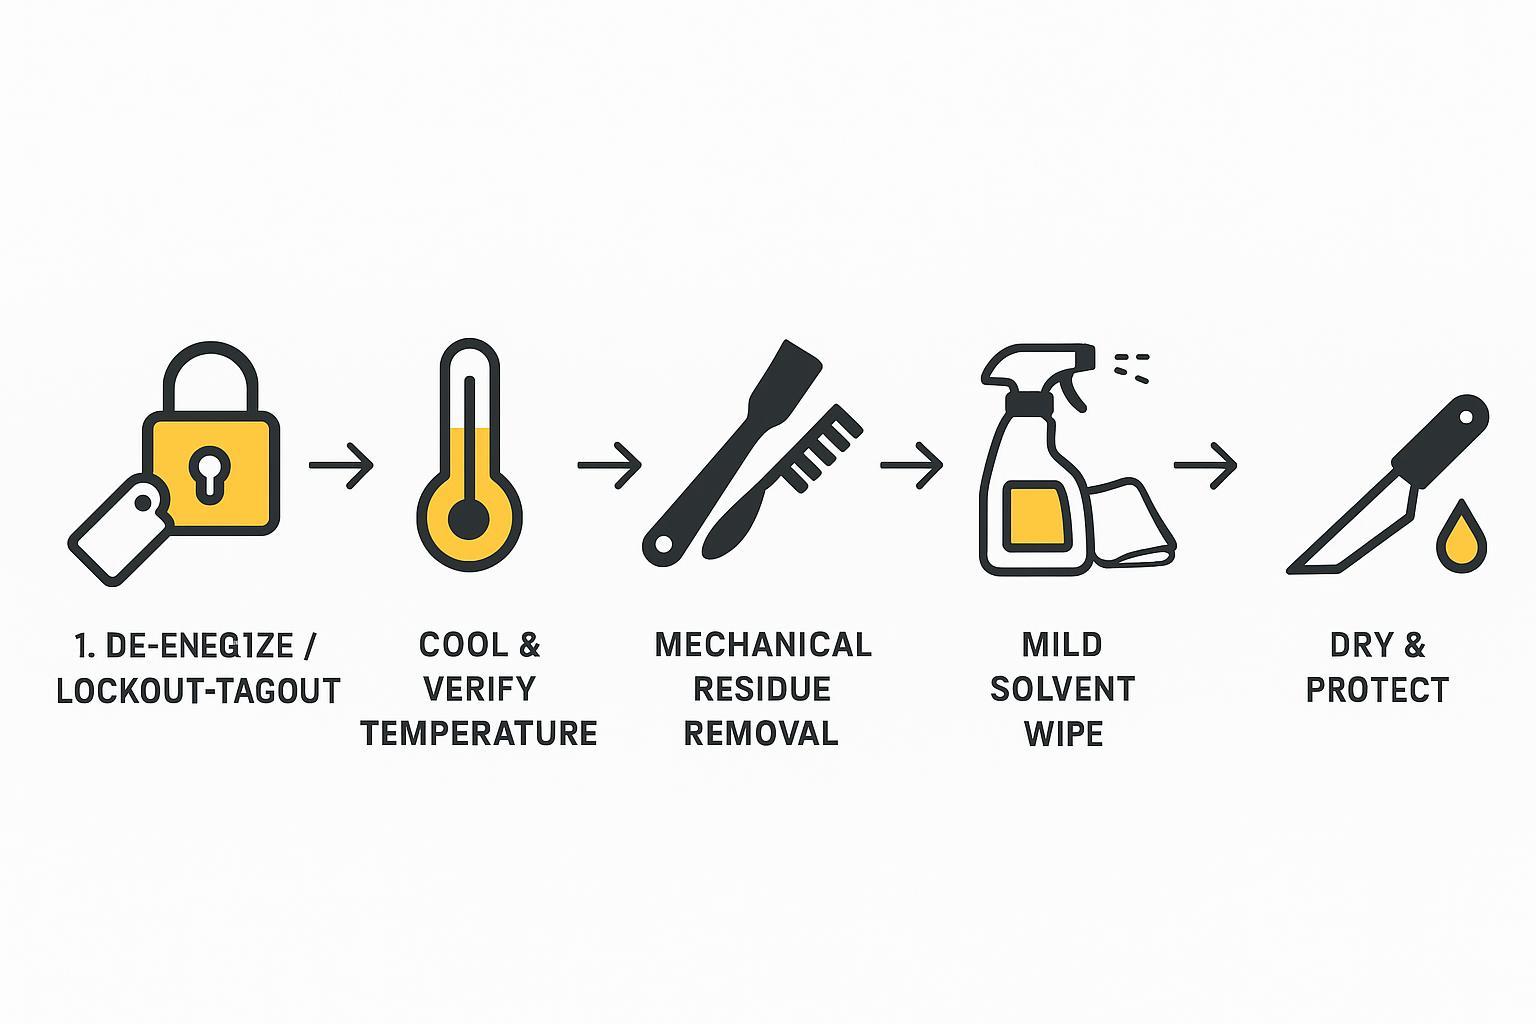
Clean step-by-step
Mechanical removal first
Start dry and gentle. Mechanical removal is the lowest-risk way to remove bulk residue without pushing chemicals under coatings or softening adhesives into a smear.
Một trình tự thực tế:
- Use a nylon or wood scraper to lift thicker deposits.
- Use a brass brush (light pressure) or a coarse cloth to remove remaining film.
- Wipe the blade face and edge line with a clean microfiber cloth.
Two edge-protection rules that prevent accidental dulling:
- Scrape away from the edge when possible; don’t “dig under” the apex.
- Avoid hard abrasives that change geometry (no sanding belts, no grinding stones, no aggressive Scotch-Brite on the edge).
If your main issue is buildup, focus on removing bulk residue first; trying to remove plastic residue from hot knife blade surfaces with aggressive scrubbing is a common way to round the edge.
Escalate with compatible solvents
If mechanical removal leaves a sticky film, escalate in controlled steps. Your goal is to dissolve residue with the mildest chemistry that works—then stop.
Use a “test small, wipe fast” approach:
- Apply a small amount of cleaner to a cloth (not directly onto hot components).
- Wipe the residue, then immediately wipe again with a clean cloth.
- If your process allows water-based cleaners, rinse/wipe per the product instructions and dry fully.
Compatibility notes that prevent damage:
- Prefer mild, non-caustic cleaners first.
- Avoid leaving solvent pooling at the blade/holder interface.
- If the blade is coated (for example PTFE), avoid aggressive solvents and hard scrubbing that can lift or scratch the coating.
Cleaner escalation decision tree for uncoated steel blades
If your shop primarily uses uncoated carbon steel or stainless steel hot knife blades, a simple escalation path keeps cleaning consistent without jumping to aggressive chemistry.
Start here and escalate only if needed:
- Dry wipe (lint-free cloth): If residue is light powder/soot and wipes clean.
- Mechanical lift (nylon/wood scraper): If you have smeared polymer film or thick deposits.
- IPA wipe (isopropyl alcohol): If you have light oil, tacky film, or thin polymer smear. Apply IPA to a cloth, wipe, then follow with a dry cloth.
- Adhesive/paint remover: Only when residue is clearly adhesive/paint transfer and IPA won’t touch it. Use small amounts, verify the product SDS, and confirm it’s approved for your blade steel and any nearby seals/holders.
Stop rules that protect the edge:
- If residue doesn’t improve after two short cycles at a given step, don’t scrub harder—move to the next step or review process parameters (temperature, dwell, feed).
- If a remover leaves a haze/film, follow the product instructions, then finish with a clean wipe and thorough dry-down.
Mini compatibility matrix
| Blade surface | OK to start with | Escalate to | Avoid unless manufacturer/EHS approves |
|---|---|---|---|
| Uncoated carbon steel | Dry wipe, nylon/wood scrape | IPA wipe | Chất ăn mòn mạnh; ngâm lâu; chất mài mòn mạnh trên cạnh cắt |
| Thép không gỉ không phủ | Dry wipe, nylon/wood scrape | Lau bằng IPA; chất tẩy keo/sơn được phê duyệt | Chất ăn mòn mạnh; hóa chất tẩy không rõ nguồn gốc trên đồ gá/gioăng phớt; chất mài mòn mạnh trên cạnh cắt |
Lời nhắc nhở: Luôn kiểm tra SDS của chất tẩy rửa—đặc biệt là Section 7 (Handling & Storage), Section 8 (Exposure Controls/PPE), Và Section 13 (Disposal)—và tuân thủ các quy tắc EHS tại nhà máy về thông gió, găng tay và phân loại chất thải.
Mẹo chuyên nghiệp: Nếu bạn quản lý nhiều loại lưỡi dao, hãy tiêu chuẩn hóa chất tẩy rửa theo nhóm lưỡi dao/lớp phủ (thép không phủ so với phủ PTFE so với các lớp phủ khác) và dán nhãn các bộ dụng cụ vệ sinh tương ứng. Để có bối cảnh bảo dưỡng rộng hơn, các Mẹo bảo dưỡng lưỡi dao công nghiệp là những danh mục kiểm tra cơ bản hữu ích.
Làm khô và chống ăn mòn
Làm khô là một phần của quá trình vệ sinh. Độ ẩm dư thừa và màng chất tẩy rửa có thể gây ăn mòn, hoen ố hoặc truyền nhiệt không đều trong lần vận hành tiếp theo.
Một quy trình hoàn thiện đơn giản, dễ lặp lại:
- Lau khô bằng khăn không xơ.
- Chỉ sử dụng khí nén nếu quy định của nhà máy cho phép và bạn có thể kiểm soát được mảnh vụn.
- Phủ một lớp mỏng chất chống gỉ hoặc màng dầu nhẹ nếu quy trình của bạn cho phép (đặc biệt là khi lưu kho).
Trước khi lắp đặt lại, hãy thực hiện kiểm tra nhanh:
- Không có vết cặn bẩn bám trên bề mặt lưỡi dao.
- Không bị dính trên cạnh cắt.
- Khu vực tiếp xúc giữa lưỡi dao và gá đỡ sạch và khô.
Protect the edge and coating
Giới hạn của PTFE và thép
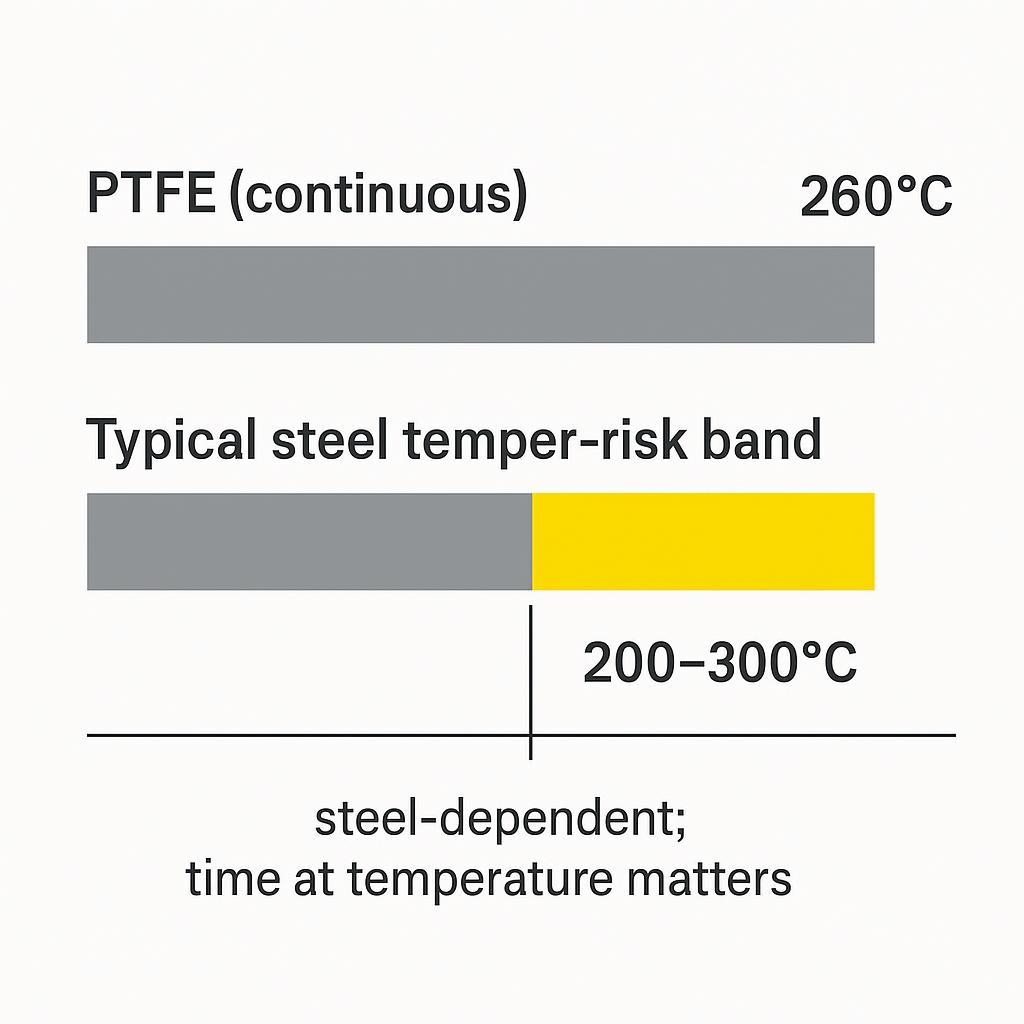
Hai thực tế về nhiệt độ giúp bạn thiết lập các quy tắc vệ sinh an toàn hơn.
Đầu tiên, lớp phủ PTFE có giới hạn nhiệt độ thực tế: Teflon.com mô tả các fluoropolymer như PTFE có khả năng chịu nhiệt trong khoảng từ -200 đến 260°C trong tài liệu tổng quan về khả năng kháng hóa chất và chịu nhiệt, và lưu ý rằng nhựa PTFE được định mức cho hoạt động liên tục ở 260°C (500°F) trên đó trang sản phẩm PTFE.
Thứ hai, độ cứng và độ dẻo dai của thép có thể thay đổi khi bạn nung nóng lại vào phạm vi ram. American Bladesmith Society lưu ý rằng độ cứng bắt đầu giảm đáng kể ở khoảng 375–400°F trong tài liệu Thảo luận về ram thép trong Heat Treating 101 (2010). Đối với các SOP tại xưởng sản xuất, bài học thực tế rất đơn giản: không sử dụng phương pháp “nung nóng.
Để biết thêm thông tin về lớp phủ (tác dụng của lớp phủ, chúng hỗ trợ ở đâu và quy trình bảo dưỡng thường như thế nào), hướng dẫn về lớp phủ lưỡi dao công nghiệp này is a useful reference.
Những điều cần tránh
Hầu hết các hư hại ở cạnh sắc đều bắt nguồn từ việc làm tắt. Hãy đưa những điều này vào danh sách “không được làm” của bạn:
- Vệ sinh khi còn nóng: làm tăng nguy cơ bị bỏng, tạo ra cặn bẩn lem nhem và dễ dẫn đến việc lạm dụng nhiệt độ cao như một “giải pháp”.”
- Chà xát quá mạnh các bề mặt có lớp phủ: đối với việc vệ sinh lưỡi dao phủ PTFE, hãy sử dụng các chất tẩy rửa nhẹ và dụng cụ mềm; hãy coi lớp phủ là một bề mặt chức năng, chứ không phải là vết bẩn cần mài sạch.
- Chất mài mòn trên cạnh sắc: bùi nhùi thép, miếng chà nhám mạnh, giấy nhám hoặc việc cạo vào phần đỉnh sẽ làm tròn cạnh sắc.
- Chất tẩy rửa ăn mòn không được phê duyệt: chất kiềm mạnh và chất tẩy dầu mỡ mạnh có thể ăn mòn một số lớp phủ nhất định và làm biến đổi màu thép.
- Ngâm các bộ phận có điện: không ngâm bộ phận gia nhiệt, tay cầm, dây dẫn hoặc bộ điều khiển vào nước.
- Dụng cụ cạy hoặc đục bằng kim loại: fast way to chip an edge or gouge a coated surface.
Prevent future buildup
Prevention is mostly about control and cadence, not stronger chemicals. The goal is to keep residue from becoming a baked-on layer.
If you need a formal hot knife maintenance SOP for audits, include: the approved cleaner list by blade/coating type, a cool-down verification step, and a sign-off point after the test cut.
Operational habits that work across shifts (see hot cut knife maintenance tips for a simple cadence model):
- Wipe-down cadence: light wipe at shift end beats aggressive weekly cleaning.
- Parameter discipline: avoid running hotter than required; stabilize feed speed and dwell to reduce smear.
- Edge checks: add a simple “test cut” check after cleaning to confirm the cut line is stable.
- Tài liệu: log cleaner type, frequency, and any coating/edge observations so you can correlate residue with jobs and materials.
MAXTOR METAL supports custom blade materials and non-stick/wear-resistant coatings (including PTFE and hard coatings) plus precision grinding, which can help match cleanability and edge stability to your specific hot-cut application.
Case example: TPU catheter hot-cut cleanup that reduced scrap
Here’s a real shop-floor example where cleaning discipline mattered as much as the edge itself.
In a medical-grade TPU (thermoplastic polyurethane) catheter hot-cut process, operators saw high-viscosity molten polymer smear plus small carbonized particles build up on the blade face over continuous heating.
Symptoms before cleaning included blade sticking and “stringing” at the cut line, plus end-face deformation on thin-wall tubing from increased friction—pushing parts out of medical tolerance.
Standardized cleaning sequence:
- Mechanical removal (controlled): After the blade is locked out and cooled to a safe handling temperature, use a soft brass brush to remove visible residue. Keep pressure light and brush away from the edge line to avoid rolling the apex.
- Solvent wipe (after cool-down): After the blade cools to a safe handling temperature, wipe with an IPA (isopropyl alcohol) dampened, industrial lint-free cloth to remove remaining film and fine oxidation.
Measured results after standardization:
- Scrap rate from cut-end defects dropped from 8% ĐẾN below 0.5%.
- Unplanned downtime for blade changeouts fell by about 35% due to preventive cleaning cadence.
Kết luận
Clean hot knife blades like a controlled maintenance task: clean only when cool, start with mechanical removal, escalate with mild compatible solvents, then dry and protect. That sequence protects the edge, preserves coatings, and keeps your cut quality stable.
Next steps:
- Document your SOP (lockout, cool-down verification, approved tools/solvents, drying/protection).
- Train across shifts and audit compliance (especially PPE and ventilation).
- Review your solvent list quarterly against coating types and updated SDS requirements.

 English
 Spanish
 Italian
 French
 Portuguese
 Russian
 German
 Arabic
 Hindi
 Vietnamese
 Indonesian
 Japanese
 Korean