

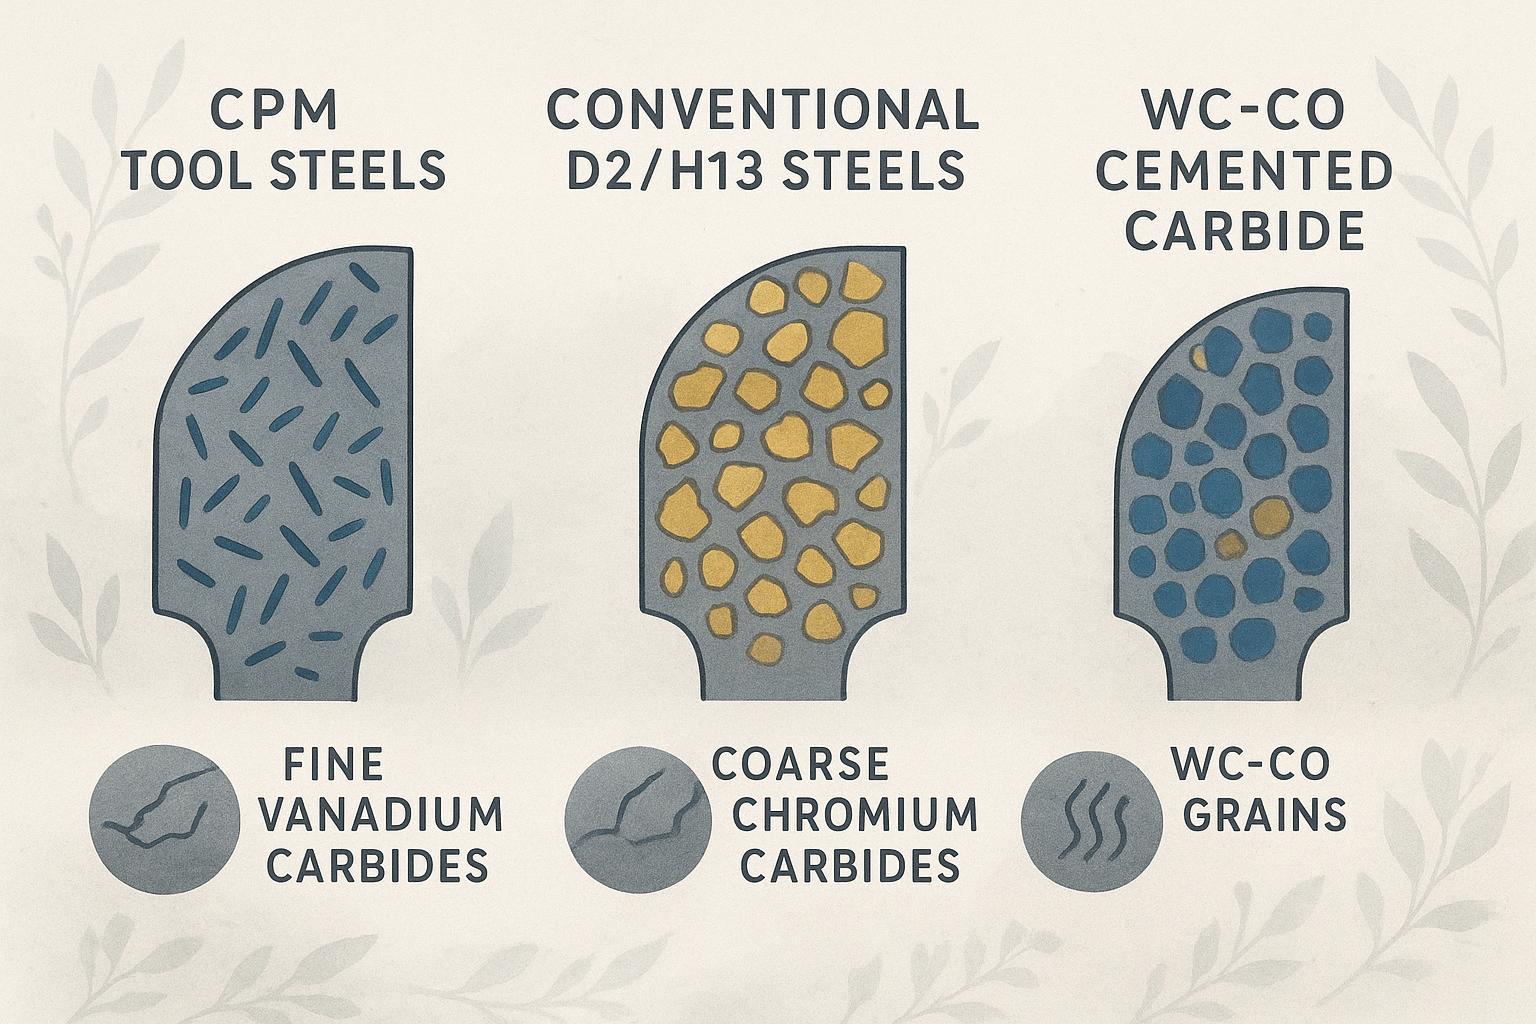
Das Granulieren unter hoher Belastung beansprucht Schneidkanten durch abrasive Füllstoffe, stoßartige Belastungen und Hitze extrem. Es gibt keinen Universalsieger. Wenn Ausbrüche an der Schneidkante Ihr Hauptproblem sind, übertreffen CPM-Werkzeugstähle in der Regel konventionellen D2 und binderarme Hartmetalle. Wenn unter konstanter Last rein abrasiver Verschleiß dominiert, bietet Hartmetall die längste Standzeit und die meisten Nachschliffe. Bei Hitzeentwicklung und thermischer Erweichung machen CPM M4 oder Warmarbeitsstähle in Kombination mit hitzebeständigen Beschichtungen den entscheidenden Unterschied.
Wichtigste Erkenntnisse
- Das dominierende Schadensbild beim Hochleistungsgranulieren sind Ausbrüche/Mikrorisse an der Schneidkante; wählen Sie Werkstoffe und Wärmebehandlungen, die die Zähigkeit bei der Arbeitshärte erhöhen.
- CPM-Granuliermesser bieten durch feine, gleichmäßig verteilte Vanadiumkarbide ein ausgewogenes Verhältnis von Verschleißfestigkeit und Zähigkeit; CPM 9V ist meist führend in der Ausbruchsicherheit unter den Stählen, während CPM 10V eine noch höhere Verschleißfestigkeit erzielt.
- D2/SKD11 bietet guten abrasiven Verschleißschutz, enthält jedoch gröbere Chromkarbide, die das Risiko von Ausbrüchen bei Stoßbelastung oder Fehlausrichtung erhöhen.
- Hartmetall (WC–Co K10–K20) ist unschlagbar bei reinem abrasiven Verschleiß und bietet höchste Formstabilität bei konstanter Belastung, allerdings steigt das Ausbruchsrisiko bei sinkendem Co-Bindergehalt.
- Bei Hitze und thermischer Erweichung behalten CPM M4 mit TiAlN sowie der Warmarbeitsstahl H13/SKD61 ihre Härte bei hohen Temperaturen besser als Kaltarbeitsstähle.
- Beschichtungen wie TiCN (gegen Abrieb) und TiAlN (gegen Hitze) können die Werkzeugstandzeit verlängern; stimmen Sie diese auf das Substrat und das Schadensbild ab.
Direkter Vergleich (Richtwerte — genaue Werte siehe Datenblätter)
| Bestes Szenario für | Werkstoffgruppe & Beispielgüten | Besonderheiten der Mikrostruktur | Typisches Härtefenster | Widerstand gegen Schneidkantenausbrüche | Abrasionsbeständigkeit | Warmhärte / Anlassbeständigkeit | Widerstand gegen plastische Verformung | Nachschliffzyklen & Stabilität | Eignung für Beschichtungen/Behandlungen | Hinweis zur Lebenszyklus-Wirtschaftlichkeit | Verfügbarkeit / Lieferzeit | Schnellbewertung (Hochleistungsgranulieren) |
|---|---|---|---|---|---|---|---|---|---|---|---|---|
| Hohe Abrasivität — konstante Belastung | WC–Co Hartmetall (K10–K20) | WC-Körner in Co-Binder; Korngröße und Co-Gehalt bestimmen die Zähigkeit | HRA ~93–94.5 (sortenabhängig) | Mittel bis gering (verbessert sich bei höherem Co-Gehalt) | Sehr hoch | Hervorragend (Hartmetall behält seine Härte bei hohen Temperaturen) | Hoch bei konstanter Belastung; spröde bei Stoßbelastung | Ermöglicht oft viele Nachschliffe; enge Toleranzen | TiN/TiCN; in bestimmten Fällen Hochtemperatur-CVD vermeiden | Hohe Anschaffungskosten; lange Standzeit bei minimaler Stoßbelastung | Mittlere Lieferzeit | 8/10 |
| Hohes Ausbruchsrisiko bei Stoßbelastung/Fehlausrichtung | CPM-Werkzeugstähle (CPM 9V, CPM 10V) | Feine VC-Karbide; homogene PM-Matrix | ~HRC Mitte 50 bis 62–64 (10V am oberen Ende) | Hoch (9V > 10V) | Hoch (10V zeichnet sich aus) | Gute Anlassbeständigkeit (PM) | Gut; verringerte Sprödbruchgefahr im Vergleich zu D2 | Gute Schleifbarkeit; stabil über mehrere Nachschliffe | TiCN bei abrasivem Verschleiß; TiAlN bei Hitze | Mid cost; strong uptime where chipping dominates | Mittlere Lieferzeit | 9/10 |
| Elevated temperature / thermal softening | CPM M4 (HSS) and H13/SKD61 | Carbide profile supports hot hardness; H13 tuned for hot work | HRC ~58–62 (M4); H13 lower room‑temp wear | Medium‑high (M4) / High (H13 toughness) | Medium‑high (M4) / Medium (H13) | Very good (M4, H13) | High; edges resist rolling at temp | Good stability; H13 robust to thermal cycles | TiAlN (heat); nitriding for fatigue | Mid cost; reduced heat‑related downtime | Short to medium lead time | 7/10 |
| Budget/availability with coatings | D2/SKD11 (cold‑work) | Coarse M7C3 chromium carbides; banding risk in ingot steel | HRC ~60–62 | Low‑medium; chipping risk under impact | Hoch | Mäßig | Moderate; edge can chip rather than roll | Acceptable; watch for grinding microcracks | TiCN for abrasives; chrome for corrosion | Low cost; may need more frequent regrinds | Short lead time | 6/10 |
Footnote: Values are indicative and scenario‑weighted. For exact heat‑treat windows and property curves, consult manufacturer datasheets.
CPM-Granuliermesser — warum Vanadiumkarbide und PM-Mikrostruktur entscheidend sind
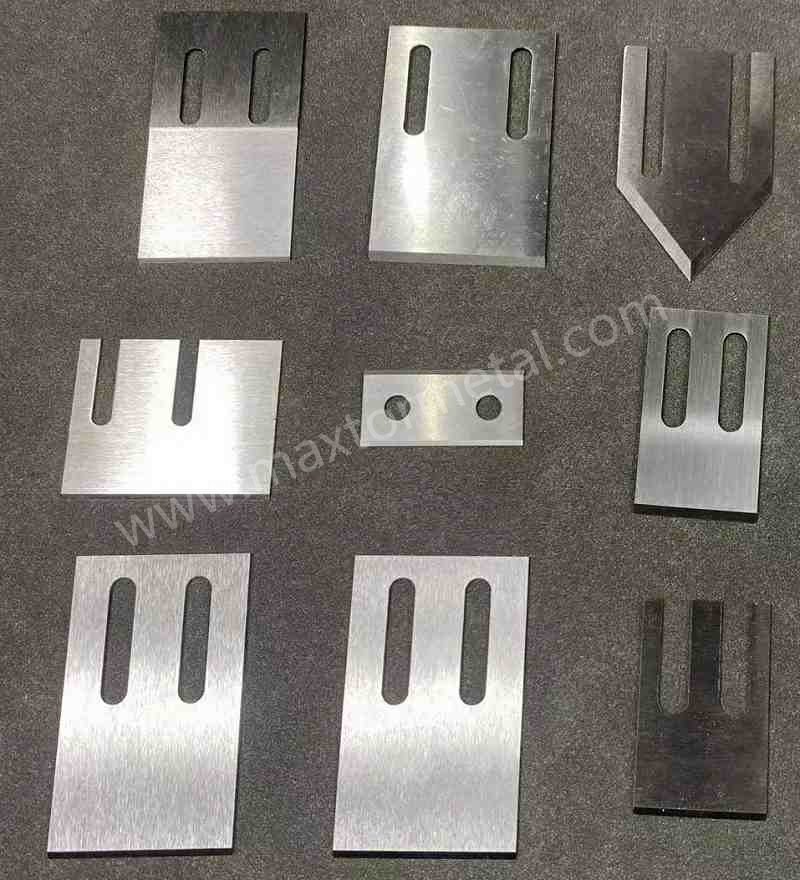
CPM grades are made via powder metallurgy, which produces a fine, uniform dispersion of carbides in a consistent matrix. That uniformity is the foundation of their toughness at a given hardness and the reason CPM pelletizer blades often resist edge chipping better than ingot steels with coarse carbides. In CPM 10V (AISI A11), high vanadium content forms hard VC carbides that deliver exceptional abrasive wear while maintaining better toughness than conventional D2. Crucible’s datasheet (via LookPolymers, 2024‑04‑17) highlights CPM 10V’s high wear resistance and typical working hardness up to around HRC 62–64 depending on heat treat; it also notes improved grindability and dimensional stability compared to conventional tool steels. See the Crucible overview in the CPM 10V datasheet mirror (2024).
By contrast, D2/SKD11’s chromium carbides (M7C3) tend to be larger and less uniformly distributed in conventional ingot‑cast products. Those coarse carbides act as stress raisers at the edge, increasing microcrack initiation and chipping risk under high load or misalignment. Uddeholm’s technical literature rates D2 lower in edge chipping resistance relative to tougher PM grades; start with their concise AISI D2 product page (2024).
CPM 10V vs. D2 Granuliermesser — Abwägung zwischen Ausbrüchen an der Schneidkante und Verschleiß
Here’s the deal: if your dominant failure is edge chipping from intermittent impacts, CPM’s finer carbides help the edge survive longer. CPM 9V generally trades a bit of wear for higher toughness versus CPM 10V, making it a strong pick where impact is real. CPM 10V, with its higher VC fraction, pushes abrasive wear resistance further and can be run at higher working hardness — often cited up to the low‑mid 60s HRC — for glass/mineral‑filled polymers.
D2 brings respectable wear at similar hardness, but those coarse M7C3 carbides make chipping more likely when contact is imperfect or loads spike. In steady contact with lower impact, coated D2 (e.g., TiCN for abrasives) can be cost‑effective, but watch for edge microcracking after regrinds.
Anonymized field case (example): In a three‑month, continuous strand trial on 30% glass‑filled PP (≈500 kg/h throughput), an anonymized compounder ran CPM 10V blanks hardened to ~62 HRC against conventional D2 at ~60 HRC. CPM blades reached first regrind at ~420 operating hours (three regrinds during the trial) with a reported scrap rate of ~0.4%; D2 reached first regrind at ~160 hours (two regrinds) with ~2.3% scrap from edge chipping. Trial conditions: steady abrasive load with occasional misfeeds.
For a practical overview of pelletizer knife selection, see this pelletizer blades guide.
Wann Hartmetall Stahl übertrifft (WC–Co) — konstante Belastungen und viele Nachschliffe
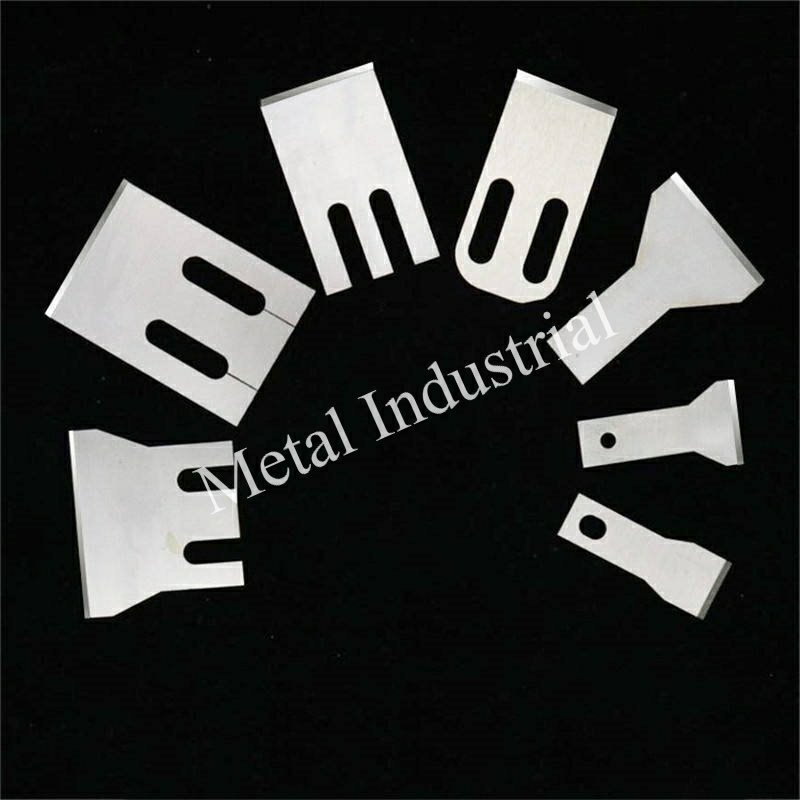
Cemented carbide (WC–Co, K10–K20) offers the highest abrasive wear resistance and holds dimensions through multiple regrinds. If your line runs steady contact on very abrasive, glass‑filled feedstocks with minimal impact, carbide typically lowers total cost over time despite higher upfront price. The catch: edge chipping risk rises as binder content drops and grains get finer. That’s why K20‑ish, higher‑Co grades are often chosen when some impact is unavoidable.
Vendor datasheets quantify hardness (HRA) and transverse rupture strength (TRS) across grades; select by abrasiveness, impact level, and regrind plan.
Wärmebehandlungs- und Beschichtungsfenster — Schneidkantenstabilität bei hohen Temperaturen
Heat matters. CPM M4 (a high‑speed steel) maintains strength at elevated temperatures better than cold‑work grades, making it valuable when thermal softening contributes to dulling. Hot‑work H13/SKD61 is engineered for temper resistance and hot toughness, though it won’t match CPM 10V’s room‑temperature abrasive wear. For H13 behavior and hot hardness context, Böhler’s W302 ISOBLOC page (2024) provides useful notes.
Pair substrates with coatings based on the failure mode:
- TiCN (often via CVD stacks) for abrasive, filled polymers; Ionbond reports microhardness around HV ~2800 and friction vs steel ~0.3 for its TiN‑TiCN‑TiN stack, as noted on Ionbond CVD 10 (2024).
- TiAlN for heat; aluminum‑rich nitride coatings form protective Al2O3‑like layers that help at higher temperatures.
- Chromium plating and nitriding can add corrosion and fatigue resistance for underwater or acidic environments; match process limits to your substrate and geometry.
Example heat‑treat windows (shop trial guidance):
- CPM 10V (A11): austenitize ≈2050°F (1120°C), hold 30–45 min; triple temper ≈1025°F (550°C) ×2h each; target HRC ~60–62. See Crucible CPM 10V datasheet (2024).
- CPM 9V: use similar austenitize range but temper slightly higher to favor toughness (aim mid‑50s HRC).
- CPM M4: follow HSS schedules (higher austenitize, lower multiple tempers) to retain hot hardness (upper‑50s HRC).
These are example windows—adjust per batch, geometry, and trialed cryo steps; verify with supplier datasheets and shop trials.
If you operate underwater pelletizing systems or corrosive die‑face lines, this underwater pelletizer blades guide offers practical context.
Entscheidungsbaum nach Schadensbild
- Edge chipping/microcracks dominate → CPM 9V (or CPM 10V at slightly lower hardness); use tough heat‑treat windows and consider TiCN if abrasives are high.
- Pure abrasive wear under steady contact → WC–Co carbide (K10–K20) tuned for Co%; plan for many regrinds and tight tolerances.
- Thermal softening contributes to dulling → CPM M4 + TiAlN; if very hot cycles, consider H13/SKD61 with nitriding.
- Corrosion pitting precedes chipping (underwater, acidic additives) → CPM or stainless‑lean PM variant with chromium plating; add nitriding for fatigue resistance.
- Budget/availability priority → D2/SKD11 with TiCN or chromium; accept shorter life and monitor chipping.
Lebenszyklus-Wirtschaftlichkeit — Eingabewerte für ein Rechenbeispiel
A simple total‑cost‑of‑ownership model can clarify trade‑offs:
- Blade cost (steel or carbide), expected runtime hours to first regrind, regrind cost, downtime per regrind, and scrap rate from chipping.
- Example: If carbide doubles runtime and supports two extra regrinds vs CPM 10V, but chipping causes a 2% scrap rate on intermittent impact, CPM may win overall despite shorter regrind intervals. Conversely, in steady load with negligible scrap, carbide’s longer life and fewer changeovers lower cost per kilogram.
To plan changeovers and maintenance, see this replacement/maintenance guide.
FAQ
Which blade material is best for glass‑filled pelletizing?
If contact is steady and impact is minimal, WC–Co carbide typically delivers the longest life and most regrinds. If intermittent impact or misalignment occurs, CPM 9V or CPM 10V at appropriate hardness provides better edge chipping resistance.
CPM 10V vs D2: which resists edge chipping better for pelletizer blades?
CPM 10V (AISI A11) benefits from a PM microstructure with fine VC carbides, improving toughness at a given hardness compared with conventional D2’s coarse M7C3 carbides. As a result, CPM grades typically resist chipping better in high‑load, abrasive duty. See Crucible’s CPM 10V datasheet mirror (2024).
When should I use cemented carbide instead of CPM for pelletizer knives?
Choose carbide when abrasive wear is the primary limiter and impact is low. Carbide’s hardness and dimensional stability support more regrinds and longer intervals. Increase Co% if slight impact is expected to reduce chipping risk.
How many regrinds can I expect from CPM vs WC–Co?
It’s application‑dependent. Carbide often supports more regrinds with tight tolerances in steady‑load duty. CPM steels grind well and hold geometry, but the exact count depends on blade geometry, process stability, and regrind practice.
Does TiCN coating extend pelletizer blade life for abrasive, filled polymers?
Yes, TiCN stacks are engineered for abrasive cutting and forming; vendors cite high microhardness and low friction that reduce wear. Actual life extension varies by substrate, coating process, and application; consult your coating supplier and run trials.
Ressourcen und Datenblätter
- CPM 10V (AISI A11) overview and heat‑treat notes: Crucible CPM 10V datasheet mirror (2024)
- Extended reading: Comprehensive pelletizer blades guide; Underwater pelletizer blades guide; Carbiding & coatings explainer
More OEM and standards references (updated 2026‑01)
- Crucible Industries: CPM 9V datasheet — heat‑treat ranges, hardness/toughness notes, and vanadium carbide content (datasheet PDF).
- Crucible Industries: CPM M4 datasheet — hot‑hardness behavior and temper resistance guidance for elevated‑temperature duty (datasheet PDF).
- ASTM International: ASTM G65‑16(2021) dry sand/rubber wheel abrasion test — widely cited comparative wear method for steels and WC–Co (designation and scope page).
- Oerlikon Balzers: BALINIT TiAlN coating overview — high‑temperature Al‑rich nitride coating family commonly applied to cutting/forming tools.
- Sandvik Coromant: ISO K10–K20 carbide application guidance — cemented carbide fundamentals and ISO K family usage context for grade selection.
Berücksichtigen Sie auch die Implementierung (neutral)
Offenlegung: Nanjing METAL ist unser Produkt.
For teams ready to trial CPM pelletizer blades against D2 or to evaluate carbide in steady‑load abrasive duty, working with a supplier that can match heat‑treat windows, verify hardness/tempering, and coordinate coatings will speed up results. Nanjing METAL manufactures custom CPM 10V/9V/M4, D2/H13, and carbide blades and can support ODM/OEM drawings, heat‑treat specs, and one‑stop import. The company’s role here is practical: aligning material choice, heat treatment, and coating with your dominant failure mode and regrind plan. See this overview of pelletizer blades for context.

 English
 Spanish
 Italian
 French
 Portuguese
 Russian
 German
 Arabic
 Hindi
 Vietnamese
 Indonesian
 Japanese
 Korean