
正確にフィットする**交換用熱切断刃(サー모カッター刃)**の選び方
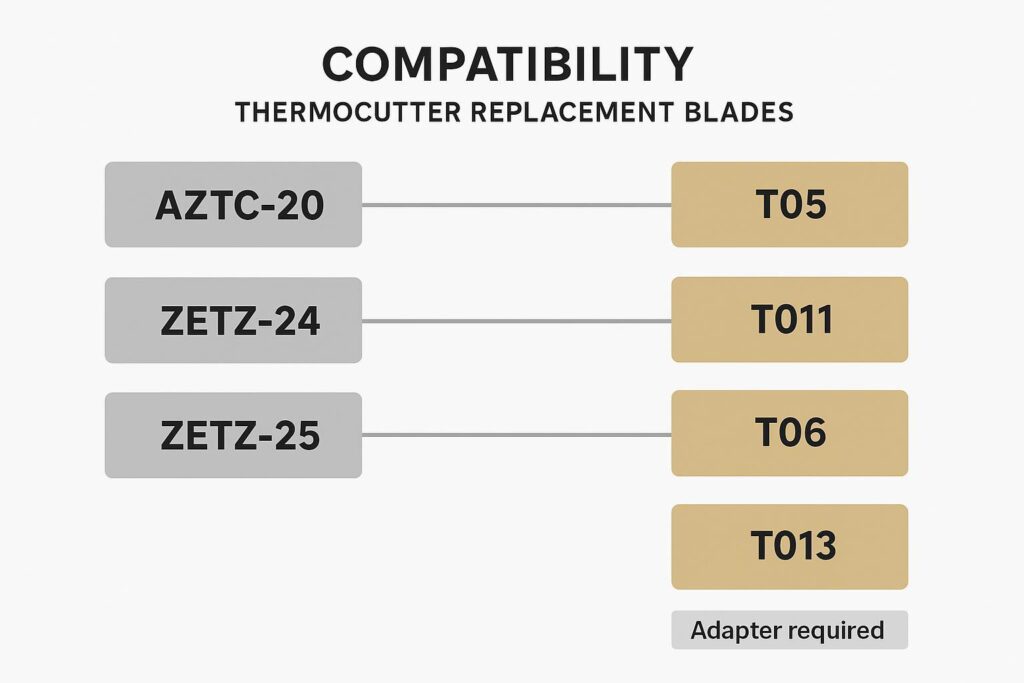
Replacement thermocutter blades look like simple consumables, but they’re often the difference between a clean, repeatable cut and a line that bleeds time in micro-stops, scrap, and rework. When the blade doesn’t fit correctly—or fits but doesn’t match your material and power profile—you’ll see it fast: blackened edges, uneven seals, dragging on multilayer stacks, and more frequent changeovers. In this guide, “compatibility” means the blade mounts correctly and heats as intended on your specific tool. “Cut quality” means the edge you ship: sealed where it should be, not over-melted, dimensionally stable, and consistent from the first cut to the last. “TCO” (total cost of ownership) means the full cost of […]
フォームカッターブレード(発泡スチロール用):EPS/XPS のクリーンな切断と低発煙
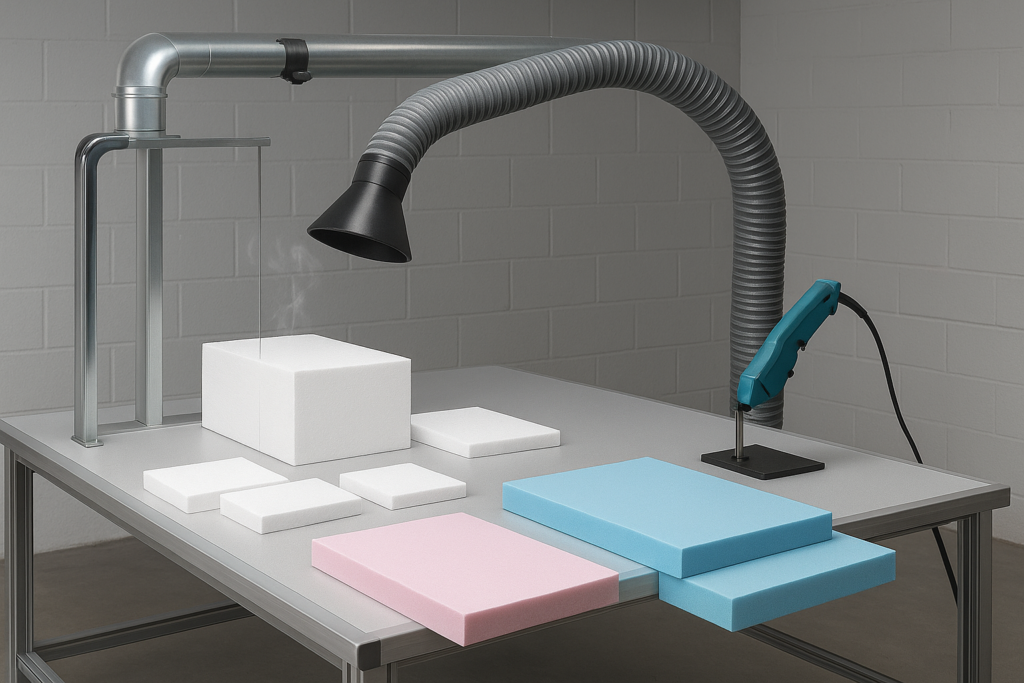
Scope & safety note: This guide focuses on handheld hot knives/thermocutter blades used on EPS and XPS. Treat it as practical process guidance—not a substitute for your facility’s EHS program. Always follow your material SDS, local regulations, and equipment manufacturer instructions, and validate ventilation and PPE with your safety team. Clean, low-smoke cutting isn’t just a “nice-to-have” for EPS and XPS. It directly affects yield (less scrap and rework), OEE (fewer stoppages to clean buildup or swap consumables), and compliance risk (fewer nuisance odors and visible emissions reaching the shop). Thermocutter blades (hot knives) and hot wires solve a different problem than cold cutting. Instead of tearing cells or throwing dust, they melt through the […]
合成繊維用ホットナイフがいかに歩留まりと OEE(設備総合効率)を向上させるか
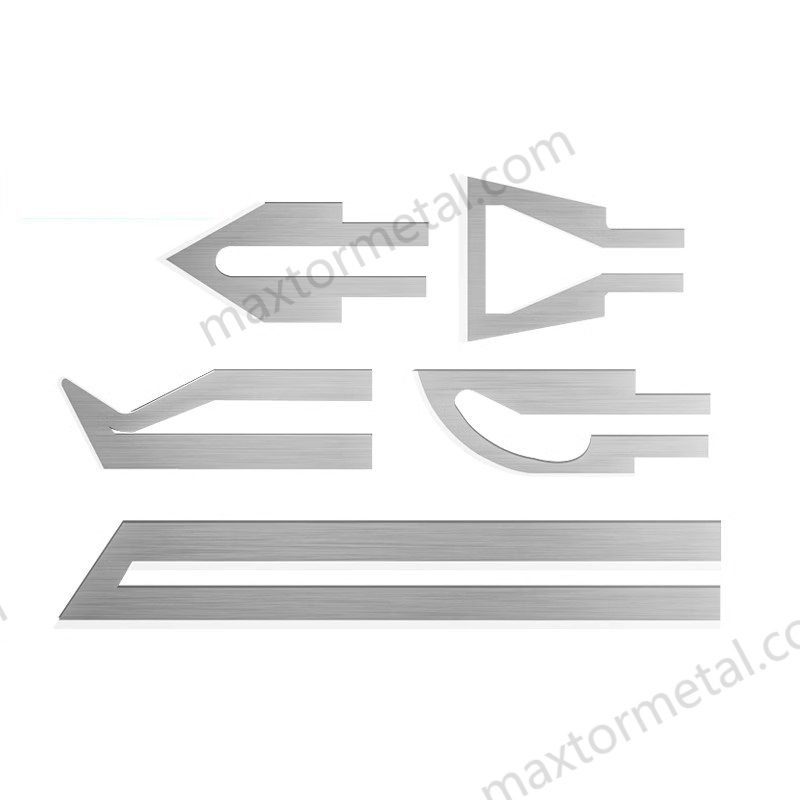
When you’re cutting nylon webbing, synthetic rope, or strap material at volume, “a little fray” isn’t cosmetic—it’s a process defect. Frayed ends trigger rework, slow assembly, and create inconsistent downstream quality checks. That adds up fast in yield loss and in OEE. A synthetic fabric hot knife (often called a thermocutter) solves the root issue by cutting and sealing in one pass—in other words, it can cut and seal synthetic webbing in a single controlled operation. Done right, it turns an edge that would unravel into a fused end that’s stable through handling, sewing, and packaging. This article explains: Stop Fraying, Boost OEE Fraying’s hidden losses Fraying is rarely “just fraying.” On a […]
固定刃およびスクエアカッター用プラスチックリサイクル刃の幾何形状
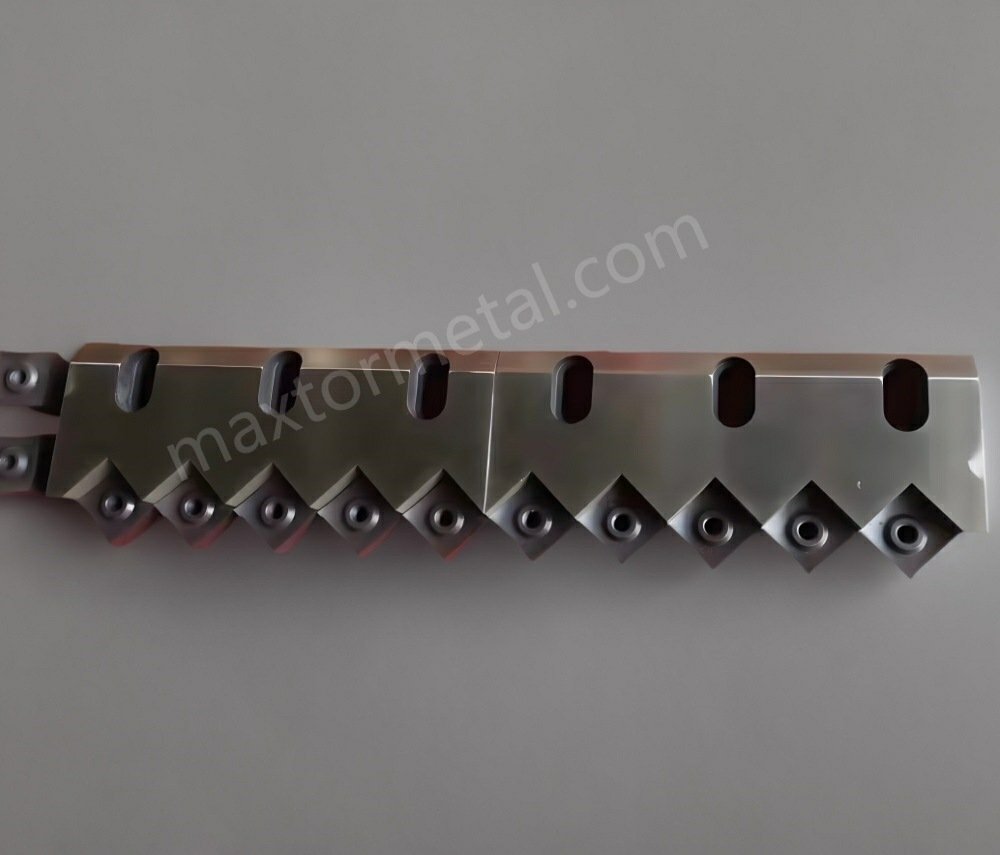
Blade geometry is one of the few levers you can pull on a single-shaft shredder that changes throughput, particle size consistency, energy per ton, wear life, and total cost of ownership (TCO)—without buying a new machine. But it only works if you treat geometry as a system: square cutters + fixed counter-knife + screen + cutting gap + feed behavior. Change one item blindly and you usually pay for it in amps, heat, noise, and chipping. Geometry determines whether the material gets a clean shear (efficient), a smear/tear (hot and power-hungry), or a jam-and-reverse cycle (throughput killer). It also determines where wear concentrates: on the cutting edge, the seating faces, or the […]
極度の摩耗に対応する破砕機刃のハードフェイシング(肉盛溶接)
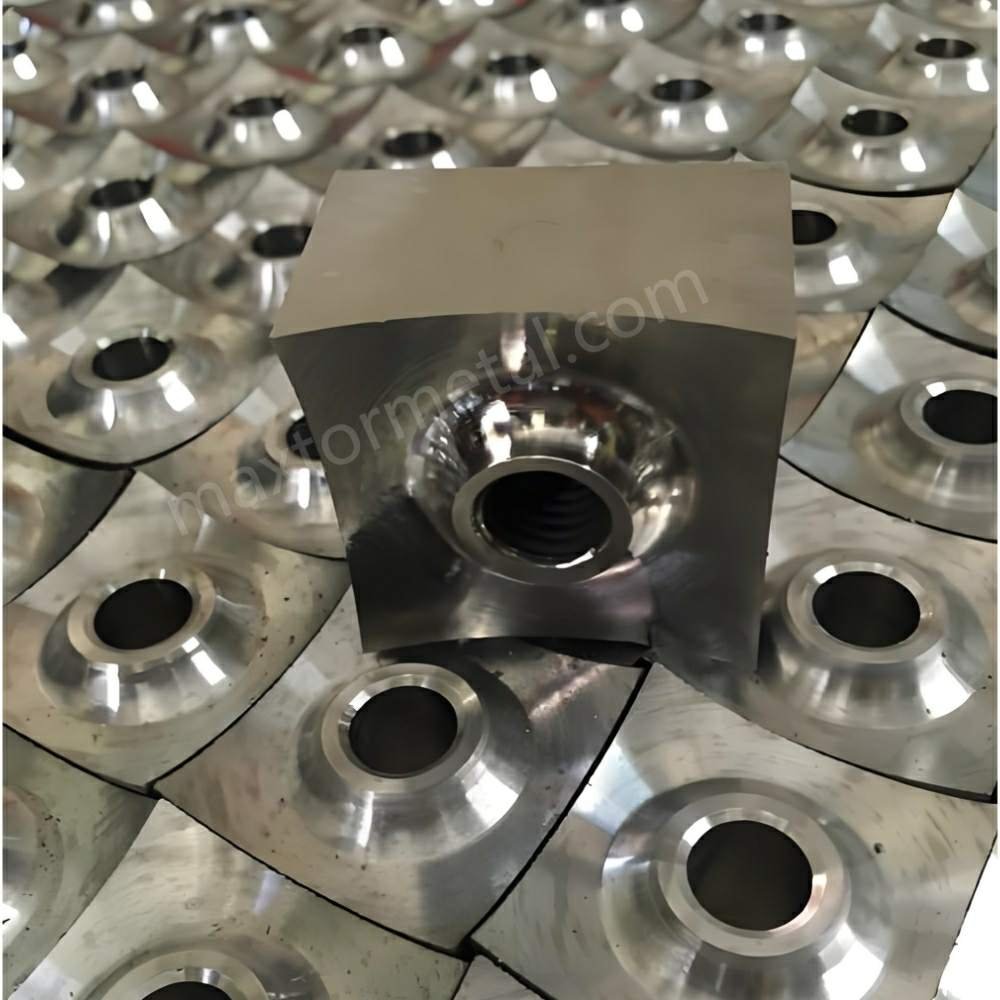
Mineral grit doesn’t “wear a knife” the way clean plastic does. It turns your cutting zone into a grinding zone: more sliding contact, more heat, and faster edge rounding. Once the edge rounds, you typically see the same cascade: higher torque variation, more vibration, wider particle-size scatter, and more stoppages. This is why abrasive duty often punishes good base steel selection unless you also protect the working surfaces. If you’re running a single-shaft shredder, the outcome is rarely “the blade lasts longer” in isolation. You’re chasing system-level stability: How to think about cost per metric ton In abrasive-duty shredding, blade wear hurts you twice: you buy knives more often, and […]
シングルシャフトシュレッダーの刃のメンテナンス:研磨か交換か

Single-shaft shredders don’t “slow down” randomly. Key Takeaway: If your team is stuck on the single-shaft shredder blades sharpen vs replace decision, don’t guess—measure clearance, verify torque, and trend amps/ton and PSD first. Most of the time, it’s the cutting system losing its geometry: rotor cutter blocks/tips and bed knives (stator) stop shearing cleanly, clearances drift, or fasteners stop holding. The result is predictable—higher amps, more heat, unstable particle size, and surprise downtime. This guide focuses on the parts you can actually control during maintenance: What you’ll use (and why these tools matter): feeler gauges (gap), torque wrench (clamp load), straightedge (flat/straight seating), bluing/marking compound (contact checks), and log sheets (trend control). […]
摩耗性の高いプラスチック用破砕機における**リサイクル刃(回収刃)**を保護するセットアップ
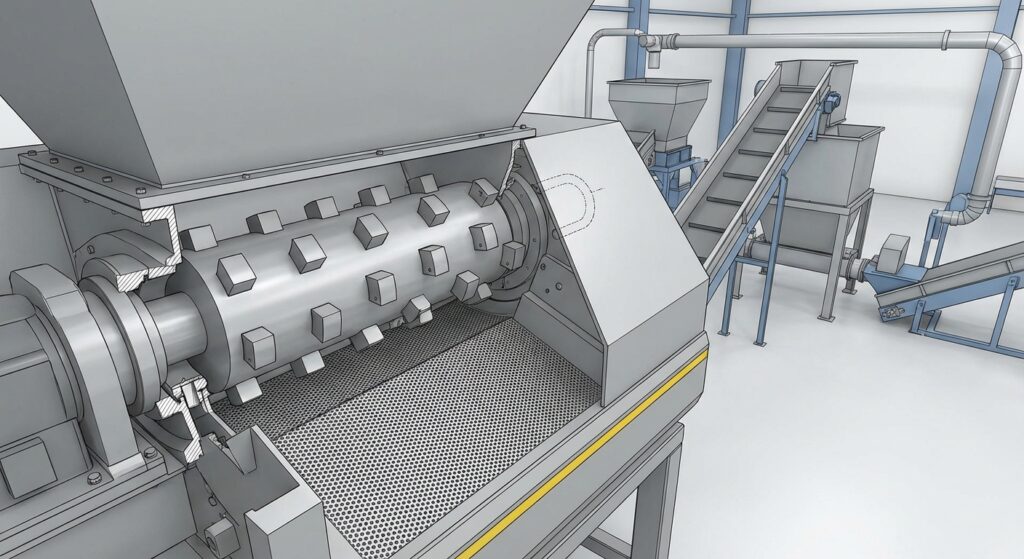
In abrasive plastic streams—glass-filled regrind, mineral-filled compounds, or bales that carry sand and grit—blade wear is rarely “just a materials problem.” In a single-shaft shredder, setup choices decide whether knives stay in steady cutting or spend their life heating, rubbing, and reverse-cycling. You control more levers than most plants document: feed rate uniformity, the speed/torque regime, and how the screen and cutting gap force material to re-circulate in the cutting chamber. Knife engineering still matters—steel choice, heat treatment quality, coatings, and edge geometry are the last line of defense for abrasive plastic recycling blades—but it works best when the process isn’t fighting the knives. Finally, the most reliable maintenance trigger […]
**凹面シュレッダーナイフ(破砕機刃)**によるスループット向上と消費電力(kWh/t)の低減
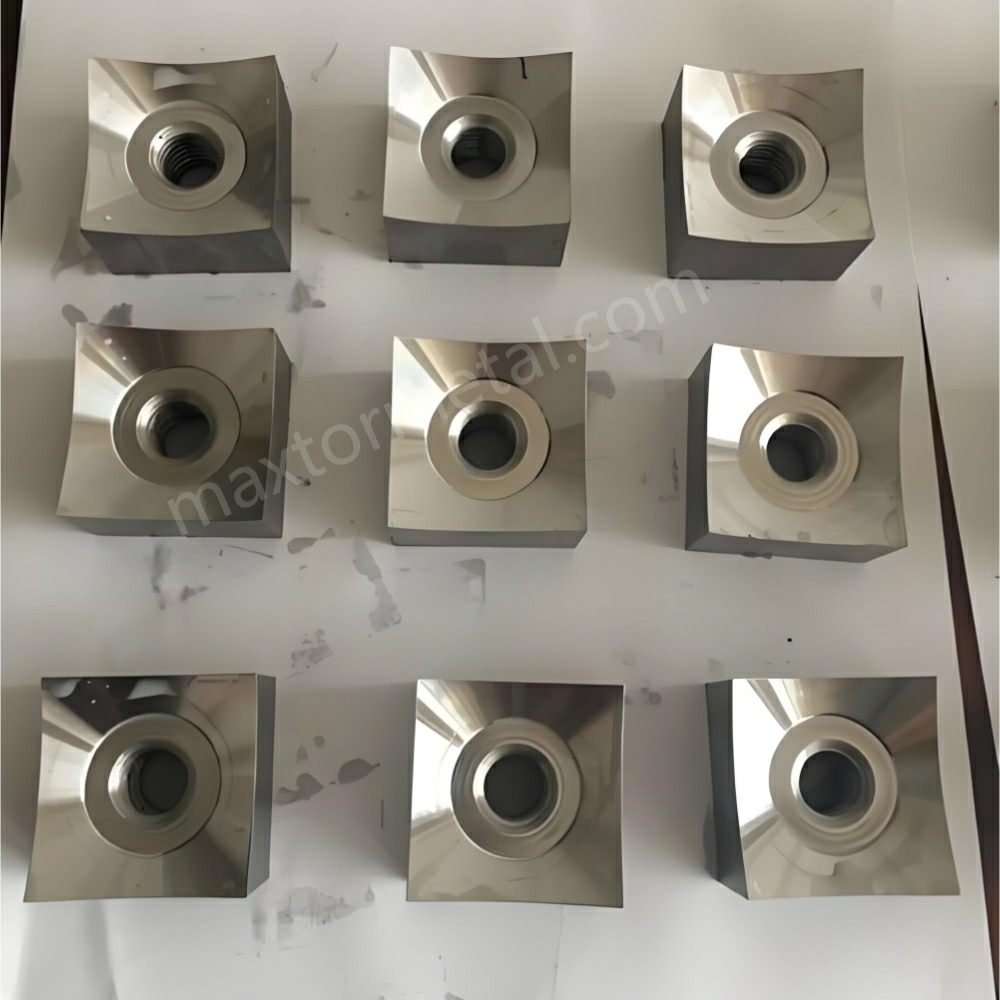
Concave shredder blades change the first contact between material and rotor in a single-shaft shredder. Instead of presenting a mostly flat edge that relies heavily on pusher force and friction to initiate a cut, a concave edge tends to create a more “hooking” engagement that encourages bite and controlled self-feeding. In the field, energy-per-ton and throughput gains are realistic when the shredder is already mechanically healthy and the process is limited by cutting efficiency rather than downstream conveying or screen plugging. Under those conditions, a measured improvement on the order of ~5–15% is often achievable—but it’s not automatic, and it’s not just about knife geometry. This guide breaks down the mechanisms (why […]
ローターとステーターのシュレッダー刃(破砕機刃)クリアランス調整ステップガイド
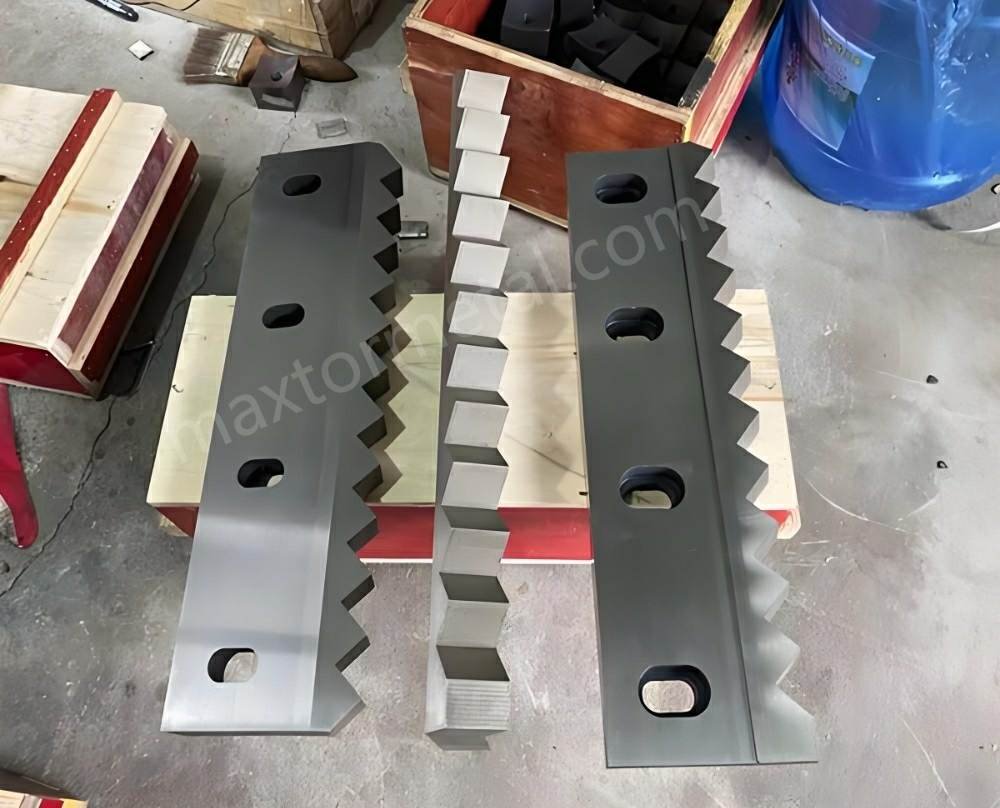
シュレッダーのブレードクリアランス(ローターナイフと固定ベッド/ステーターナイフの間の隙間)は、シングルシャフトシュレッダーで重要な要素、つまり切断品質と出力サイズ、処理量、消費電力、そしてナイフが欠けたり、転がったり、切断ではなく「研磨」し始めるまでの寿命など、あらゆる面を静かに左右する設定の一つです。隙間を広く設定しすぎると、材料が切断ゾーンで曲がったり、折り畳まれたり、擦り切れたりする傾向があります。これは多くの場合、発熱量の増加、電流値の増加、粒子サイズの不均一性、および再循環時間の増加として現れます。隙間を狭く設定しすぎると、金属同士の接触、突然の刃先の損傷、振動、そして計画していた停止が[…]
排出サイズの安定化を実現する交換用シュレッダーナイフ(破砕機刃)
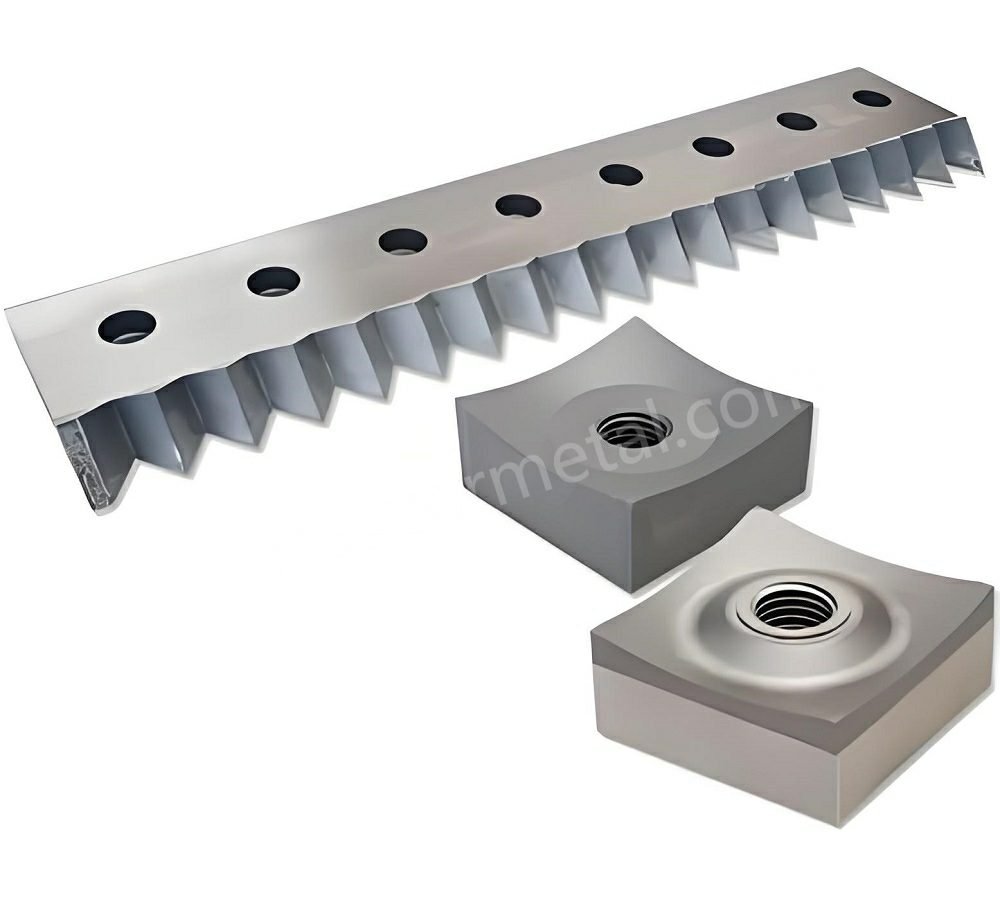
安定した出力サイズは「あれば良い」ものではありません。それは、シフトごとに実感する3つの要素、すなわち処理量、エネルギー効率、そして下流工程の品質を守るものです。粒子サイズが変動すると、スクリーンの負荷が不均一になり、電流が上昇し、次の工程(洗浄ライン、空気分級、造粒、ペレット化、または選別)は安定した運転ではなく、変動と戦うことになります。シュレッダーブレードの交換は、「機械の切れ味」だけでなく、実際に使用する切断形状、つまり切断円、シートスタックアップ、ナイフの厚さ、そしてカウンターナイフギャップに影響を与えます。これらの要素によって、きれいに切断できるか、それとも引き裂き、擦り切れ、微粉が発生するかが決まります。このガイドは、一般的なシングルシャフトシュレッダーで出力を安定させる交換用ナイフとカウンターナイフの選択を支援するために作成されました。[…]

 English
 Spanish
 Italian
 French
 Portuguese
 Russian
 German
 Arabic
 Hindi
 Vietnamese
 Indonesian
 Japanese
 Korean