요약: 단순 HRC 경도를 극대화하는 대신 내마모성(경도)과 샬피 충격 인성(Charpy impact toughness)의 최적 밸런스를 확보해야 합니다. 58–60 HRC 경도의 DC53강은 이물질이 혼입된 폐타이어 및 ELV 파쇄 공정에서 D2(SKD11) 대비 약 2배의 충격 인성을 제공합니다. 아울러 실증 사례 분석 결과, 나이프 파손의 실제 원인은 소재의 경도 부족이 아닌 볼트 체결공(Mounting-hole geometry) 부위의 응력 집중인 경우가 많습니다.
범위: 본 가이드는 폐타이어 원형 및 폐차(ELV) 혼합 원료의 1차 파쇄 및 전처리 파쇄(Pre-shredding) 공정에 중점을 두고 있습니다. 이러한 공정에서는 스틸 보강재, 이물질 금속(Tramp metal), 충격 하중 및 마모성 오염 물질이 핵심 고려 사항입니다. 2차 고무 분쇄 및 와이어가 제거된 고무 분말(Crumb) 가공에는 마모 저항성과 인성(Toughness) 간의 다른 균형이 요구됩니다。
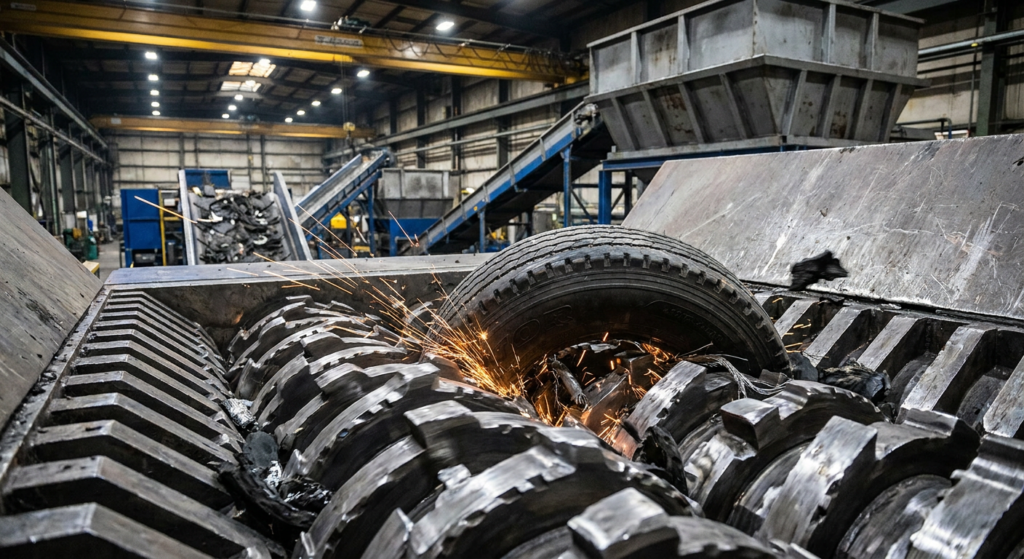
폐타이어 재활용 및 폐차(ELV) 감량화 작업은 산업 폐기물 처리 분야에서 기계적 부하가 가장 심한 공정 중 하나입니다. 균일한 플라스틱 분쇄나 깨끗한 박판 절단과 달리, 라디알 타이어 전체와 자동차 스크랩을 처리할 때 파쇄기 날(Shredder Knives)은 단일 연속 공정 내에서 강력한 기계적 충격, 높은 마찰열, 그리고 지속적인 마모의 가혹한 결합에 직면하게 됩니다. 승용차 및 상용 트럭용 스틸벨트 타이어는 탄성 가황 고무 내부에 고장력 스프링 강철 레이어와 두꺼운 비드 와이어 번들이 직접 매립되어 있습니다.
작업자가 1차 이축 또는 단축 파쇄기용 칼날을 선택할 때, 마모 수명을 극대화하기 위해 가장 경도가 높은 공구강을 선택하는 경우가 많습니다. 그러나 대용량 재활용 공장에서의 현장 경험에 따르면 경도만 극대화할 경우 조기 칼날 이빠짐(chipping), 치명적인 바디 파손, 그리고 막대한 비용을 초래하는 예기치 않은 설비 가동 중단이 발생합니다. 성공적인 가동을 위해서는 내마모성 경도와 내충격성 파괴 인성 사이의 정밀한 균형이 필수적입니다. 기성 칼날 구매 방식에서 금속학적 재료 선택 방식으로 전환한 엔지니어링 팀은 초기 로크웰 경도 수치 대신 처리 톤당 총 비용을 기준으로 성능을 평가합니다. Maxtor Metal와 같은 맞춤형 칼날 제조업체는 정밀 연마된 파쇄기 칼날 및 파쇄용 나이프 가 이러한 다축 충격 하중 하에서도 구조적 무결성을 유지하도록 설계합니다.
다음의 엔지니어링 가이드는 Maxtor Metal의 내부 금속 및 재료 기술팀의 전문 지식을 바탕으로 합니다. 당사는 ISO 9001 인증 품질 관리 시스템 하에서 철스크랩 재활용, 폐기물 처리 및 감용 파쇄기용 열처리 산업용 나이프의 정밀 연삭 분야에서 15년 이상의 경력을 보유하고 있습니다. 아래의 소재 선정 및 파손 원인 분석(Failure analysis) 권장 사항은 단순 제조업체 데이터시트의 이론에 그치지 않고, 공구강(Tool steel) 재가공 현장에서 축적된 실전 노하우를 반영합니다.
폐타이어 및 ELV 투입재가 파쇄기 나이프를 손상시키는 이유
폐타이어 완제품 및 ELV(폐차) 스크랩 파쇄 작업은 일반적인 고형 폐기물이나 플라스틱 재활용 시 발생하는 응력을 훨씬 초과하는 심각한 충격 및 마모 동역학에 절삭날을 노출시킵니다.
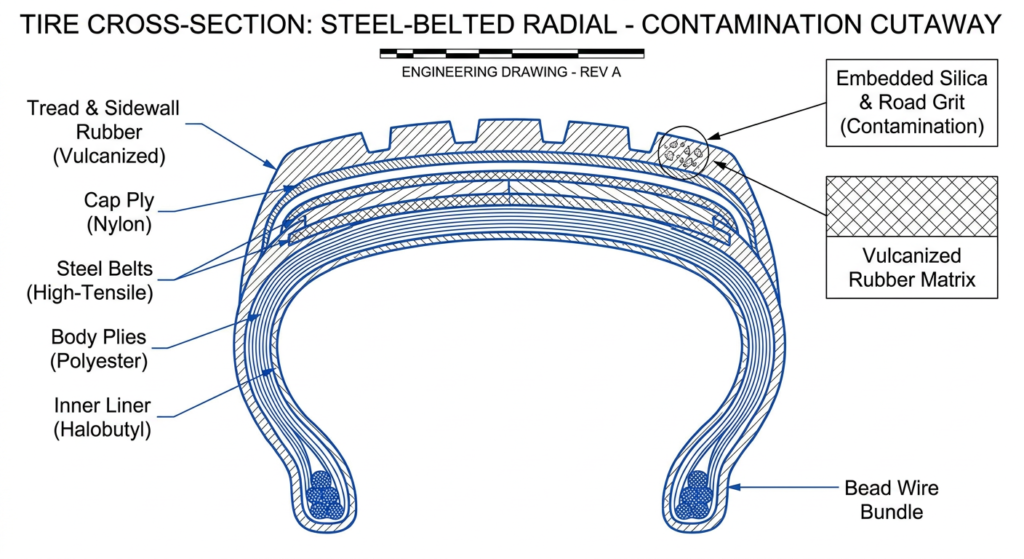
- 극심한 충격 쇼크: 고장력 강철 비드 와이어 번들(1,500 MPa에서 2,100 MPa 사이의 인장 강도) 및 중량 자동차 구조 프레임은 기존 냉간 공구강의 항복 강도를 초과하는 갑작스러운 피크 충격 하중을 유발합니다.
- 탄성 에너지 손실: 두꺼운 가황 고무의 탄성은 전단이 일어나기 전에 기계적 에너지를 흡수합니다. 이로 인해 파쇄기 칼날은 상대 칼날(counter-knife)에 원료를 밀착시키면서 극도로 강력한 물림을 유지해야 하므로 강한 마찰이 발생합니다.
- 복합 연마 마모 열화: 박혀 있는 도로 모래, 석영 실리카, 브레이크 분진 및 분리되지 않은 트램프 아이언(이물질 철분)은 칼날 측면에 연마재 역할을 하여 마모성 라운딩을 가속화하는 동시에, 충격 하중으로 인해 절삭날을 따라 미세 치핑(micro-chipping)이 발생하기 쉬운 환경을 만듭니다.
핵심 요점: 타이어 파쇄는 단순한 절단 작업이 아닙니다. 이는 고에너지 충격, 금속 전단 및 심각한 고무 마모가 결합된 격렬한 공정입니다. 오직 내마모성만을 위해 설계된 칼날은 피로 파괴로 인해 빠르게 파손됩니다.
스틸 벨트 고무의 독특한 응력 프로파일
철강 구조는 ELV(폐차) 총 중량의 65%에서 70%를 차지합니다. 폐타이어 완제품이나 차량 어셈블리가 1차 파쇄기에 투입되면, 로터가 회전할 때마다 칼날 훅이 탄성 합성 고무와 고강도 강철 와이어를 동시에 전단해야 합니다.
고무는 열 절연체 역할을 하기 때문에 전단 사이클 동안 발생하는 마찰열이 빠르게 방출되지 못합니다. 클리어런스(간극)가 악화되거나, 칼날이 무뎌지거나, 연마성 오염 물질이 증가하면 국부적인 마찰 열화가 심각해질 수 있습니다. 실제 칼날 온도는 로터 속도, 칼날 간극, 투입물 구성, 접촉 시간 및 냉각 조건에 크게 좌우되므로, 고정된 200–300°C 값을 보편적인 작동 온도로 간주해서는 안 됩니다.
저온에서 템퍼링된 저급 공구강의 경우, 이러한 작동 열이 원치 않는 2차 템퍼링을 유발하여 국부적인 표면 경도를 낮추고, 압축 잔류 응력을 완화하며, 측면 마모를 가속화합니다.
요약하자면: 타이어 및 ELV 투입물은 고장력 비드 와이어 충격, 단열 마찰열, 연마성 오염을 하나의 연속적인 사이클로 결합하므로, 단일 특성(경도 또는 인성 단독)만으로는 이 세 가지 요소를 모두 견뎌낼 수 없습니다.
경도 대 인성(Toughness)의 상충 관계
공구강 금속학에서 경도와 충격 인성은 저울대의 양끝에 위치합니다. 로크웰 C 스케일(HRC)로 측정되는 경도는 국부적인 소성 변형, 표면 침투 및 연마 마모에 대한 재료의 저항성을 정량화합니다. 샤르피 V-노치 테스트를 통해 줄(J) 또는 제곱센티미터당 줄(J/cm²) 단위로 정량화되는 충격 인성은 고속 충격을 받았을 때 파손 없이 에너지를 흡수하고 소성 변형하는 강재의 능력을 측정합니다.
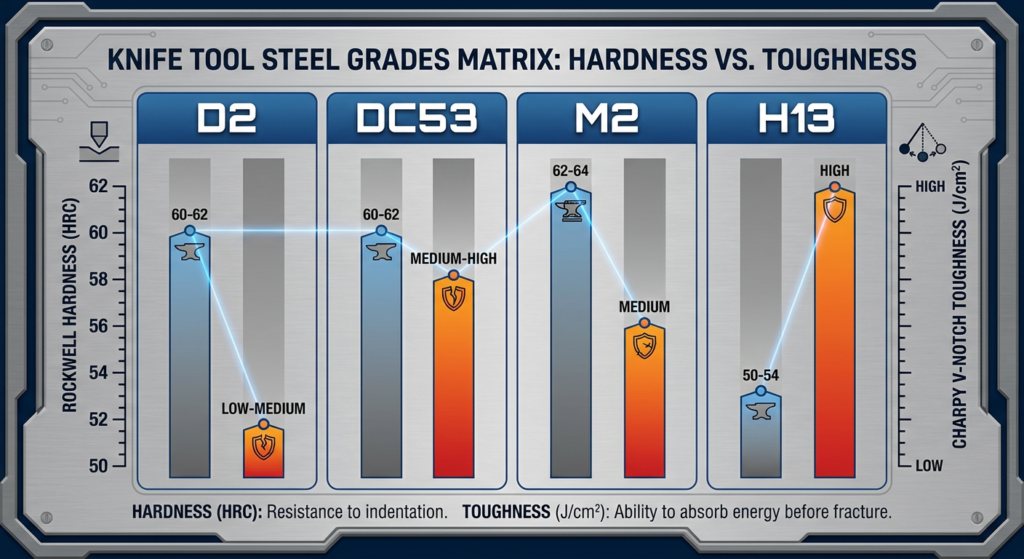
탄소 함량을 높이거나 퀜칭 매개변수를 변경하여 HRC를 높이면 연마 마모 저항성과 칼날 예리함 유지력이 향상됩니다. 그러나 경도가 높아지면 재료의 파괴 인성이 감소하여 트램프 메탈(이물질 금속)과 충돌할 때 절삭 훅이 치명적인 균열에 취약해집니다. 반대로 HRC를 낮추면 충격 흡수력이 향상되고 칼날 파손이 방지되지만, 연마성 실리카와 스틸 벨트의 마찰로 인해 칼날 끝이 조기에 둥글게 마모됩니다.
최적의 합금 선택은 달성 가능한 가장 높은 HRC 등급을 쫓는 것이 아니라, 투입물의 오염 수준과 1차 로터 속도에 전적으로 좌우됩니다.
타이어 및 ELV 작업용 HRC 범위 해석
칼날 금속학을 특정 가공 단계에 맞추기 위해 다음과 같은 엔지니어링 표준이 적용됩니다. ASTM A681 공구강 사양 공구강을 특화된 경도 및 인성 범위로 분류합니다:
| 공구강 등급 | 일반적인 경도 범위 | 무노치 샤르피 충격 에너지 | 주요 파손 저항성 | 권장 가공 애플리케이션 |
|---|---|---|---|---|
| AISI D2 / SKD11 | 약 58–62 HRC | 15–25 J/cm² | 높은 연마 마모 | 깨끗하고 사전 분류된 고무 또는 2차 분쇄(granulating) |
| DC53 (개량형 D2) | 템퍼링 조건에 따라 ~58–60 HRC | 40–60 J/cm² | 균형 잡힌 마모 및 충격 저항 | 1차 타이어 파쇄 및 오염된 ELV 스트림 |
| AISI M2 / SKH51 | 약 62–64 HRC | 10–18 J/cm² | 극도의 내마모성 및 고온 경도 | 트램프 메탈이 없는 깨끗한 고속 전단 |
| AISI H13 / SKD61 | 고부하 작업 환경에서 ~50–54 HRC | 80–120 J/cm² | 높은 충격 및 열충격 저항 | 중량급 1차 폐차(ELV) 스크랩 및 이물질 함량이 높은 피드 |
DC53이 오염된 원료 스트림의 벤치마크인 이유
DC53은 일본 Daido Steel이 표준 AISI D2 (JIS SKD11)의 고인성 대체재로 개발한 업그레이드된 냉간 공구강으로, Daido가 자사의 공식 DC53 냉간 공구강 브로셔에서 명확히 밝히고 있는 포지셔닝입니다., which describes the grade as overcoming SKD11’s shortcomings in hardness and toughness. By contrast, standard D2 steel contains large, coarse primary chromium carbides (M₇C₃) that form network boundaries during solidification. These coarse carbides act as internal stress risers where micro-cracks originate under impact.
DC53 is registered as an 8% chromium, 8Cr-2Mo cold-work grade — a composition ASM International catalogs in its independent DC53 materials digest — and trims carbon to roughly 0.95% while adding molybdenum (~2.0%) and vanadium (~0.35%). When subjected to high-temperature double tempering at 520°C to 530°C, DC53 undergoes secondary precipitation hardening. This process precipitates sub-micron M₂C carbides uniformly throughout a tempered martensitic matrix.
The resulting microstructure delivers a working hardness of 58–60 HRC while yielding a Charpy impact toughness roughly double that of standard D2 steel. This extra toughness allows DC53 shredder knives to withstand direct impacts against high-tensile bead wires and stray bolts without spalling or shattering.
Heat Treatment as the Hidden Lever
A tool steel’s chemical composition represents only half of its final performance potential. Advanced heat treatment procedures serve as the critical lever to unlock maximum fatigue life:
- Vacuum Hardening: Eliminates surface decarburization and scale, ensuring uniform hardness from the knife skin to its inner core.
- Deep Cryogenic Treatment: Subjecting quenched knives to liquid nitrogen temperatures (-196°C) converts residual retained austenite (RA) into hard, stable martensite, preventing dimensional growth and micro-cracking during service.
- Dual-Hardness Profiles: Differential hardness should be treated as an application-specific design option rather than a default heat-treatment route. Where a blade architecture requires a wear-resistant working zone and a tougher structural region, the manufacturer should validate the hardness gradient, transition zone, dimensional stability, and crack resistance on the actual cross-section..
Diagnose the Failure Mode Before Choosing a Grade
DC53 is often described — and sometimes oversold — as a universal upgrade for D2. From a metallurgist’s standpoint, that framing is too simple. A grade is only as good as the failure mode it is asked to defeat. If the dominant problem is pure abrasive edge rounding on a clean, pre-sorted feed, a well-refined D2 at high hardness can remain the more economical choice, because its heavier carbide fraction buys the most wear life for the lowest cost. A move to DC53 only earns its premium when the dominant mode is impact, or a genuine impact-plus-abrasion duty — and even then, removing a stress-concentration point in the blade geometry is frequently just as important as the choice of steel.
That is why Maxtor Metal’s engineers frame shredder procurement as a failure-mode diagnosis first and a D2-versus-DC53 decision second. The matrix below is a practical first screen:
| Observed Field Symptom | Primary Suspect | What to Measure First | Is a D2 → DC53 Swap Justified? |
|---|---|---|---|
| Edge chipping | Toughness shortfall | Fracture microscopy, HRC, edge condition | Usually worth evaluating |
| Large or body fracture | Stress concentration + impact | Crack origin, hole and keyway geometry, dimensions | Not by material alone — redesign first |
| Rapid flank wear | Insufficient wear resistance | Edge radius, wear-depth profile | May help |
| Cracking from the mounting hole | Stress concentration | Hole-edge radius, surface defects, SEM | Redesign geometry first, then grade |
| Normal hardness but early failure | Toughness, microstructure, or design | Metallography + fracture analysis | Hardness alone cannot pass judgment |
| Edge spalling | Impact combined with high hardness | Edge microscopy + HRC | DC53 / tougher grades worth comparing |
| Uniform wear with no fracture | 마모 | Wear profile under steady load | D2 may remain the more economical choice |
The verified D2 blade-base case later in this guide is a textbook illustration of why this sequence matters. There, hardness measured within the expected range and heat treatment was not the root cause; the crack initiated at the mounting-hole stress concentration and propagated rearward. Read through the matrix, no grade swap — D2 to DC53 or otherwise — would have solved that failure on its own, because the geometry, not the steel, was the controlling defect.
요약하자면: diagnose the failure mode first—chipping points toward toughness, flank wear points toward hardness, and fracture from a mounting hole points toward geometry, not steel grade at all.
폐타이어 및 ELV 처리용 나이프 형상(Geometry) 선정
Material properties must work in harmony with mechanical blade design. Even the toughest steel grade will fail if structural stress points are built into the knife geometry.
Aggressive Hook Angle → Higher Rubber Bite → Greater Edge Stress
Generous Fillet Radii → Smooth Stress Flow → Eliminates Corner Cracks
Broad Cross-Section → High Flexural Rigidity → Prevents Blade Deflection
- Hook Profile Optimization: Extremely steep, sharp hook angles maximize bite on slippery elastic tires, but thin knife tips suffer extreme bending stresses when shearing steel bead wire. Truncating hook tips slightly increases structural support behind the cutting edge without sacrificing throughput.
- Section Thickness and Stiffness: Primary tire shredders apply tens of thousands of Newton-meters of torque. Knives must feature sufficient cross-sectional thickness to prevent lateral deflection, which alters blade-to-counter-knife clearances and causes binding.
- Stress Concentration Management: Internal keyways, bore corners, and mounting bolt holes are classic failure sites. Machining generous fillet radii (minimum 3–5 mm) at all internal corners redistributes internal tensile stresses, preventing fatigue cracks from propagating through the blade body.
요약하자면: hook angle, fillet radius, and section thickness determine whether a tough steel grade actually gets to use that toughness—geometry and material selection have to be solved together.
실제 경제성: 초기 경도보다 톤당 처리 비용(Cost Per Ton)이 우선합니다
In industrial recycling management, purchasing decisions driven solely by the initial price tag of replacement knives often result in higher overall operating expenses.
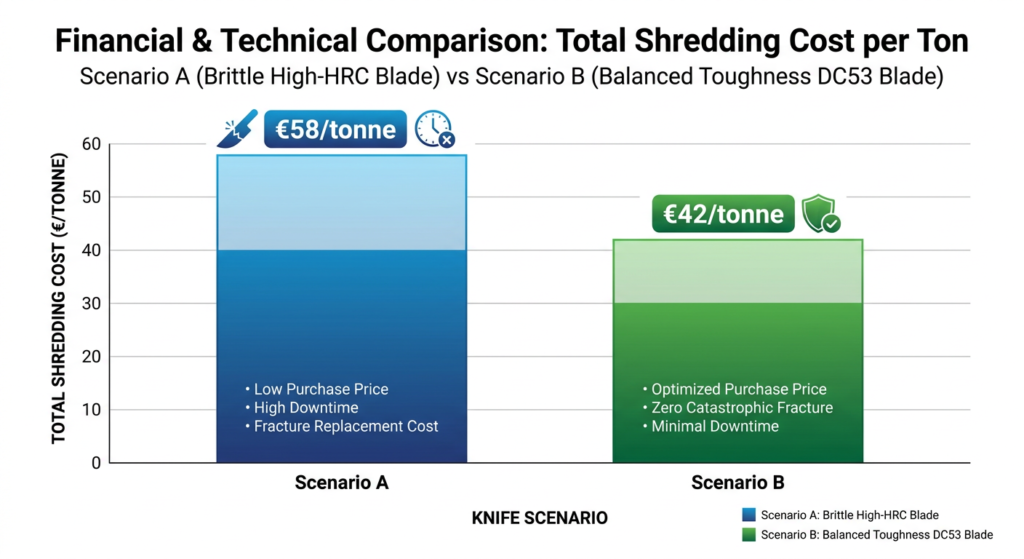
When a brittle, low-cost blade shatters after 300 operating hours, the true expense includes not just the purchase price of a replacement knife set, but also four to eight hours of unscheduled plant downtime, crane rental, maintenance labor, and lost production capacity. Primary tire shredding operational costs typically range between €40 and €60 per tonne. In high-capacity processing plants, unexpected downtime directly erodes profitability.
프로 팁: Well-engineered shredder knives crafted from balanced DC53 or refined D2 steel routinely operate for 10,000 to 15,000 tonnes of whole tire processing before requiring edge resharpening or hard-facing maintenance.
Building a Cost-Per-Ton Comparison Model
To calculate true tooling economics, maintenance directors utilize a Total Cost of Ownership (TCO) formula:
Cost Per Ton = Knife Set Cost + Installation Labor + Downtime Lost Revenue + Resharpening Costs/Total Processed Tonnage Over Blade Lifetime
The scenarios below are illustrative TCO calculations built around typical published cost ranges, not a specific customer’s invoiced figures—use them as a modeling template with your own site’s downtime and labor rates.
Scenario A: High-HRC Low-Toughness Blade (Standard D2 at 61 HRC)
- Initial Knife Set Cost: €12,000
- Lifespan Before Failure: 350 Hours (1,750 Tonnes) due to catastrophic edge spalling from tramp metal.
- Downtime & Replacement Labor: €9,500 (2 unscheduled shutdowns).
- Total Operational Cost: €21,500 / 1,750 Tonnes = €12.28 per tonne in knife overhead.
Scenario B: Balanced Toughness Blade (DC53 at 59 HRC)
- Initial Knife Set Cost: €15,500
- Lifespan Before Maintenance: 2,200 Hours (11,000 Tonnes) with uniform flank wear and zero cracking.
- Scheduled Maintenance Labor: €3,000 (1 planned overhaul).
- Total Operational Cost: €18,500 / 11,000 Tonnes = €1.68 per tonne in knife overhead.
Failure Mode Diagnosis: Reading the Knife
Inspecting worn shredder blades provides direct diagnostic feedback regarding rotor alignment and metallurgical fit:
- Uniform Abrasive Flank Rounding: Indicates that the blade material possesses adequate toughness, but wear resistance can be improved by stepping up HRC slightly or selecting a grade with higher vanadium content (such as M2 or DC53).
- Chipping, Spalling, or Corner Cracking: Signals that the blade is excessively brittle for the feedstock contamination level. The operator should immediately reduce HRC or transition to a tougher steel grade like DC53 or H13.
- Galling and Thermal Cracking: Indicates severe friction buildup caused by improper knife clearance, dull edges, or inadequate high-temperature tempering resistance.
For failures that don’t fit a clean wear-vs-chipping pattern — or when you need lab-confirmed root cause rather than a field read — see our guide on 치명적인 블레이드 파손: 야금학적 근본 원인 및 예방 for the fractography sequence (macro mapping → SEM/EDS → metallography → XRD) that separates heat-treatment, material, and overload causes.
요약하자면: a cheaper, harder blade that fractures early can cost 7x more per tonne than a tougher blade with a higher sticker price, once downtime and unscheduled labor are counted.
실증 현장 사례: 사용 3개월 만에 발생한 D2 나이프 베이스 균열

To ground the hardness-versus-toughness discussion in real field evidence rather than only in brand experience, we reference an independently published failure-analysis case study in the peer-reviewed journal Engineering Failure Analysis. The study documents a steel blade-base cutting tool used on a two-rotor, low-speed shear machine pre-shredding end-of-life passenger and truck tires that contain steel-belt reinforcement.
The component was manufactured from AISI D2 tool steel, and the failure was a complete fracture, not a worn edge: it cracked through approximately three months into service, despite a predicted working life of roughly one year. Because this study is publicly indexed and independently verifiable, operators and engineers can use it as a neutral reference point when assessing their own knife metallurgy.
Evidence classification: Independent published failure-analysis case; not a Maxtor Metal customer case.
| Verified Case Data | 값 |
|---|---|
| 재료 | AISI D2 tool steel |
| 적용 분야 | End-of-life tire (ELT) pre-shredding |
| Machine principle | Two-rotor, low-speed shear between counter-rotating rotors |
| Expected working life | ~12 months |
| Actual time to failure | ~3 months |
| Life achieved vs. prediction | ~25% |
| Failure mode | Cracking / complete fracture |
| 경도 | Within expected range |
| 열처리 | Not identified as the primary cause |
The fracture did not begin as uniform abrasive wear. Crack initiation occurred at the connection-hole region and then propagated rearward through the blade body, producing visibly distinct regions across the fracture face. Read as a system, the failure was an interaction between impact loading, stress concentration at the mounting geometry, and material/design fit — not a simple case of “the edge went dull.” Diagnosing this correctly matters, because a premature edge-rounding problem and a catastrophic fracture problem demand opposite engineering responses.
A Field-Verifiable Five-Step Failure Diagnosis
The most reliable way to separate a genuine material deficiency from a geometry- or impact-driven failure is a disciplined, evidence-based inspection sequence rather than a quick visual check:
- Operating History: Record actual service hours, processed tire type, unexpected shutdowns, blade or base replacement frequency, and any operator-reported abnormal vibration or impact events.
- Hardness Verification: Measure Rockwell hardness on the failed component. The goal is not to prove “harder is better” but to confirm whether the part was genuinely under- or over-hardened. In this case, hardness measured within the expected range, ruling out a simple hardness anomaly as the primary cause.
- Chemical Analysis: Verify that the actual steel chemistry matches the specified grade (here, AISI D2). An off-spec heat silently invalidates every subsequent conclusion.
- Macroscopic Fracture Inspection: Examine crack origin, crack direction, connection-hole geometry, and overall fracture morphology on the as-received part.
- Metallography and SEM: Use optical microscopy, scanning electron microscopy, and cross-sectional examination to confirm the crack-initiation site and map the propagation path.
Only after these steps can an engineer conclude whether the corrective action belongs in chemistry, heat treatment, geometry, or operator/application management.
In this instance, the correct response was a design-and-material requalification rather than a one-line “switch to a harder grade and the problem disappears.” Because the fracture originated at the mounting-hole geometry under impact, upgrading toughness around unchanged stress-concentration points would still concentrate load at the same location. A balanced evaluation starts with DC53, an 8% chromium cold-work tool steel that Daido’s tool-steel catalog lists as an 8Cr-2Mo grade combining high hardness with high toughness — which is what gives it its higher-impact-toughness advantage over SKD11 (D2-class) at comparable hardness, working around 58–60 HRC rather than chasing 62–63 HRC. Here fracture resistance matters more than maximum attainable hardness, and the chosen range must ultimately be validated against the actual hook geometry, section thickness, and heat-treatment result — not assumed from a datasheet.
원천: “Failure Analysis of an AISI D2 Blade-Base Used in Tire Waste Recycling Machine,” Engineering Failure Analysis, 2013 (Elsevier ScienceDirect). Figures in the case table above report the published study’s documented findings; the surrounding engineering-response discussion contextualizes them for blade procurement and requalification.
요약하자면: in the published case, hardness was within spec and heat treatment wasn’t the cause—the crack started at the mounting-hole stress concentration, meaning a harder or tougher grade alone would not have fixed it.
리스크 없는 호환용(Non-OEM) 나이프 조달

To reduce replacement tool budgets, many recycling operators procure non-OEM shredder blades. However, sourcing non-OEM components requires strict quality verification to prevent installation fitment issues and premature mechanical failure.
For the full incoming-inspection workflow this section summarizes—spec control, CMM sampling plans, and MTR documentation review—see 애프터마켓 파쇄기(shredder) 나이프 조달: 사양 관리, CMM 계획, MTR 검증 및 기능적 적합성 검증..
- Precision Dimensional Tolerances: Verify that mounting bores, hex shafts, and thickness dimensions conform to H7/f7 fits. A thickness variance of just +0.05 mm across a 20-blade rotor stack creates cumulative stack-up errors that destroy precise counter-knife clearance. The GD&T controls and selective-fit spacer strategy that prevent this kind of stack-up error on multi-shaft rotors are covered in 편마모 해결: 다축 슈레더 나이프의 누적 공차(Tolerance Stacking) 가이드.
- Metallurgical Certification: Demand official Material Test Certificates conforming to EN 10204 MTC 3.1. The certificate must document complete heat-lot chemical spectro-analysis and mechanical hardness testing.
- Ultrasonic Inspection: For heavy-section blades where internal soundness is a specified requirement, define the ultrasonic inspection method, acceptance class, and sampling plan separately in the purchase specification. ISO 4957 can be used to specify the tool-steel grade and material requirements, but it should not be presented as the ultrasonic inspection acceptance standard.
책임감 있는 주문 제작 나이프 제조사가 증명할 수 있어야 하는 핵심 사안
Asking for certificates on paper is one thing; being able to explain how those numbers were produced is another. Because procurement risk lives in the batch-to-batch gap between a datasheet and a delivered knife, Maxtor Metal runs every custom heavy-duty blade through a five-stage qualification protocol. This keeps a requested material change directed, documented, and traceable rather than assumed:
- Stage 1 — Incoming Material (traceability): For each heat, the steel grade, heat number, and mill certificate are recorded, with chemical composition and material thickness confirmed, and ultrasonic inspection performed on any heavy sections the drawing requires to be internally sound. Off-spec chemistry is stopped before it reaches a machine.
- Stage 2 — Heat-Treatment Verification: Each batch carries batch and furnace identifiers plus hardness mapping, quenching and tempering records, and dimensional-change readings, confirming that the delivered hardness profile matches the drawing rather than the invoice.
- Stage 3 — Blade Geometry: Critical dimensions — OD, ID, thickness, flatness, parallelism, mounting-hole position, edge radius, and edge runout — are measured on finished parts. This is where the ±0.05 mm stack-up errors that destroy counter-knife clearance are caught before a rotor set is assembled.
- Stage 4 — Failure Inspection on Returned Knives: When a customer returns a failed knife, the part is investigated rather than silently replaced: photography, macroscopic inspection, hardness mapping, chemical verification, crack-origin inspection and, when necessary, metallography and SEM to pin down the actual failure mode.
- Stage 5 — Material Decision and Re-qualification: Only after Stages 1–4 can an engineer answer the question that really drives replacement cost — not “D2 or DC53?” but “is this duty wear-dominated, impact-dominated, or stress-concentration-dominated?” — and then select and re-qualify the grade, hardness, and geometry accordingly.
This is offered as a method rather than as any single customer’s proprietary figures. The independently verifiable anchors for it remain the published D2 blade-base failure above and Daido’s own microstructural and impact data for DC53, so operators can check Maxtor Metal’s approach against their own evidence instead of taking a vendor’s word alone.
자주 묻는 질문
스틸벨트가 매립된 폐타이어 파쇄에 가장 적합한 공구강(Tool Steel) 소재는 무엇입니까?
고장력 스틸 와이어 및 이물질 금속이 혼입되는 폐타이어 1차 파쇄 공정에서는 58–60 HRC로 템퍼링된 DC53 공구강이 업계 표준으로 널리 인정받고 있습니다. 이 소재는 높은 내마모성을 유지하면서 표준 AISI D2(STD11) 대비 약 2배의 충격 인성을 제공합니다。
ELV 폐차 스크랩 처리 시 표준 D2 파쇄기 날에 치핑(날 나감) 현상이 발생하는 이유는 무엇인가요?
표준 AISI D2 강철의 미세 구조에는 조대한 일차 크롬 탄화물이 포함되어 있습니다. D2 칼날이 고장력 비드 와이어나 자동차 구조용 강재에 충격을 가할 때, 이러한 대형 탄화물은 응력 집중점으로 작용합니다. 이는 미세 균열을 유발하여 날 끝의 박리 및 빠른 치핑(날 나감) 현상으로 이어집니다.
1차 파쇄기용 나이프 소재로서 DC53은 D2(STD11) 대비 어떤 성능 차이가 있습니까?
DC53은 D2 강재의 금속 조직을 개선한 업그레이드형 공구강입니다. 탄소 함량을 최적화하고 고온 고온 2회 템퍼링(520–530°C)을 적용하여 미세한 탄화물 구조를 형성합니다. 이를 통해 동일한 경도(58–60 HRC) 조건에서 D2 대비 약 2배 높은 샬피 충격 인성을 확보하여, 강한 충격 하중 하에서도 파쇄 나이프의 전단 파손(대형 날 부러짐)을 효과적으로 방지합니다.
폐타이어 파쇄기 나이프의 적정 록웰 경도(HRC)는 얼마입니까?
폐타이어 및 ELV 1차 파쇄기의 경우 권장 경도 범위는 56–60 HRC입니다. 와이어가 제거된 깨끗한 고무 분말(Crumb)을 처리하는 2차 분쇄기(Granulator)의 경우, 내마모 수명을 극대화하기 위해 더 높은 경도 범위(60–62 HRC)를 적용할 수 있습니다.
폐타이어 1차 파쇄기 나이프 1세트는 재연마 전까지 몇 톤을 처리할 수 있습니까?
DC53 또는 정련된 D2와 같은 고품질, 금속학적으로 최적화된 공구강을 사용할 경우, 1차 폐타이어 파쇄기 나이프 1세트는 재연마 또는 하드페이싱(육성 용접) 보수가 필요하기 전까지 일반적으로 10,000~15,000톤의 폐타이어를 처리할 수 있습니다.
누적 두께 공차가 비순정(non-OEM) 파쇄기 나이프 Performance에 어떤 영향을 미치나요?
다구형 파쇄기 샤프트에서는 개별 나이프의 미세한 두께 오차가 로터 전체 길이에 걸쳐 누적됩니다. 개별 나이프의 공차가 단 ±0.03 mm만 초과하더라도 30개의 나이프를 적층할 경우 전체 측면 오차가 거의 1 mm에 달하게 됩니다. 이는 회전 날과 고정 날(Counter-knife) 간의 간섭, 과도한 마찰 및 로터 걸림(Jamming) 현상을 유발합니다.
비순정(non-OEM) 교체용 나이프 구매 시 어떤 품질 보증 서류를 요구해야 합니까?
화학 성분 및 열처리 배치 경도를 보증하는 EN 10204 MTC 3.1 소재 성적서(Mill Test Certificate), 내부 결함 유무를 확인하는 초음파 탐상 검사(UT) 보고서, 그리고 내경 공차 및 두께 평행도를 검증하는 CNC 치수 검사 성적서를 반드시 요구해야 합니다.
결론
폐타이어 및 ELV 폐차 스크랩 감용 파쇄 공정에서 수익성을 극대화하려면 단순히 가장 높은 경도의 나이프만을 찾는 것이 아니라 계산된 금속학적 전략이 필요합니다. 극단적인 HRC 경도는 이론적인 내마모성을 제공하지만, 실제 재활용 현장의 파쇄 공정에서는 높은 충격 인성과 구조적 피로 강도를 요구하는 강력한 충격 하중이 발생합니다. DC53과 같은 고급 공구강, 정밀 열처리, 응력 집중을 완화하는 블레이드 형상 설계로 록웰 경도와 샬피 충격 에너지를 최적으로 균형 있게 조율함으로써, 파쇄 나이프의 대형 전단 파손을 완전히 방지하고 톤당 총 운용 비용을 획기적으로 절감할 수 있습니다.
선도적인 재활용 기업들은 공구 예산을 효율적으로 절감하면서도 파쇄 설비의 안전성을 확보하기 위해 엄격한 금속학적 검증과 체계적인 비순정(non-OEM) 교체 부품 조달 프로세스를 결합하여 운용하고 있습니다.
면책 조항 및 정보 공개본 문서의 재료공학 지침은 엔지니어링 검토를 위한 객관적이고 현장 지향적인 기술 정보로 제공됩니다. Maxtor Metal은 맞춤형 정밀 연삭 산업용 나이프 전문 제조업체로서 본문에 언급된 칼날 제품을 공급할 수 있습니다. 장비 또는 공정 성능에 대한 모든 언급은 검증된 사례 데이터와 공인된 공구강 규격을 반영한 것이며, 특정 결과에 대한 보증을 의미하지는 않습니다. 설비 운용자는 자체 파쇄 설비 및 작업 조건에 맞게 소재, 형상, 열처리 사양을 직접 검증해야 합니다。
To explore custom blade geometries, material test certifications, and long-life replacement options for your machinery, consult with the engineering specialists at Maxtor Metal for custom industrial shredder blade replacement solutions.
저자 소개
낸시 우 — Senior Manufacturing Engineer, PE (Production Engineering), Maxtor Metal
Nancy Wu brings 12 years of hands-on manufacturing-engineering experience to industrial blade design and production. Her expertise spans the machining, material, and coating characteristics of the most common industrial blade grades — including SKD11, D2, M2, H13, powder-metallurgy steels, and tungsten carbide — along with advanced high-precision CNC grinding programming capability.
She holds the SME Certified Manufacturing Engineer (CMfgE), PMP, Six Sigma Black Belt, and ASM International certifications, applying disciplined process control and quality methodology to the tool-steel solutions discussed throughout this guide.
 English
 Spanish
 Italian
 French
 Portuguese
 Russian
 German
 Arabic
 Hindi
 Vietnamese
 Indonesian
 Japanese
 Korean