

Blade selection is one of the fastest levers you can pull to improve pellet uniformity, uptime, and total cost. In strand pelletizing, the blade story is about helical scissor geometry, rotor‑to‑bed knife gap, and how quickly wear drifts that gap. In underwater pelletizing (die‑face/water‑ring), it’s about keeping a clean, stable cut through controlled knife contact pressure, thermal balance at startup, and robust process‑water flow.
In this guide, you’ll compare materials, geometries, gap/pressure windows, and coatings for masterbatch pelletizer blades. We focus on two real production pain points: underwater startup stability and knife pressure control (tails/fines), and strand gap drift and changeover cadence—while providing a practical selection matrix to speed decisions.
Những điểm chính cần ghi nhớ
- Underwater pelletizing: start with a controlled engage pressure, then trim down as the system stabilizes; maintain a warm die at startup and sufficient water flow to prevent tails/fines spikes, per OEM guidance such as ECON and MAAG/Gala, and application notes from Xinda and Plastics Technology.
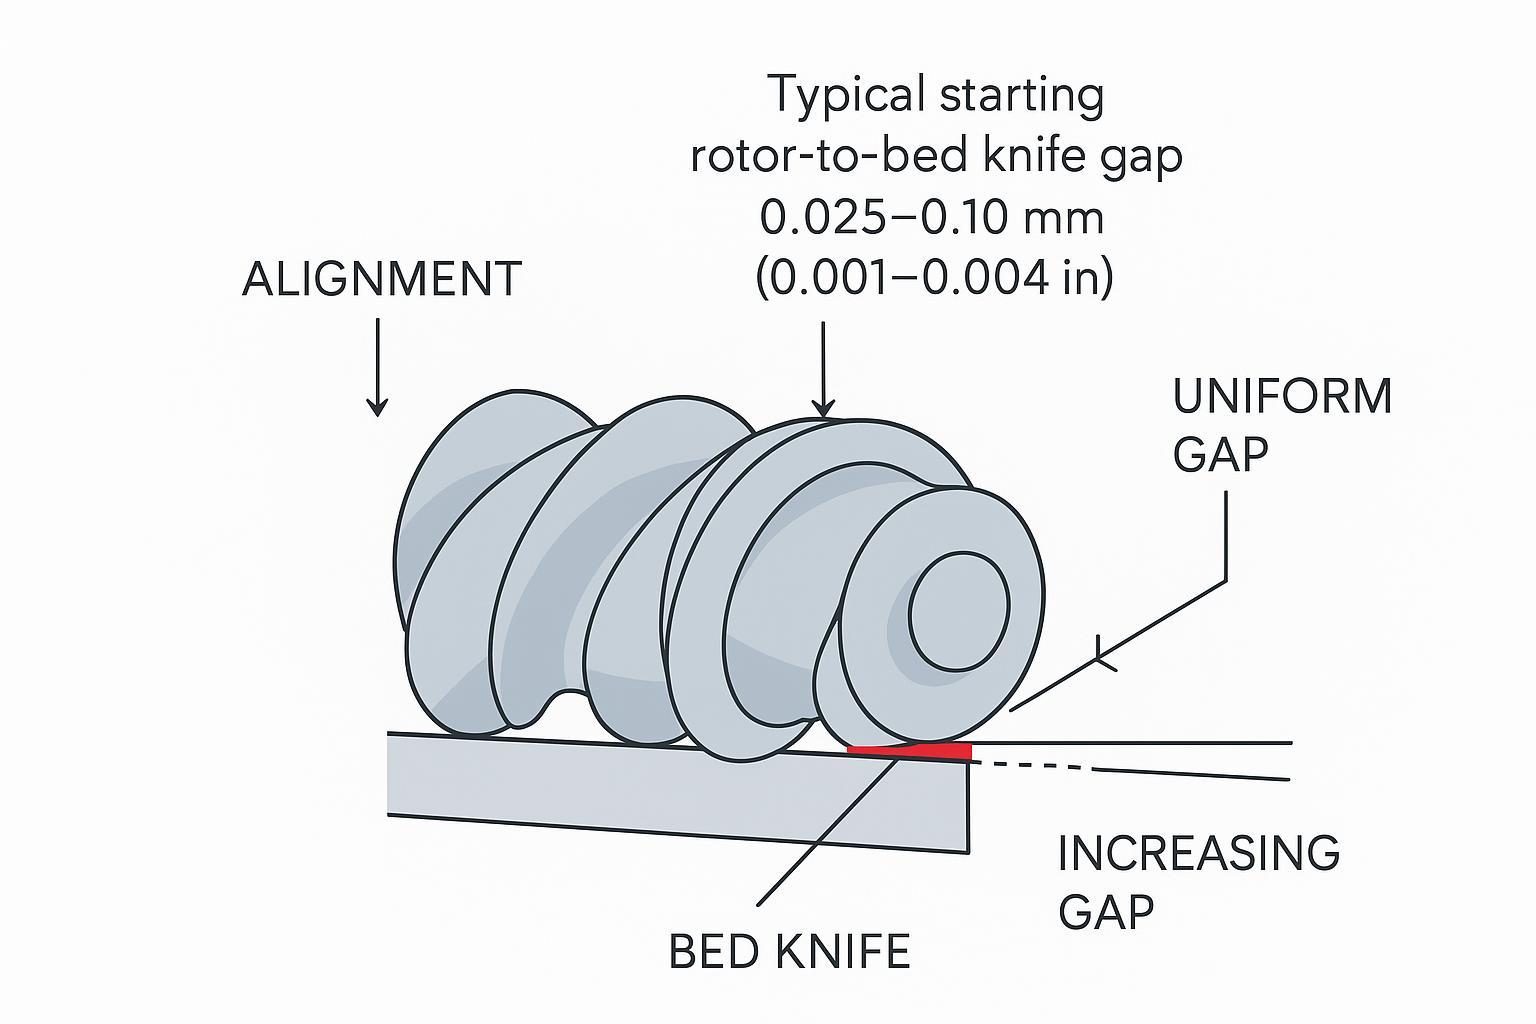
- Strand pelletizing: a sharp helical rotor cutting against a straight bed knife with a uniform, tight starting gap window (on the order of 0.025–0.10 mm) reduces fines—re‑gap and realign as wear accumulates.
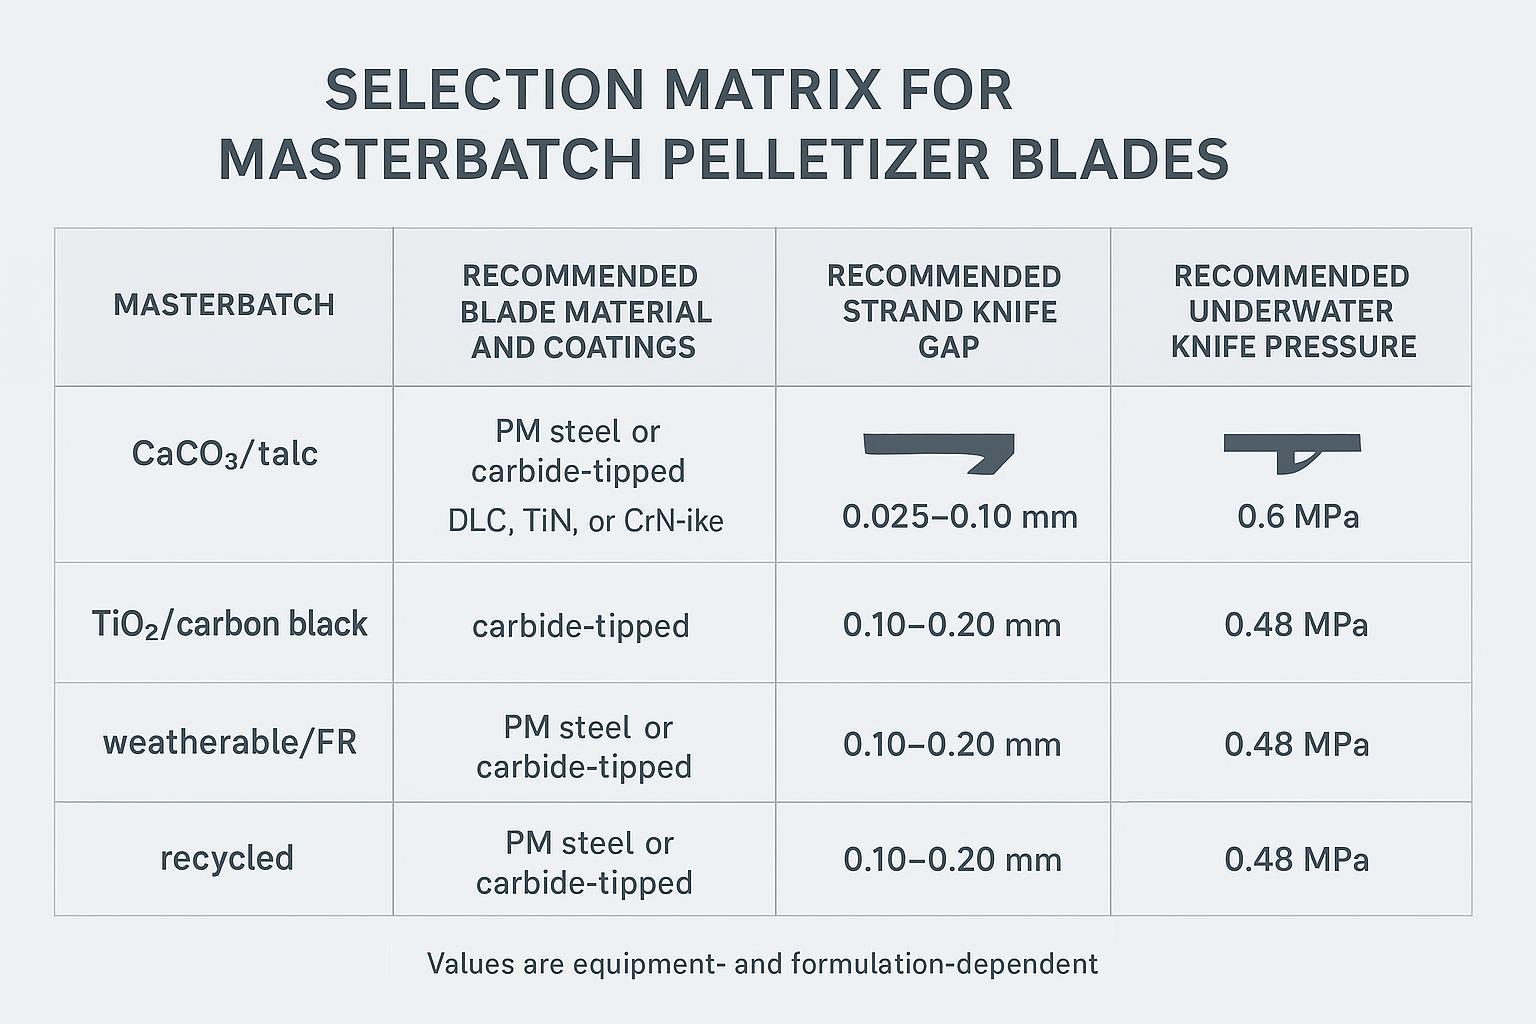
- Abrasive masterbatches (CaCO3/talc) favor tougher, wear‑resistant substrates (PM steels, carbide‑tipped) and low‑friction coatings; TiO2/carbon black reward tough substrates with anti‑pickup coatings.
- Always treat numbers here as “typical starting windows.” Confirm against your OEM manual and validate in trials for your formulation and throughput.
Strand pelletizing essentials
Rotor/bed materials for abrasives
For high‑fill CaCO3 or talc masterbatches, abrasion quickly rounds cutting edges. Practical starting choices include D2/SKD11 as a baseline, M2 HSS or PM‑grade tool steels (vanadium‑rich) where heat and wear are severe, and, in extreme cases, carbide‑tipped bed knives. Typical knife body hardness targets sit roughly in the 57–62 HRC band (grade‑dependent), extending life without making edges so brittle that micro‑chipping cascades into fines. Vendor summaries and OEM pages describe these ranges and coating options, for example in Sollex’s pellet blade overview (typical 55–62 HRC) and MAAG’s knife and holder documentation. See the discussions in the Sollex category page on pellet blades and MAAG’s knife‑holders and knives pages for reference.
- According to the Sollex overview of pellet blades (typical hardness ranges 55–62 HRC), harder substrates plus PVD coatings such as TiN/CrN/DLC‑like can extend service life while reducing pickup. Source: the Sollex pellet blades overview.
- MAAG’s strand pelletizer literature emphasizes precision alignment and durable cutting components, which are essential when running abrasive fillers at speed. Source: MAAG strand pelletizer brochures.
Helical scissor geometry and gap
Underwater pelletizing: start with a controlled engage pressure, then trim down as the system stabilizes; maintain a warm die at startup and sufficient water flow to prevent tails/fines spikes (Plastics Technology — “Mitigating and Troubleshooting Underwater Pelletizing Issues”, 2020; MAAG — PURO tempered‑water systems brochure, 2016; Xinda application note, accessed 2026).
- For background on scissor action and upstream influences, see the Plastics Technology article on what happens between extruder and pelletizer.
- For practical troubleshooting cues (e.g., when to re‑gap), see Plastics Technology’s “Solve Seven Common Pelletizing Problems.”
Changeovers and adjustment
- Verify rotor/bed knife sharpness and clean seating surfaces; torque fasteners per the OEM spec. Use the built‑in eccentric adjustment to “dial in” uniform contact, then back off to the target gap.
- Present strands squarely: maintain feed‑roll grip and replace grooved rolls; minimize push distance from nip to cut point; keep strand diameters consistent from the die/stranding plate. These steps are repeatedly called out in Plastics Technology problem‑solving features.
- Re‑gap at the first sign of rising fines/length variance or after any blade touch, and log hours/tons per edge to establish a changeover cadence.
- OEM/model-size example tolerances and torque (public-facing examples): For small/compact (T‑class) chambers expect flatness/parallelism targets in the order of 0.01–0.03 mm and clamp/fastener torque examples of 8–12 N·m for common knife‑holder bolts. For large/industrial (S‑class) chambers expect flatness ≈0.02–0.05 mm and clamp torque 12–20 N·m as a vendor‑level example. These figures reflect aftermarket/vendor precision claims (see Cowles Tool precision claims Và GL Knife concentricity claims) and MAAG/Gala model families for context (see MAAG strand pelletizer family pages). Always follow your OEM service manual as authoritative and validate on‑machine with a torque wrench and flatness gauge.
Underwater pelletizing essentials
Knife materials and coatings
Underwater service adds corrosion and thermal cycling to the wear equation. Tool steels like D2 and M2 HSS are common baselines; PM grades offer better abrasion resistance; in corrosive or aqueous environments some OEMs note stainless tool steels (e.g., 440‑series) at moderate hardness. Typical underwater blade hardness references cluster around ~55–60 HRC to balance toughness with life. Coatings such as TiN/CrN or DLC‑like films help limit adhesion and abrasion. For representative ranges and construction concepts (e.g., self‑sharpening blades, TC nibs on die faces), see MAAG/Gala documentation on knife holders and AMN dies, as well as the Sollex overview of pellet blades and X‑Keen’s example (57–60 HRC) for underwater knives.
- MAAG/Gala documents insulated dies and self‑sharpening concepts that maintain a consistent edge at the die face. See MAAG’s knife‑holders and AMN die pages.
- The Sollex pellet blade overview summarizes hardness and coating choices commonly used across pelletizing applications.
Contact pressure control
Knife contact pressure is a primary quality and life lever. Many systems engage with a higher force to ensure a clean initial cut, then reduce as the system stabilizes.
- Pneumatic control: Xinda’s application note describes a manual startup where feeding air is set around 0.6 MPa to engage, then reduced stepwise (≈0.01 MPa increments) toward ≈0.48 MPa before switching to automatic, while monitoring cutter motor current. Treat these as equipment‑specific examples and adjust by resin and die size. See Xinda’s guidance on underwater pelletizer control.
- Servo/hydraulic control: ECON’s EUP documentation emphasizes thermal insulation and controlled knife force to maintain contact without die freeze sensitivity across output swings. See ECON’s EUP overview.
- General principle: Avoid sudden pressure changes; track cutter current and surface wear marks; excessive force accelerates wear and can trigger sticking or padding at the die face. Plastics Technology’s selection/troubleshooting coverage reinforces these points.
Độ ổn định của nước và khi khởi động
Khởi động ổn định giúp giữ thông các lỗ đùn và hạt nhựa sạch.
- Nhiệt độ khuôn đùn so với nhiệt độ nóng chảy: Plastics Technology khuyên dùng mức chênh lệch khởi động thực tế, trong đó khuôn đùn được giữ cao hơn nhiệt độ nóng chảy khoảng 25°F (≈14°C) khi khởi động để tránh bị đông đặc; điều chỉnh theo loại nhựa và điều kiện thực tế tại nhà máy. Xem các bài viết khắc phục sự cố cắt hạt dưới nước của Plastics Technology để biết cách giảm thiểu và giải quyết các vấn đề thường gặp.
- Nhiệt độ và lưu lượng nước công nghệ: MAAG/Gala lưu ý rằng với khuôn đùn cách nhiệt, nước công nghệ thường không cần vượt quá khoảng 70°C khi khởi động, và lưu lượng tiêu chuẩn là đủ khi được hướng chính xác vào khuôn đùn. Đường cong bơm của nhà sản xuất thiết bị gốc (OEM) cho thấy lưu lượng tỷ lệ thuận với năng suất—ví dụ: hệ thống nước điều ôn PURO ghi nhận khoảng 15 m³/h (~250 L/min) ở mức năng suất gần 500 kg/h cho đến ~70 m³/h (~1,167 L/min) ở các dải năng suất cao hơn. Xem tài liệu giới thiệu về hệ thống nước điều ôn PURO của MAAG và Gala để biết các giá trị tiêu biểu.
Các khoảng thông số khởi động điển hình (tham khảo nhanh)
| Tham số | Khoảng thông số khởi động | Tài liệu chứng minh (nhà xuất bản, năm) |
|---|---|---|
| Khe hở giữa dao rotor và dao tĩnh (bed knife) của máy cắt sợi | ≈ 0.025–0.10 mm (0.001–0.004 in) đối với dao sắc; sau đó điều chỉnh | Các bài viết khắc phục sự cố của Plastics Technology; hướng dẫn điều chỉnh của OEM |
| Áp lực ép dao → tinh chỉnh dao cắt hạt dưới nước (ví dụ hệ thống khí nén) | Ép dao ≈ 0.6 MPa → tinh chỉnh ≈ 0.48 MPa trước khi chuyển sang chế độ tự động; bước điều chỉnh ≈ 0.01 MPa trong khi theo dõi dòng điện của động cơ | Tài liệu ứng dụng của Xinda (truy cập năm 2026) |
| Nhiệt độ khuôn đùn so với nhiệt độ nóng chảy khi khởi động hệ thống cắt hạt dưới nước | Khuôn đùn ≈ nhiệt độ nóng chảy + 25°F (≈14°C) khi khởi động | Tài liệu khắc phục sự cố cắt hạt dưới nước của Plastics Technology (giai đoạn 2019–2023) |
| Nhiệt độ nước công nghệ | Thông thường ≤ 70°C là đủ đối với khuôn đùn cách nhiệt | Tài liệu giới thiệu của MAAG/Gala (lưu ý về CPT/khuôn đùn cách nhiệt) |
| Lưu lượng nước công nghệ so với năng suất | Tỷ lệ thuận với kg/h (ví dụ: ~15 m³/h ở mức ~500 kg/h → ~70 m³/h ở mức ~4,000–6,000 kg/h) | Tài liệu giới thiệu hệ thống nước điều ôn MAAG PURO |
| Nhựa | Cắt hạt dưới nước (UW) — áp lực dao & ép dao→tinh chỉnh; nhiệt độ khuôn đùn so với nhiệt độ nóng chảy khi khởi động | Cắt sợi — khe hở ban đầu giữa rotor→dao tĩnh & mẹo điều chỉnh |
|---|---|---|
| PP (polypropylene) | Ví dụ/khoảng thông số khởi động: Áp lực cấp khí nén ép dao ≈ 55–0.65 MPa, tinh chỉnh theo các bước ≈0.01 MPa hướng tới ~0,45–0,50 MPa khi dòng điện và chất lượng hạt nhựa ổn định; giữ khuôn đùn ~nhiệt độ nóng chảy + 25°F (≈14°C) khi khởi động; giữ nước công nghệ ≤70°C và xác minh lưu lượng theo đường cong bơm của OEM (xem Hướng dẫn của Xinda năm 2021; Công nghệ Nhựa 2020). | Ví dụ/khoảng thông số khởi động: Bắt đầu với khe hở hẹp—~0,03–0,08 mm—sau đó chạy thử nghiệm ngắn ở tốc độ dây chuyền và tăng khe hở thêm 0.01–0.02 mm nếu xảy ra ma sát hoặc nhiệt độ tăng; điều chỉnh lại khe hở ngay khi có dấu hiệu đầu tiên của mạt nhựa/sự sai lệch chiều dài hạt (xem Tài liệu khắc phục sự cố của Plastics Technology). |
| PE (HDPE/LDPE) | Ví dụ/khoảng thông số khởi động: Ép dao ≈ 50–0.60 MPa, tinh chỉnh hướng tới ~0,42–0,50 MPa trong khi theo dõi dòng điện động cơ dao cắt; đặt nhiệt độ khuôn đùn ≈ nhiệt độ nóng chảy + 25°F (≈14°C) khi khởi động và đảm bảo tốc độ dòng nước đầy đủ theo hướng dẫn lưu lượng của MAAG/Gala (Tài liệu giới thiệu MAAG PURO năm 2016); xử lý HDPE ở mức lực cao hơn so với LDPE. | Ví dụ/khoảng thông số khởi động: Bắt đầu ở mức ~0,03–0,10 mm (HDPE cứng hơn → chọn giới hạn dưới; LDPE mềm hơn → chọn giới hạn cao hơn một chút); xác minh độ cứng của sợi nhựa trước khi cắt và sử dụng các bộ điều chỉnh lệch tâm để cân bằng tiếp xúc trên toàn bộ rotor. |
| PA (nylon) | Example/starting window: Engage slightly lower or more cautiously—~0.45–0.55 MPa engage, trim to ~0.40–0.48 MPa; maintain die warm (melt + ~14°C) to prevent freeze and reduce hole plugging—nylons are sensitive to thermal gradients (see Công nghệ Nhựa 2020 Và Cowin extrusion 2026). | Example/starting window: Use ~0.04–0.10 mm starting gap depending on strand diameter; avoid shock cuts—confirm strand straightness and use slower ramp-up of rotor speed during commissioning. |
| PET (amorphous & semi-crystalline) | Example/starting window: For high‑MFI or hygroscopic PET, engage ~0.50–0.60 MPa, trim to ~0,45–0,50 MPa while watching cutter current and hole integrity; hold die ≈ nhiệt độ nóng chảy + 25°F (≈14°C) and ensure dehumidified feed and stable water temperature per OEM practice (MAAG/Gala 2016; [Plastics Technology 2020]). | Ví dụ/khoảng thông số khởi động: Bắt đầu ở mức ~0.03–0.07 mm for brittle melts; prioritize strand cooling uniformity and run short validation batches—increase gap only if streaking or rubbed surfaces appear. |
All values are equipment- and formulation-dependent example/starting windows; always confirm with your OEM manual and validate in short trials while monitoring cutter current, fines/tails, and die hole integrity.
Notes: Values are starting points. Confirm against your OEM manual and validate through trials.
Selection criteria for blades
Match to masterbatch type
- High CaCO3/talc (abrasive): PM tool steels or carbide‑tipped knives; consider DLC/TiN/CrN‑like coatings to lower friction and extend life. Emphasize precise alignment (strand) and controlled contact force (underwater).
- TiO2 or carbon black (edge chipping and pickup): Favor tough substrates (D2/PM); use low‑friction coatings (DLC‑/CrN‑like) to reduce buildup; maintain sharpness to avoid micro‑chipping.
- Weatherable/FR systems (deposition/corrosion risk): Pair low‑friction wear coatings with corrosion‑resistant substrates (e.g., 440‑series in aqueous environments). Manage water chemistry.
- Recycled/heterogeneous compounds (impurities): Balance abrasion resistance and toughness with PM steels or carbide‑tipped designs; for underwater, avoid overly brittle edges and monitor for corrosion.
Tolerances and life extension
Specify flatness, parallelism, and edge geometry tightly enough to keep the working gap or contact condition stable as wear accumulates. On strand systems, even tens of microns of drift can raise fines; on underwater systems, force that is too high to “chase” a worn geometry often shortens life. Coatings that reduce adhesion lower the torque/current spikes that precede tails and fines.
Specify masterbatch blades
Disclosure: MAXTOR METAL is our product. KIM LOẠI MAXTOR offers custom, precision‑ground pelletizer blades that can be specified with tighter tolerances and ceramic‑like coatings to extend service intervals on highly abrasive CaCO3‑filled masterbatches.
- Example request to vendors: “For a CaCO3/talc masterbatch at X kg/h, strand pelletizer target gap 0.025–0.10 mm; recommend PM‑grade or carbide‑tipped bed knife with low‑friction coating. For underwater on the same formulation, propose a tough substrate (~55–60 HRC) with DLC‑like coating and knife‑force engage‑then‑trim procedure per our OEM.”
Maintenance and ROI
Mini case examples (representative plant examples — not universal)
Case A — Underwater, high‑CaCO3 masterbatch (die‑face water ring)
- Context: 800 kg/h line, PE masterbatch with 25% CaCO3; symptoms: tails/fines ~1.8% by weight and frequent cutter trips. Intervention: replace uncoated D2 knives with DLC‑like coated PM‑grade knives and adopt an engage→trim pneumatic routine (engage ≈ 0.60 MPa → trim to ≈ 0.48 MPa while monitoring cutter current). Result (after 2 weeks): fines fell to ~0.7%, average cutter motor current dropped ~12%, mean hours per blade edge rose from ~120 h to ~210 h, and unplanned stops fell from 3/month to 1/month. Improvements align with pressure/startup guidance from Xinda application notes and die‑thermal practice summarized by Plastics Technology.
Case B — Strand, high‑fill talc masterbatch
- Context: 600 kg/h strand line, PP masterbatch with 30% talc; symptoms: length variance and fines ~1.5%, blade changeovers every 5 days. Intervention: switch to carbide‑tipped bed knives, tightened re‑gap routine to a starting window of ~0.03–0.08 mm, and formalized alignment checklist. Result (30‑day trial): fines reduced to ~0.5%, average edge life increased from 90 h to ~220 h between regrinds, changeovers dropped 55%, and estimated blade‑related cost‑per‑ton improved by ~18% (materials + labor + avoided downtime). Findings are consistent with strand gap and carbide‑tip recommendations in vendor/industry literature (see Tài liệu khắc phục sự cố của Plastics Technology and MAAG strand guidance).
Preventive routines
- Underwater: verify knife force setpoints (feed/return or servo), inspect the die face and blade wear tracks, confirm water temperature and flow, and use the OEM’s circulation/bypass steps before engagement. See the guidance in Plastics Technology’s mitigation article on underwater pelletizing issues and MAAG/Gala’s brochures on insulated dies and startup practices.
- Strand: check rotor and bed edges for rounding, re‑gap to your target window, maintain feed‑roll grip and alignment, and ensure strand conditioning upstream (bath length, guide‑roll condition) remains stable. Plastics Technology’s “Solve Seven Common Pelletizing Problems” provides relevant cues.
Sharpening/rotation strategy
Rotate multi‑edge bed knives and sharpen before edges round to the point where motor current and fines rise. For underwater systems equipped with in‑operation grinding, use it to refresh edges without stopping. Log hours/tons per edge set and relate to tails/fines to set a data‑driven rotation cadence.
Cost‑per‑ton tracking
Track total blade cost (purchase + sharpening) plus labor and downtime across each edge set, divided by tons produced on that set. Correlate with tails/fines and cutter current to flag early degradation. As a simple worked example: if a carbide‑tipped underwater knife set costs $X and runs Y tons between planned refreshes, while reducing tails by Z% (cutting rework and unplanned stops), calculate cost/ton with and without the improved set and compare against your downtime value per hour. This method mirrors standard maintenance economics used in plant optimization literature.
Strand and underwater pelletizing reward different priorities. On strand lines, keep a sharp helical‑to‑straight scissor cut with a tight, uniform gap and re‑gap as wear accumulates. On underwater lines, control knife force through a stable engage‑then‑trim routine, keep the die warm at startup, and ensure adequate, well‑directed process‑water flow. Match blade substrates and coatings to your masterbatch—abrasive fillers push you toward tougher PM steels or carbide‑tipped edges with low‑friction coatings; sticky or brittle systems benefit from tough substrates and anti‑pickup surfaces. Next steps: define your gap/pressure target windows, specify materials/coatings aligned to your formulation, and validate through short trials while logging fines/tails and cost‑per‑ton.
References (selected; each URL used once)
- Xinda — knife pressure via feeding/return air (engage ≈0.6 MPa → trim ≈0.48 MPa; step ≈0.01 MPa; accessed 2026): https://www.xindacorp.com/how-to-control-pellet-moisture-with-underwater-pelletizer-2/
- Plastics Technology — mitigating and troubleshooting underwater pelletizing issues (die ≈ melt + 25°F; startup practices): https://www.ptonline.com/blog/post/mitigating-and-troubleshooting-underwater-pelletizing-issues
- ECON EUP — thermal insulation and controlled knife force: https://www.econ.eu/eup.html
- MAAG — PURO tempered‑water systems (flow vs throughput examples): https://maag.com/wp-content/uploads/PURO_Tempered-Process-Water-Systems.pdf
- Plastics Technology — Solve Seven Common Pelletizing Problems (strand alignment/gap cues): https://www.ptonline.com/articles/solve-seven-common-pelletizing-problems

 English
 Spanish
 Italian
 French
 Portuguese
 Russian
 German
 Arabic
 Hindi
 Vietnamese
 Indonesian
 Japanese
 Korean
4 bình luận
Thanks for breaking down the nuances between strand and underwater pelletizing blade requirements—especially the emphasis on gap control and startup stability really resonates with the challenges we’ve seen in production. It’s easy to overlook how critical consistent knife contact pressure and thermal balance are for maintaining pellet quality, particularly during those tricky start-up phases. Your take on wear drift and its impact on uptime is spot on, and it reinforces why blade selection should be a strategic consideration rather than an afterthought.