

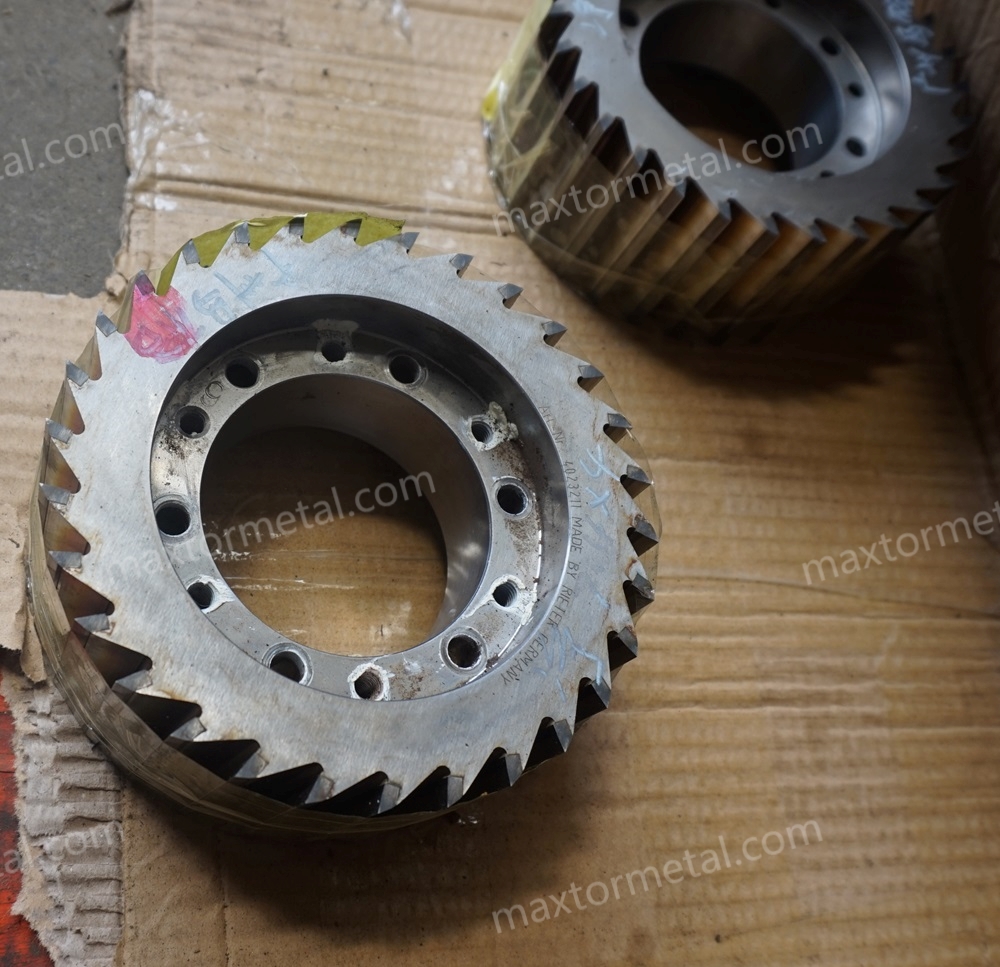
वाटर-स्ट्रैंड पेलेटाइजिंग (Water-strand pelletising) यूके के कंपाउंडिंग और रीसाइक्लिंग उद्योगों में एक मुख्य आधार है। फिर भी अपघर्षक (abrasive), हाई-फिल और रीसायकल किए गए फॉर्मूलेशन में, सॉलिड रोटरी चाकू तेजी से घिसते हैं, बदलाव (changeovers) में लंबा समय लगता है, और पेलेट की गुणवत्ता प्रभावित होती है—फाइन्स और टेल्स (fines and tails) बढ़ जाते हैं, और ऑपरेटरों को बार-बार क्लीयरेंस को एडजस्ट करना पड़ता है। इंसर्टेड ब्लेड रोटरी कटर (Inserted blade rotary cutter) डिज़ाइन एक मोनोलिथिक रोटर को हटाने और फिर से ग्राइंड करने के बजाय आपको इन-सीटू (in situ) किनारों को इंडेक्स या बदलने की अनुमति देकर मूल कारणों पर प्रहार करते हैं।.
यह गाइड Maag/Automatik PRIMO/PRIMOplus और Scheer/SGS-स्टाइल स्ट्रैंड पेलेटाइजर्स चलाने वाले यूके के प्लांटों पर केंद्रित है। यह बुनियादी समस्याओं—तेजी से घिसना, लंबे बदलाव (changeovers), फाइन्स/टेल्स और पेलेट भिन्नता—का समाधान करती है और बताती है कि कैसे इंसर्टेड/इंडेक्सेबल सिस्टम रखरखाव के प्रयास को कम कर सकते हैं, बदलावों को नियंत्रित, दोहराने योग्य रूटीन में समेट सकते हैं, और अच्छी कूलिंग और एलाइनमेंट प्रथाओं के सहयोग से गुणवत्ता को स्थिर कर सकते हैं।.
डेटा क्या दिखाता है? समान ड्राई-कट स्ट्रैंड पेलेटाइजर्स पर OEM सामग्री टूल-लेस एक्सेस और मॉड्यूलर हेड्स के माध्यम से डिस्असेंबली और बदलाव के समय में महत्वपूर्ण कमी का दस्तावेजीकरण करती है—उदाहरण के लिए, MAAG की T200 सीरीज रिपोर्ट करती है कि कुछ डिस्असेंबली चरण लगभग 30 मिनट से घटकर लगभग 2 मिनट रह गए, जैसा कि निर्माता के T200 सीरीज पेज, पर वर्णित है, और PRIMO FC फैमिली 30 मिनट से अधिक समय में रोटर प्रतिस्थापन न होने का उल्लेख एक प्रदर्शन नवाचारों पर निर्माता के समाचार संक्षिप्त विवरण में करती है. । ये आंकड़े मॉडल-विशिष्ट हैं, न कि इंसर्टेड बनाम सॉलिड चाकू की सीधी तुलना, इसलिए इस गाइड में हम सुधार बैंड जैसे कि 20–50% रखरखाव में कमी, 15–45 मिनट के बदलाव, और 2–5× एज लाइफ को स्पष्ट मान्यताओं और सीमाओं के साथ इंजीनियरिंग योजना श्रेणियों के रूप में मानते हैं।.
इस गाइड का उपयोग कैसे करें: मैकेनिक्स (इंसर्टेड सिस्टम कैसे भिन्न होते हैं) को समझें, फिर रखरखाव लागत मॉडल (TCO), उसके बाद अपटाइम/गुणवत्ता प्रथाएं, अनुकूलता के जोखिम को कम करने के लिए एक रेट्रोफिट चेकलिस्ट, और अंत में आपकी लाइन पर लाभ साबित करने के लिए KPIs के साथ एक सत्यापन योजना।.
चाबी छीनना
- वाटर-स्ट्रैंड पेलेटाइजिंग के लिए इंसर्टेड ब्लेड रोटरी कटर इन-सीटू एज इंडेक्सिंग को सक्षम करके व्यावहारिक रखरखाव और डाउनटाइम को कम कर सकता है; जब तक कि साइट डेटा अन्यथा साबित न करे, एक रूढ़िवादी इंजीनियरिंग रेंज के रूप में 20–50% रखरखाव घंटे की कमी की योजना बनाएं।.
- जब दायरा परिभाषित हो, टूलिंग तैयार हो, और सुरक्षित कार्य प्रणालियों का पालन किया जाए, तो इंडेक्सिंग या इंसर्ट स्वैप के लिए बदलाव 15–45 मिनट की विंडो में होने की उम्मीद करें; संबंधित मॉडलों पर समान OEM दावे तंत्र का समर्थन करते हैं, न कि सीधे समान-से-समान तुलना का।.
- उपयुक्त सामग्री, हीट ट्रीटमेंट और नियंत्रित एज रेडियस के साथ, इंडेक्सेबल इंसर्ट अपघर्षक कार्य में 2–5× उपयोगी एज-लाइफ विंडो प्रदान कर सकते हैं; एक मिलान किए गए पूर्व/पश्चात परीक्षण और प्रलेखित माप विंडो के साथ सत्यापित करें।.
- स्वामित्व की कुल लागत (Total cost of ownership) बदल जाती है क्योंकि जब रोटर मशीन में रहते हैं तो श्रम और खोया हुआ उत्पादन कम हो जाता है; पुर्जों का खर्च रोटर रीग्राइंड से इंसर्ट सेट पर स्थानांतरित हो जाता है—जो अक्सर प्रति-टन के आधार पर शुद्ध-तटस्थ से कम होता है।.
- पेलेट की गुणवत्ता की स्थिरता कटर डिज़ाइन के साथ-साथ गैप/एलाइनमेंट और कूलिंग पर भी निर्भर करती है; क्लीयरेंस, रन-आउट और बैलेंस के लिए औपचारिक जांच का उपयोग करें, और ASTM-संरेखित तरीकों के माध्यम से फाइन्स को नियंत्रित करें।.
How it works
इंसर्ट सिस्टम बनाम सॉलिड चाकू
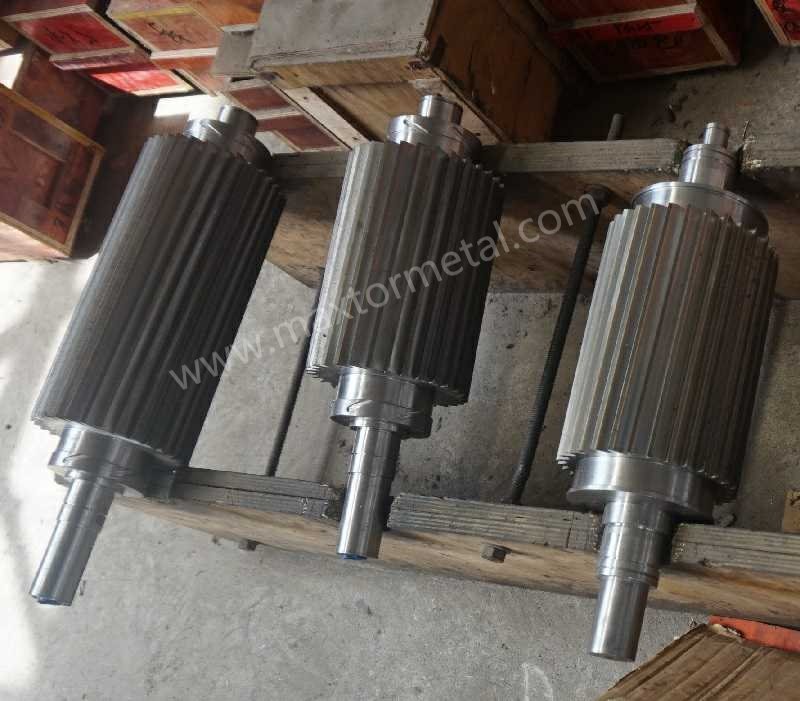
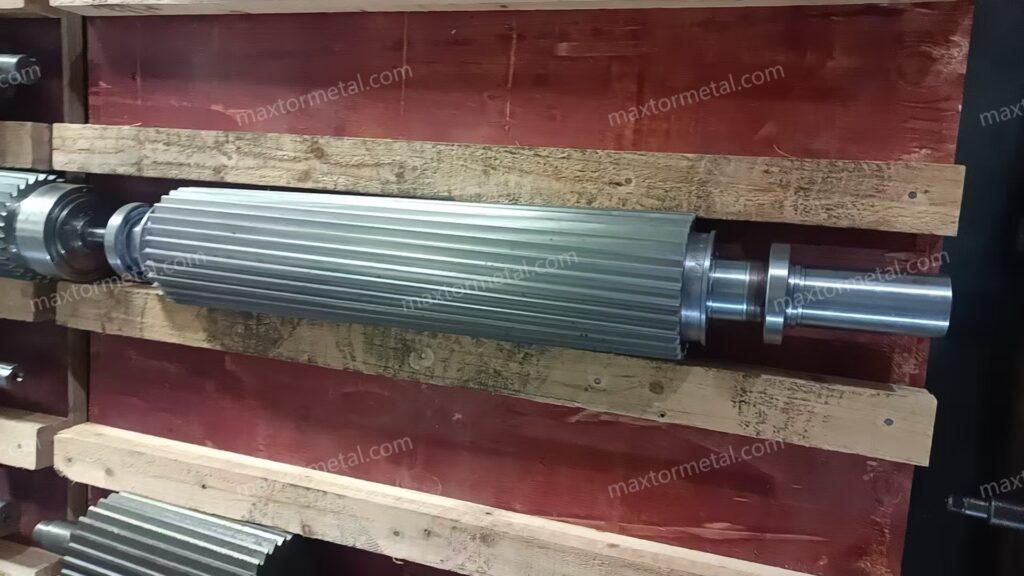
इंसर्टेड या इंडेक्सेबल सिस्टम रोटर पर प्रिसिजन-मिल्ड पॉकेट्स में छोटे, कड़े किए गए कटिंग इंसर्ट माउंट करते हैं। जब कोई किनारा सुस्त (dull) हो जाता है, तो आप रीग्राइंड के लिए पूरे रोटर को हटाने के बजाय इंसर्ट को इंडेक्स या बदलते हैं। सॉलिड चाकू (मोनोलिथिक रोटर्स) को किनारे को बहाल करने के लिए रोटर को हटाने और रीग्राइंड करने की आवश्यकता होती है।.
| पहलू | इंसर्टेड/इंडेक्सेबल सिस्टम | सॉलिड चाकू/मोनोलिथिक रोटर |
|---|---|---|
| एज रिन्यूअल (किनारे का नवीनीकरण) | इन-सीटू (in situ) इंसर्ट को इंडेक्स/बदलें | रोटर निकालें, रीग्राइंड करें, फिर से स्थापित करें |
| विशिष्ट बदलाव (changeover) का दायरा | इंसर्ट क्लैम्प्स को ढीला करें, इंडेक्स करें, टॉर्क दें, गैप सत्यापित करें | लॉकआउट, डिस्असेंबल करें, रोटर निकालें, ऑफ-लाइन रीग्राइंड करें, फिर से स्थापित करें, री-एलाइन करें |
| रीग्राइंड चक्र (Regrind cycle) | अक्सर टाला या स्थगित किया जाता है | नियमित, संचयी सामग्री हटाने के साथ |
| अपघर्षक कार्य उपयुक्तता (Abrasive duty suitability) | PM स्टील्स/कोटिंग्स और माइक्रो-होन (micro-hone) के साथ अनुकूल | चिपिंग और लंबे रीग्राइंड डाउनटाइम के प्रति संवेदनशील |
| जोखिम बिंदु (Risk points) | पॉकेट घिसाव, क्लैंप टॉर्क अनुशासन | हैंडलिंग क्षति, रीग्राइंड परिवर्तनशीलता |
PRIMO/PRIMOplus के लिए OEM साहित्य पहुंच और त्वरित टूल एक्सचेंज को रेखांकित करता है, और समान MAAG मॉडल डिस्असेंबली और सब-असेंबली के लिए बड़े समय की बचत का दस्तावेजीकरण करते हैं, जो यह बताता है कि अनुशासित SOPs के साथ लागू होने पर इंसर्टेड सिस्टम अक्सर रखरखाव को आधा क्यों कर देते हैं।.
सामग्री और एज ज्योमेट्री (Materials and edge geometry)
अपघर्षक, हाई-फिल और रीसायकल किए गए कंपाउंड्स (ग्लास फाइबर, CaCO3, संदूषक) के लिए, स्थायित्व स्टील ग्रेड, हीट ट्रीटमेंट, सतह की स्थिति और एज ज्योमेट्री के एक साथ काम करने से आता है:
- उच्च घिसाव प्रतिरोध वाले टूल या पाउडर-मेटालर्जी स्टील्स, जो कार्य के लिए उपयुक्त सत्यापित Rockwell C मानों पर टेम्पर्ड होते हैं, माइक्रो-चिपिंग को कम करते हैं।.
- कटिंग एज पर एक नियंत्रित माइक्रो-होन (micro-hone) रेडियस भंगुर फ्रैक्चर का प्रतिरोध करता है और कट को सटीक बनाए रखता है।.
- TiN/TiCN जैसी कोटिंग्स या हार्डमेटल टिपिंग का उपयोग वहां किया जा सकता है जहां वे इंसर्ट फॉर्मेट और बेड नाइफ पेयरिंग के साथ संगत हों।.
विनिर्देशों का दस्तावेजीकरण करते समय और पुर्जों को प्राप्त करते समय, ISO 6508‑1 रॉकवेल परीक्षण या इसके समकक्ष ASTM E18 जैसी स्वीकृत विधि से कठोरता को सत्यापित करें और बैच-लिंक्ड रिकॉर्ड रखें। औद्योगिक ब्लेडों में कठोरता के विकल्पों की पृष्ठभूमि के लिए, इसमें व्याख्यात्मक अवलोकन देखें रॉकवेल कठोरता परीक्षण (ISO 6508‑1) का संदर्भ देने वाले ISO प्रविष्टि पृष्ठ और एक व्यावहारिक औद्योगिक चाकू रॉकवेल कठोरता गाइड.
गैप और संरेखण नियंत्रण
इंडेक्सेबल हो या नहीं, कट की गुणवत्ता मैकेनिकल सेटअप पर निर्भर करती है:
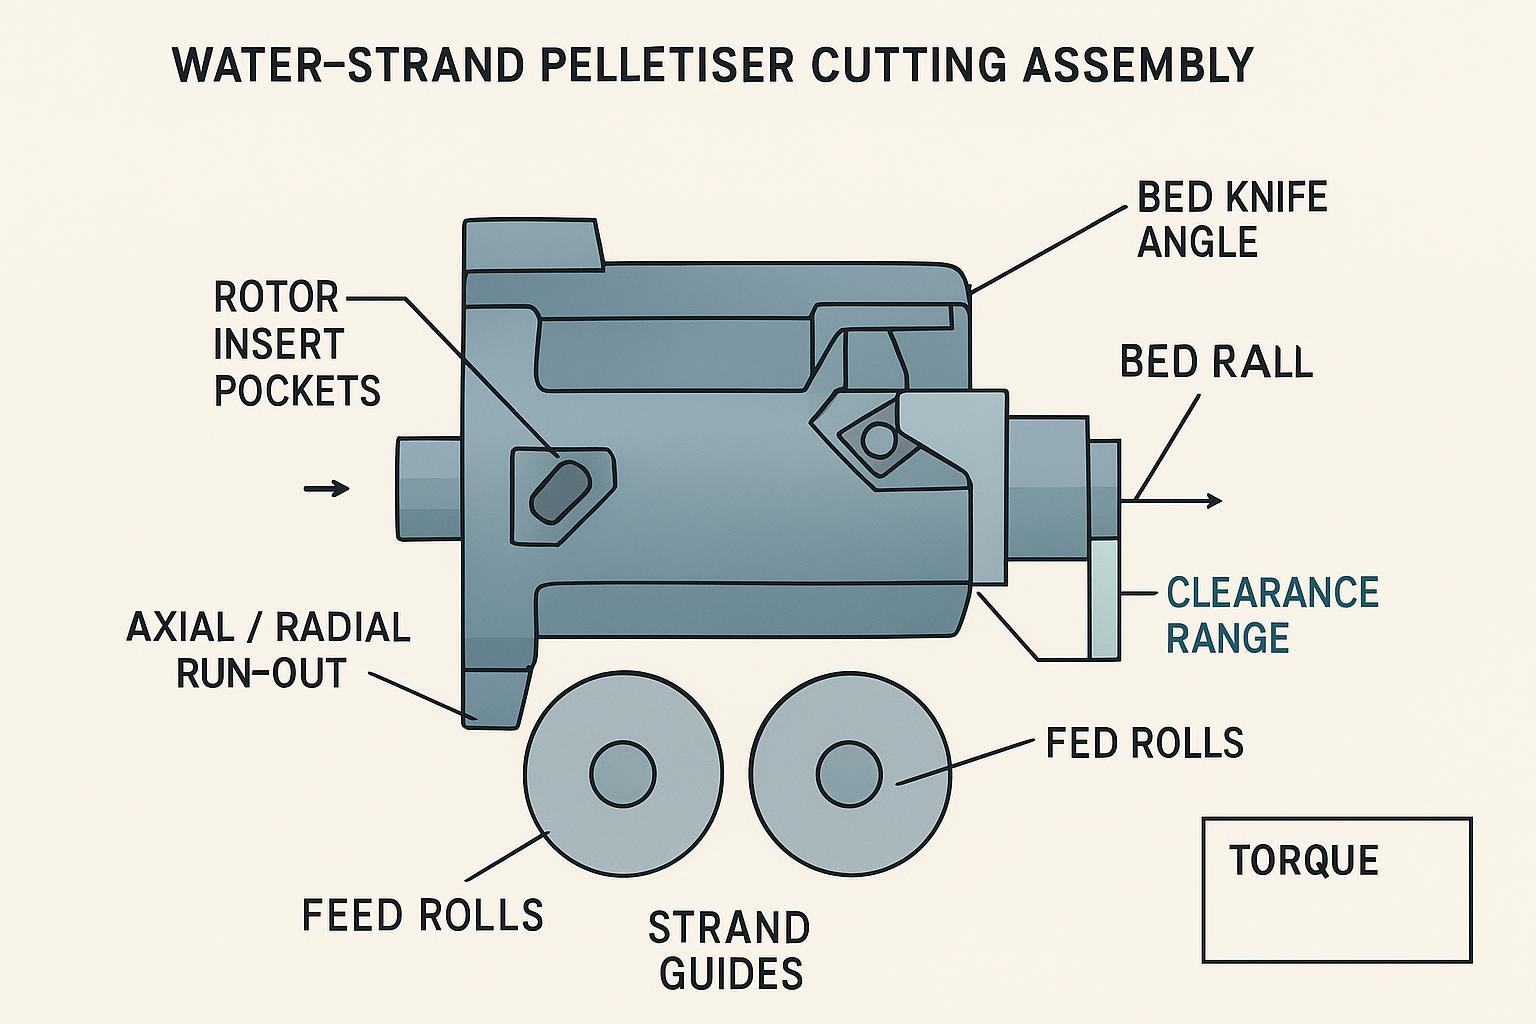
- विभिन्न कोणीय स्थितियों पर कटर-टू-बेड क्लीयरेंस को मापें; अक्षीय और रेडियल रन-आउट को लॉग करें।.
- इंसर्ट इंडेक्सिंग या प्रतिस्थापन के बाद, सेवा में वापस लाने से पहले रोटर संतुलन और स्वीकार्य रन-आउट को सत्यापित करें। अवधारणाओं और सहनशीलता को इसमें शामिल किया गया है रोटर संतुलन पर ISO 21940 श्रृंखला (शीर्षक और दायरा).
- स्ट्रैंड गाइड और फीड रोल को संरेखित रखें ताकि पार्श्व घर्षण से बचा जा सके जिससे बारीक कण और टेल्स उत्पन्न होते हैं। पर्याप्त शीतलन स्ट्रैंड्स को कड़ा करता है और व्यावहारिक क्लीयरेंस विंडो को बढ़ाता है।.
औद्योगिक ब्लेड और असेंबली पर व्यावहारिक निरीक्षण विधियों और सहनशीलता रिपोर्टिंग के लिए, इस पर एक उपयोगी अवलोकन उपलब्ध है निरीक्षण और सहनशीलता व्याख्याकर्ता.
Maintenance cost model
Inserted blade rotary cutter for water‑strand pelletizing changes the TCO shape because you renew edges without rotor extraction. The model has four stacks: Parts, Labour, Lost Production, and Scrap.
Parts and regrind avoided
A solid rotor’s cost pattern is dominated by periodic regrinds and eventual replacement. Inserted systems shift spend to insert sets and pocket upkeep while often reducing or deferring regrind frequency. Two levers drive the economics: edge renewal without rotor extraction cuts handling hours and eliminates regrind transport/queue time; and insert geometry with harder steels maintains edge integrity longer in abrasive duty when paired with the right bed knife hardness.
Labour and downtime
Citable OEM signals on analogous dry‑cut strand pelletisers show how design for access collapses minutes. For example, MAAG’s T200 series reports a reduction from around 30 minutes to approximately 2 minutes for specific disassembly tasks through tool‑less mechanisms, and PRIMO FC reports rotor replacement in no more than 30 minutes. Applied to PRIMO/PRIMOplus and SGS with inserted systems, a conservative planning range for an index or insert swap is 15–45 minutes, assuming defined scope, competent crew, safe isolation, and no seized fasteners.
Quality and waste
Quality losses show up as scrap and rework costs. Measure fines and dust as mass percentage using a recognised method such as ASTM D7486, and track pellet size dispersion as coefficient of variation. Stabilised clearances and fresh edges reduce tails and fines, often improving downstream feeding stability.
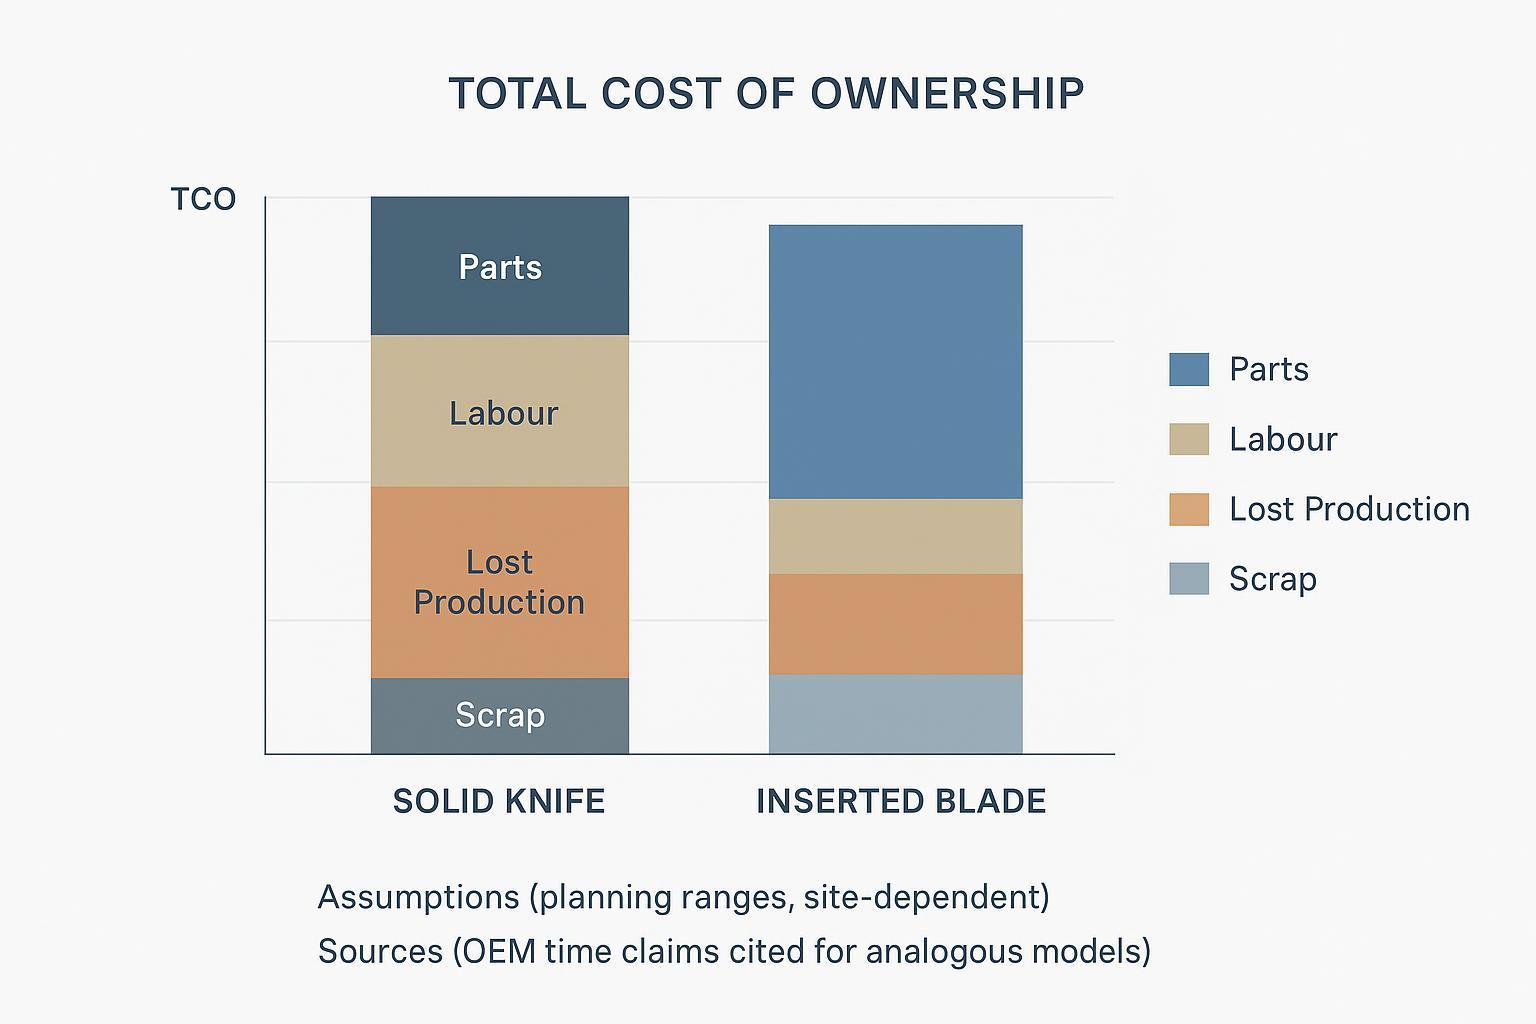
Assumptions note: The chart visualises planning ranges using typical UK labour rates, line‑specific lost‑production valuations, and conservative scrap penalties. Replace with your site data during validation.
Uptime and quality
Changeover time benchmarks
Treat time bands as planning tools, not promises. For indexable systems on PRIMO/PRIMOplus and SGS‑style machines, 15–45 minutes typically covers isolation, indexing or insert swap, torque verification, gap checks, a short run‑in and QC sampling. This aligns directionally with OEM claims on analogous models where tool‑less access compresses sub‑tasks—see MAAG’s T200 series and PRIMO FC time notes for context from the manufacturer pages cited above.
Pellet uniformity, fines, tails
Define and hold a common yardstick. Fines and dust: weigh before/after sieving per ASTM D7486 and report as wt%. Pellet uniformity: capture sample images or caliper data to compute pellet dimension CV; track median and IQR rather than cherry‑picking best runs. Acceptance in abrasive duty: target a sustained reduction in fines percentage versus baseline and a tighter pellet size CV after retrofit and SOP stabilisation.
Cooling and strand condition
Cooling dictates strand stiffness and cut behaviour. Ensure bath length and temperature bring strands below softening before the cut. Practical guidance on estimating bath length and preventing streamers is outlined in Plastics Technology articles such as bath length estimation for strand pelletising और tips to prevent streamers. Keep trough speed, spray patterns and guide geometry consistent to prevent lateral vibration.
Retrofit checklist
Interface and balance
Before committing to an inserted blade rotary cutter for water‑strand pelletizing on PRIMO/PRIMOplus or SGS‑style lines, verify mounting interface dimensions (shaft, hub, key, axial locating features) and axial stack‑up; rotor envelope (diameter, width), insert pocket geometry and clamp style clearance to guards; and balance grade targets and verification method post‑assembly per ISO 21940 balancing concepts.
Clearance, torque, SOP
Standardise a short, unambiguous SOP. Lockout‑tagout the drive and isolate utilities, then verify zero energy. Index or replace inserts, clean contact faces, apply the specified torque sequence, and record torque values. Set cutter‑to‑bed clearance uniformly, confirm axial/radial run‑out, and perform a brief no‑load rotation check before product runs. Re‑check fastener torque after the first warm cycle, then move to planned intervals.
Documentation and QA
Suppliers should provide batch‑traceable documentation at delivery: material test certificates, heat‑treatment certificates, Rockwell hardness results to ISO 6508‑1 or ASTM E18, and dimensional tolerance reports from an approved inspection method. Serialise rotors and, where practical, insert sets, and maintain regrind/index logs linked to batch IDs.
A neutral example of how a manufacturer frames this is available from मैक्सटोर धातु, which provides batch‑linked QA artefacts and educational resources. For assembling your receiving checklist, see a practical inspection and tolerance explainer and, for hardness background, the औद्योगिक चाकू रॉकवेल कठोरता गाइड. This is offered as context, not as a performance claim.
Trial and validation
KPIs and acceptance
Design a matched pre/post trial on the same product family and throughput. Define windows for maintenance hours per 1,000 tonnes (planned vs unplanned), changeover minutes per event and per 1,000 tonnes, fines percentage by mass and pellet size CV, scrap and restart losses (£/tonne), and any downstream feeder stability incidents. Use medians and IQR across multiple runs. If the inserted solution shows a statistically meaningful reduction in maintenance hours and fines with neutral or lower TCO, approve the change.
Starter spares and policies
For abrasive duty, hold at least one full set of inserts per active edge position plus a contingency reserve for two rapid swaps. Keep critical fasteners, clamps and a torque‑verified tool kit on the line. Define regrind policies for bed knives and any solid companions, and serialise components to track life by batch and station.
Risk controls and safety
Align with UK PUWER duties on work equipment: guard dangerous parts, isolate before maintenance, and ensure competence. See the regulator’s PUWER overview for scope and duties. Embed LOTO in every SOP, specify fastener property classes and torque targets, and verify balance/run‑out after any insert work before returning to production.
निष्कर्ष
Inserted/indexable cutters change the economics of water‑strand pelletising by removing rotor extractions from routine maintenance. With disciplined alignment and cooling practice, plants frequently see roughly half the maintenance effort, steadier pellet quality, and safer, shorter changeovers—outcomes you can verify through a simple, standards‑aligned trial.
Next steps: assemble a pilot plan on a single PRIMO/PRIMOplus or SGS line, define KPIs and data capture, run matched trials, and review supplier documentation against a receiving checklist covering MTCs, heat treatment, hardness and tolerances. For neutral QA artefacts and measurement explainers to shape your internal templates, the HSE PUWER guidance and the industrial blade रॉकवेल कठोरता गाइड are practical starting points.
Author and disclosure
लेखक: Tommy Tang, Senior Sales Engineer, Nanjing METAL Industrial.
अनुभव: 12 years in industrial blades and pelletising-related cutting applications.
प्रमाणपत्र: CSE, CME, Six Sigma Green Belt, PMP.
Disclosure and update note: This guide is intended for engineering planning and SOP design. Always follow your pelletiser OEM manual, site risk assessments, and UK legal duties (e.g., PUWER) before changing tooling or procedures. Standards and linked sources are periodically reviewed and may change as new revisions are published.

 English
 Spanish
 Italian
 French
 Portuguese
 Russian
 German
 Arabic
 Hindi
 Vietnamese
 Indonesian
 Japanese
 Korean