

Terakhir diperbarui: 2026-03-30
Catatan keselamatan & kepatuhan (UK): Artikel ini memberikan panduan praktik terbaik umum untuk penggantian pisau potong rotari. Artikel ini tidak menggantikan penilaian risiko lokasi Anda, dokumentasi OEM, atau keputusan rekayasa yang kompeten. Selalu verifikasi celah pelindung (guarding clearances), batas runout, dan sistem kerja yang aman di bawah PUWER sebelum mengoperasikan kembali peralatan.
Pernyataan: Artikel ini merujuk pada produk dan kapabilitas MAXTOR METAL. Penulis berafiliasi dengan Nanjing METAL Industrial.
Ruang lingkup & asumsi
- Panduan ini mencakup penggantian yang serupa (like-for-like) proyek penggantian pisau potong rotari di mana tujuannya adalah untuk memulihkan fungsi dan pengadaan yang dapat diulang (spesifikasi → verifikasi → dokumentasi).
- Memang benar bukan menyediakan penilaian keselamatan yang lengkap. Jika penggantian Anda mengubah celah pelindung, getaran/kebisingan, gaya pemotongan, parameter kontrol, atau menimbulkan bahaya baru, perlakukan hal tersebut sebagai modifikasi dan ikuti manajemen perubahan (management-of-change) serta tinjauan rekayasa kompeten di lokasi Anda.
- Setiap contoh “tipikal” dalam artikel ini adalah hanya untuk referensi. Tentukan kriteria penerimaan (misalnya, pengaturan/batas runout, metode uji kekerasan) dengan dokumentasi OEM Anda dan insinyur yang bertanggung jawab sebelum menyalakan kembali peralatan.
Lini produksi lama jarang sekali rusak sekaligus. Kerusakan terjadi satu per satu pada suku cadang habis pakai—hingga bagian yang tidak dapat Anda beli menjadi bagian yang menghentikan seluruh lini produksi.
Alasan umumnya dapat diprediksi:
- OEM tidak lagi mendukung mesin tersebut, atau nomor suku cadang telah dihentikan.
- “Suku cadang pengganti yang ”mirip" sebenarnya tidak cocok dengan kesesuaian (fit), penjepitan (clamp), atau geometri pemotongan.
- Biaya downtime terus meningkat karena pergantian suku cadang menjadi sering, lambat, dan lebih berisiko.
Jika Anda menjalankan lini produksi di mana waktu operasional (uptime) dan kualitas pelet terkait langsung dengan pisau potong rotari, penggantian mesin secara penuh sering kali merupakan cara paling mahal untuk menyelesaikan masalah suku cadang.
Jalur yang lebih aman adalah dengan mengkualifikasi penggantian pisau potong rotari kustom—yang dibuat sesuai dengan fungsional geometri dari pisau potong lama Anda, diverifikasi melalui proses first-article, dan didokumentasikan dengan cukup baik sehingga bagian pengadaan dan pemeliharaan dapat mengulang pesanan tanpa harus melakukan rekayasa ulang setiap saat.
Apa yang akan Anda dapatkan dari pendekatan ini:
- Jaminan kesesuaian (fit) melalui pengukuran berbasis datum dan pemetaan toleransi
- Kembali beroperasi lebih cepat dengan persetujuan first-article yang terkontrol
- Total biaya kepemilikan (TCO) yang lebih rendah dengan memperpanjang waktu pengoperasian dan mengurangi risiko pergantian
Poin Penting: Perlakukan pisau potong sebagai proyek suku cadang terkontrol (spesifikasi → verifikasi → dokumentasi), bukan pembelian darurat.
Esensi rekayasa balik (reverse engineering)
Penerimaan dan pengambilan data
Rekayasa balik bekerja paling baik ketika Anda memperlakukan bagian yang aus sebagai bukti, bukan sebagai cetak biru.
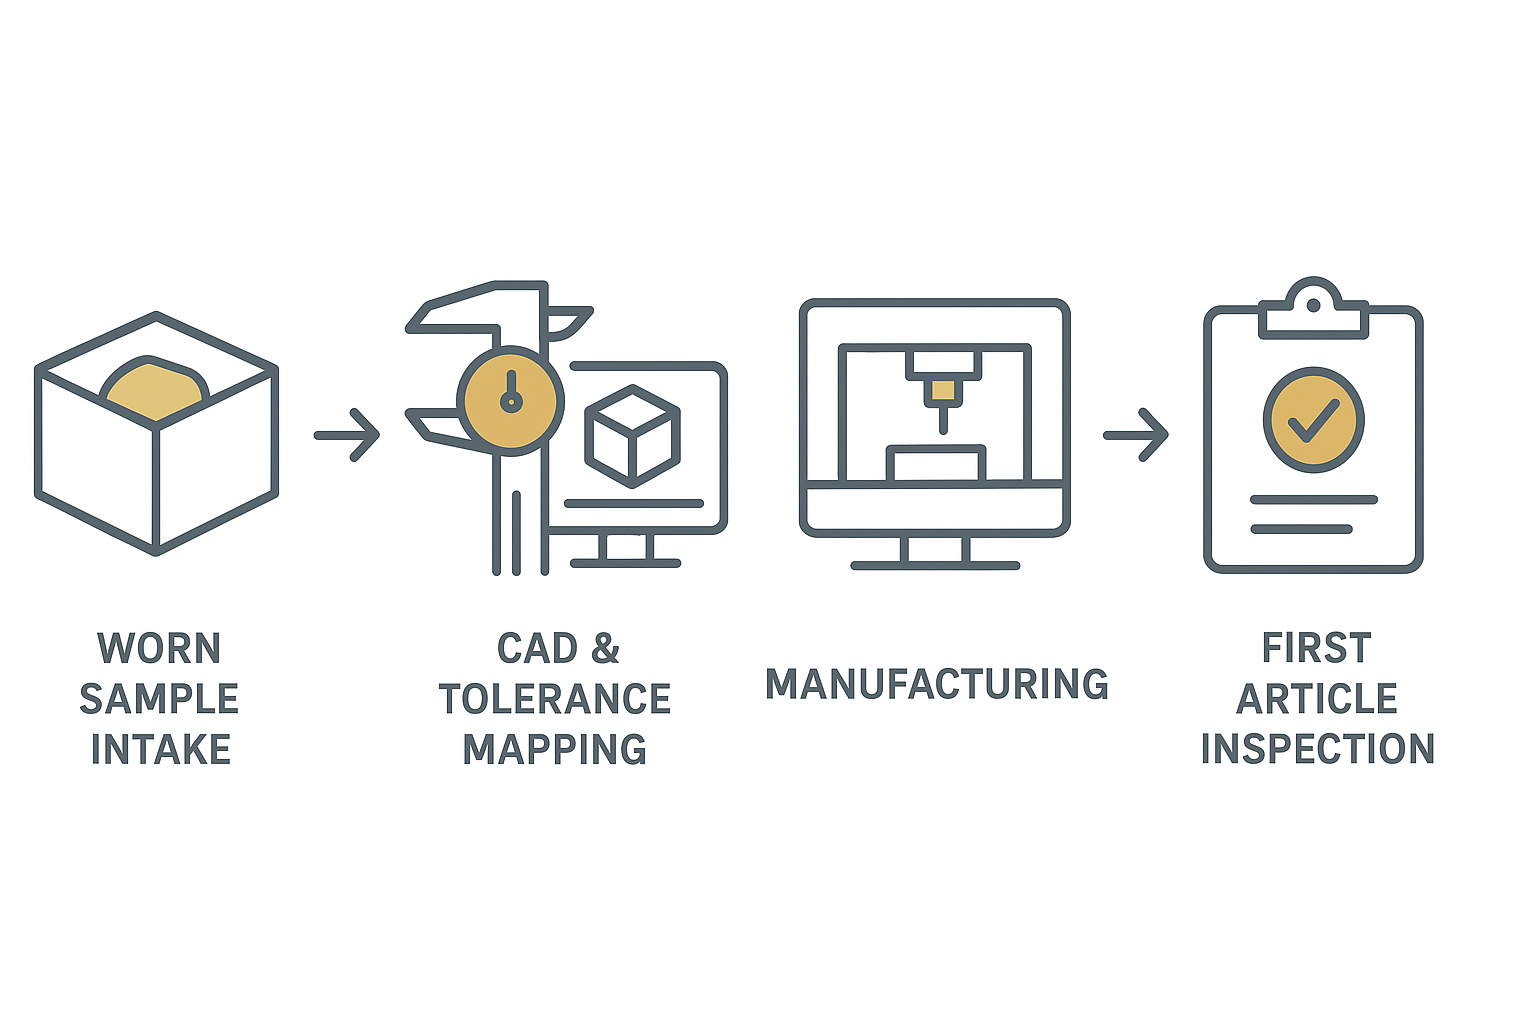
Mulailah dengan proses penerimaan yang mengurangi ambiguitas:
- Pahami konteks pengoperasian: material yang dipotong (virgin vs regrind, senyawa terisi), throughput tipikal, dan mode kegagalan yang Anda lihat (tumpul cepat, micro-chipping, bekas panas, burr).
- Foto dan beri label bagian tersebut sebelum dibersihkan (kedua sisi, permukaan pemasangan, tanda apa pun).
- Ukur referensi “non-aus” terlebih dahulu: lubang (bores), alur pasak (keyways), permukaan pemasangan, lingkaran baut—fitur yang menentukan posisi pada poros dan sering kali dapat lebih dipercaya daripada tepi pemotong.
Untuk pengambilan data, metode hibrida adalah hal yang umum:
- Dimensi dasar dengan jangka sorong/mikrometer
- Kesesuaian kritis dan geometri dengan CMM atau pemindaian 3D (terutama ketika pisau potong memiliki profil yang kompleks)
Tujuannya bukan untuk mengumpulkan “data sebanyak mungkin.” Tujuannya adalah untuk mengumpulkan enough data to define datums and control the features that affect fit, runout, and cutting performance—so your penggantian pisau potong rotari kustom behave predictably when installed.
Tolerance mapping and CAD
Once you have measurements, map them into a CAD model around a datum structure:
- Primary datum: typically a mounting face or bore that defines axial location
- Secondary datum: a feature that defines rotation or concentricity (bore, pilot, shaft interface)
- Tertiary datum: a keyway/bolt pattern that locks orientation
Then, assign tolerances based on how the cutter behaves in the machine:
- Fits that control concentricity and runout get the tightest attention.
- Cutting edges and relief angles are controlled to preserve function (cut quality) rather than copying wear.
- Features that don’t influence assembly or safety can be looser to keep cost sensible.
In metrology-focused reverse engineering guidance (for example, Verisurf’s reverse engineering best practices), the recurring theme is the same: define datums early and close the loop between measurement, CAD, and inspection—so you reduce “do-overs” and supplier interpretation drift over repeat orders.
If you want a formal language for this, the ISO GPS (Geometrical Product Specifications) framework is commonly referenced in manufacturing. For example, ISO 1101 defines the symbol language and rules for geometrical tolerancing (form, orientation, location, and run-out).
First-article approval
A replacement should not go straight from “CAD done” to “production batch.” A controlled first-article step is your risk firewall.
A practical first-article approval flow includes:
- First-article manufacturing to the mapped tolerances
- Inspection against the CAD drawing / agreed checkpoints
- A sign-off package (FAI) you can file and reuse
Kiat Profesional: Your FAI checkpoints should match how you’ll actually accept future batches—don’t measure “nice-to-have” dimensions that nobody will re-check under time pressure.
FAI checklist (copy/paste template)
- Part ID, revision, and quantity (first article vs pilot)
- Material grade and heat-treatment record
- Hardness test method and results (e.g., Rockwell per ISO 6508, Vickers per ISO 6507, or Brinell per ISO 6506)
- Datum features verified first (mounting face / bore / pilot / keyway)
- Bore size and fit-critical dimensions
- Runout/concentricity at the mounting interface (define measurement setup and acceptance criteria)
- Axial location features (spacers, shoulders) and stack-up notes
- Bolt circle / keyway orientation (if applicable)
- Edge geometry checkpoints (relief angles, edge condition, burr limits)
- Surface finish on mounting faces / contact areas
- Visual inspection (chips, cracks, coating defects) + packaging protection for edges
Tip: Replace each line with your site’s specific acceptance criteria and measurement method so future reorders can be received consistently.
For a widely used example of how organizations structure and document first-article inspection, see SAE AS9102 (Aerospace First Article Inspection Requirement). It is aerospace-focused, but the documentation logic (part accountability, material/process accountability, characteristic results) is a useful reference when building a clear FAI/FAIR pack for industrial spares.
Material, presisi, QA
Steel, carbide, coatings
Material choices for rotary cutters are usually a trade between ketahanan aus dan kekerasan.
- Tool steels (e.g., D2/SKD-11 class) are common when you need a balanced option with predictable heat treatment.
- HSS can improve toughness where intermittent loading or impact is a concern.
- Carbide (tipped or solid) is often used when abrasion dominates (e.g., glass-filled compounds), but brittleness has to be managed through geometry and handling.
Coatings can be a second lever—particularly when you’re fighting friction and abrasive wear. Material selection resources for granulator blades commonly highlight matching the steel/carbide route to the plastic and filler content, rather than defaulting to one “best” material.
Specifying custom rotary cutter replacements
A spec that prevents costly back-and-forth typically includes:
- Cutter type and function (rotary knife, pelletizer cutter, granulator rotor knife)
- Quantity and whether you’re qualifying a single first article or a small pilot batch
- A drawing (preferred) or a controlled reverse-engineering scope (datums + checkpoints)
- Surface finish and edge condition requirements
- Heat treatment expectations (hardness range and where it matters)
If you’re sourcing globally, it also helps to specify what documents are non-negotiable at the quote stage (not after the parts are in transit).
Precision targets and traceability
For legacy machines, precision is less about “tight everywhere” and more about “tight where it prevents downtime.”
Typical high-impact controls include:
- Runout / concentricity control at the mounting interface (define the measurement setup and acceptance criteria with your engineer/OEM; values are equipment-specific)
- Axial positioning so the cutter tracks correctly relative to the bed knife/anvil (verify guarding clearances and safe operation before restart)
- Edge geometry consistency to avoid pellet tails, fines, or quality drift
This is also the point where supplier capability matters—especially for plants that need repeatability over multiple reorder cycles.
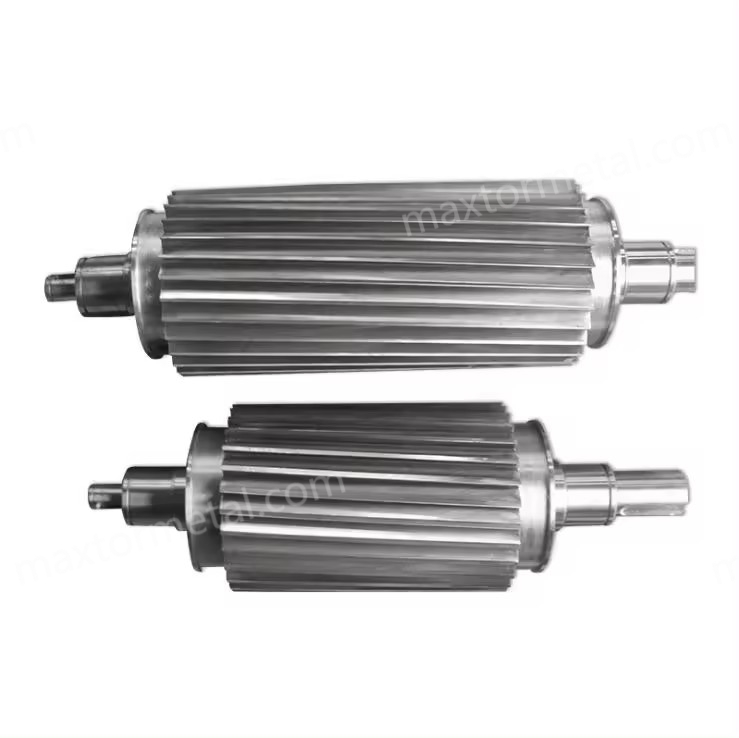
Misalnya, LOGAM MAXTOR manufactures custom industrial blades (including plastic granulator rotary knives dan plastic pelletizer knives) and is set up for build-from-drawing/sample workflows. In practice, the useful question to ask any supplier is not “can you copy this part?” but:
- Can you define and agree the datums that control fit?
- Can you provide an inspection pack aligned to those checkpoints?
- Can you maintain traceability (material and process records) batch-to-batch?
Answering those three questions up front is how you avoid tolerance drift and “mystery reworks” on the shop floor.
⚠️ Peringatan: If a quote comes back with no mention of inspection/acceptance criteria, you’re likely buying interpretation—not a controlled spare part.
Contoh hasil (dari sumber yang dipublikasikan)
Because results depend heavily on polymer, throughput, cutter design, and maintenance practice, use the examples below as illustrative only, not guaranteed outcomes.
Mini-case A: Fewer changeovers and lower blade-related cost
- Masalah: Frequent blade changes and rising downtime/labour cost.
- Action (reported): Switching to a better-fit/customized blade approach and tightening maintenance/sharpening practice.
- Outcome (reported): Blade changes reduced from 12 to 3 per month (reported as ~65% less downtime) and monthly blade-related cost lowered from >$800 to ~$450 (including labour).
- When it applies: Plants where changeovers are frequent and knives are treated as consumables without a controlled acceptance/maintenance routine.
Mini-case B: Longer life via process/material treatment (industry example)
- Masalah: Short knife life and inconsistent performance in pelletizing.
- Action (reported): Evaluating process/material treatment improvements (e.g., cryogenic processing trials) and verifying against a defined acceptance method.
- Outcome (reported): Extended service life and cost savings were reported in a pelletizer blade trial case study; results vary by polymer, throughput, and knife geometry.
- When it applies: High-throughput lines where small improvements in knife life compound into measurable downtime and scrap reduction.
Sources (examples):
- Granulator maintenance/sharpening article with the changeover/cost example: https://maxtormetal.com/maintain-sharpen-granulating-blade-optimal-performance-2025/
- Pelletizer blade cryogenic processing case study: https://ctpcryogenics.com/services/industrial/case-study-rubbermaid/
If you want, we can replace these with your own internal examples later (even anonymized ranges) to make the outcomes more directly relevant to your equipment.
Kepatuhan UK, impor, TCO
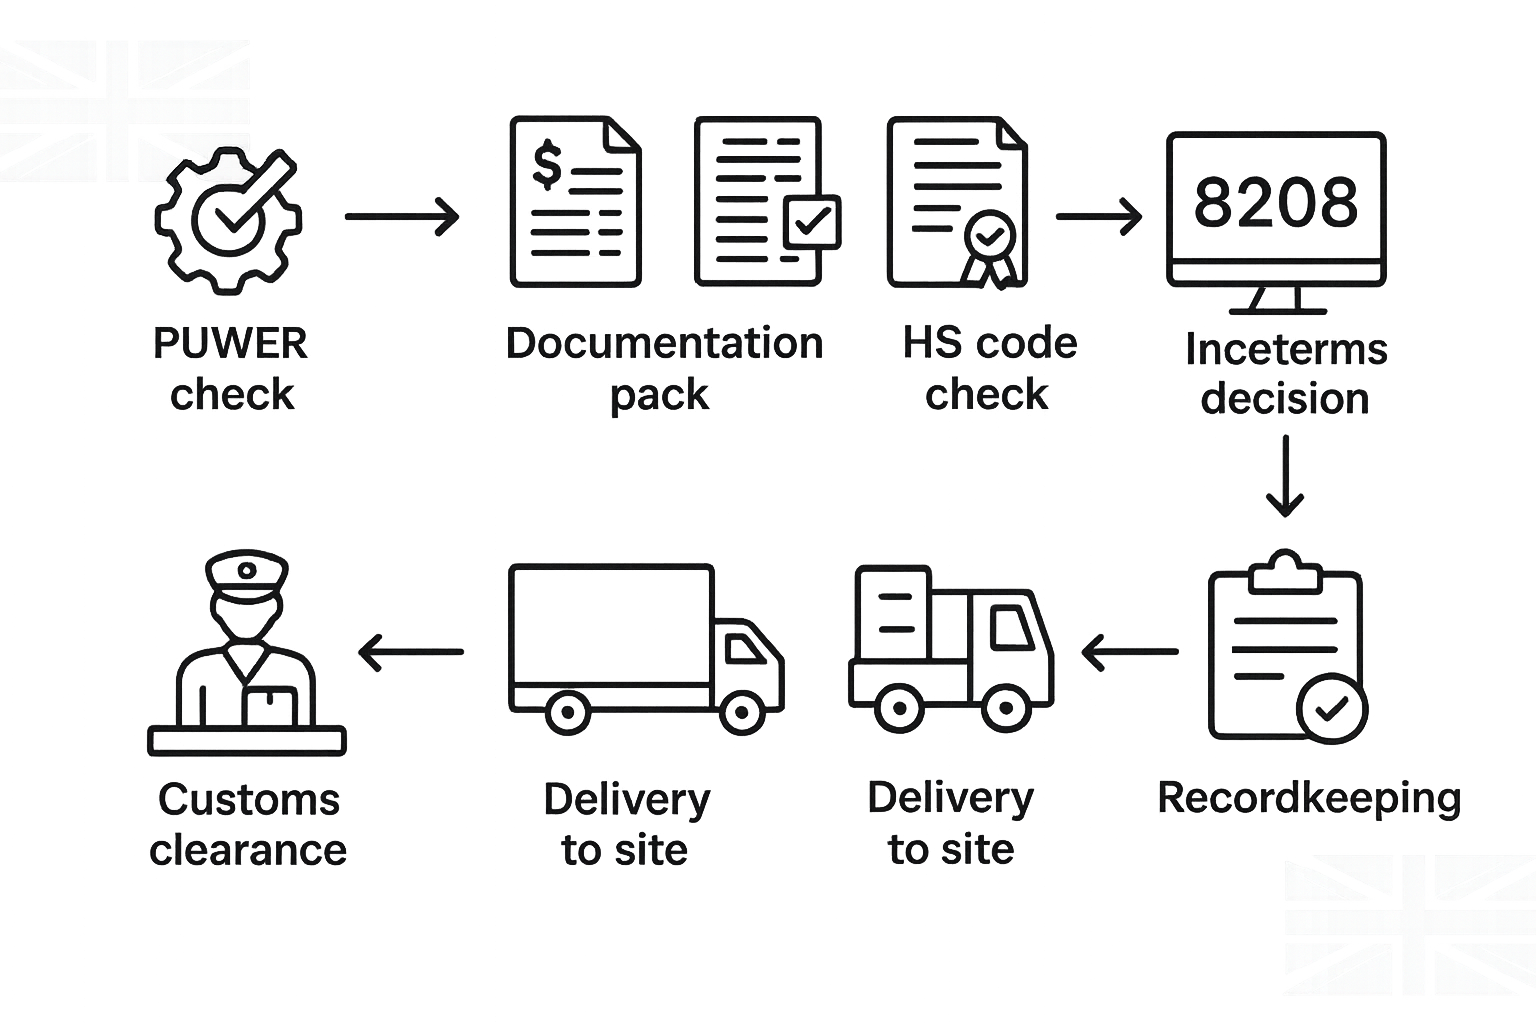
PUWER, UKCA/CE scope
For UK operators, two practical lenses matter:
- Safe use of work equipment (PUWER)
HSE’s overview of PUWER (Provision and Use of Work Equipment Regulations 1998) emphasises that equipment must be suitable for use, maintained, inspected where needed, and supported by appropriate information/instructions and training.
A rotary cutter replacement affects exactly those points—because it can change guarding clearances, cutting forces, vibration, and the operator’s safe system of work.
- When modifications become “substantial”
If the change is like-for-like (same function, no new hazards), you’re typically in a maintenance/refurbishment space. If the change introduces new hazards or materially changes how the machine operates, HSE’s guidance on refurbished and modified machinery explains why the modifier may take on “manufacturer-like” responsibilities.
For context on supply-side obligations, the UK government guidance on the Supply of Machinery (Safety) Regulations 2008 (Great Britain) is the right place to sanity-check whether your change stays a spare-part replacement—or edges into a broader conformity assessment question.
Docs, HS codes, Incoterms
For importing cutters into the UK, smooth procurement is mostly about eliminating paperwork gaps.
A practical documentation pack usually includes:
- Commercial invoice and packing list
- Proof of origin (acceptable formats are explained on GOV.UK’s guidance for Get proof of origin for your goods)
- Material and inspection documents you need for acceptance (e.g., hardness, key dimensions)
On classification, industrial knives and cutter blades often sit under HS heading 8208—confirm the exact commodity code for your specific cutter description using the GOV.UK Trade Tariff tool.
Incoterms decide who does what:
- DDP: supplier typically manages import clearance and delivery duties (lower admin load for the buyer, but verify what’s included).
- DAP: buyer handles import clearance and pays duties/VAT (more control, more responsibility).
If your team has been burned by delays before, align Incoterms with who will provide each document—and who is accountable if customs asks questions.
Life, downtime, payback
TCO is rarely dominated by the cutter’s unit price.
The big levers are:
- Biaya waktu henti per changeover (lost throughput, labour, restart waste)
- Quality cost (fines, tails, off-spec pellets, downstream feeding issues)
- Reorder risk (a replacement that doesn’t fit creates a second downtime event)
A simple way to quantify payback is:
- Estimate how many changeovers you can avoid per month if the replacement holds edge longer.
- Add the cost of one “bad fit” event as a risk cost (even if it’s low probability).
- Compare that against the delta between a standard blade and a verified, documented custom replacement.
Kesimpulan
Custom rotary cutter replacements are a practical way to extend the life of legacy machines—jika you treat them as a controlled engineering and procurement process.
That process is straightforward:
- Specify the cutter around datums and functional geometry, not around worn edges
- Qualify the part with mapped tolerances and a first-article inspection pack
- Import with confidence by aligning documentation, HS code checks, and Incoterms responsibilities
Langkah selanjutnya:
- Share the worn sample and/or drawings
- Agree the critical tolerances (fits, runout, axial location, edge geometry)
- Request an FAI pack that matches how your site will accept repeat orders
Referensi
- HSE: PUWER (Provision and Use of Work Equipment Regulations 1998): https://www.hse.gov.uk/work-equipment-machinery/puwer.htm
- HSE: Refurbished and modified machinery: https://www.hse.gov.uk/work-equipment-machinery/refurbished-modified-machinery.htm
- GOV.UK: Supply of Machinery (Safety) Regulations 2008 (Great Britain): https://www.gov.uk/government/publications/supply-of-machinery-safety-regulations-2008/supply-of-machinery-safety-regulations-2008-great-britain
- GOV.UK: Get proof of origin for your goods: https://www.gov.uk/guidance/get-proof-of-origin-for-your-goods
- GOV.UK: Trade Tariff tool: https://www.gov.uk/trade-tariff
- ISO: ISO 1101 (Geometrical tolerancing): https://www.iso.org/standard/66777.html
- SAE: AS9102 (Aerospace First Article Inspection Requirement): https://www.sae.org/standards/as9102-aerospace-first-article-inspection-requirement
- IAQG: 9102 First Article Inspection Requirement overview: https://iaqg.org/standard/9102-first-article-inspection-requirement/
Pengarang
Written by Tommy Tang, Senior Sales Engineer at Industri Logam Nanjing (12 years). Certifications: CSE, CME, Sabuk Hijau Six Sigma, PMP.

 English
 Spanish
 Italian
 French
 Portuguese
 Russian
 German
 Arabic
 Hindi
 Vietnamese
 Indonesian
 Japanese
 Korean