

Zuletzt aktualisiert: 2026-03-30
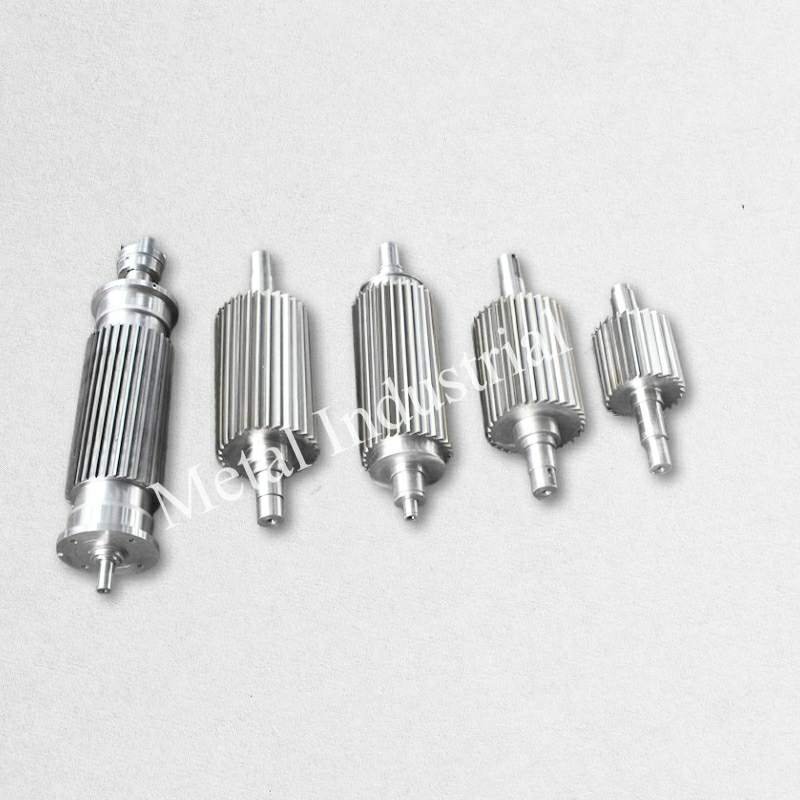
Sicherheits- und Konformitätshinweis (UK): Dieser Artikel bietet allgemeine Best-Practice-Richtlinien für den Austausch von Rotationsmessern. Er ersetzt nicht die Risikobeurteilung vor Ort, die OEM-Dokumentation oder das fachmännische Urteil eines Ingenieurs. Überprüfen Sie vor der Wiederinbetriebnahme von Geräten stets die Schutzabstände, Rundlaufgrenzen und sicheren Arbeitssysteme gemäß PUWER.
Hinweis: Dieser Artikel bezieht sich auf Produkte und Funktionen von MAXTOR METAL. Der Autor ist mit Nanjing METAL Industrial verbunden.
Umfang & Annahmen
- Dieser Leitfaden umfasst eins-zu-eins Projekte zum Austausch von Rotationsmessern, bei denen das Ziel darin besteht, die Funktion und eine wiederholbare Beschaffung wiederherzustellen (Spezifizieren → Verifizieren → Dokumentieren).
- Er stellt nicht keine vollständige Sicherheitsbewertung dar. Wenn Ihr Austausch Schutzabstände, Vibrationen/Geräusche, Schnittkräfte oder Steuerungsparameter verändert oder neue Gefahren mit sich bringt, behandeln Sie dies als Modifikation und befolgen Sie das Änderungsmanagement (Management of Change) Ihres Standorts sowie die Prüfung durch einen qualifizierten Ingenieur.
- Alle “typischen” Beispiele in diesem Artikel dienen nur als Referenz. Definieren Sie Abnahmekriterien (z. B. Rundlaufeinstellung/-grenzen, Härteprüfverfahren) anhand Ihrer OEM-Dokumentation und mit dem zuständigen Ingenieur, bevor Sie die Anlage wieder in Betrieb nehmen.
Ältere Produktionslinien fallen selten auf einmal aus. Sie fallen Verschleißteil für Verschleißteil aus – bis das Teil, das Sie nicht kaufen können, zu dem Teil wird, das die gesamte Linie stilllegt.
Die üblichen Gründe sind vorhersehbar:
- Der OEM unterstützt die Maschine nicht mehr oder die Teilenummer wurde eingestellt.
- “Nahezu passende” Ersatzteile entsprechen oft nicht der tatsächlichen Passung, Klemmung oder Schneidgeometrie.
- Die Ausfallkosten steigen weiter, da Werkzeugwechsel häufiger, langsamer und riskanter werden.
Wenn Sie eine Linie betreiben, bei der Betriebszeit und Granulatqualität direkt von einem Rotationsmesser abhängen, ist ein kompletter Maschinenaustausch oft der teuerste Weg, ein Ersatzteilproblem zu lösen.
Ein sicherer Weg ist die Qualifizierung maßgeschneiderter Rotationsmesser-Ersatzteile– gefertigt nach der funktionellen Geometrie Ihres bestehenden Messers, verifiziert durch ein Erstmusterprüfverfahren und so gut dokumentiert, dass Einkauf und Instandhaltung die Bestellung wiederholen können, ohne sie jedes Mal neu konstruieren zu müssen.
Was Sie mit diesem Ansatz erreichen:
- Passgenauigkeit durch bezugsbasierte Messung und Toleranzzuordnung
- Schnellere Wiederinbetriebnahme durch eine kontrollierte Erstmusterfreigabe
- Niedrigere Gesamtbetriebskosten (TCO) durch längere Laufzeiten und geringeres Wechselrisiko
Wichtigste Erkenntnis: Behandeln Sie das Messer als kontrolliertes Ersatzteilprojekt (Spezifizieren → Verifizieren → Dokumentieren) und nicht als Notkauf.
Grundlagen des Reverse Engineering
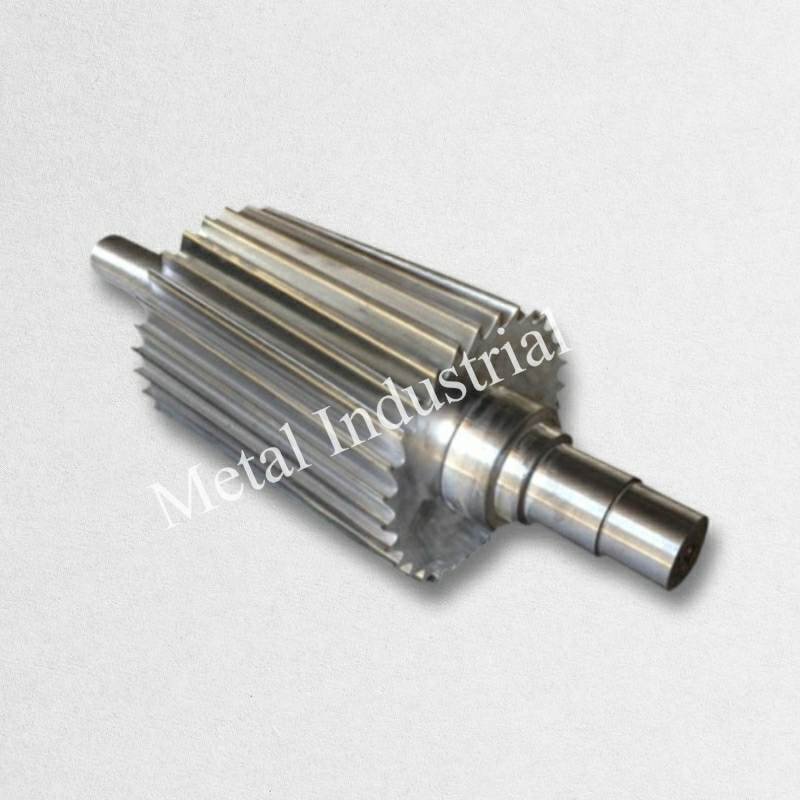
Erfassung und Datenerhebung
Reverse Engineering funktioniert am besten, wenn Sie das verschlissene Teil als Beweismittel, und nicht als Blaupause betrachten.
Beginnen Sie mit einer Erfassung, die Unklarheiten ausschließt:
- Erfassen Sie den Betriebskontext: zu schneidendes Material (Neuware vs. Mahlgut, gefüllte Compounds), typischer Durchsatz und das auftretende Verschleißbild (schnelles Abstumpfen, Mikroausbrüche, Hitzespuren, Gratbildung).
- Fotografieren und kennzeichnen Sie das Teil vor der Reinigung (beide Seiten, Montageflächen, eventuelle Markierungen).
- Messen Sie zuerst die verschleißfreien Referenzen: Bohrungen, Passfedernuten, Montageflächen, Lochkreise – Merkmale, die die Position auf der Welle definieren und denen oft mehr vertraut werden kann als der Schneidkante.
Für die Datenerfassung ist eine Hybridmethode üblich:
- Grundmaße mit Messschiebern/Mikrometern
- Kritische Passungen und Geometrien mittels KMG (Koordinatenmessgerät) oder 3D-Scanning (insbesondere bei komplexen Messerprofilen)
The goal isn’t to collect “as much data as possible.” It’s to collect enough data to define datums and control the features that affect fit, runout, and cutting performance—so your maßgeschneiderter Rotationsmesser-Ersatzteile behave predictably when installed.
Tolerance mapping and CAD
Once you have measurements, map them into a CAD model around a datum structure:
- Primary datum: typically a mounting face or bore that defines axial location
- Secondary datum: a feature that defines rotation or concentricity (bore, pilot, shaft interface)
- Tertiary datum: a keyway/bolt pattern that locks orientation
Then, assign tolerances based on how the cutter behaves in the machine:
- Fits that control concentricity and runout get the tightest attention.
- Cutting edges and relief angles are controlled to preserve function (cut quality) rather than copying wear.
- Features that don’t influence assembly or safety can be looser to keep cost sensible.
In metrology-focused reverse engineering guidance (for example, Verisurf’s reverse engineering best practices), the recurring theme is the same: define datums early and close the loop between measurement, CAD, and inspection—so you reduce “do-overs” and supplier interpretation drift over repeat orders.
If you want a formal language for this, the ISO GPS (Geometrical Product Specifications) framework is commonly referenced in manufacturing. For example, ISO 1101 defines the symbol language and rules for geometrical tolerancing (form, orientation, location, and run-out).
First-article approval
A replacement should not go straight from “CAD done” to “production batch.” A controlled first-article step is your risk firewall.
A practical first-article approval flow includes:
- First-article manufacturing to the mapped tolerances
- Inspection against the CAD drawing / agreed checkpoints
- A sign-off package (FAI) you can file and reuse
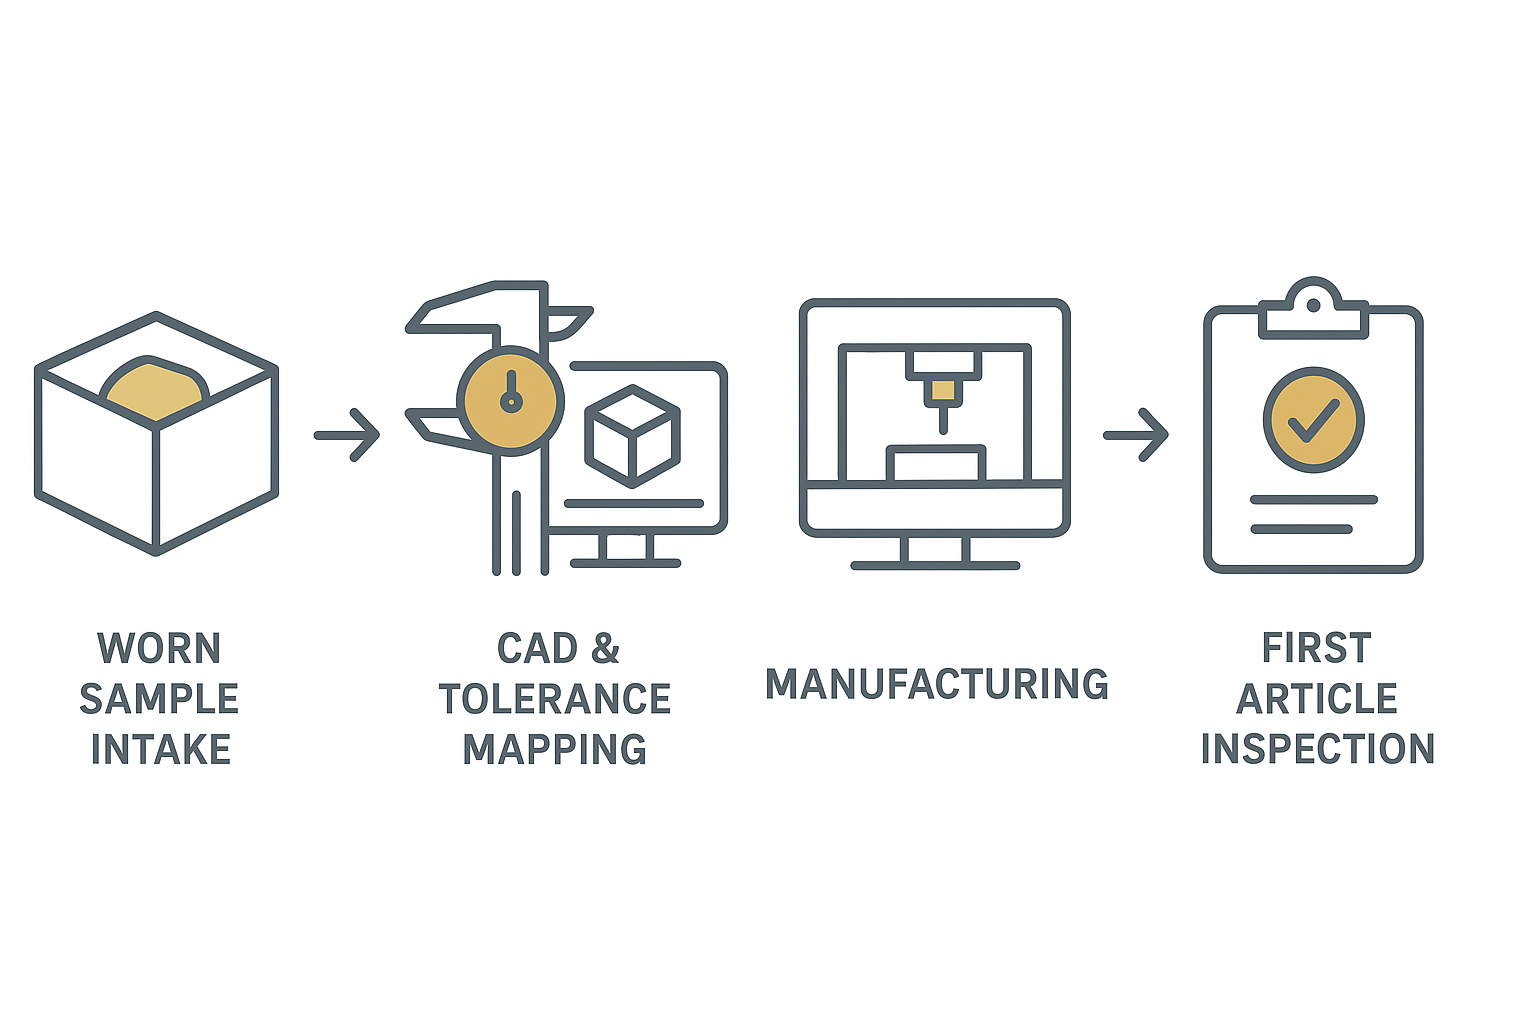
Profi-Tipp: Your FAI checkpoints should match how you’ll actually accept future batches—don’t measure “nice-to-have” dimensions that nobody will re-check under time pressure.
FAI checklist (copy/paste template)
- Part ID, revision, and quantity (first article vs pilot)
- Material grade and heat-treatment record
- Hardness test method and results (e.g., Rockwell per ISO 6508, Vickers per ISO 6507, or Brinell per ISO 6506)
- Datum features verified first (mounting face / bore / pilot / keyway)
- Bore size and fit-critical dimensions
- Runout/concentricity at the mounting interface (define measurement setup and acceptance criteria)
- Axial location features (spacers, shoulders) and stack-up notes
- Bolt circle / keyway orientation (if applicable)
- Edge geometry checkpoints (relief angles, edge condition, burr limits)
- Surface finish on mounting faces / contact areas
- Visual inspection (chips, cracks, coating defects) + packaging protection for edges
Tip: Replace each line with your site’s specific acceptance criteria and measurement method so future reorders can be received consistently.
For a widely used example of how organizations structure and document first-article inspection, see SAE AS9102 (Aerospace First Article Inspection Requirement). It is aerospace-focused, but the documentation logic (part accountability, material/process accountability, characteristic results) is a useful reference when building a clear FAI/FAIR pack for industrial spares.
Werkstoffe, Präzision, Qualitätssicherung
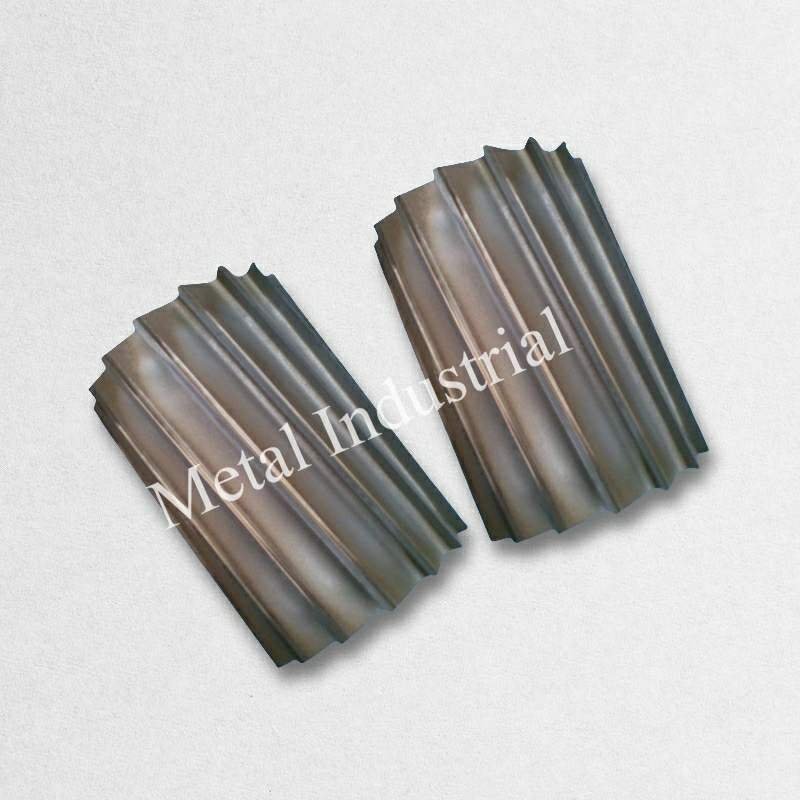
Steel, carbide, coatings
Material choices for rotary cutters are usually a trade between Verschleißfestigkeit und Zähigkeit.
- Tool steels (e.g., D2/SKD-11 class) are common when you need a balanced option with predictable heat treatment.
- HSS can improve toughness where intermittent loading or impact is a concern.
- Carbide (tipped or solid) is often used when abrasion dominates (e.g., glass-filled compounds), but brittleness has to be managed through geometry and handling.
Coatings can be a second lever—particularly when you’re fighting friction and abrasive wear. Material selection resources for granulator blades commonly highlight matching the steel/carbide route to the plastic and filler content, rather than defaulting to one “best” material.
Specifying custom rotary cutter replacements
A spec that prevents costly back-and-forth typically includes:
- Cutter type and function (rotary knife, pelletizer cutter, granulator rotor knife)
- Quantity and whether you’re qualifying a single first article or a small pilot batch
- A drawing (preferred) or a controlled reverse-engineering scope (datums + checkpoints)
- Surface finish and edge condition requirements
- Heat treatment expectations (hardness range and where it matters)
If you’re sourcing globally, it also helps to specify what documents are non-negotiable at the quote stage (not after the parts are in transit).
Precision targets and traceability
For legacy machines, precision is less about “tight everywhere” and more about “tight where it prevents downtime.”
Typical high-impact controls include:
- Runout / concentricity control at the mounting interface (define the measurement setup and acceptance criteria with your engineer/OEM; values are equipment-specific)
- Axial positioning so the cutter tracks correctly relative to the bed knife/anvil (verify guarding clearances and safe operation before restart)
- Edge geometry consistency to avoid pellet tails, fines, or quality drift
This is also the point where supplier capability matters—especially for plants that need repeatability over multiple reorder cycles.
Zum Beispiel, MAXTOR METAL manufactures custom industrial blades (including plastic granulator rotary knives und plastic pelletizer knives) and is set up for build-from-drawing/sample workflows. In practice, the useful question to ask any supplier is not “can you copy this part?” but:
- Can you define and agree the datums that control fit?
- Can you provide an inspection pack aligned to those checkpoints?
- Can you maintain traceability (material and process records) batch-to-batch?
Answering those three questions up front is how you avoid tolerance drift and “mystery reworks” on the shop floor.
⚠️ Warnung: If a quote comes back with no mention of inspection/acceptance criteria, you’re likely buying interpretation—not a controlled spare part.
Beispielhafte Ergebnisse (aus veröffentlichten Quellen)
Because results depend heavily on polymer, throughput, cutter design, and maintenance practice, use the examples below as illustrative only, not guaranteed outcomes.
Mini-case A: Fewer changeovers and lower blade-related cost
- Problem: Frequent blade changes and rising downtime/labour cost.
- Action (reported): Switching to a better-fit/customized blade approach and tightening maintenance/sharpening practice.
- Outcome (reported): Blade changes reduced from 12 to 3 per month (reported as ~65% less downtime) and monthly blade-related cost lowered from >$800 to ~$450 (including labour).
- When it applies: Plants where changeovers are frequent and knives are treated as consumables without a controlled acceptance/maintenance routine.
Mini-case B: Longer life via process/material treatment (industry example)
- Problem: Short knife life and inconsistent performance in pelletizing.
- Action (reported): Evaluating process/material treatment improvements (e.g., cryogenic processing trials) and verifying against a defined acceptance method.
- Outcome (reported): Extended service life and cost savings were reported in a pelletizer blade trial case study; results vary by polymer, throughput, and knife geometry.
- When it applies: High-throughput lines where small improvements in knife life compound into measurable downtime and scrap reduction.
Sources (examples):
- Granulator maintenance/sharpening article with the changeover/cost example: https://maxtormetal.com/maintain-sharpen-granulating-blade-optimal-performance-2025/
- Pelletizer blade cryogenic processing case study: https://ctpcryogenics.com/services/industrial/case-study-rubbermaid/
If you want, we can replace these with your own internal examples later (even anonymized ranges) to make the outcomes more directly relevant to your equipment.
UK-Konformität, Import, TCO
PUWER, UKCA/CE scope
For UK operators, two practical lenses matter:
- Safe use of work equipment (PUWER)
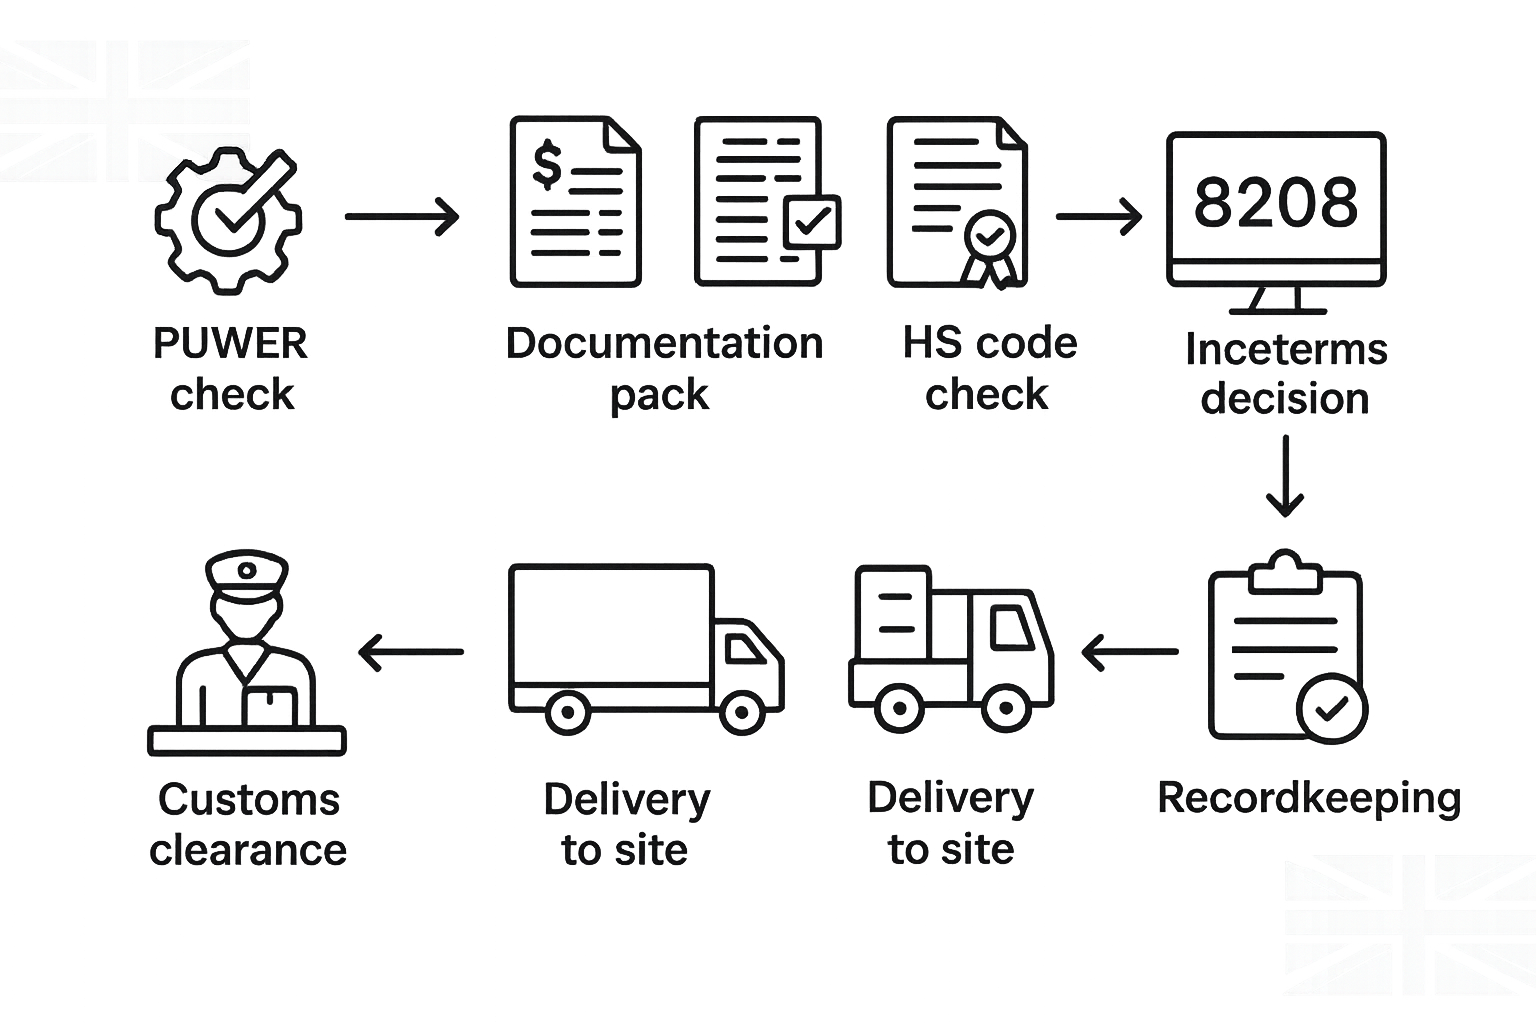
HSE’s overview of PUWER (Provision and Use of Work Equipment Regulations 1998) emphasises that equipment must be suitable for use, maintained, inspected where needed, and supported by appropriate information/instructions and training.
A rotary cutter replacement affects exactly those points—because it can change guarding clearances, cutting forces, vibration, and the operator’s safe system of work.
- When modifications become “substantial”
If the change is like-for-like (same function, no new hazards), you’re typically in a maintenance/refurbishment space. If the change introduces new hazards or materially changes how the machine operates, HSE’s guidance on refurbished and modified machinery explains why the modifier may take on “manufacturer-like” responsibilities.
For context on supply-side obligations, the UK government guidance on the Supply of Machinery (Safety) Regulations 2008 (Great Britain) is the right place to sanity-check whether your change stays a spare-part replacement—or edges into a broader conformity assessment question.
Docs, HS codes, Incoterms
For importing cutters into the UK, smooth procurement is mostly about eliminating paperwork gaps.
A practical documentation pack usually includes:
- Commercial invoice and packing list
- Proof of origin (acceptable formats are explained on GOV.UK’s guidance for Get proof of origin for your goods)
- Material and inspection documents you need for acceptance (e.g., hardness, key dimensions)
On classification, industrial knives and cutter blades often sit under HS heading 8208—confirm the exact commodity code for your specific cutter description using the GOV.UK Trade Tariff tool.
Incoterms decide who does what:
- DDP: supplier typically manages import clearance and delivery duties (lower admin load for the buyer, but verify what’s included).
- DAP: buyer handles import clearance and pays duties/VAT (more control, more responsibility).
If your team has been burned by delays before, align Incoterms with who will provide each document—and who is accountable if customs asks questions.
Life, downtime, payback
TCO is rarely dominated by the cutter’s unit price.
The big levers are:
- Downtime cost per changeover (lost throughput, labour, restart waste)
- Quality cost (fines, tails, off-spec pellets, downstream feeding issues)
- Reorder risk (a replacement that doesn’t fit creates a second downtime event)
A simple way to quantify payback is:
- Estimate how many changeovers you can avoid per month if the replacement holds edge longer.
- Add the cost of one “bad fit” event as a risk cost (even if it’s low probability).
- Compare that against the delta between a standard blade and a verified, documented custom replacement.
Fazit
Custom rotary cutter replacements are a practical way to extend the life of legacy machines—Wenn you treat them as a controlled engineering and procurement process.
That process is straightforward:
- Specify the cutter around datums and functional geometry, not around worn edges
- Qualify the part with mapped tolerances and a first-article inspection pack
- Import with confidence by aligning documentation, HS code checks, and Incoterms responsibilities
Next steps:
- Share the worn sample and/or drawings
- Agree the critical tolerances (fits, runout, axial location, edge geometry)
- Request an FAI pack that matches how your site will accept repeat orders
Literaturhinweise
- HSE: PUWER (Provision and Use of Work Equipment Regulations 1998): https://www.hse.gov.uk/work-equipment-machinery/puwer.htm
- HSE: Refurbished and modified machinery: https://www.hse.gov.uk/work-equipment-machinery/refurbished-modified-machinery.htm
- GOV.UK: Supply of Machinery (Safety) Regulations 2008 (Great Britain): https://www.gov.uk/government/publications/supply-of-machinery-safety-regulations-2008/supply-of-machinery-safety-regulations-2008-great-britain
- GOV.UK: Get proof of origin for your goods: https://www.gov.uk/guidance/get-proof-of-origin-for-your-goods
- GOV.UK: Trade Tariff tool: https://www.gov.uk/trade-tariff
- ISO: ISO 1101 (Geometrical tolerancing): https://www.iso.org/standard/66777.html
- SAE: AS9102 (Aerospace First Article Inspection Requirement): https://www.sae.org/standards/as9102-aerospace-first-article-inspection-requirement
- IAQG: 9102 First Article Inspection Requirement overview: https://iaqg.org/standard/9102-first-article-inspection-requirement/
Autor
Written by Tommy Tang, Senior Sales Engineer at Nanjing METAL Industrie (12 years). Certifications: CSE, CME, Six Sigma Green Belt, PMP.

 English
 Spanish
 Italian
 French
 Portuguese
 Russian
 German
 Arabic
 Hindi
 Vietnamese
 Indonesian
 Japanese
 Korean