

Dernière mise à jour : 2026-03-30
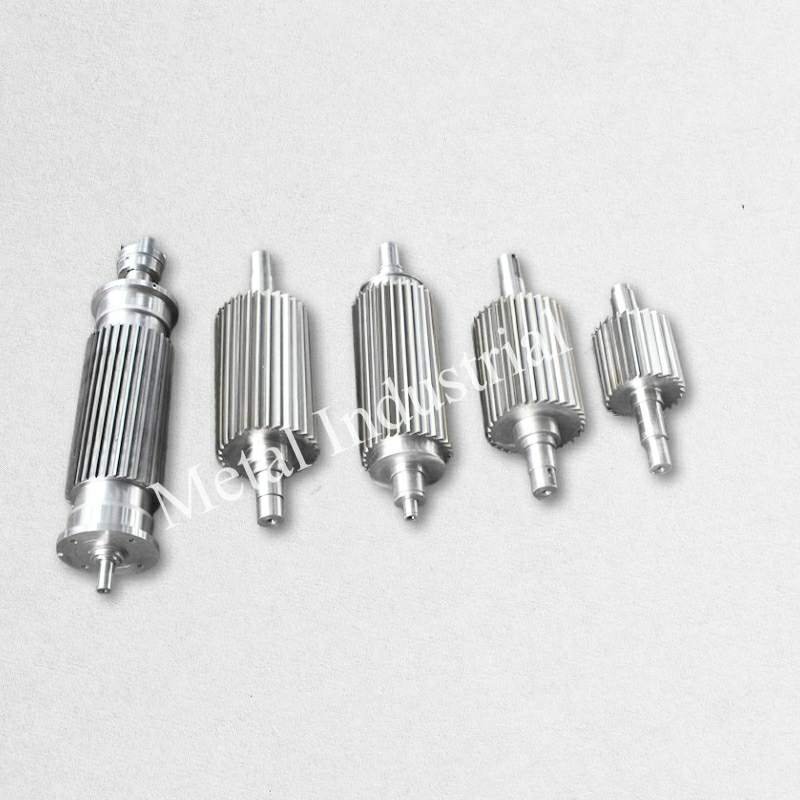
Note de sécurité et de conformité (Royaume-Uni) : Cet article fournit des conseils généraux sur les meilleures pratiques pour le remplacement des couteaux rotatifs. Il ne remplace pas l'évaluation des risques de votre site, la documentation du fabricant d'origine (OEM) ou le jugement d'un ingénieur compétent. Vérifiez toujours les jeux de protection, les limites de faux-rond et les systèmes de travail sûrs conformément à la réglementation PUWER avant de remettre l'équipement en service.
Avis Cet article fait référence aux produits et capacités de MAXTOR METAL. L'auteur est affilié à Nanjing METAL Industrial.
Portée et hypothèses
- Ce guide couvre à l'identique les projets de remplacement de couteaux rotatifs où l'objectif est de restaurer le fonctionnement et de garantir un approvisionnement reproductible (spécifier → vérifier → documenter).
- Il ne fournit pas remplace pas d'évaluation complète de la sécurité. Si votre remplacement modifie les jeux de protection, les vibrations/bruits, les forces de coupe, les paramètres de contrôle ou introduit de nouveaux risques, traitez-le comme une modification et suivez la gestion du changement de votre site ainsi que l'examen par un ingénieur compétent.
- Tous les exemples “ typiques ” de cet article sont fournis à titre de référence uniquement. Définissez les critères d'acceptation (par ex. configuration/limites de faux-rond, méthode d'essai de dureté) avec la documentation de votre OEM et l'ingénieur responsable avant de redémarrer l'équipement.
Les lignes de production existantes tombent rarement en panne d'un coup. Elles tombent en panne un consommable à la fois — jusqu'à ce que la pièce que vous ne pouvez pas acheter devienne celle qui arrête toute la ligne.
Les raisons habituelles sont prévisibles :
- Le fabricant d'origine (OEM) ne prend plus en charge la machine, ou la référence de la pièce a été abandonnée.
- “Les pièces de rechange ” à peu près similaires » ne correspondent pas réellement à l'ajustement, au serrage ou à la géométrie de coupe.
- Les coûts d'arrêt de production ne cessent de grimper car les changements de format deviennent fréquents, lents et plus risqués.
Si vous exploitez une ligne où le temps de fonctionnement et la qualité des granulés sont directement liés à un couteau rotatif, le remplacement complet de la machine est souvent le moyen le plus coûteux de résoudre un problème de pièces de rechange.
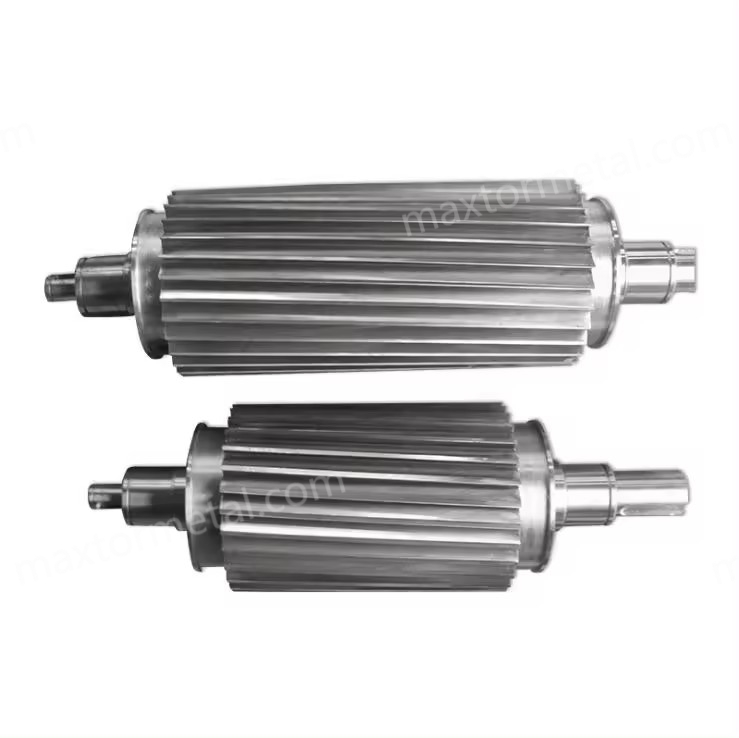
Une voie plus sûre consiste à qualifier des couteaux rotatifs de rechange sur mesure— fabriqués selon la géométrie fonctionnelle de votre couteau existant, vérifiés par un processus de premier article, et documentés de manière à ce que les achats et la maintenance puissent renouveler la commande sans avoir à refaire l'ingénierie à chaque fois.
Ce que vous obtiendrez de cette approche :
- Assurance de l'ajustement grâce à la mesure basée sur les références et à la cartographie des tolérances
- Remise en service plus rapide grâce à une approbation contrôlée du premier article
- Coût total de possession (TCO) réduit en prolongeant le temps de fonctionnement et en réduisant le risque de changement
Points clés à retenir: Traitez le couteau comme un projet de pièce de rechange contrôlé (spécifier → vérifier → documenter), et non comme un achat d'urgence.
Les essentiels de la rétro-ingénierie
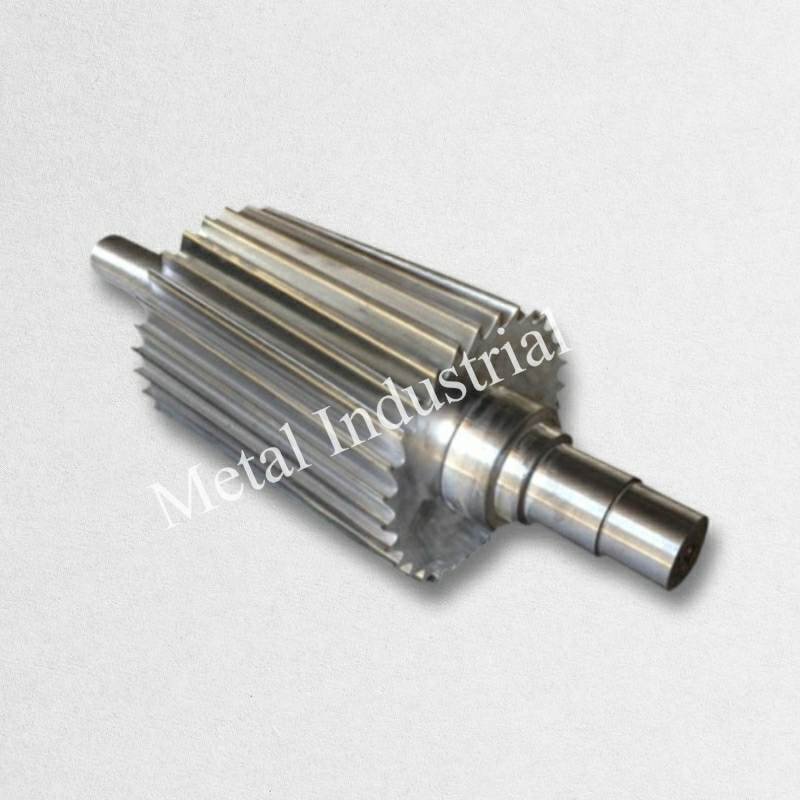
Collecte et saisie des données
La rétro-ingénierie fonctionne le mieux lorsque vous considérez la pièce usée comme une preuve, et non comme le plan d'origine.
Commencez par une collecte de données qui réduit l'ambiguïté :
- Saisissez le contexte de fonctionnement: matériau coupé (vierge vs broyé, composés chargés), débit typique et mode de défaillance observé (émoussement rapide, micro-ébréchure, traces d'échauffement, bavures).
- Photographiez et étiquetez la pièce avant le nettoyage (les deux côtés, les faces de montage, tous les marquages).
- Mesurez d'abord les références “ sans usure ”: alésages, clavetages, faces de montage, cercles de boulonnage — des caractéristiques qui définissent la position sur l'arbre et auxquelles on peut souvent faire plus confiance qu'à l'arête de coupe.
Pour la saisie des données, une méthode hybride est courante :
- Dimensions de base au pied à coulisse/micromètre
- Ajustements et géométrie critiques par MMT ou numérisation 3D (en particulier lorsque le couteau présente des profils complexes)
The goal isn’t to collect “as much data as possible.” It’s to collect enough data to define datums and control the features that affect fit, runout, and cutting performance—so your des couteaux rotatifs de rechange sur mesure behave predictably when installed.
Tolerance mapping and CAD
Once you have measurements, map them into a CAD model around a datum structure:
- Primary datum: typically a mounting face or bore that defines axial location
- Secondary datum: a feature that defines rotation or concentricity (bore, pilot, shaft interface)
- Tertiary datum: a keyway/bolt pattern that locks orientation
Then, assign tolerances based on how the cutter behaves in the machine:
- Fits that control concentricity and runout get the tightest attention.
- Cutting edges and relief angles are controlled to preserve function (cut quality) rather than copying wear.
- Features that don’t influence assembly or safety can be looser to keep cost sensible.
In metrology-focused reverse engineering guidance (for example, Verisurf’s reverse engineering best practices), the recurring theme is the same: define datums early and close the loop between measurement, CAD, and inspection—so you reduce “do-overs” and supplier interpretation drift over repeat orders.
If you want a formal language for this, the ISO GPS (Geometrical Product Specifications) framework is commonly referenced in manufacturing. For example, ISO 1101 defines the symbol language and rules for geometrical tolerancing (form, orientation, location, and run-out).
First-article approval
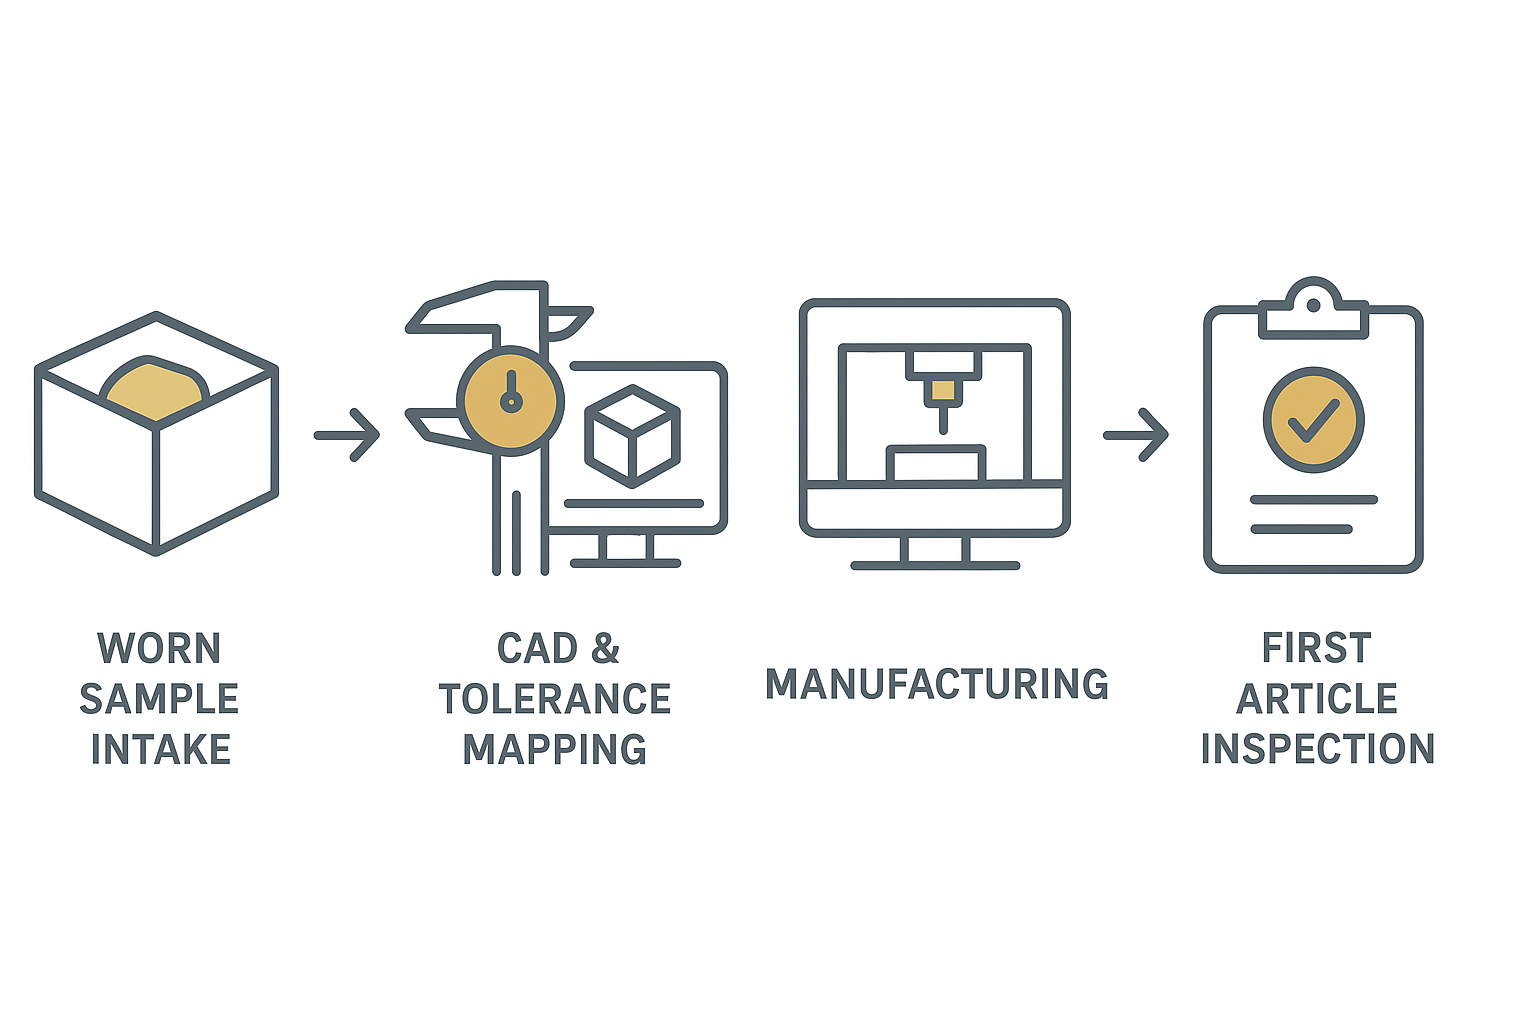
A replacement should not go straight from “CAD done” to “production batch.” A controlled first-article step is your risk firewall.
A practical first-article approval flow includes:
- First-article manufacturing to the mapped tolerances
- Inspection against the CAD drawing / agreed checkpoints
- A sign-off package (FAI) you can file and reuse
Conseil de pro: Your FAI checkpoints should match how you’ll actually accept future batches—don’t measure “nice-to-have” dimensions that nobody will re-check under time pressure.
FAI checklist (copy/paste template)
- Part ID, revision, and quantity (first article vs pilot)
- Material grade and heat-treatment record
- Hardness test method and results (e.g., Rockwell per ISO 6508, Vickers per ISO 6507, or Brinell per ISO 6506)
- Datum features verified first (mounting face / bore / pilot / keyway)
- Bore size and fit-critical dimensions
- Runout/concentricity at the mounting interface (define measurement setup and acceptance criteria)
- Axial location features (spacers, shoulders) and stack-up notes
- Bolt circle / keyway orientation (if applicable)
- Edge geometry checkpoints (relief angles, edge condition, burr limits)
- Surface finish on mounting faces / contact areas
- Visual inspection (chips, cracks, coating defects) + packaging protection for edges
Tip: Replace each line with your site’s specific acceptance criteria and measurement method so future reorders can be received consistently.
For a widely used example of how organizations structure and document first-article inspection, see SAE AS9102 (Aerospace First Article Inspection Requirement). It is aerospace-focused, but the documentation logic (part accountability, material/process accountability, characteristic results) is a useful reference when building a clear FAI/FAIR pack for industrial spares.
Matériaux, précision, assurance qualité
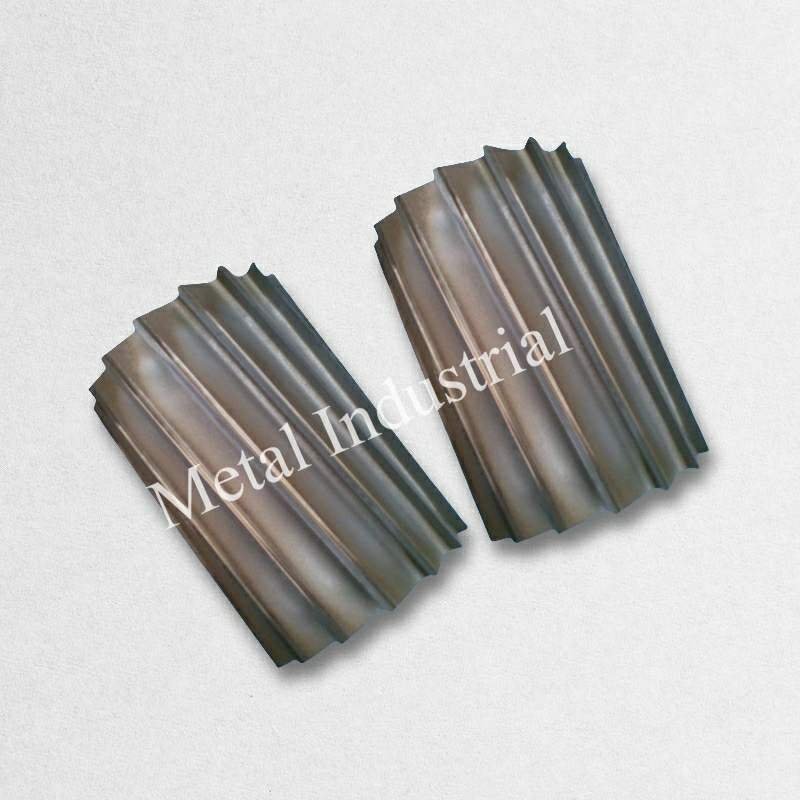
Steel, carbide, coatings
Material choices for rotary cutters are usually a trade between résistance à l'usure et dureté.
- Tool steels (e.g., D2/SKD-11 class) are common when you need a balanced option with predictable heat treatment.
- HSS can improve toughness where intermittent loading or impact is a concern.
- Carbide (tipped or solid) is often used when abrasion dominates (e.g., glass-filled compounds), but brittleness has to be managed through geometry and handling.
Coatings can be a second lever—particularly when you’re fighting friction and abrasive wear. Material selection resources for granulator blades commonly highlight matching the steel/carbide route to the plastic and filler content, rather than defaulting to one “best” material.
Specifying custom rotary cutter replacements
A spec that prevents costly back-and-forth typically includes:
- Cutter type and function (rotary knife, pelletizer cutter, granulator rotor knife)
- Quantity and whether you’re qualifying a single first article or a small pilot batch
- A drawing (preferred) or a controlled reverse-engineering scope (datums + checkpoints)
- Surface finish and edge condition requirements
- Heat treatment expectations (hardness range and where it matters)
If you’re sourcing globally, it also helps to specify what documents are non-negotiable at the quote stage (not after the parts are in transit).
Precision targets and traceability
For legacy machines, precision is less about “tight everywhere” and more about “tight where it prevents downtime.”
Typical high-impact controls include:
- Runout / concentricity control at the mounting interface (define the measurement setup and acceptance criteria with your engineer/OEM; values are equipment-specific)
- Axial positioning so the cutter tracks correctly relative to the bed knife/anvil (verify guarding clearances and safe operation before restart)
- Edge geometry consistency to avoid pellet tails, fines, or quality drift
This is also the point where supplier capability matters—especially for plants that need repeatability over multiple reorder cycles.
Par exemple, MAXTOR MÉTAL manufactures custom industrial blades (including plastic granulator rotary knives et plastic pelletizer knives) and is set up for build-from-drawing/sample workflows. In practice, the useful question to ask any supplier is not “can you copy this part?” but:
- Can you define and agree the datums that control fit?
- Can you provide an inspection pack aligned to those checkpoints?
- Can you maintain traceability (material and process records) batch-to-batch?
Answering those three questions up front is how you avoid tolerance drift and “mystery reworks” on the shop floor.
⚠️ Avertissement: If a quote comes back with no mention of inspection/acceptance criteria, you’re likely buying interpretation—not a controlled spare part.
Exemples de résultats (de sources publiées)
Because results depend heavily on polymer, throughput, cutter design, and maintenance practice, use the examples below as illustrative only, not guaranteed outcomes.
Mini-case A: Fewer changeovers and lower blade-related cost
- Problème: Frequent blade changes and rising downtime/labour cost.
- Action (reported): Switching to a better-fit/customized blade approach and tightening maintenance/sharpening practice.
- Outcome (reported): Blade changes reduced from 12 to 3 per month (reported as ~65% less downtime) and monthly blade-related cost lowered from >$800 to ~$450 (including labour).
- When it applies: Plants where changeovers are frequent and knives are treated as consumables without a controlled acceptance/maintenance routine.
Mini-case B: Longer life via process/material treatment (industry example)
- Problème: Short knife life and inconsistent performance in pelletizing.
- Action (reported): Evaluating process/material treatment improvements (e.g., cryogenic processing trials) and verifying against a defined acceptance method.
- Outcome (reported): Extended service life and cost savings were reported in a pelletizer blade trial case study; results vary by polymer, throughput, and knife geometry.
- When it applies: High-throughput lines where small improvements in knife life compound into measurable downtime and scrap reduction.
Sources (examples):
- Granulator maintenance/sharpening article with the changeover/cost example: https://maxtormetal.com/maintain-sharpen-granulating-blade-optimal-performance-2025/
- Pelletizer blade cryogenic processing case study: https://ctpcryogenics.com/services/industrial/case-study-rubbermaid/
If you want, we can replace these with your own internal examples later (even anonymized ranges) to make the outcomes more directly relevant to your equipment.
Conformité au Royaume-Uni, importation, TCO
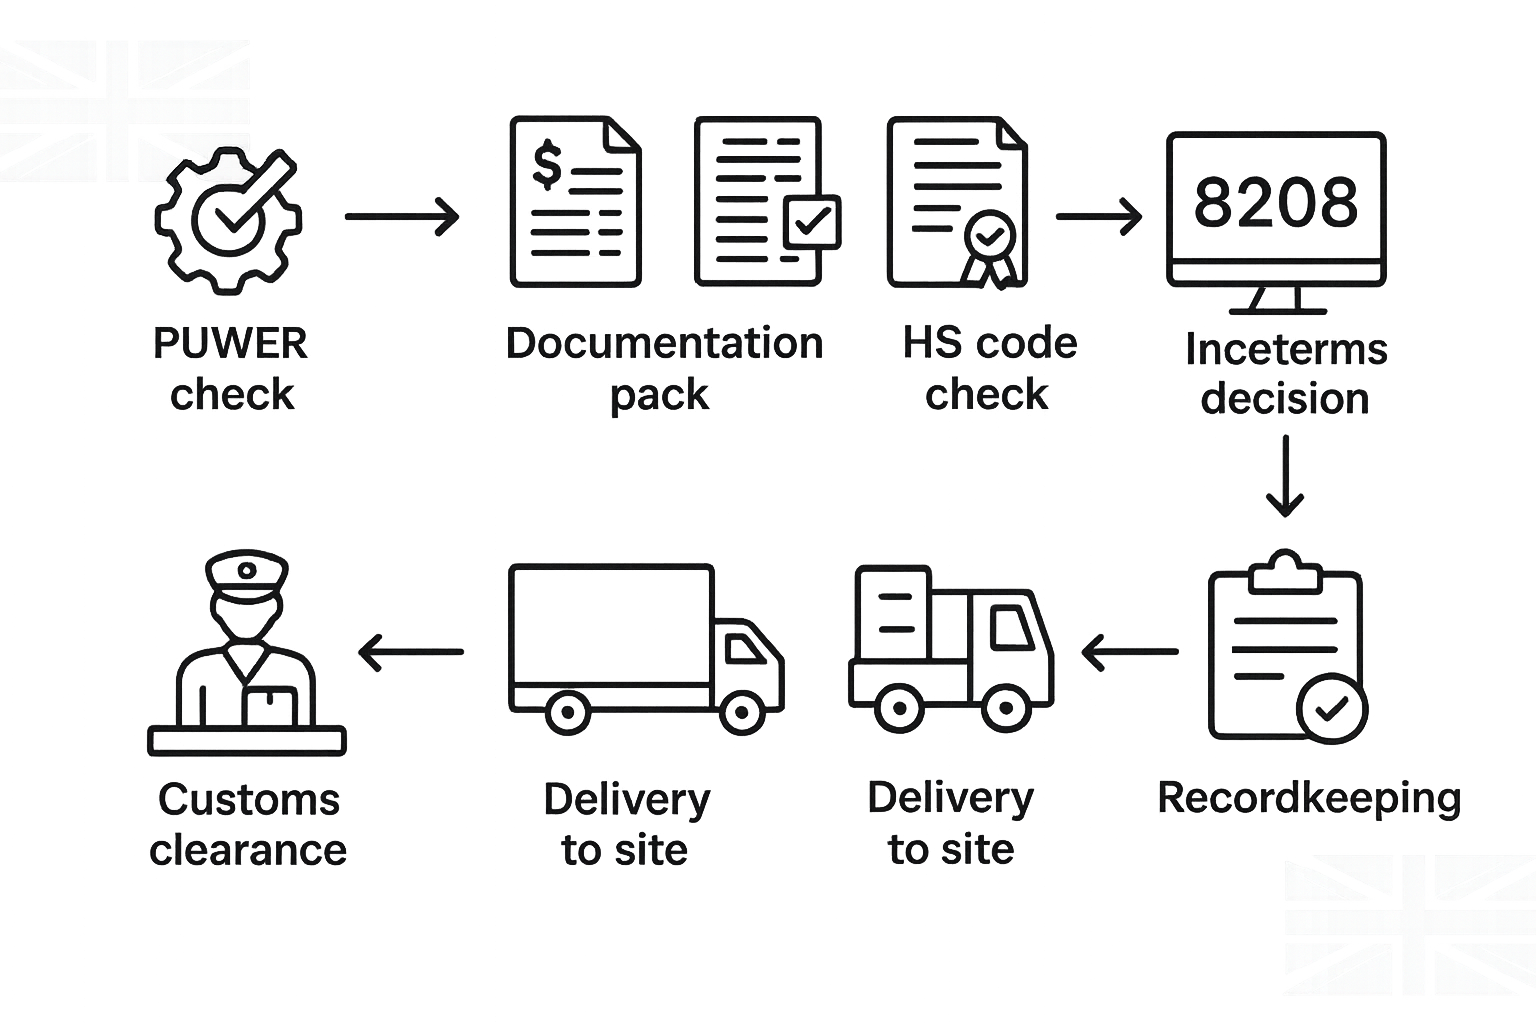
PUWER, UKCA/CE scope
For UK operators, two practical lenses matter:
- Safe use of work equipment (PUWER)
HSE’s overview of PUWER (Provision and Use of Work Equipment Regulations 1998) emphasises that equipment must be suitable for use, maintained, inspected where needed, and supported by appropriate information/instructions and training.
A rotary cutter replacement affects exactly those points—because it can change guarding clearances, cutting forces, vibration, and the operator’s safe system of work.
- When modifications become “substantial”
If the change is like-for-like (same function, no new hazards), you’re typically in a maintenance/refurbishment space. If the change introduces new hazards or materially changes how the machine operates, HSE’s guidance on refurbished and modified machinery explains why the modifier may take on “manufacturer-like” responsibilities.
For context on supply-side obligations, the UK government guidance on the Supply of Machinery (Safety) Regulations 2008 (Great Britain) is the right place to sanity-check whether your change stays a spare-part replacement—or edges into a broader conformity assessment question.
Docs, HS codes, Incoterms
For importing cutters into the UK, smooth procurement is mostly about eliminating paperwork gaps.
A practical documentation pack usually includes:
- Commercial invoice and packing list
- Proof of origin (acceptable formats are explained on GOV.UK’s guidance for Get proof of origin for your goods)
- Material and inspection documents you need for acceptance (e.g., hardness, key dimensions)
On classification, industrial knives and cutter blades often sit under HS heading 8208—confirm the exact commodity code for your specific cutter description using the GOV.UK Trade Tariff tool.
Incoterms decide who does what:
- DDP: supplier typically manages import clearance and delivery duties (lower admin load for the buyer, but verify what’s included).
- DAP: buyer handles import clearance and pays duties/VAT (more control, more responsibility).
If your team has been burned by delays before, align Incoterms with who will provide each document—and who is accountable if customs asks questions.
Life, downtime, payback
TCO is rarely dominated by the cutter’s unit price.
The big levers are:
- Coût des temps d'arrêt per changeover (lost throughput, labour, restart waste)
- Quality cost (fines, tails, off-spec pellets, downstream feeding issues)
- Reorder risk (a replacement that doesn’t fit creates a second downtime event)
A simple way to quantify payback is:
- Estimate how many changeovers you can avoid per month if the replacement holds edge longer.
- Add the cost of one “bad fit” event as a risk cost (even if it’s low probability).
- Compare that against the delta between a standard blade and a verified, documented custom replacement.
Conclusion
Custom rotary cutter replacements are a practical way to extend the life of legacy machines—if you treat them as a controlled engineering and procurement process.
That process is straightforward:
- Specify the cutter around datums and functional geometry, not around worn edges
- Qualify the part with mapped tolerances and a first-article inspection pack
- Import with confidence by aligning documentation, HS code checks, and Incoterms responsibilities
Next steps:
- Share the worn sample and/or drawings
- Agree the critical tolerances (fits, runout, axial location, edge geometry)
- Request an FAI pack that matches how your site will accept repeat orders
Références
- HSE: PUWER (Provision and Use of Work Equipment Regulations 1998): https://www.hse.gov.uk/work-equipment-machinery/puwer.htm
- HSE: Refurbished and modified machinery: https://www.hse.gov.uk/work-equipment-machinery/refurbished-modified-machinery.htm
- GOV.UK: Supply of Machinery (Safety) Regulations 2008 (Great Britain): https://www.gov.uk/government/publications/supply-of-machinery-safety-regulations-2008/supply-of-machinery-safety-regulations-2008-great-britain
- GOV.UK: Get proof of origin for your goods: https://www.gov.uk/guidance/get-proof-of-origin-for-your-goods
- GOV.UK: Trade Tariff tool: https://www.gov.uk/trade-tariff
- ISO: ISO 1101 (Geometrical tolerancing): https://www.iso.org/standard/66777.html
- SAE: AS9102 (Aerospace First Article Inspection Requirement): https://www.sae.org/standards/as9102-aerospace-first-article-inspection-requirement
- IAQG: 9102 First Article Inspection Requirement overview: https://iaqg.org/standard/9102-first-article-inspection-requirement/
Auteur
Written by Tommy Tang, Senior Sales Engineer at Nanjing METAL Industriel (12 years). Certifications: CSE, Formation médicale continue, Ceinture verte Six Sigma, PMP.

 English
 Spanish
 Italian
 French
 Portuguese
 Russian
 German
 Arabic
 Hindi
 Vietnamese
 Indonesian
 Japanese
 Korean