

Choisir un fabricant de lames de trancheuse à pain est une décision opérationnelle à long terme, et non un simple achat de pièces de rechange. Si vous qualifiez correctement le fournisseur — capacité d'ingénierie, rigueur en matière d'AQ/conformité et fiabilité d'approvisionnement —, vous obtiendrez des tranches plus nettes, moins de miettes et de défauts, des cycles de production plus longs entre les changements et un coût total de possession (TCO) inférieur.
Ce guide est rédigé pour les lames de trancheuse à pain industrielles utilisées dans les lignes de boulangerie à haut débit et les programmes de construction OEM, où la répétabilité d'un lot à l'autre importe plus qu'un seul bon échantillon.
Ce que vous allez évaluer : ingénierie, AQ/conformité, fiabilité d'approvisionnement
Résultats : meilleure qualité de tranche, TCO réduit, moins de changements et de défauts
Comment utiliser ce guide : demandez des données, lancez des projets pilotes, vérifiez les documents, puis passez à l'échelle
Cadre de sélection pour un fabricant de lames de trancheuse à pain

Qualifier un fabricant
Commencez par un processus de qualification rigoureux et difficile à contourner. Pour un approvisionnement à long terme, vous recherchez la répétabilité d'un lot à l'autre, et non un “ bon échantillon ” unique.”
Capacité d'ingénierie (peuvent-ils fabriquer ce dont votre ligne a besoin ?)
- Peuvent-ils travailler à partir de plans, d'échantillons ou de photos et traduire cela en dimensions contrôlées et en géométrie de tranchant ?
- Peuvent-ils expliquer comment ils choisissent l'acier, le traitement thermique, les objectifs de dureté et la finition du tranchant pour différents types de pain et vitesses de ligne ?
- Peuvent-ils fournir une liste de contrôle de compatibilité (modèle de machine, nombre de lames, longueur/largeur/épaisseur, configuration des trous, guides, méthode de tension) et confirmer les tolérances avant de faire une offre ?
Capacité d'AQ/conformité (pouvez-vous passer les audits avec leurs documents ?)
- Peuvent-ils fournir une traçabilité par lot (matière première → traitement thermique → rectification → inspection finale → emballage) ?
- Peuvent-ils fournir la documentation relative au contact alimentaire et à l'hygiène adaptée à votre région et aux exigences de vos clients ?
- Disposent-ils d'étapes d'inspection contrôlées (matériel entrant, contrôles en cours de processus, inspection finale) et de registres que vous pouvez auditer ?
Fiabilité d'approvisionnement (peuvent-ils assurer votre production pendant 12 à 36 mois ?)
- Peuvent-ils s'engager sur des plages de délais de livraison et des objectifs de performance de livraison à temps et complète (OTIF) ?
- Peuvent-ils gérer un stock tampon/VMI si vos changements sont fréquents ou si la demande est saisonnière ?
- Disposent-ils d'une procédure d'escalade définie lorsqu'un défaut apparaît sur une ligne en fonctionnement ?
Points clés à retenir: Un fournisseur de lames “ qualifié ” est un fournisseur auprès duquel vous pouvez commander à nouveau sans avoir à revivre de mauvaises expériences — car les données d'ingénierie, les dossiers d'AQ et le modèle d'approvisionnement sont tous contrôlés.
Conception des indicateurs clés de performance (KPI) et du plan de test
Une comparaison de fournisseurs échoue lorsque les KPI sont vagues (“ coupe bien ”) ou que la configuration pilote change d'un cycle à l'autre. Définissez vos KPI et vos conditions de test avant de couper la première miche.
Définissez des KPI mesurables sur le terrain
- Variance de l'épaisseur des tranches: mesurez la répartition de l'épaisseur des tranches (cible, plage de tolérance et dérive dans le temps).
- Génération de miettes: pesez les miettes pour X miches ou mesurez le volume de miettes capturé par votre système de collecte sur un cycle défini.
- Taux de défauts: déchirements, tranches écrasées, bords irréguliers, “ cheveux d'ange ”, défauts sur les tranches d'extrémité.
- Durée de vie de la lame: nombre de miches ou d'heures jusqu'à un seuil de fin de vie défini (par ex., le taux de miettes dépasse la limite, la variance d'épaisseur dépasse la limite ou les défauts visuels dépassent la limite).
- Temps de changement: minutes écoulées entre l'arrêt de sécurité et la première miche conforme validée.
- Impact sur la ligne: minutes de temps d'arrêt attribuables au changement/réglage des lames ; opérations de retension ou d'alignement après changement.
Verrouiller les conditions de test
- Type de pain et spécifications (pain de mie moelleux, pain croustillant, enrichi, etc.).
- Plage de température du produit (en particulier si le tranchage à chaud est prévu).
- Réglages de la trancheuse : consigne de tension, état des guides, vitesse et intervalle de nettoyage.
Si vous avez besoin d'une référence de base sur ce qui compte le plus à l'interface lame/ligne, BakingBusiness souligne que le pas, le tranchant et la tension sont les propriétés fondamentales qui déterminent les performances de tranchage en conditions de production (Les trois propriétés fondamentales des lames de trancheuse à pain — Baking Business).
Montée en puissance et requalification
Un approvisionnement à long terme nécessite des contrôles après la phase pilote.
- Plan de montée en puissance: définissez comment vous passez des quantités pilotes au volume de production complet (par ex., 1 ligne → 1 usine → multi-sites).
- Échantillon de référence + contrôle des révisions: verrouillez une lame de référence (dimensions + spécifications du tranchant + spécifications de finition) et exigez une notification de modification contrôlée.
- Déclencheurs de requalification: new steel heat, new grinding wheel/process, new coating, new packaging, or any design iteration.
- Ongoing verification: periodic incoming checks (dimensions, hardness/edge checks as applicable) and trend monitoring on crumb and thickness KPIs.
Ingénierie et performance

Materials and hardness targets
Your blade material and hardness targets should be chosen around three realities: bread type, sanitation environment, and the failure mode you can’t tolerate.
- Corrosion resistance vs edge retention: food-contact environments demand cleanable surfaces and corrosion resistance, but you still need edge stability under high throughput.
- Toughness vs brittleness: a very hard blade can hold an edge longer but may be less forgiving if alignment or tension is inconsistent. In tool steels, hardness and toughness commonly trade off—harder conditions tend to chip/crack more easily under shock, while tougher conditions may wear faster (overview: https://www.edconsteel.com.au/articles/steel-and-metal-articles/hardness-vs-toughness-tool-steel/).
What to request from a manufacturer:
- Material grade options and why they recommend them for your bread and slicer type.
- Heat treatment method and controlled hardness range (and how they verify it per lot). Heat treatment is a primary lever for tailoring hardness, ductility, toughness, and wear behavior (general explanation: https://www.metalsupermarkets.com/how-heat-treatment-of-metals-work/).
- Any surface finishing or coating options intended to reduce sticking/drag (evaluate these in your crumb and warm-bread tests).
For background reading on bread-blade materials and selection factors, you can reference MAXTOR METAL’s internal guide on bread cutting blades for industrial use.
Edge geometry and finish
Edge geometry is where slice quality, crumb behavior, and blade life meet. If your supplier can’t describe geometry in measurable terms, you’re buying outcomes blind.
- Tooth form and pitch: affects how aggressively the blade enters the crumb and crust.
- État de surface de l'arête: burr control and grind quality influence crumb generation and how quickly the edge degrades.
- Matched sets: for multi-blade frames, consistency across a set matters as much as the average.
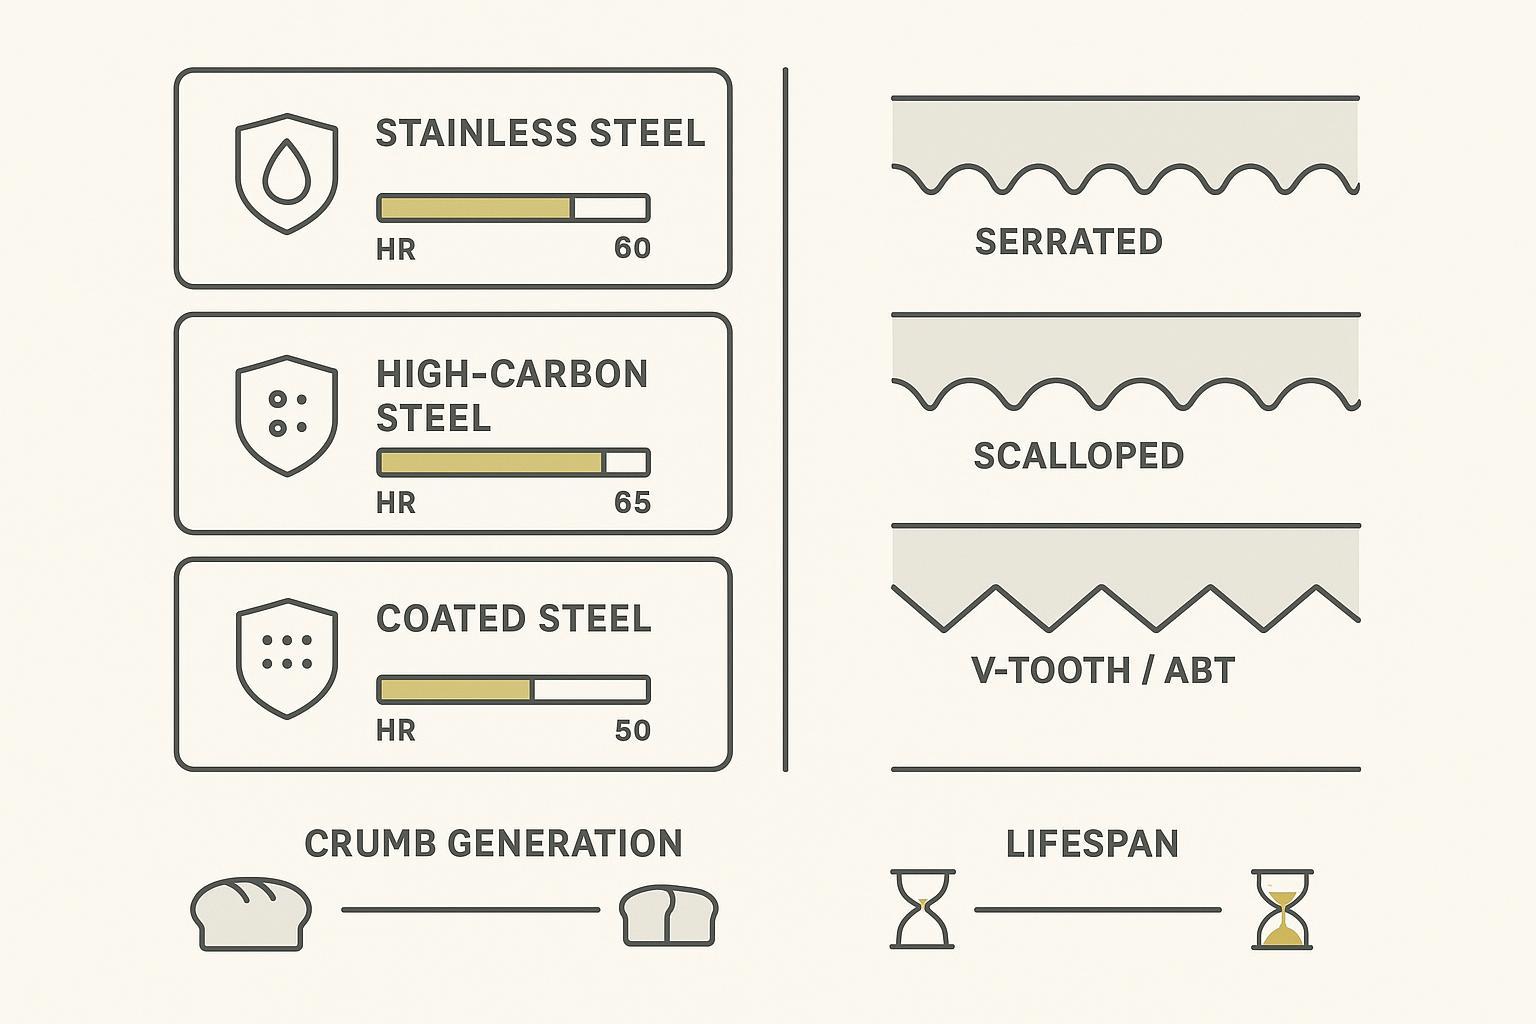
A practical way to compare profiles is to map them to your defect modes:
- If you fight tearing and ragged edges, geometry and tension stability are usually the first variables to verify.
- If you fight crumb load and sanitation burden, edge finish (burr control) and the profile’s rubbing behavior matter.
For a deeper internal breakdown of edge options (without turning this post into a product brochure), see MAXTOR METAL’s comparison of scallop vs V-tooth vs ABT bread slicer blade edges.
Warm bread and crumb control
Warm slicing is where many “fine in the lab” blades fail on the floor. As product temperature rises, crumb softens, stickiness increases, and small geometry differences show up as compression, drag, and tearing.
What to validate in a warm-bread pilot:
- Stick/slip and drag: does the blade start pulling the loaf, or does it cut cleanly at speed?
- Crumb buildup pattern: where does debris accumulate (guides, blade face, tension points), and does it cause thickness drift?
- Cleaning interval sensitivity: does slice quality fall off sharply if sanitation is delayed by one cycle?
Conseil de pro: Treat warm-bread slicing as its own qualification condition. If your production sometimes slices warm, don’t accept a supplier that only tests on fully cooled loaves.
Conformité et AQ
Food-contact and hygiene basis
For bakeries and OEMs, “food contact” is not a slogan—it’s a documentation and cleanability discipline.
For EU markets, your supplier’s documentation should align with the EU food-contact framework requirements and good manufacturing practice expectations—at a minimum, the general safety principles in Règlement (CE) n° 1935/2004 and GMP controls in Regulation (EC) No 2023/2006 (see the European Commission overview of food contact materials: https://food.ec.europa.eu/food-safety/chemical-safety/food-contact-materials_en).
For metals and alloys specifically, it’s also common to reference the EDQM (Council of Europe) guidance on metals and alloys used as food contact materials, which provides release-limit guidance and test approaches used across Europe (EDQM activities page: https://www.edqm.eu/en/metals-and-alloys-used-in-food-contact-materials-and-articles).
At minimum, you want the manufacturer to clearly state:
- Which blade materials are intended for food-contact environments and how they control surface condition (finish, burrs, corrosion risk) for food-grade slicer blades.
- What cleaning/sanitation chemicals are assumed in their material recommendations.
- How blades are packaged to prevent corrosion and contamination in transit and storage.
Traceability and ISO 9001
Traceability is your fastest path to root-cause analysis when slice quality changes.
What to request:
- Lot-level traceability: material heat/lot, heat treatment batch, in-process inspection records, final inspection results, and packing identification.
- ISO 9001 documentation: certificate validity, scope, and the supplier’s actual inspection and nonconformance control records tied to your product. For buyers, a practical check is whether the supplier can show controlled “documented information” and audit evidence consistent with ISO 9001:2015 expectations (ISO overview: https://asq.org/quality-resources/iso-9001).
- CoA / material certificate pack: composition where applicable, hardness verification method/range, and dimensional inspection report.
Neutral capability note (MAXTOR METAL): MAXTOR METAL can provide standard QA documentation packages for industrial blades—typically including a lot-linked Certificate of Analysis (CoA) and a Declaration of Conformity (DoC) upon request, along with inspection records aligned to an ISO 9001 quality management approach—so buyers can support supplier approval and internal audit requirements.
Sanitation SOPs and audit records
For long-term supply, don’t just request documents—verify that the supplier’s hygiene controls match your reality.
- Ask for a sanitation SOP that covers handling, packing, and contamination control.
- Request example audit records or inspection logs (with sensitive details redacted) that show repeatable execution.
- Define how nonconformances are handled: containment, root cause, corrective action, and re-release criteria.
Compatibilité et personnalisation

OEM fit and guides
Most “blade problems” show up as fitment and guiding problems in production.
Before you scale a new supplier, verify:
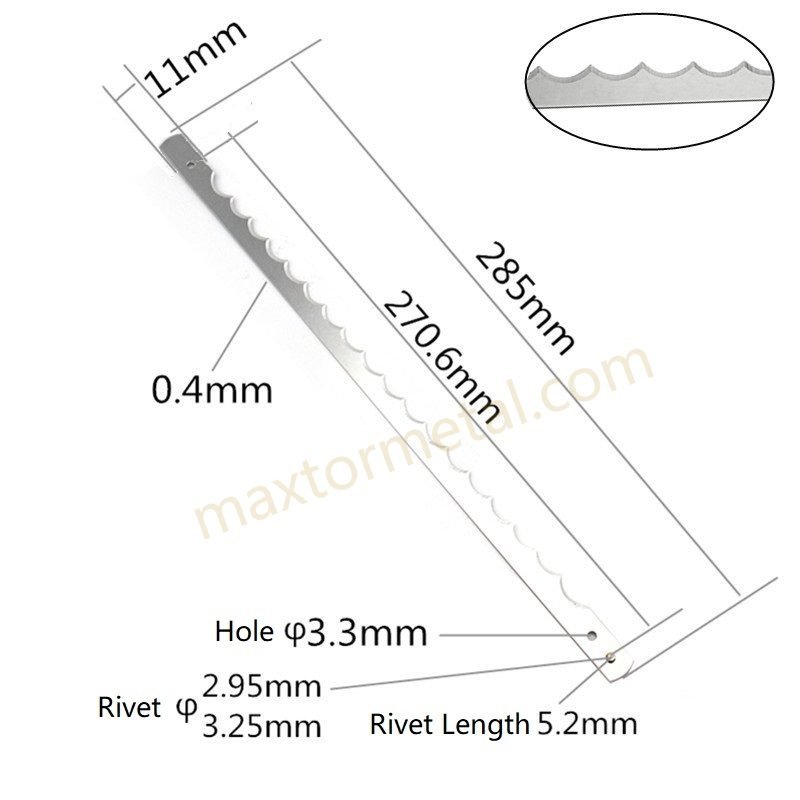
- Blade dimensions and mounting interface match your slicer design.
- Guides and wear parts are within spec; worn guides can turn a good blade into a crumb generator.
- The supplier can provide a fitment confirmation checklist tied to your machine model and drawing revision.
If you need a reference point for what information a supplier typically requests to avoid fitment surprises, MAXTOR METAL’s bread slicer blades page summarizes common configurations and manufacturing scope.
Non-standard designs and iterations
OEMs and high-mix bakeries often need iteration: tooth form changes, finish changes, material changes, or small dimensional adjustments.
To make iterations safe and fast:
- Require revision control on drawings/specs.
- Define what changes require requalification (material, heat treat, coating, edge geometry).
- Run short “A/B” pilots with the same bread spec and the same sanitation cycle.
Changeover, tension, alignment
Changeover is where supply decisions become OEE decisions.
What to evaluate in a supplier’s solution:
- Does the blade set arrive as a matched set that reduces time spent chasing tension balance?
- Are installation and tensioning instructions explicit, verifiable, and safe?
- Does the blade hold alignment across a run, or do you see repeated re-tension events?
If you want a quick refresher on how tension and edge properties drive slice outcomes, refer back to BakingBusiness’ pitch/edge/tension overview cited earlier.
Modèle d'approvisionnement et conditions commerciales

Lead times, MOQ, VMI options
A long-term blade supplier is also a supply-chain partner. For high-volume lines, the best engineering outcome still fails if you stock out.
Options to evaluate:
- Lead time bands (standard vs expedited) with documented historical performance.
- MOQ policy that doesn’t force you into excess inventory.
- VMI / safety stock for plants with seasonal demand or frequent changeovers.
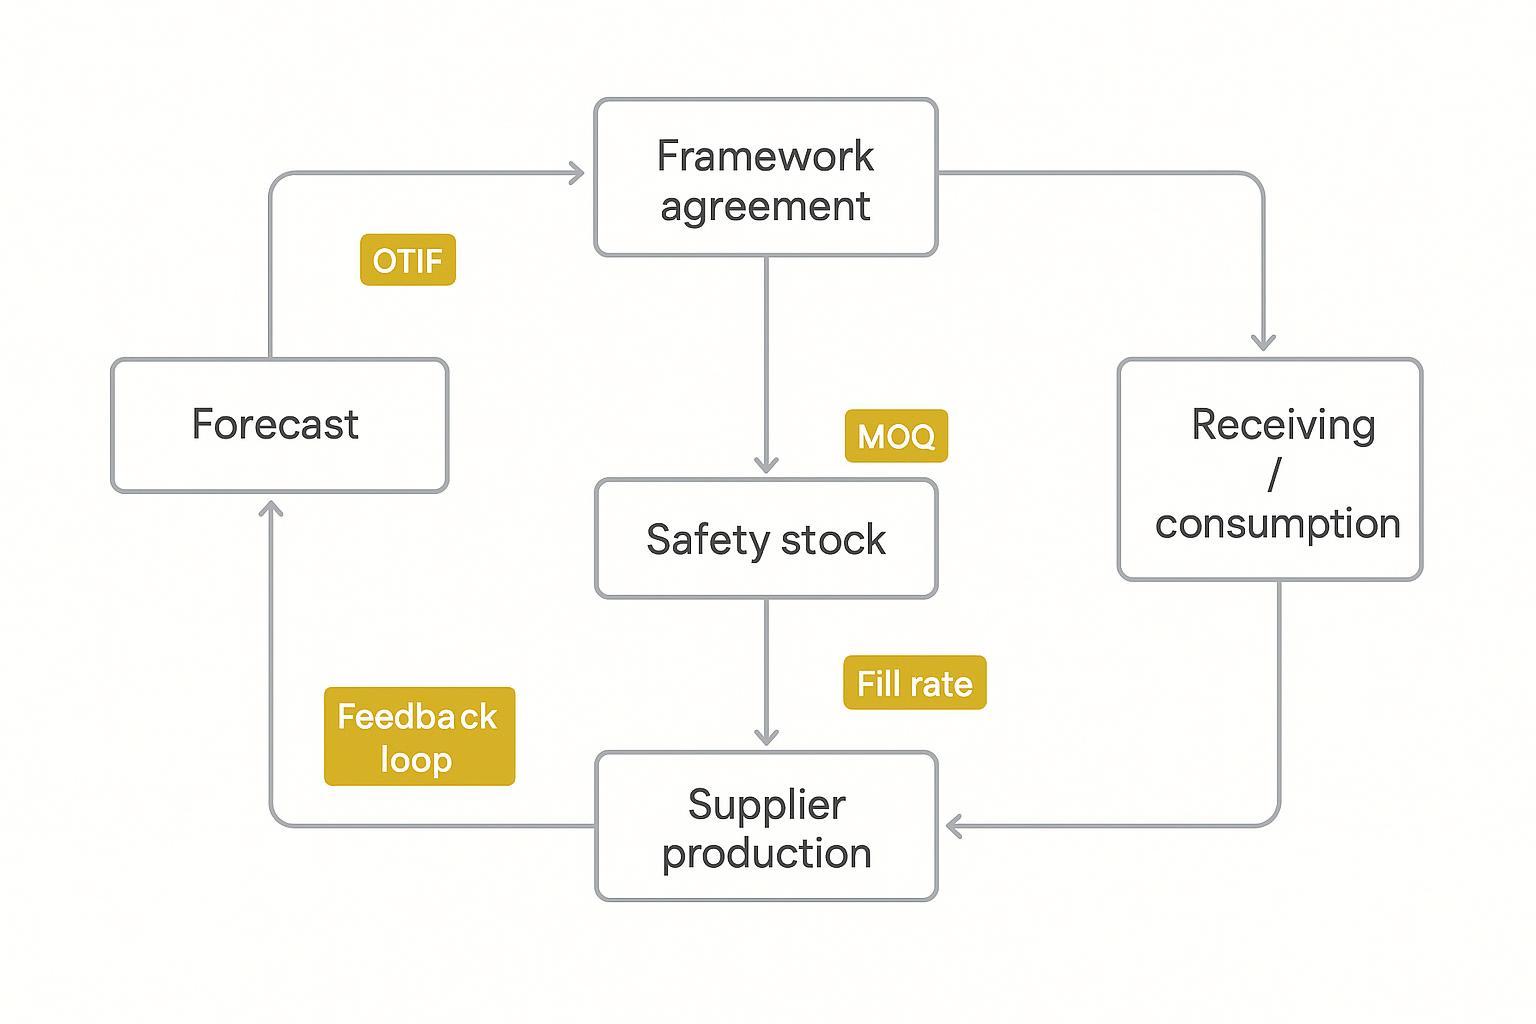
A practical VMI model for blades usually includes:
- rolling forecast (your demand signal)
- agreed safety stock at the supplier or local hub
- OTIF tracking and an escalation path when performance slips
Terms, SLAs, and KPIs
If you want long-term stability, put operational definitions into the commercial agreement.
Exemples :
- OTIF: define “on time” and “in full” precisely.
- Quality escape rate: what counts as a defect in your process, and how it’s measured.
- Corrective action timing: response time, containment timeline, and replacement policy.
- Change notification: mandatory notice for material/process changes and the requalification requirement.
Warranty and after-sales
Blades are consumables, but the supplier relationship shouldn’t be disposable.
Check whether the manufacturer provides:
- Clear warranty scope tied to measurable criteria (not vague promises).
- After-sales support for troubleshooting: tension guidance, fitment checks, and iteration support.
- A documented feedback loop: how pilot data becomes the next design iteration.
For a practical operations-oriented approach to keeping performance stable after installation, MAXTOR METAL’s bread slicer blade maintenance guide is a useful internal reference you can align with your own SOPs.
Conclusion
Key takeaways: verify KPIs, compliance docs, and supply terms before commitment
Next steps: issue RFI/RFQ, run pilot on your SKUs, finalize framework and VMI
If you want to move from “supplier quotes” to a controlled long-term supply decision, build your RFI/RFQ around the qualification framework above, attach your drawings/specs, and require a pilot plan with acceptance KPIs (crumb, thickness variance, defect rate, blade life, and changeover time).
Avis This article is an operational buyer’s guide. Any references to MAXTOR METAL are provided as optional examples and further reading; you should validate fit, performance, and compliance against your specific line conditions and regional requirements.
Dernière mise à jour : 2026-05-03
When you’re ready to run a pilot, MAXTOR MÉTAL can support engineering review from drawings/samples and align the QA document pack (e.g., CoA/DoC and lot traceability requirements) so your scale-up decision is based on verified data—not assumptions.
FAQ
What information should I send a manufacturer for a correct quote?
Send a drawing whenever possible, plus a fitment checklist: slicer model, blade count, length/width/thickness, hole pattern, guide style, and how your frame tensions the blades. Also include bread type, line speed, cleaning chemistry, and whether you ever slice warm—those inputs drive material, hardness, and edge geometry decisions.
Which KPIs matter most in a blade pilot?
Use measurable, floor-friendly KPIs: slice thickness variance, crumb generation, defect rate (tearing, ragged edges, compression), blade life to a defined end-of-life threshold, and changeover time. The key is consistency: lock your test conditions so results are comparable across lots and suppliers.
How do I avoid being fooled by a “good sample” that can’t be repeated?
Treat the pilot as a process qualification, not a one-off test. Ask for lot-based traceability, confirm controlled dimensions and edge specs, and require revision control on the “golden sample.” Then define requalification triggers (new steel heat, new grinding wheel/process, coating changes, or packaging changes) before you scale.
What should EU buyers ask for on food-contact compliance?
At a minimum, ask the supplier to state the intended food-contact material(s), the assumed sanitation chemicals, and the packaging method that prevents corrosion/contamination. For EU markets, make sure they can support the general safety expectations under the EU framework for food contact materials and GMP controls—summarized by the European Commission in Food contact materials—and be able to discuss how they evaluate metals and alloys against recognized European guidance such as EDQM metals and alloys used in food contact materials and articles.
What does ISO 9001 tell me about a supplier’s quality discipline?
ISO 9001 doesn’t guarantee “no defects,” but it does indicate the supplier should have structured controls for documented information, internal audits, and nonconformance handling. When you review a supplier, verify that their certificate scope actually covers your product/process and that they can show product-linked inspection and corrective-action records consistent with ISO 9001:2015 concepts outlined by ASQ’s ISO 9001 overview.
How do materials and heat treatment affect crumb, tearing, and blade life?
In practice, you’re balancing corrosion resistance, wear resistance, and fracture resistance. Harder conditions often improve wear but can chip more easily under shock or misalignment, while tougher conditions may tolerate variability but wear faster—an overview is described in Edcon Steel’s hardness vs toughness discussion. Heat treatment is one of the main levers that shifts this balance by changing microstructure and mechanical properties; see Metal Supermarkets’ heat treatment overview.
Should we qualify warm slicing separately?
Yes. Warm product increases stickiness and deformation, so small geometry and finish differences show up quickly as drag, compression, and tearing. If warm slicing occurs in your operation—even occasionally—treat it as a separate qualification condition with its own acceptance thresholds and cleaning-interval sensitivity checks.
Auteur
Jesse Xu — Senior Quality Engineer, QA (Quality Assurance). 15 years of experience in industrial blade quality and failure analysis.
- Failure analysis focus: Able to distinguish whether issues like edge chipping and poor wear resistance are driven primarily by heat treatment process problems or by material segregation.
- Certifications: ASQ – CQE; ISO 9001 Lead Auditor; ASNT Level II.

 English
 Spanish
 Italian
 French
 Portuguese
 Russian
 German
 Arabic
 Hindi
 Vietnamese
 Indonesian
 Japanese
 Korean