
विनाशकारी ब्लेड टूटना: धातुकर्म मूल कारण, फ्रैक्चर मैकेनिक्स, और रोकथाम के लिए आपूर्तिकर्ता नियंत्रण

Quick Answer: Catastrophic blade shattering is almost never one cause—it’s the convergence of metallurgical defects (retained austenite, carbide banding), thermal-process errors (quench cracks, insufficient temper), and geometric stress risers, triggered by a contamination event. Fractography (macro mapping → SEM/EDS → metallography → XRD) identifies which lever failed; supplier controls like AMS 2750 pyrometry and lot-level […]
सर्कुलर स्लिटिंग ब्लेड पर एडहेसिव जमाव: हीट-कॉन्टैक्ट फीडबैक, कोटिंग चयन और स्तरित डायग्नोस्टिक प्रोटोकॉल।
When adhesive starts building up on circular slitting blades, the first sign is rarely dramatic. Slit edges become slightly tacky. Roll geometry drifts. Edge quality degrades before the shift supervisor can pinpoint why. By the time a visible polymer deposit — a built-up edge (BUE) — has formed on the knife face, the blade has […]
स्लॉट तल पर ग्रिड ब्लेड टूटने को रोकना: R≥0.2 mm डिज़ाइन के लिए फिलेट रेडियस, EDM सत्यनिष्ठा, और डबल-टेंपर नियंत्रण
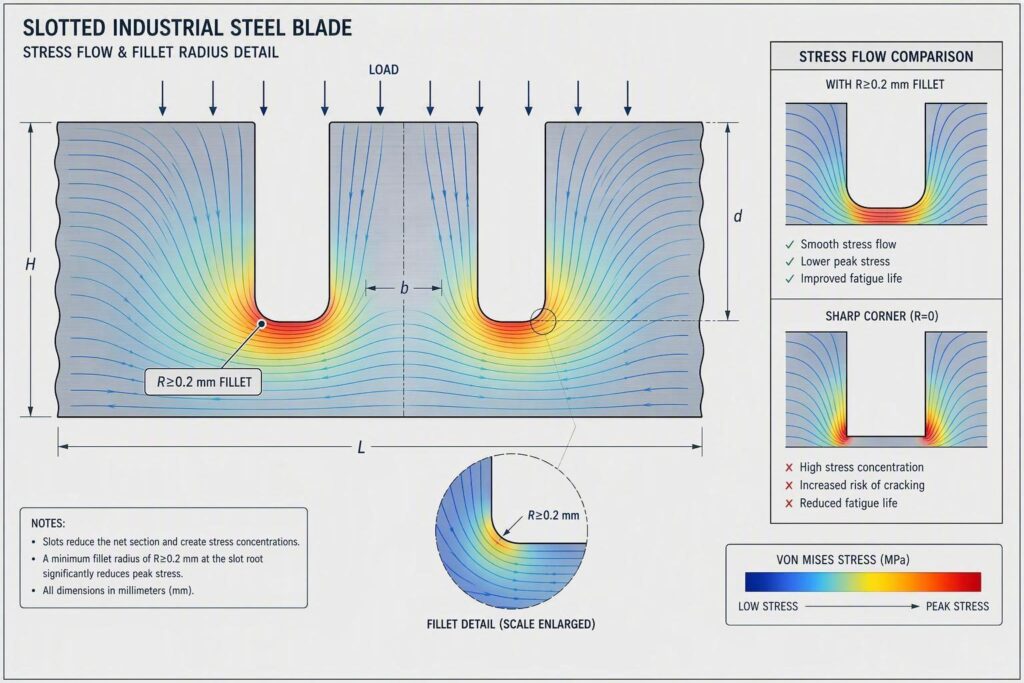
त्वरित उत्तर: स्लॉट के निचले हिस्से में ग्रिड ब्लेड का टूटना तीन कारकों के एक साथ होने के कारण होता है: उच्च प्रत्यास्थ तनाव संकेंद्रण (तीखे कोनों वाले स्लॉट के लिए Kt 7–12), सतह के दोष जो दरार शुरू करने वाले (crack initiators) के रूप में कार्य करते हैं (EDM रीकास्ट परतें, ग्राइंडिंग बर्न), और आसपास की सामग्री में अपर्याप्त टफनेस। प्राथमिक इंजीनियरिंग समाधान स्लॉट फिलेट त्रिज्या (slot fillet radius) निर्दिष्ट करना है […]
मेडिकल-ग्रेड पॉलिमर प्रोसेसिंग चाकू चयन: 420 बनाम 440C स्टेनलेस, सतह की गुणवत्ता, और वॉटर-लूप नियंत्रण
त्वरित उत्तर: मेडिकल-ग्रेड पॉलीमर पेलेटाइजिंग में, 420 और 440C स्टेनलेस विनिमेय नहीं हैं: 420 सैनिटाइजेशन-गहन या परिवर्तनशील-रसायन विज्ञान वाले वॉटर लूप में उच्च टफनेस, बेहतर पॉलिशेबिलिटी और अधिक संक्षारण सहनशीलता प्रदान करता है; जबकि 440C स्थिर, नियंत्रित-रसायन विज्ञान वाले लूप में अपघर्षक पॉलिमर के लिए उत्कृष्ट एज रिटेंशन प्रदान करता है। दोनों ग्रेडों के लिए Ra ≤ 0.4 µm मिरर फिनिश और ASTM के अनुसार सत्यापित पैसिवेशन आवश्यक है […]
कतरनी ब्लेड किनारे के टूटने का मूल कारण विश्लेषण: फ्रैक्टोग्राफी, निर्णय वृक्ष, और SOP सुधार
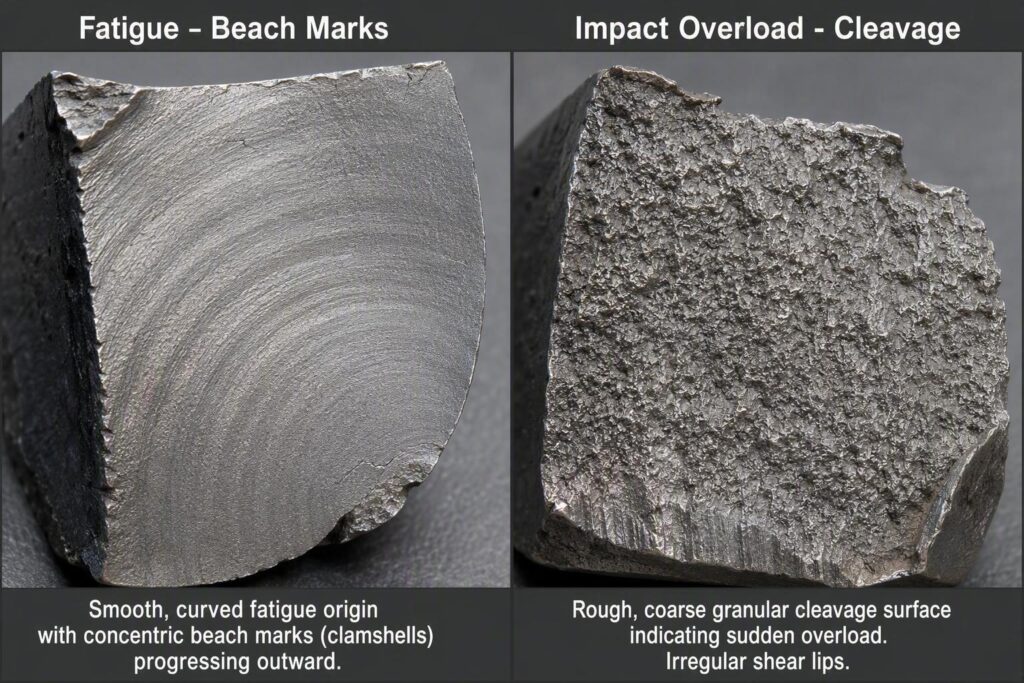
Quick Answer: Shear blade edge chipping root cause falls into two modes: fatigue (from cyclic stress — clearance errors, parallelism faults, or grinding burns) and impact (from sudden overload — foreign objects, excessive hardness, or geometry spikes). Read the fracture surface first: concentric arc-shaped beach marks mean fatigue; coarse granular cleavage with no arc pattern means […]
रोटरी चाकू ओवरलैप सेटिंग्स: कतरनी यांत्रिकी, सामग्री विंडोज और आर्बर नियंत्रण

In continuous metal coil processing, achieving a clean, square, and burr-free edge is the primary benchmark of a well-calibrated slitting line. Behind every high-yield slitting run are two critical geometric parameters governing shear-cut quality: horizontal side clearance and vertical rotary knife overlap. While horizontal clearance dictates the stress concentration across the strip width, vertical knife […]
स्क्रैप टायर और ELV श्रेडर ब्लेड: प्रति टन लागत कम करने के लिए कठोरता बनाम मजबूती को संतुलित करना
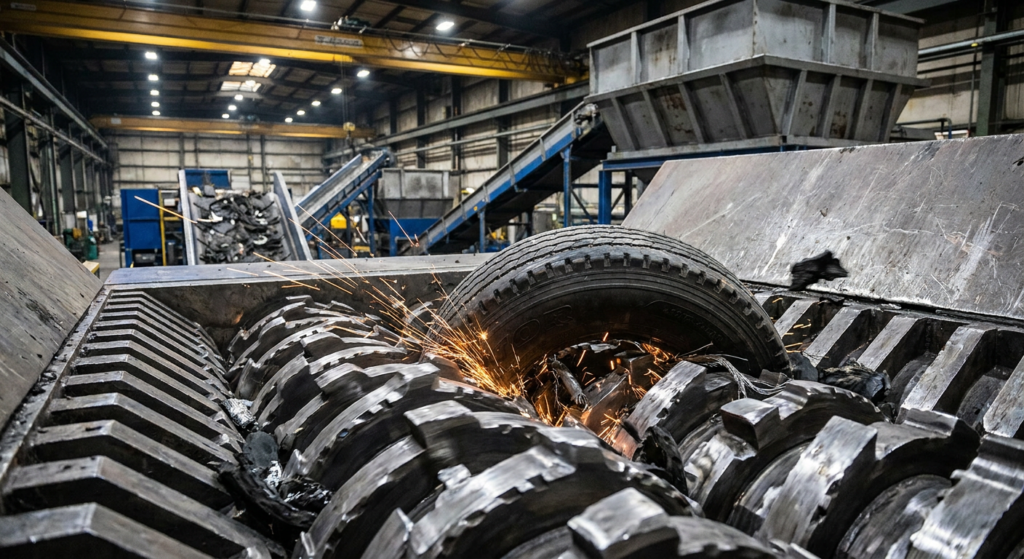
Quick Answer: Balance hardness (wear resistance) against Charpy impact toughness rather than maximizing HRC alone—DC53 at 58–60 HRC delivers roughly double D2’s impact toughness for contaminated tire/ELV streams, while a documented real-world case shows that fracture at mounting-hole geometry, not material hardness, is often the true root cause. Scope: This guide focuses primarily on primary and pre-shredding […]
स्लिटिंग डस्ट जनरेशन का मूल कारण विश्लेषण: ब्लेड फ्लैंक Ra, कार्बाइड माइक्रोस्ट्रक्चर और सेटअप टॉलरेंस।
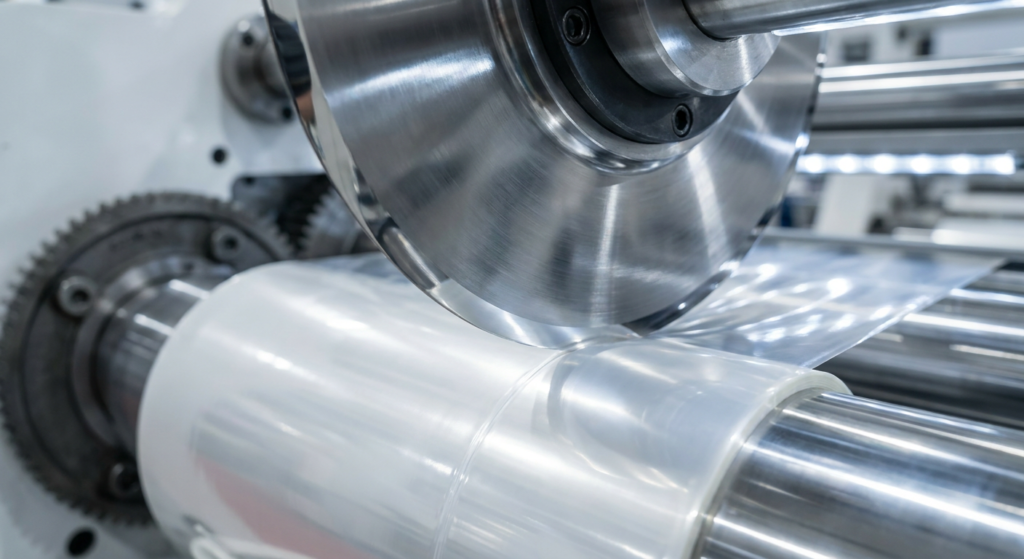
These four principles form the engineering framework Maxtor Metal’s application team applies when qualifying circular slitting knives for zero-dust converting programs in flexible packaging, nonwoven, and specialty paper lines. In high-speed flexible packaging, technical textile, non-woven, and specialty paper converting, particulate contamination is a major cause of unscheduled line shutdowns. What plant operators frequently diagnose […]
इंडस्ट्रियल स्ट्रिप ब्लेड को रीग्राइंड करना: शार्पनिंग थ्रेशोल्ड, स्क्रैप मानदंड, और जीवनचक्र लागत मॉडल
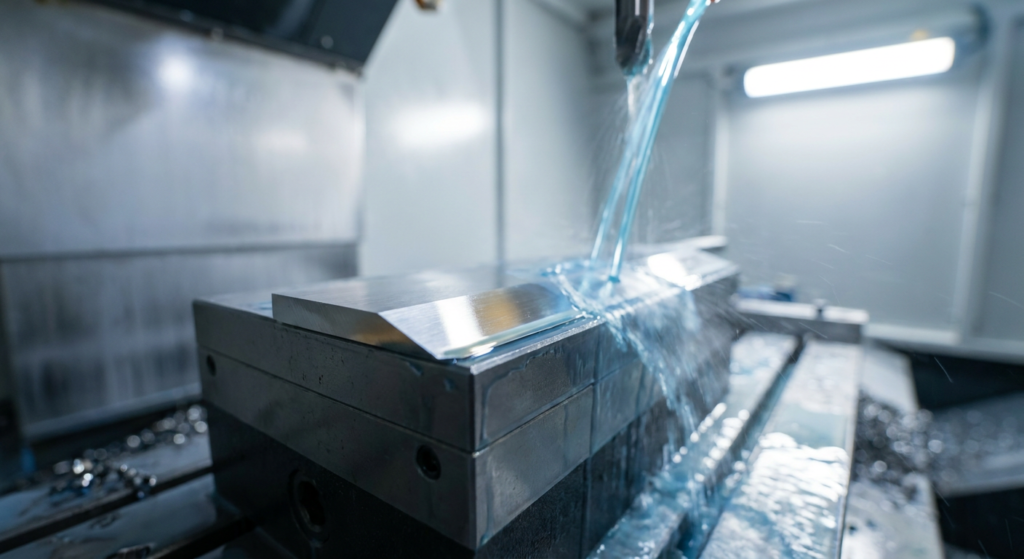
Quick Answer: Regrinding industrial strip blades is economical when: chipping depth is under 0.5 mm, remaining thickness is above 60–70% of nominal, and the estimated regrind cost is below 50% of a new replacement blade. The minimum safe stock removal is 0.010–0.015 in (0.254–0.381 mm) to clear the subsurface micro-fractured fatigue layer. Blades with radial cracks, […]
M390 बनाम CPM S90V पाउडर धातुकर्म पेलेटाइज़र ब्लेड: उच्च ग्लास-फाइबर घर्षण के तहत ग्रेड चयन
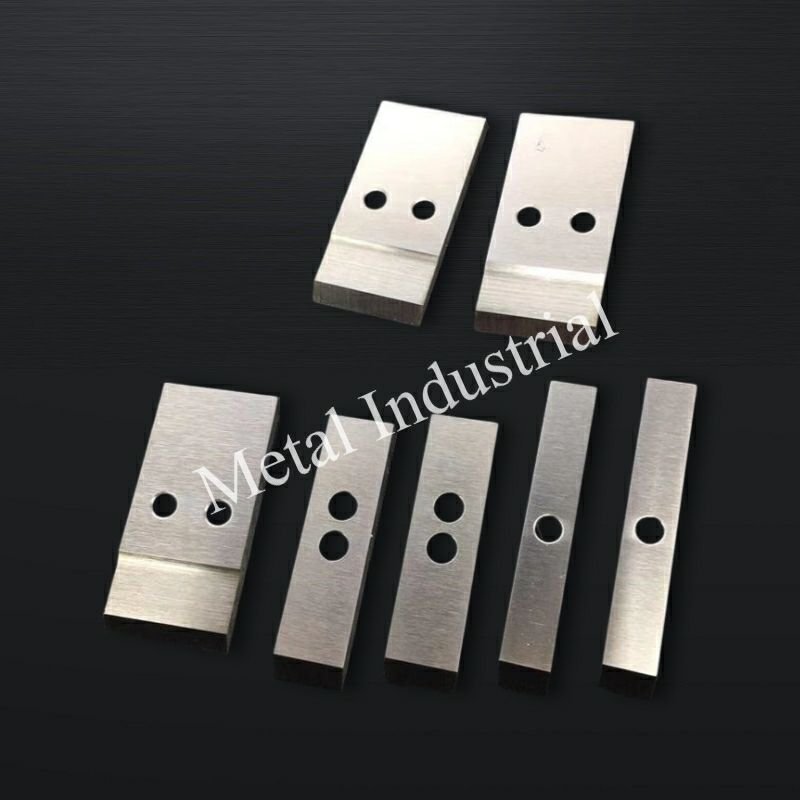
Quick answer: For pelletizing blades under high glass-fiber wear, powder metallurgy stainless steels outperform conventional tool steels because their fine, uniform carbide distribution resists micro-ploughing without the toughness trade-offs of high-alloy ingot steels. Between M390 and CPM S90V: choose CPM S90V when abrasion load is the dominant failure mode (>30% GF, neutral water); choose M390 when […]

 English
 Spanish
 Italian
 French
 Portuguese
 Russian
 German
 Arabic
 Hindi
 Vietnamese
 Indonesian
 Japanese
 Korean