
الانهيار الكارثي للشفرات: الجذور المعدنية، وميكانيكا الكسور، ورقابة الموردين للوقاية

Quick Answer: Catastrophic blade shattering is almost never one cause—it’s the convergence of metallurgical defects (retained austenite, carbide banding), thermal-process errors (quench cracks, insufficient temper), and geometric stress risers, triggered by a contamination event. Fractography (macro mapping → SEM/EDS → metallography → XRD) identifies which lever failed; supplier controls like AMS 2750 pyrometry and lot-level […]
تراكم المواد اللاصقة على شفرات القطع الدائرية: التغذية الراجعة لملامسة الحرارة، واختيار الطلاء، وبروتوكول التشخيص الطبقي.
When adhesive starts building up on circular slitting blades, the first sign is rarely dramatic. Slit edges become slightly tacky. Roll geometry drifts. Edge quality degrades before the shift supervisor can pinpoint why. By the time a visible polymer deposit — a built-up edge (BUE) — has formed on the knife face, the blade has […]
إيقاف كسر سكاكين الشبكة عند قاع الشق: نصف قطر التدوير، سلامة EDM، وعناصر التحكم في المراجعة المزدوجة للتصاميم R≥0.2 مم
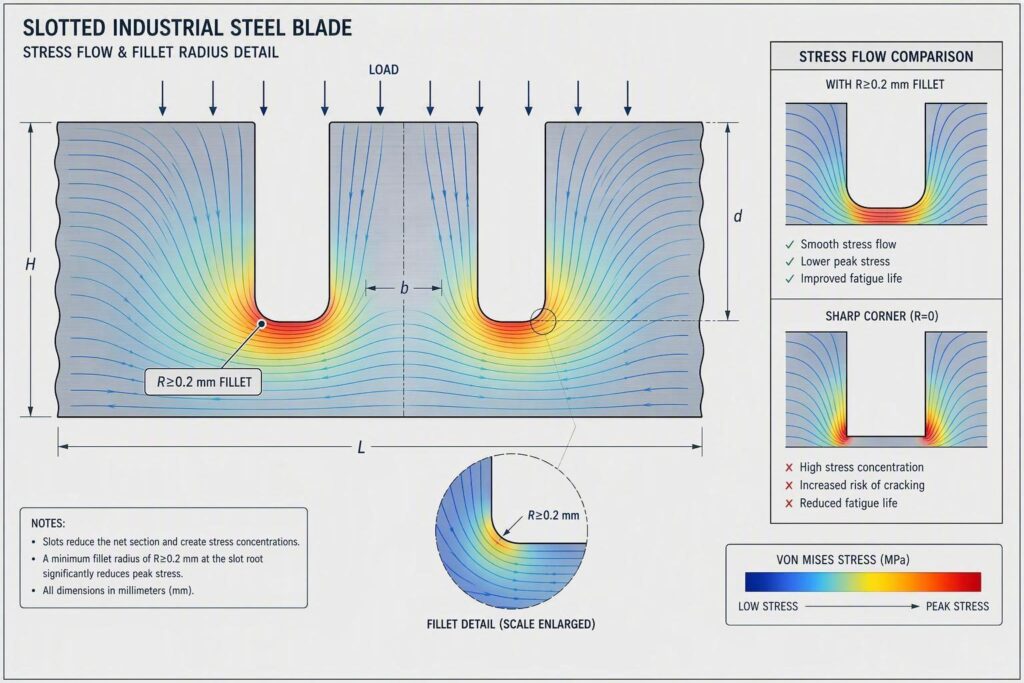
Quick Answer: Grid blade snapping at slot bottoms is caused by the coexistence of three factors: high elastic stress concentration (Kt 7–12 for sharp-cornered slots), surface defects that act as crack initiators (EDM recast layers, grinding burns), and insufficient toughness in the surrounding material. The primary engineering fix is to specify a slot fillet radius […]
اختيار سكاكين معالجة البوليمرات الطبية: الفولاذ المقاوم للصدأ 420 مقابل 440C، وإنهاء السطح، والتحكم في دورة المياه
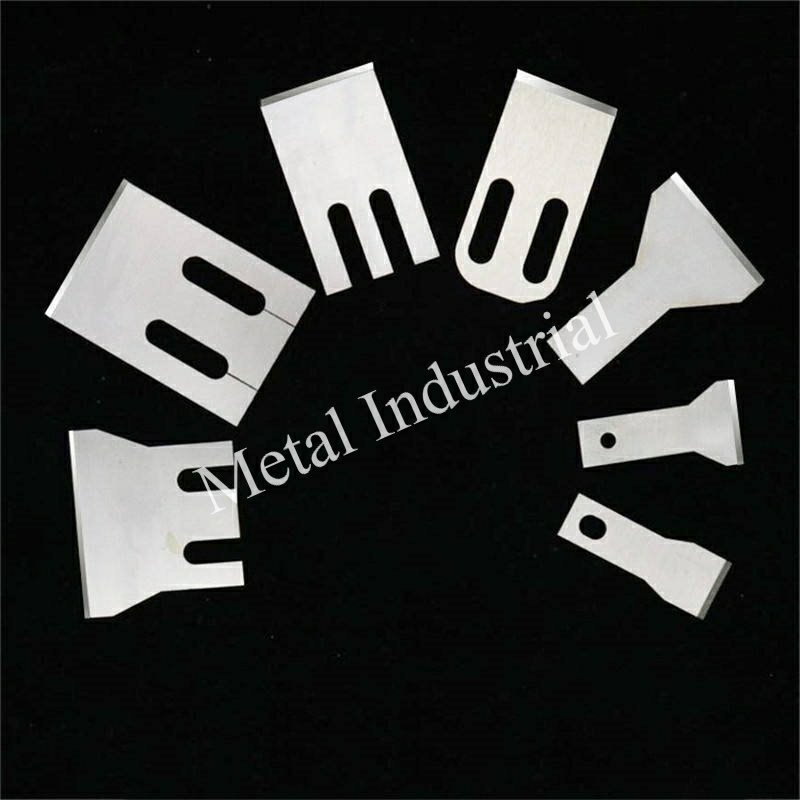
Quick answer: In medical-grade polymer pelletizing, 420 and 440C stainless are not interchangeable: 420 offers higher toughness, better polishability, and more corrosion tolerance in sanitization-intensive or variable-chemistry water loops; 440C delivers superior edge retention for abrasive polymers in stable, controlled-chemistry loops. Both grades require Ra ≤ 0.4 µm mirror finish and verified passivation per ASTM […]
تحليل السبب الرئيسي لتشقق حافة شفرات القص: دراسة أسطح الكسر، شجرة القرارات، وتصحيحات إجراءات التشغيل القياسية (SOP)
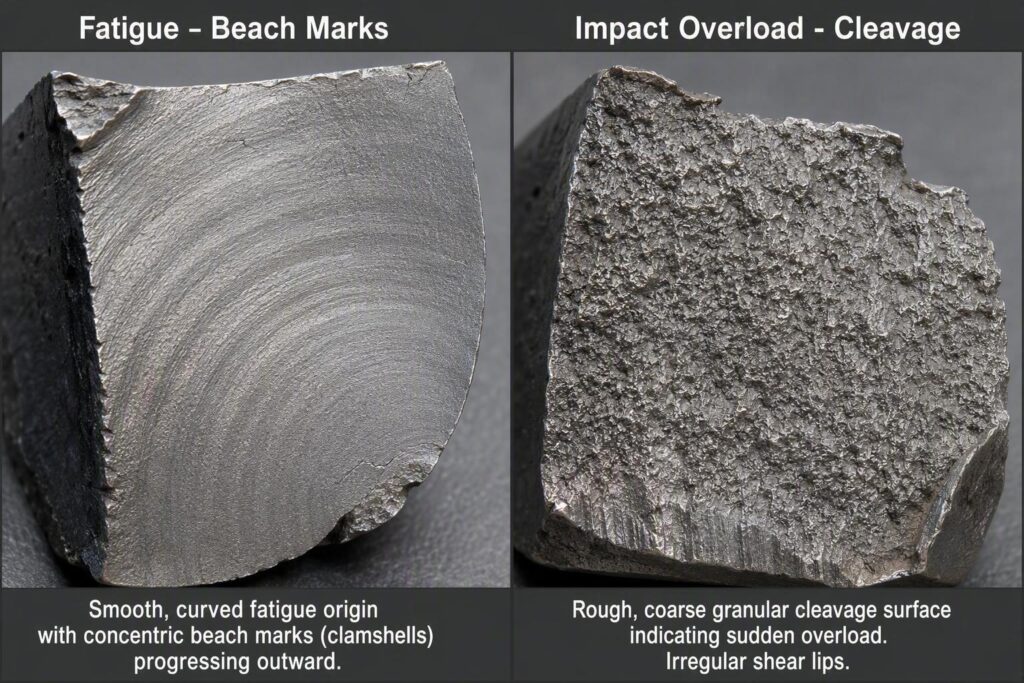
Quick Answer: Shear blade edge chipping root cause falls into two modes: fatigue (from cyclic stress — clearance errors, parallelism faults, or grinding burns) and impact (from sudden overload — foreign objects, excessive hardness, or geometry spikes). Read the fracture surface first: concentric arc-shaped beach marks mean fatigue; coarse granular cleavage with no arc pattern means […]
إعدادات تداخل السكاكين الدائرية: ميكانيكا القص، فئات المواد، والتحكم في عمود الدوران

In continuous metal coil processing, achieving a clean, square, and burr-free edge is the primary benchmark of a well-calibrated slitting line. Behind every high-yield slitting run are two critical geometric parameters governing shear-cut quality: horizontal side clearance and vertical rotary knife overlap. While horizontal clearance dictates the stress concentration across the strip width, vertical knife […]
شفرات تمزيق إطارات السيارات والسيارات المتهالكة: الموازنة بين الصلابة والمتانة لتقليل التكلفة لكل طن
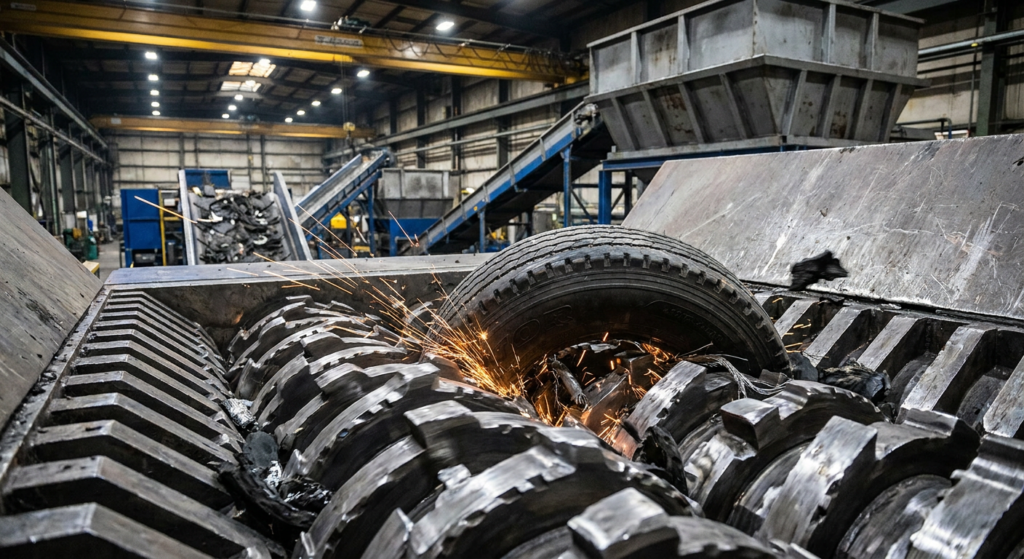
Quick Answer: Balance hardness (wear resistance) against Charpy impact toughness rather than maximizing HRC alone—DC53 at 58–60 HRC delivers roughly double D2’s impact toughness for contaminated tire/ELV streams, while a documented real-world case shows that fracture at mounting-hole geometry, not material hardness, is often the true root cause. Scope: This guide focuses primarily on primary and pre-shredding […]
تحليل السبب الجذر لظاهرة غبار التقطيع: خشونة جانب الشفرة Ra، البنية المجهرية للكربيد، وتفاوتات الضبط.
These four principles form the engineering framework Maxtor Metal’s application team applies when qualifying circular slitting knives for zero-dust converting programs in flexible packaging, nonwoven, and specialty paper lines. In high-speed flexible packaging, technical textile, non-woven, and specialty paper converting, particulate contamination is a major cause of unscheduled line shutdowns. What plant operators frequently diagnose […]
إعادة تجليخ شفرات الشريط الصناعية: عتبات الشحذ، معايير التخريد، ونموذج تكلفة دورة الحياة
Quick Answer: Regrinding industrial strip blades is economical when: chipping depth is under 0.5 mm, remaining thickness is above 60–70% of nominal, and the estimated regrind cost is below 50% of a new replacement blade. The minimum safe stock removal is 0.010–0.015 in (0.254–0.381 mm) to clear the subsurface micro-fractured fatigue layer. Blades with radial cracks, […]
شفرات تحبيل البلاستيك من ميتالورجيا المساحيق M390 مقابل CPM S90V: اختيار الدرجة تحت ظروف التآكل العالي بألياف الزجاج
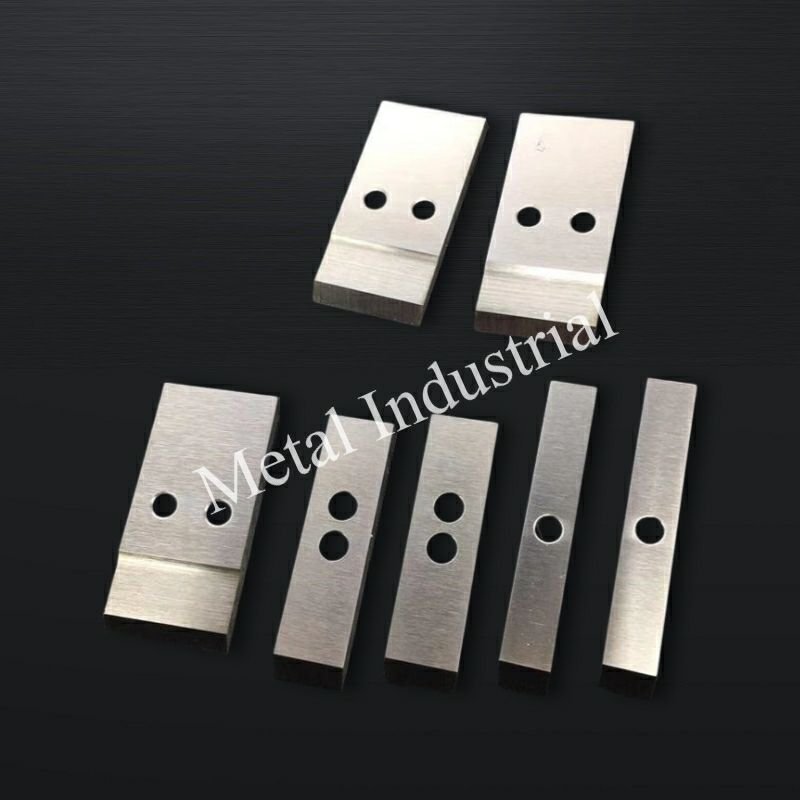
Quick answer: For pelletizing blades under high glass-fiber wear, powder metallurgy stainless steels outperform conventional tool steels because their fine, uniform carbide distribution resists micro-ploughing without the toughness trade-offs of high-alloy ingot steels. Between M390 and CPM S90V: choose CPM S90V when abrasion load is the dominant failure mode (>30% GF, neutral water); choose M390 when […]

 English
 Spanish
 Italian
 French
 Portuguese
 Russian
 German
 Arabic
 Hindi
 Vietnamese
 Indonesian
 Japanese
 Korean