

स्लिटिंग बर (slitting burr) में कमी उन "छोटी धार" वाली समस्याओं में से एक है जो तेजी से बड़ी लागत की समस्या बन जाती है: बर ग्राहकों की शिकायतों का कारण बनती है, डाउनस्ट्रीम फॉर्मिंग (downstream forming) की समस्याएं पैदा करती है, और चुपचाप चाकू के जीवन (knife life) को कम कर देती है।
यह हैंडबुक Maxtor Metal के टेक्निकल सपोर्ट स्पेशलिस्ट, Jerry Chu द्वारा संकलित की गई है, जो कार्बन स्टील, AHSS, स्टेनलेस और एल्युमिनियम को प्रोसेस करने वाली कॉइल स्लिटिंग लाइनों में 10 से अधिक वर्षों के फील्ड ट्रबलशूटिंग अनुभव पर आधारित है। इसे Maxtor Metal की एप्लीकेशन इंजीनियरिंग टीम द्वारा पीयर-रिव्यू किया गया है और इसे व्यावहारिक, सत्यापन-प्रथम (verification-first) दृष्टिकोण के साथ लिखा गया है, जहां सफल रणनीति अनुशासित सेटअप विंडो, त्वरित मूल-कारण अलगाव (root-cause isolation) और निरंतर माप है।.
यदि आपकी लाइन रोलर शियरिंग ब्लेड (या समकक्ष स्लिटिंग नाइफ सिस्टम) का उपयोग करती है, तो नीचे दिए गए सिद्धांत अभी भी लागू होते हैं: कट को एक नियंत्रित फ्रैक्चर/शियर घटना के रूप में मानें, फिर उन कुछ वेरिएबल्स को नियंत्रित करें जो वास्तव में बर (burr) का कारण बनते हैं। रोलर शियर टूलिंग के लिए विशिष्ट सामग्री चयन, क्लीयरेंस इंजीनियरिंग और विफलता मोड डायग्नोस्टिक्स (failure mode diagnostics) के लिए, Maxtor Metal की देखें रोटरी स्लिटिंग नाइफ और रोलर शियर ब्लेड इंजीनियरिंग गाइड.
इस हैंडबुक में क्या शामिल है
मूल कारणों (क्लीयरेंस/ओवरलैप, चाकू की स्थिति, अलाइनमेंट, गति, स्नेहन, तनाव) को अलग करके, सामग्री परिवार के अनुसार प्रारंभिक सेटअप विंडो को परिभाषित करके, और निरीक्षण, स्वीकृति बैंड और ROI ट्रैकिंग को मानकीकृत करके किनारे के बर (edge burr) को कम करने के लिए एक शॉप-फ्लोर और इंजीनियरिंग संदर्भ। यह आपके ग्राहक के प्रिंट (ड्राइंग) विनिर्देशों का विकल्प नहीं है — इष्टतम मापदंडों तक तेज़ी से पहुँचने के लिए इसका उपयोग करें, फिर अपनी स्वयं की प्रक्रिया क्षमता (process capability) के विरुद्ध सत्यापित करें।
यह किसके लिए है
विभिन्न ग्रेडों और मोटाई के दौरान स्लिट गुणवत्ता को ट्यून करने वाले प्रोसेस इंजीनियर्स; आर्बर स्थिति (arbor condition), रनआउट (runout), और स्टैक अखंडता के लिए जिम्मेदार रखरखाव प्रमुख; किनारे की गुणवत्ता के साथ अपटाइम को संतुलित करने वाले उत्पादन प्रबंधक; टूलिंग, स्पेसर्स और रीग्राइंड अर्थशास्त्र (regrind economics) का मूल्यांकन करने वाली तकनीकी खरीद टीम।
लाइव लाइन पर इसका उपयोग कैसे करें: सबसे पहले माप अनुशासन (measurement discipline) की पुष्टि करें → कुछ भी बदलने से पहले सबसे संभावित कारण की पहचान करने के लिए मूल कारण मैट्रिक्स (root-cause matrix) का उपयोग करें → शुरुआती बिंदु के रूप में सामग्री सेटअप विंडो को लागू करें, फिर छोटे वेतन वृद्धि में ट्यून करें → किसी भी बदलाव के बाद, एक छोटी सत्यापन पट्टी (verification strip) चलाएं और फिर से मापें।
ट्रैक करने के लिए प्रमुख मेट्रिक्स
स्ट्रिप की मोटाई के % के रूप में बर की ऊंचाई (और/या पूर्ण ऊंचाई जब ग्राहक इसे निर्दिष्ट करता है) · चौड़ाई सहनशीलता और बहाव (संचयी स्पेसर्स/स्टैक त्रुटि सहित) · अपटाइम / OEE प्रभाव (सेटअप समय, परिवर्तन, अनियोजित रोक) · टूल जीवन (प्रति रीग्राइंड टन, प्रति सेट टन, और विफलता मोड: घिसाव बनाम सूक्ष्म-चिपिंग)।
मुख्य निष्कर्ष: बर (burr) में सुधार जिसे लॉग नहीं किया जाता है और प्रिंट (ड्राइंग) के खिलाफ सत्यापित नहीं किया जाता है, वह टिकाऊ नहीं रहेगा।
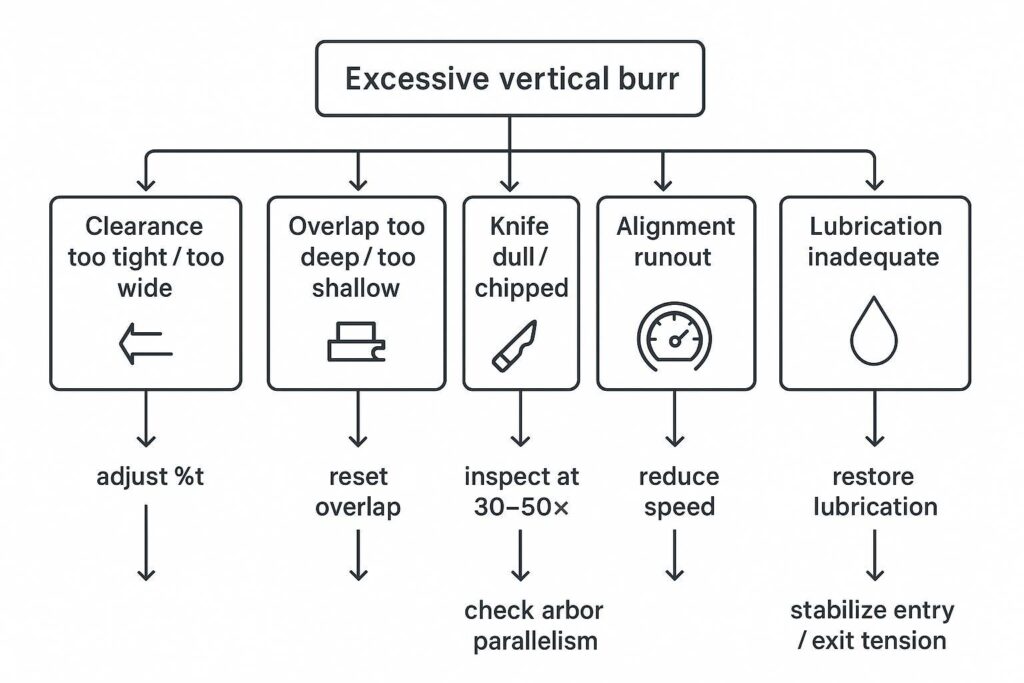
स्लिटिंग बर में कमी के लिए मूल कारण मैट्रिक्स
क्लीयरेंस और ओवरलैप त्रुटियां
यहाँ से शुरू करें क्योंकि हॉरिजॉन्टल क्लीयरेंस और वर्टिकल ओवरलैप अक्सर सबसे अधिक प्रभावी और परीक्षण करने में सबसे तेज़ वेरिएबल्स होते हैं। व्यावहारिक उद्योग मार्गदर्शन लगातार बर (burr) को गलत क्लीयरेंस और अत्यधिक ओवरलैप से जोड़ता है।.द फैब्रिकेटर (The Fabricator): “हाउ टू अवॉइड स्लिट-इन कॉइल स्लिटिंग प्रॉब्लम्स” (2006)
क्या जांचें (क्रम में):
- हॉरिजॉन्टल क्लीयरेंस (%t): बहुत टाइट होने से किनारा रगड़/रोल हो सकता है; बहुत चौड़ा होने से शियर होने के बजाय फट सकता है। (अक्सर इसे स्लिटिंग नाइफ क्लीयरेंस प्रतिशत.)
- वर्टिकल ओवरलैप: बहुत गहरा होने से बर (burr) और किनारे की क्षति बढ़ जाती है; बहुत उथला होने से कट अस्थिर हो सकता है। (आपका स्लिटिंग ओवरलैप सेटिंग भी %t जितना ही महत्वपूर्ण है।)
- बर साइड बायस (Burr side bias): एक किनारे पर अधिक बर (burr) होना अक्सर अलाइनमेंट/स्टैक की समस्याओं की ओर इशारा करता है, न कि केवल “गलत %t” की ओर।”
सुधारात्मक उपाय (Corrective levers):
- क्लीयरेंस को एक सामग्री-आधारित प्रारंभिक सीमा (सामग्री के अनुसार सेटअप विंडो देखें) पर रीसेट करें।.
- जब गहराई के साथ बर (burr) बढ़ता है, तो छोटे चरणों में ओवरलैप को कम करें।.
- यदि स्ट्रैंड्स में बर (burr) का पैटर्न असंगत है, तो स्टैक समरूपता (stack symmetry) और स्पेसर की स्थिति की पुन: जांच करें।.
For the full mechanics behind overlap-to-clearance coordination — including burnish/break ratio interpretation, material-specific penetration windows, and arbor positioning best practices — see the rotary knife overlap settings guide.
विफलता मोड (Failure modes) जो बताते हैं कि आप गलत उपाय अपना रहे हैं:
- बर (burr) थोड़ी देर के लिए कम होता है लेकिन कुछ ही मिनटों में वापस आ जाता है → नाइफ एज की स्थिति या मलबे/गर्मी की समस्या।.
- कम गति पर बर (burr) ठीक है लेकिन उत्पादन गति पर विफल हो जाता है → तनाव स्थिरता (tension stability), स्नेहन (lubrication), या गतिशील अलाइनमेंट (dynamic alignment)।.
नाइफ की तीक्ष्णता (sharpness), ज्यामिति (geometry), और कोटिंग्स
बर (burr) अक्सर नाइफ की स्थिति की समस्या होती है जो सेटअप समस्या के रूप में छिपी होती है।.
क्या जांचें:
- एज रेडियस ग्रोथ (Edge radius growth) (मंद होना) और माइक्रो-चिपिंग (micro-chipping) (विशेष रूप से AHSS/स्टेनलेस पर)।.
- ज्यामिति स्थिरता (Geometry consistency) पूरे सेट में (बेवल समरूपता, फेस रनआउट)।.
- गॉलिंग / पिकअप (Galling / pickup) स्टेनलेस या एल्युमिनियम पर (यह “अचानक बर” आने का एक सामान्य कारण है)।.
सुधारात्मक उपाय (Corrective levers):
- समय रहते निरीक्षण को पहले करें: गुणवत्ता खराब होने से पहले किनारों की जांच करें।.
- “घिसाव-जनित बर” (wear-driven burr) को “चिप-जनित बर” (chip-driven burr) से अलग करें: घिसाव धीरे-धीरे बढ़ता है; चिप्स अचानक बदलाव लाते हैं।.
- विफलता मोड (गॉलिंग बनाम अपघर्षक घिसाव) से जुड़े कोटिंग लॉजिक का उपयोग करें।.
अलाइनमेंट, गति, स्नेहन (lubrication), और तनाव (tension)
यदि क्लीयरेंस/ओवरलैप सीमा के भीतर है और नाइफ अच्छे दिख रहे हैं, तो अगला स्तर यह है कि “लाइन कट को विस्थापित कर रही है।”
क्या जांचें:
- संरेखण: आर्बर पैरेललिज्म (arbor parallelism), नाइफ फेस रनआउट, गाइड और सेपरेटर सेंटरिंग।.
- रफ़्तार: यदि गति के साथ बर (burr) गैर-रैखिक रूप से बढ़ता है, तो गर्मी, कंपन और स्ट्रिप नियंत्रण की जांच करें।.
- स्नेहन: द्रव अनुप्रयोग (fluid application) को एक प्राथमिक एज कंट्रोल वेरिएबल के रूप में मानें। एल्युमिनियम और स्टेनलेस स्लिटिंग के लिए, फेल्ट पैड या मिस्ट नोजल के माध्यम से लगाए जाने वाले हल्के सिंथेटिक तेल या वैनिशिंग तेल घर्षण को कम करते हैं और नाइफ के फेस पर सामग्री के जमाव (गॉलिंग) को रोकते हैं। भारी कार्बन स्टील्स पर, बाउंड्री लुब्रिकेंट्स शियर-ज़ोन की घर्षण गर्मी को नष्ट करते हैं जो अन्यथा नाइफ एज के थर्मल सॉफ्टनिंग को तेज करती है।.
- तनाव: unstable entry/exit tension can distort strip, drive flutter, and produce edge damage.
Reference point: an industry association bulletin notes burr height can be minimized by attention to slitter rigidity, horizontal/vertical clearance, and resharpening discipline (Australian Steel Institute, Technical Bulletin TB-F2).
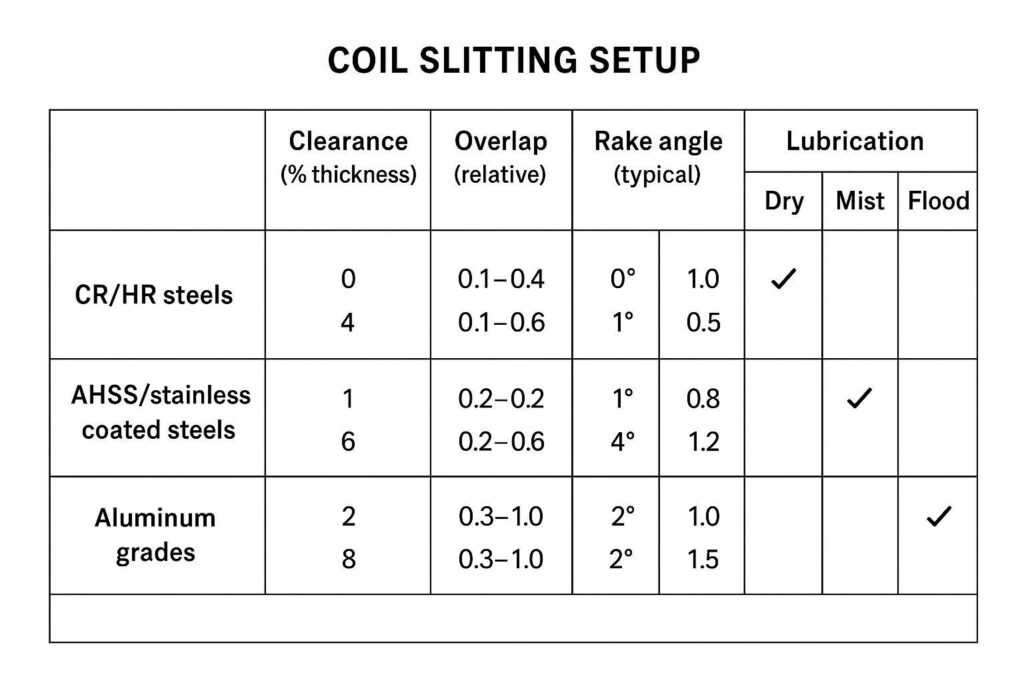
सामग्री के अनुसार सेटअप विंडो
These are starting windows to shorten setup time and reduce trial-and-error. Always validate against your customer print and your line’s stiffness, knife diameter, and arbor condition. If you need the keyword-friendly phrasing: this section is your practical slitting setup window by material.
| Material Group | Horizontal Clearance (%t) | Vertical Overlap (mm / in) | Key Focus Areas |
|---|---|---|---|
| CR / HR Carbon Steel | 8% – 12% t (Mid-grade: ~10% t) | +0.25 mm to +0.50 mm (+0.010″ to +0.020″) | Balance shear-to-break ratio; avoid excessive overlap |
| AHSS / Stainless Steel | 10% – 15% t (High tensile: ~12% t) | +0.10 mm to +0.30 mm (+0.004″ to +0.012″) | Prevent micro-chipping; monitor edge radius & galling |
| Aluminum & Soft Alloys | 5% – 8% t (Tight alignment required) | +0.05 mm to +0.20 mm (+0.002″ to +0.008″) | Anti-galling coatings (DLC); prevent pickup & galling |
CR/HR steels
Starting intent: stable shear zone with minimal tearing.
Standard carbon steels feature balanced ductility and tensile strength, allowing a traditional 1/3 shear and 2/3 break edge ratio. Operating within 8%–12% t clearance achieves a clean fracture transition without excessive edge rolling or deep tearing.
- Clearance: start mid-window (~10% t), then tune toward minimum burr.
- Overlap: moderate; avoid “deep overlap as insurance.”
- Speed: increase only after burr is stable at low-to-mid speed.
- Lubrication: use consistent lubrication strategy to prevent heat-driven edge degradation.
Practical note: ASI’s TB-F2 bulletin illustrates that recommended clearances vary by need (general production vs minimum burr) and highlights that optimum clearance reduces burr.Australian Steel Institute Technical Bulletin TB-F2 (Shearing and slitting steel sheet and strip)
प्रो टिप: When you widen the window for throughput, document what you changed (clearance, overlap, speed, tension). Otherwise your next “same material” run won’t actually be the same.
AHSS, stainless, and coated steels
Starting intent: prevent chipping and edge cracking while maintaining burr control.
High-tensile AHSS and work-hardening stainless steels exhibit extreme yield strengths and low elongation. Wider clearance (10%–15% t) is critical to relieve peak side-thrust forces on the knife edge, preventing micro-chipping while accommodating the abrupt shear fracture characteristic of high-strength alloys.
- Clearance: keep within a controlled window (~12% t); avoid extremes.
- Overlap: conservative; too deep can spike edge damage.
- Knife condition: inspect more frequently; micro-chips matter.
- Lubrication: treat as critical—pickup and heat are common triggers.
- Tension: prioritize stability over maximum throughput.
Aluminum grades
Starting intent: prevent pickup/galling and protect edge finish.
Aluminum and soft non-ferrous alloys possess high ductility and a strong tendency toward material adhesion (galling). A tighter clearance (5%–8% t) prevents the soft strip from dragging and folding over the knife edge, which would otherwise form heavy, continuous roll-over burrs.
- Clearance: typically tighter than steels (5%–8% t), but only when alignment is proven.
- Overlap: conservative; avoid unnecessary depth.
- Lubrication: ensure the method matches the alloy and surface requirements.
- Knife surface condition: watch for pickup—small deposits can produce large burr changes.
टूलिंग चयन और रखरखाव
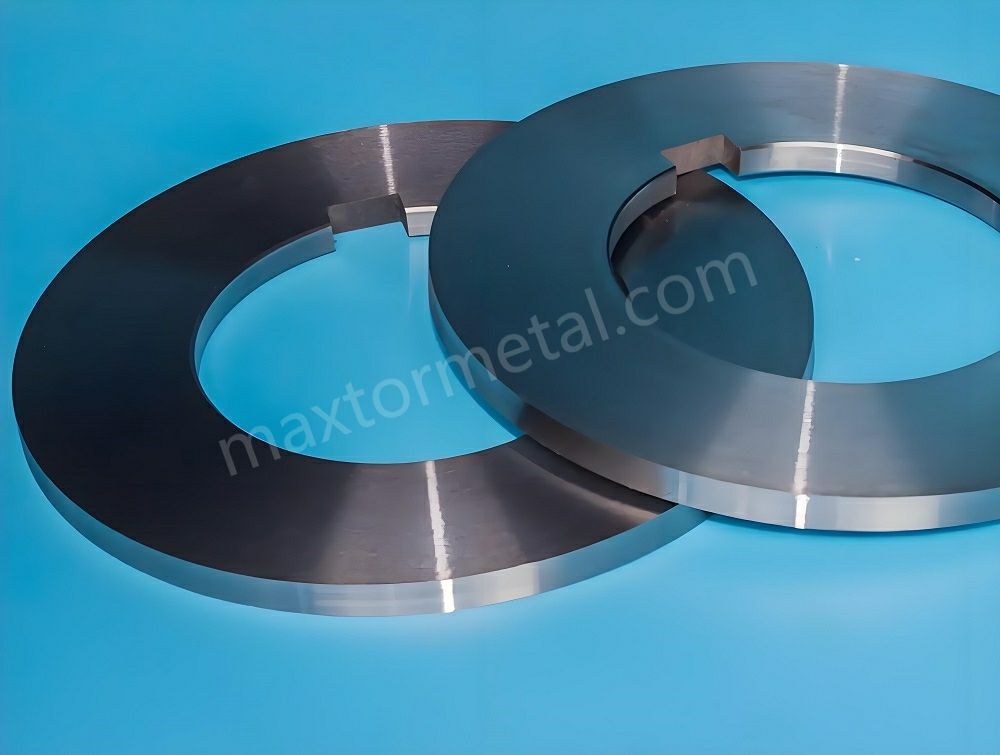
Knife steels and surface coatings
Maxtor Metal’s standard coating selection follows a failure-mode-first logic: डीएलसी is the default choice when galling and pickup are the primary risk (stainless steel, aluminum, and coated substrates); TiAlN is selected when abrasive wear and heat at the cutting edge dominate (high-speed AHSS processing, heavy-gauge carbon steel). For mixed-material lines, Maxtor Metal’s after-sales team typically recommends trialing one coating per failure mode on separate knife sets, then comparing tons-per-grind and edge condition trends over 3–5 production runs before standardizing.
Regrind intervals and edge inspection (30–50×)
A workable standard is to inspect at 30–50× magnification on a schedule that matches your burr tolerance and material severity.
To move from reactive grinding (sharpening only after burr complaints) to scheduled preventive maintenance, baseline your regrind frequency using practical tonnage thresholds:
| Material Severity | Typical Tonnage Interval (per Set) | Inspection Focus at 30–50× |
|---|---|---|
| Standard Carbon Steel (CR/HR) | Every 200 – 400 tons | Uniform edge radius growth (<0.03 mm) |
| AHSS / High-Strength Alloys | Every 100 – 180 tons | Micro-chipping, notch wear, edge breakdown |
| Stainless Steel / Aluminum | Every 120 – 250 tons | Metal pickup/galling, land face buildup |
What to standardize:
- Inspection triggers: first coil after changeover, after speed ramp, and when burr trends upward.
- Edge criteria: edge radius growth, micro-chips, pickup, and uneven wear.
- Regrind rule: regrind before burr becomes your “alarm,” not after.
What failure looks like:
- You only regrind after burr fails the customer spec → your process is reactive, not controlled.
Spacer accuracy and stack integrity
Spacer and stack control is a width-tolerance problem और a burr problem.
What to standardize:
- Spacer verification and traceability (measured thickness, wear history).
- Stack build procedure (cleanliness, torque discipline, consistent orientation).
- Periodic checks for cumulative error across multi-knife setups.
What failure looks like:
- Width drift over a run, plus burr variability strand-to-strand → stack integrity and runout are suspects.
For spacer tolerance specifications, rubber ring compression targets, and a rebuild checklist template, see the precision slitting spacers and rubber rings guide.
अलाइनमेंट और तनाव नियंत्रण

Arbor parallelism and runout checks
If your arbors are not parallel or runout is uncontrolled, clearance becomes “different at every angle.”
Practical checks:
- Measure runout on relevant surfaces (arbor, knife face seating).
- Confirm parallelism across the working width.
- Re-check after maintenance events and after any tooling crash.
For a structured runout verification procedure — covering dial indicator setup, TIR acceptance tiers, and blue-check protocol — see the OEM स्लिटर नाइफ ब्लूप्रिंट: स्पिंडल फिट ऑडिट, ISO टॉलरेंस और TIR गेट्स.
Passline, guides, and separator setup
Poor strip guidance can add lateral forces that change the effective cut.
Setup focus:
- Guides centered and consistent across the line.
- Separators aligned to prevent edge contact that creates secondary burr.
- Confirm the strip is not being “steered” into the knives.
Entry/exit tension and recoiler settings
Tension instability can look like a knife problem.
मानकीकरण हेतु नियंत्रण:
- Entry/exit tension setpoints by grade and thickness.
- Procedures for speed changes (ramp rates) that don’t induce strip flutter.
- Clear rules for when to prioritize burr control over throughput.
माप, स्वीकृति और ROI ट्रैकिंग
Burr measurement and logging
To reduce burr reliably, define measurement like a process parameter:
- Where to measure (edge location and distance from coil start/end)
- Sampling frequency (per coil, per slit, per changeover)
- Method (microscope, optical measurement, or profilometry) and operator training
Log at minimum:
- material grade, thickness, coating
- clearance (%t) and overlap setting
- knife set ID, regrind count, inspection findings
- line speed, lubrication mode, tension setpoints
- burr height results (and scrap/rework events)
Acceptance bands and documentation
Align your acceptance bands to the customer print—not tribal knowledge.
For drawing/spec language, ISO 13715 is the primary international reference for indicating and dimensioning edges of undefined shape (including burr/undercut indications) on technical documentation. Industry practice guidance from major manufacturing and steel industry associations consistently emphasizes establishing clear edge condition tolerances prior to production runs.
Practical approach:
- Convert the customer requirement into a measurable acceptance band (absolute or %t).
- Include side designation when relevant (which side burr is acceptable on).
- Keep records auditable: who measured, what method, what calibration state.
If your team uses a rebuild checklist and burr trend log as part of this process, Maxtor Metal’s slitting spacers and ring rebuild template set provides a ready-to-use format.
ROI/TCO templates and baselining
Burr reduction pays back when it reduces total cost per ton, not only when the edge “looks better.” Baseline before you change anything:
- Scrap and rework cost attributable to edge quality
- Downtime minutes from changeovers and unplanned stops
- Knife cost per ton (including regrinds and expedited orders)
- Customer returns/chargebacks tied to burr or edge condition
Then track deltas after you apply setup windows:
- Burr compliance rate (first-pass yield)
- Tons per grind and tons per knife set
- Setup time per changeover
If you’re building a knife material ROI case alongside setup window improvements, the rotary slitter knife ROI guide provides a cost-per-ton model covering PM-HSS vs tool steel trade-offs for AHSS, stainless, and aluminum.
Case Study: Automotive Stamping Supply Line Burr Reduction
A Tier-1 automotive coil slitting facility processing 1.5mm AHSS (DP780) experienced recurring edge burr exceeding 12% of material thickness, resulting in high customer reject rates and frequent knife micro-chipping.
By implementing the setup window and inspection protocol developed with Maxtor Metal’s technical support team — covering clearance/overlap reset, magnification-based inspection scheduling, and first-article verification discipline:
- Parameter Adjustment: Re-set horizontal clearance from an uncontrolled 18% t to a disciplined 11% t, and reduced vertical overlap from +0.60 mm to +0.20 mm.
- Knife Care: Shifted from post-failure grinding to 40× magnification optical inspection after every 150 tons.
- परिणाम: Average burr height dropped from 0.18 mm (12% t) को <0.05 mm (3.3% t), meeting ISO 13715 specs. Tons per regrind increased by 42%, and annual edge-defect scrap cost was reduced by an estimated $30,000–$45,000 (based on material cost and reject rate data provided by the facility; anonymized and range-normalized).
- सीमाएँ: These results were observed under stable incoming coil flatness and arbor runout below 0.010 mm. Lines with worn bearings, uncontrolled tension, or mixed operator discipline may see smaller gains from setup window changes alone.
FAQs:
Q: कॉइल स्लिटिंग लाइन पर बर (burr) को कम करने का सबसे तेज़ तरीका क्या है?
A: क्षैतिज निकासी (horizontal clearance) और लंबवत ओवरलैप (vertical overlap) से शुरुआत करें, फिर 30–50× पर चाकू की धार की स्थिति की जांच करें। यदि बर की मात्रा गति के साथ बदलती है, तो तनाव की स्थिरता और स्नेहन (lubrication) की जांच करें।
Q: मुझे स्लीटर चाकू निकासी (slitter knife clearance) प्रतिशत किस स्तर से शुरू करना चाहिए?
A: सामग्री-आधारित शुरुआती विंडो का उपयोग करें (एक निश्चित % नहीं)। विंडो के मध्य से शुरुआत करें, एक छोटी सत्यापन पट्टी चलाएं, फिर बर की ऊंचाई दर्ज करते हुए छोटे वेतन वृद्धि में ट्यून करें।
Q: क्या अधिक लंबवत ओवरलैप (vertical overlap) हमेशा बर (burr) को कम करता है?
A: नहीं। अत्यधिक ओवरलैप से बर बढ़ सकता है और किनारे को नुकसान पहुँच सकता है। ओवरलैप को एक नियंत्रित चर (variable) के रूप में मानें और यदि गहराई बढ़ने के साथ बर बढ़ता है तो इसे कम करें।
Q: मैं लगातार बर की ऊंचाई (burr height) को कैसे मापूं?
A: एक परिभाषित विधि (माइक्रोस्कोप/ऑप्टिकल/प्रोफाइलोमीटर), निश्चित नमूनाकरण स्थान (sampling locations) और एक दोहराने योग्य लॉगिंग टेम्पलेट का उपयोग करें। जब ड्राइंग अनुमति दे, तो बर की ऊंचाई को मोटाई के % के रूप में रिपोर्ट करें।
Q: एक कटे हुए किनारे पर बर (burr) दूसरे की तुलना में अधिक खराब क्यों होता है?
A: यह पैटर्न अक्सर अलाइनमेंट, रनआउट (runout), या स्टैक/स्पेसर्स मुद्दों की ओर इशारा करता है जो असमान निकासी (uneven clearance) पैदा करते हैं। आर्बर समानता, चाकू की सीटिंग और स्पैसर सटीकता की पुन:-जांच करें।
Q: स्लीटर चाकू (slitter knives) की कितनी बार जांच और रीग्राइंड (reground) किया जाना चाहिए?
A: 30–50× आवर्धन (magnification) का उपयोग करते हुए, अपनी बर सहनशीलता (burr tolerance) और सामग्री की गंभीरता से जुड़ी समय सारणी के अनुसार जांच करें। बर के अलार्म स्थिति बनने से पहले रीग्राइंड करें।
Q: स्टेनलेस या एल्यूमीनियम स्लिटिंग पर गॉलिंग (galling/चिपकने) को रोकने के लिए सबसे अच्छा कोटिंग कौन सा है?
A: एंटी-गॉलिंग/पिकअप जोखिम के लिए आमतौर पर DLC कोटिंग को चुना जाता है; अपनी स्नेहन (lubrication) और गति स्थितियों के तहत पिकअप, बर के रुझान और प्रति रीग्राइंड टन (tons-per-grind) की निगरानी करके इसे सत्यापित करें।
Q: मैं ऑपरेशन्स और खरीद (procurement) टीमों को बर में कमी के ROI को कैसे साबित करूं?
A: स्क्रैप/रीवर्क, डाउनटाइम और प्रति टन चाकू लागत का एक बेसलाइन डेटा तैयार करें, फिर निश्चित सेटअप विंडो और सुसंगत माप अनुशासन का उपयोग करके एक नियंत्रित परीक्षण के साथ इसकी तुलना करें।
निष्कर्ष
- Summarize diagnostic priorities and parameter windowsDiagnostic priority is simple: (1) clearance/overlap, (2) knife condition, then (3) alignment/tension/lubrication. Use the setup windows as starting ranges, tune with small changes, and avoid simultaneous multi-variable “guessing.”
- Reinforce measurement discipline and verification against customer printsBurr control only holds if you measure it the same way every time and verify acceptance against the customer print language—especially when edges are specified using formal indication practices such as ISO 13715 (as described in the Acceptance bands section above).ISO 13715:2017 — ISO catalog page
- Next steps: pilot runs, data logging, and continuous improvementRun a short pilot on one representative grade, lock the logging fields, and convert your best settings into a controlled setup window.This is also where Maxtor Metal‘s after-sales support fits most naturally: if you want a second opinion on your regrind interval, coating selection, or clearance window for a specific material, Maxtor Metal’s technical support team can review your current setup parameters and edge inspection findings — and provide documented recommendations tied to your material grade, line speed, and knife geometry.Keeping tooling decisions, regrind intervals, and acceptance bands tied to the same dataset is how improvements survive operator changes and material mix shifts.
Author & Technical Reviewer
जेरी चू
Technical Support Specialist, After-sales Service | Maxtor Metal
Jerry Chu is Technical Support Specialist at Maxtor Metal, with over 10 years of coil slitting troubleshooting experience across carbon steel, AHSS, stainless, and aluminum processing lines. His field work focuses on root-cause isolation for burr and edge quality failures — translating setup window discipline, knife inspection protocols, and regrind scheduling into measurable reductions in scrap, rework, and unplanned downtime. The diagnostic framework and setup windows in this handbook reflect the approach Jerry applies in Maxtor Metal’s after-sales technical support engagements. Certifications: PMP (Project Management Professional), CMRP (Certified Maintenance & Reliability Professional).

 English
 Spanish
 Italian
 French
 Portuguese
 Russian
 German
 Arabic
 Hindi
 Vietnamese
 Indonesian
 Japanese
 Korean