

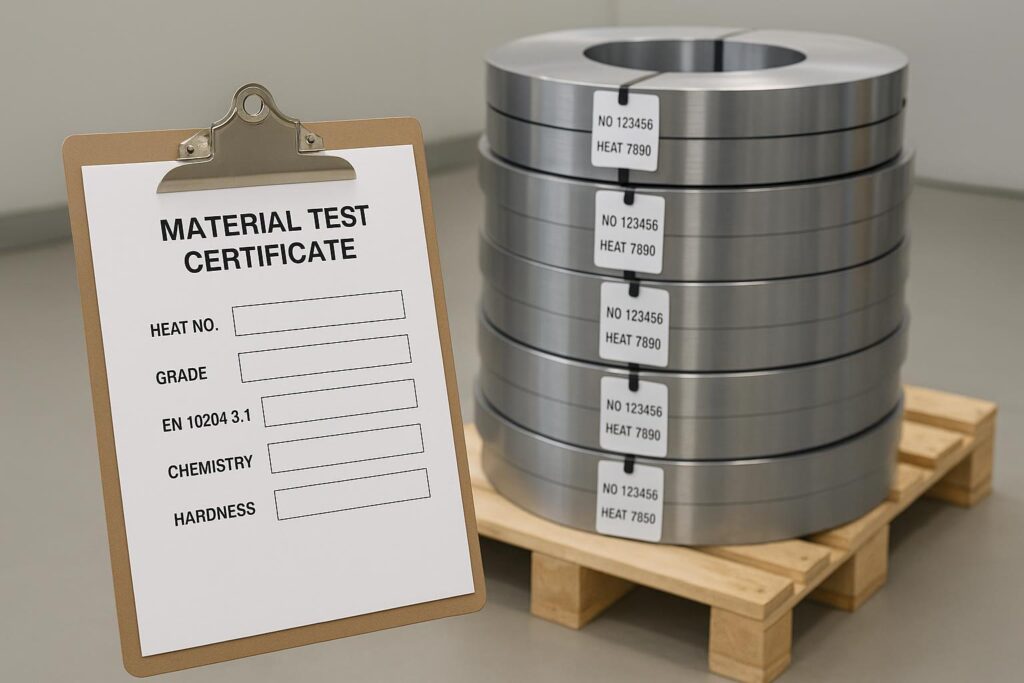
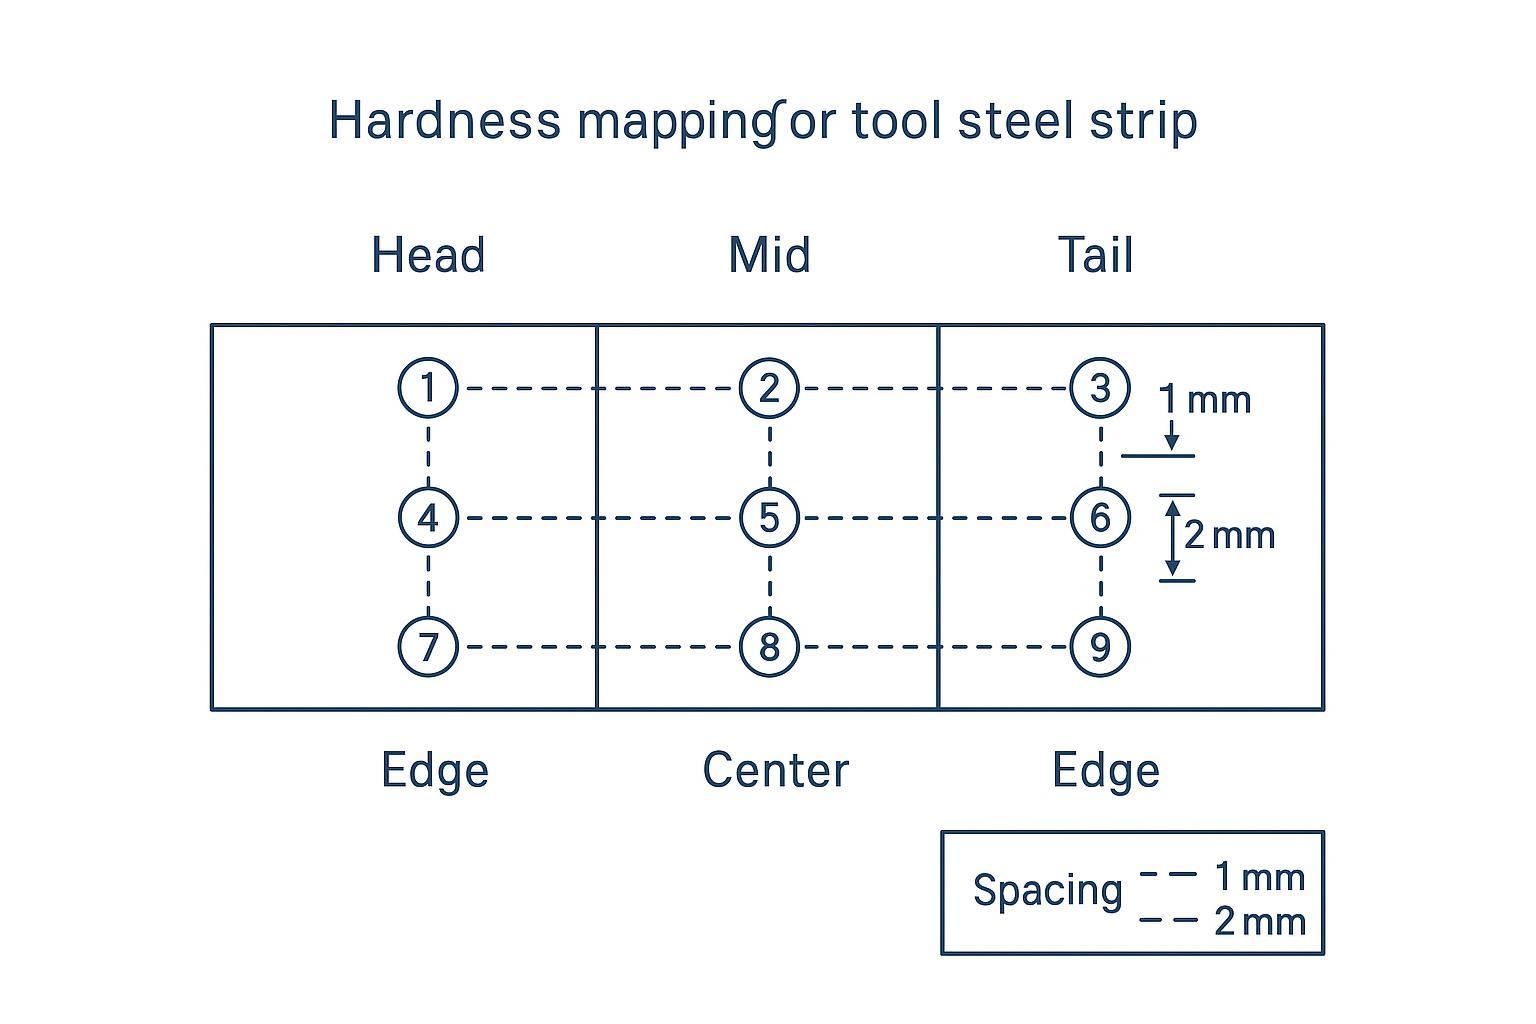
Risposta rapida: Per leggere un MTC dell'acciaio per utensili per lame per nastri, iniziare dall'intestazione: confermare il tipo di certificato EN 10204 3.1, l'identità del fornitore, il grado dell'acciaio e il numero di colata. Quindi, verificare incrociando la tabella chimica con l'ordine d'acquisto o le specifiche (utilizzando ASTM A681 o ISO 4957 come standard di riferimento). Verificare l'uniformità della durezza con una mappatura a 9 punti (testa/centro/coda × bordo/centro/bordo secondo ASTM E18) e aggiungere un controllo della decarburazione (ASTM E1077) quando le prestazioni del tagliente sono critiche. Il numero di colata deve collegare il MTC, l'etichetta del coils e i registri di lotto interni per formare una catena di tracciabilità completa.
In strip-blade manufacturing, a tool steel MTC is only useful if it helps you make a fast, defensible receiving decision—and if you can still prove traceability after the coil has been slit, ground, and converted into internal lots. This practical checklist is prepared by the Maxtor Metal QA & Metallurgical Engineering Team, drawing on over 15 years of specialized experience in industrial blade manufacturing, custom steel selection, and strict quality control protocols when aligning paperwork, tagging, and verification between supplier and buyer.
- Scopo: consentire decisioni di accettazione rapide e affidabili per le lame a nastro
- Ambito: Focus su EN 10204 3.1 (certificato EN 10204 3.1), numero di colata, composizione chimica, uniformità di durezza
- Norme di riferimento: EN 10204, ASTM E18, ASTM E1077, ASTM A681/ISO 4957
- Perché la lettura del certificato di colata (MTC) dell'acciaio per utensili è fondamentale per QA, uptime e FPY
- Come questa checklist riduce test ripetuti, scarti e tempi di fermo macchina
Concetto chiave: Treat the MTC as the starting point for acceptance: it anchors traceability and declared results, but your receiving checks decide whether the coil is safe to process.
Concetti di base del certificato MTC
Cosa copre un certificato EN 10204 3.1
Un certificato di collaudo EN 10204 Tipo 3.1 è il formato comune di “certificato di collaudo / certificato del materiale” utilizzato nella fornitura di metalli. In parole semplici, è la dichiarazione del produttore che il prodotto consegnato è conforme all'ordine e include i risultati dei test associati all'unità di prova.
Questo è il certificato EN 10204 3.1 a cui fa infine riferimento il vostro sistema di tracciabilità.
Per le definizioni formali e i tipi di documenti, fare riferimento direttamente alla norma EN 10204:2004, disponibile tramite gli organismi di normazione ufficiali come BSI (EN 10204:2004) o l'ente di normazione locale. La norma definisce tutti i tipi di documenti (2.1, 2.2, 3.1, 3.2) e i requisiti di autorizzazione per ciascuno.
Checklist (nozioni di base del 3.1):
- EN 10204 3.1 risultati misurati.
- (non solo "conforme"). È firmato/convalidato.
- dal rappresentante di collaudo autorizzato del produttore. Numero di colata e collegamento di tracciabilità Per le lame a nastro, il numero di colata è la via più rapida per rispondere alla domanda: "Sappiamo esattamente cos'è questo coil?". È il fulcro della tracciabilità del numero di colata nella fornitura basata su coil. Deve collegare:.
l'MTC (composizione chimica dichiarata + test)
Checklist di ricezione (collegamento di tracciabilità):
- corrisponde a
- quello indicato sul cartellino del coil.
- L'identificativo del coil (n. coil, n. cartellino, n. bobina) viene registrato nel registro di ricezione.
- ereditano
1 vs 3.2 vs 2.2
- Utilizzate questo schema come scorciatoia decisionale: : dichiarazione di conformità basata su controllo non specifico (adatta per usi a basso rischio; limitata per gli audit). : certificato di collaudo emesso dal produttore con i risultati dei test (base di riferimento tipica per gli acciai per utensili industriali).
- : certificato di collaudo con il coinvolgimento/presenza di una terza parte o del rappresentante dell'acquirente (da utilizzare quando richiesto dal rischio o dal contratto).
- Un MTC per acciaio per utensili non è "valido" solo perché elenca dei numeri, ma perché quei numeri corrispondono a quanto ordinato. Regola pratica di accett il numero di colata e mantenerlo associato durante il WIP.
1 vs 3.2 vs 2.2
Usa questo come scorciatoia decisionale:
- 2.2: dichiarazione di conformità basata su controllo non specifico (ottima per usi a basso rischio; limitata per gli audit).
- 3.1: certificato di collaudo emesso dal produttore con i risultati delle prove (linea di base tipica per gli acciai per utensili industriali).
- 3.2: certificato di collaudo con il coinvolgimento/presenza di una terza parte o del rappresentante dell'acquirente (da utilizzare quando il rischio o il contratto lo richiedono).
Come verificare la composizione chimica su un MTC dell'acciaio per utensili — e quando andare oltre il PMI
bande di accettazione D2/M2/O1
Un MTC di un acciaio per utensili non è “buono” perché elenca dei numeri: è buono perché i numeri corrispondono a quanto ordinato.
Regola pratica di accettazione:
- Le tue bande di accettazione dovrebbero derivare da quanto indicato nel tuo PO o nelle specifiche, che tipicamente fanno riferimento a una norma sui materiali per acciai per utensili come ASTM A681 O ISO 4957:2018.
| Grado | Carbonio (C) | Cromo (Cr) | Vanadio (V) | Molibdeno (Mo) | Tungsten (W) |
|---|---|---|---|---|---|
| D2 (1.2379) | 1.40 – 1.60% | 11.00 – 13.00% | 0.70 – 1.10% | 0.70 – 1.20% | — |
| M2 (1.3343) | 0.78 – 1.05% | 3.75 – 4.50% | 1.75 – 2.20% | 4.50 – 5.50% | 5.50 – 6.75% |
| O1 (1.2510) | 0.85 – 1.00% | 0.40 – 0.60% | 0.05 – 0.30% | — | 0.40 – 0.60% (optional) |
Reference source: ASTM A681 / ISO 4957 standard chemistry composition limits.
Checklist (chemistry acceptance):
- Grade is stated clearly (e.g., D2, M2, O1) and matches the PO.
- Chemistry table includes the critical alloying elements for that grade.
- Heat number on the chemistry report matches the heat number on the certificate header.
For a detailed framework on how material grade validation — including heat-treatment batch records and XRD-based retained austenite verification — is specified for blade strip steel at the incoming stage, see Validating 440C Dicer Replacement Blades at HRC 56–58.
Pro tip: For incoming coils intended for strip blades, set a “stop the line” rule for grade ambiguity (for example, ambiguous equivalents or missing grade designation). It’s almost always cheaper than chasing performance scatter later.
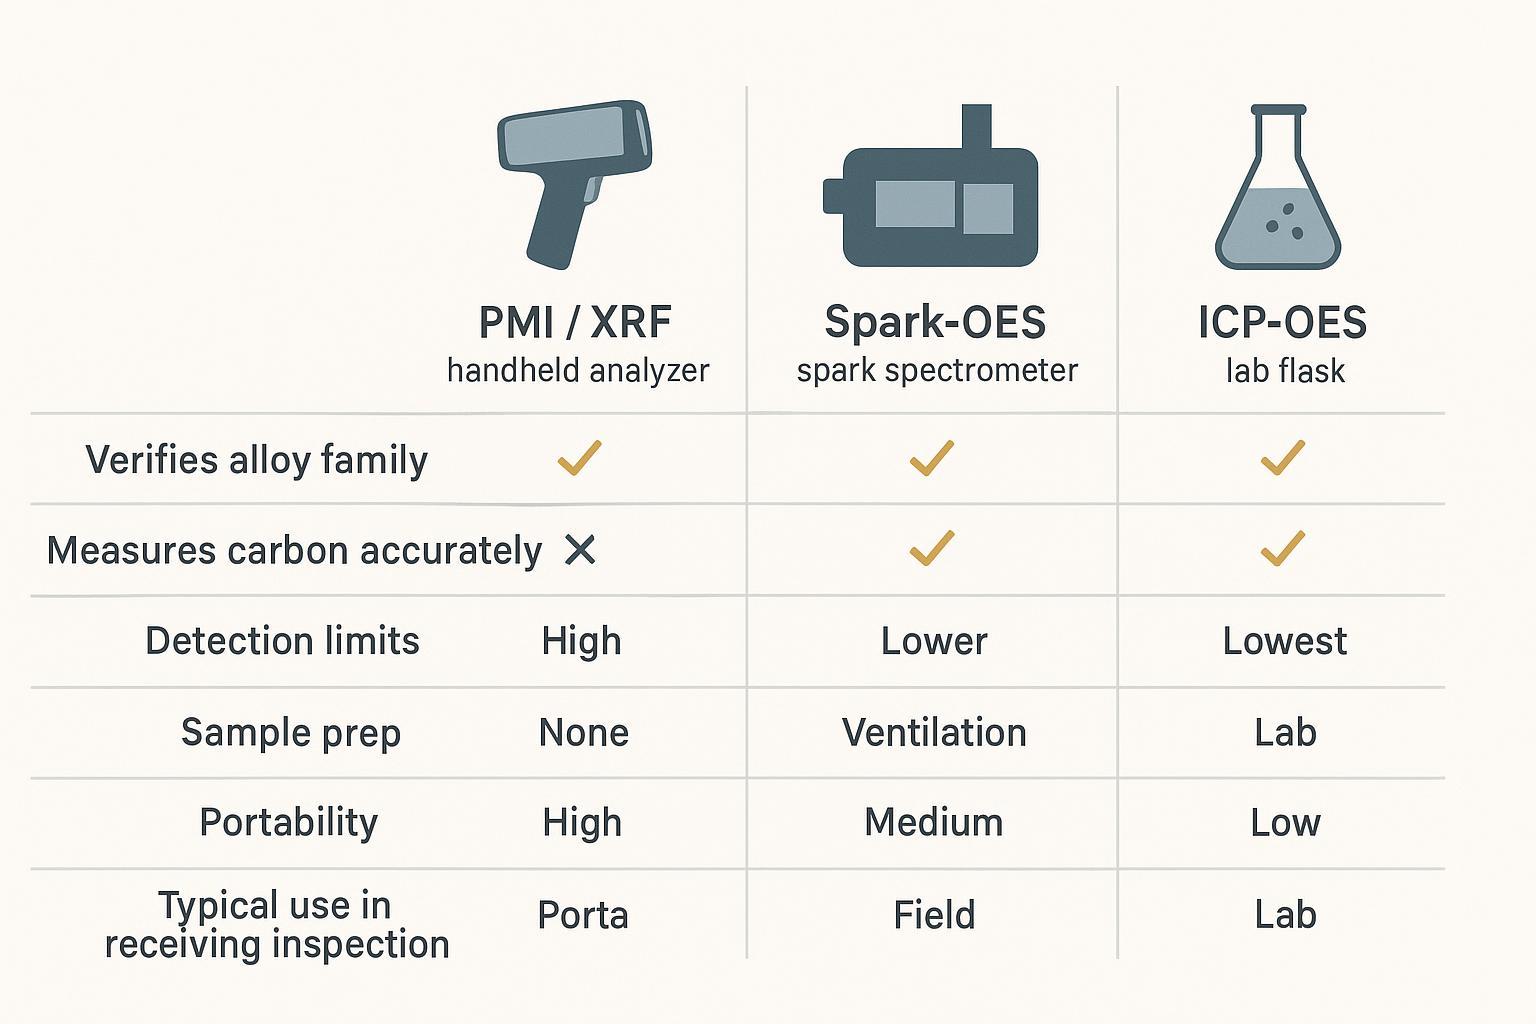
PMI vs spark-OES/ICP-OES
Positive Material Identification (PMI) is often treated as a universal answer. It isn’t.
- PMI/XRF is strong for confirming alloy family and many elements, but it’s limited for carbon.
- Spark-OES and ICP-OES are typically used when you need more complete chemistry, including carbon-critical acceptance decisions.
Checklist (use the right method):
- Use PMI/XRF to screen: “Is this broadly the correct alloy family?”
- Use spark-OES or ICP-OES when the acceptance hinges on carbon-sensitive outcomes (hardness response, carbide network behavior), or when the contract requires lab confirmation.
- Document the method and instrument ID in the receiving record so results are auditable.
Resolve discrepancies to PO/spec
When chemistry results conflict (MTC vs your test vs supplier re-test), the fastest way to avoid downtime is to follow a written escalation path.
Discrepancy-resolution checklist:
- Freeze the identity: confirm heat number + coil tag + sample location (head/mid/tail).
- Confirm the reference: pull the PO/spec revision and identify which standard governs (e.g., ASTM A681 / ISO 4957).
- Confirm methods: PMI vs OES vs ICP-OES; note detection limits and whether carbon was actually measured.
- Re-sample intentionally: take a second sample from a different location and document chain-of-custody.
- Decide action: accept, hold for disposition, downgrade use, or reject—based on the governing spec and risk.
Perché l'uniformità della durezza conta più della media — e come mapparla sul nastro
For Rockwell testing, cite the official method: ASTM E18 Rockwell hardness test method. For practical context on why thickness/support matter, NIST’s guidance is a useful companion: NIST Rockwell hardness recommended practice.
Supply condition: Annealed vs. Pre-hardened
Before evaluating hardness values, clarify the delivery state on the PO/MTC:
- Annealed strip (Soft): Shipped in a spheroidized annealed state for severe forming, slitting, or punching before final heat treatment.
- Pre-hardened / Hardened & Tempered strip: Delivered at working hardness for direct grinding, edging, or light slitting without subsequent full quenching.
| Grado | Annealed State (Max Hardness) | Pre-hardened / Heat Treated State (Working Range) |
|---|---|---|
| D2 | Max 255 HBW (~25 HRC) | 58 – 62 HRC |
| M2 | Max 269 HBW (~27 HRC) | 60 – 65 HRC |
| O1 | Max 229 HBW (~20 HRC) | 56 – 62 HRC |
Mixing up delivery conditions is a common source of false rejects and false accepts — always confirm with the MTC header what condition the material is in before applying any hardness acceptance limit.
Strip sampling map: edge–center–edge; head/mid/tail
Hardness scatter in strip often hides in two directions:
- Across the width (edge-to-edge differences from processing, decarb, or leveling)
- Along the length (head/mid/tail differences from heat treatment variation or coil-end effects)
Checklist (minimum map that still finds problems):
- Sample at head / mid / tail.
- At each length position, test edge / center / edge.
- Record location IDs so a future complaint can be traced back to the zone.
Setup validity: thickness, spacing, support
A hardness number is only actionable if the test setup is valid for the strip geometry.
Setup checklist:
- Confirm you are using a Rockwell scale appropriate for the strip thickness.
- Ensure the specimen is flat and well supported on the proper anvil; avoid rocking.
- Keep indentations far enough from edges and from each other to avoid interaction.
- If your strip is thin, don’t “solve it” by stacking layers—control the method instead.
Interpret spread and actions
Don’t just look at the average. Look at the spread.
Interpretation checklist:
- If head/mid/tail shift together, suspect batch heat treatment O process-window drift.
- If edges are consistently lower than center, suspect decarburization or edge conditioning effects.
- If one zone is off, isolate that zone in WIP routing (don’t blend lots).
Action checklist:
- Accept: hardness meets PO targets and spread is within your internal control limit.
- Hold / retest: hardness is borderline or spread suggests a localized issue.
- Reject / disposition: hardness is out of spec, or spread indicates non-uniformity that will create FPY loss.
Decarburazione e uniformità
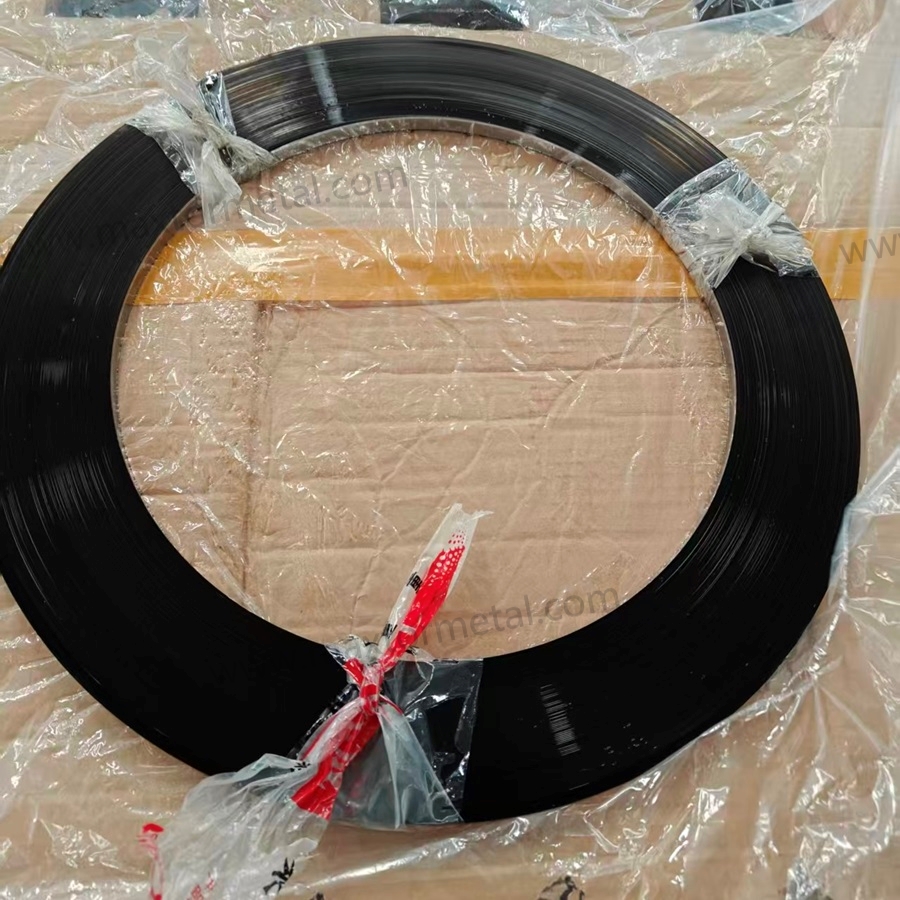
Detect and measure per ASTM E1077
If strip edges are soft, chip early, or don’t hold a stable grind, decarburization is a prime suspect—especially in thin sections where the surface zone is a larger fraction of the cross-section.
ASTM’s method for estimating decarb depth is ASTM E1077 — Standard Test Methods for Estimating the Depth of Decarburization of Steel Specimens.
Checklist (what to request/report):
- Sample location and orientation (edge vs center; head/mid/tail if relevant).
- Whether results are reported as total E partial decarburization depth.
- Metallography prep and etching method (so results are comparable across labs).
Impact on hardness and mitigation
Decarb turns into performance scatter because it shifts the hardness profile near the working surface.
Impact checklist:
- Softer surface zone → faster wear, unstable edge, unpredictable grinding response.
- Edge zone affected → failures show up as chipping or rapid dulling even when “bulk hardness” looks OK.
Mitigation checklist:
- Set decarb limits on the PO when the application is edge-sensitive.
- Control incoming verification for high-risk lots (new supplier, process change, unusual thickness).
- After secondary processing (slitting, grinding, heat treatment), re-verify hardness and surface condition before releasing to production.
SOP per la documentazione e la tracciabilità
Link MTC, coil tags, internal lots
A practical SOP connects physical identity to records so you can pass audits and also troubleshoot downtime quickly.
Checklist (minimum traceability chain):
- Archive the MTC PDF with a filename that includes supplier + grade + heat number.
- Photograph or scan the coil tag on receipt.
- Assign internal lot numbers that preserve the heat number association.
Nota tecnica: If your traceability SOP needs to align with coil supply format specifications — including reel dimensions, lot splitting conventions, and documentation requirements — see Maxtor Metal’s reference page on industrial blade strip steel in beveled reels for form-factor and traceability documentation standards.
If your traceability review also involves coil length planning and changeover scheduling, see OEE and Profit Gains from Reducing Coil Change Frequency for the supply-side consistency controls that make longer runs reliable.
Retest records and change control
Retests are unavoidable; uncontrolled retests are expensive.
Checklist (retest discipline):
- Record retest triggers (what failed, where, and why you retested).
- Store test method, instrument, operator, and sample location.
- Tie retest results to a disposition decision (accept/hold/reject) and keep the revision history.
- If the PO/spec changes, lock the revision used for acceptance of each lot.
Supplier collaboration for verification
Collaboration here doesn’t mean marketing—it means preventing “paper-compliant, performance-unstable” material from entering production.
Practical collaboration checklist:
- Align on what the 3.1 must include (heat no., grade/spec callout, chemistry, hardness where applicable).
- Agree on a discrepancy path: who re-tests, with what method, and how chain-of-custody is documented.
- Lock a shared definition of “equivalent grade” acceptance (or forbid it unless approved).
Maxtor Metal provides customers with pre-aligned documentation packages — including certificate format templates, coil tag conventions, and verification record structures — so that traceability decisions remain consistent after slitting, leveling, and lot splitting. Customers running formal incoming QA programs can request the documentation alignment checklist from the Maxtor Metal technical team before the first shipment.
Audit & Re-verification Triggers
To prevent quality issues from slipping into production, establish clear conditions that trigger a mandatory joint audit or secondary lab re-verification:
- New Supplier / Subcontractor First Lot: Mandatory complete chemistry (OES) and 9-point hardness mapping on the initial 3 production heats.
- Process Change Notification (PCN): Any declared change in supplier annealing, heat treatment furnace, or slitting line parameters.
- Consecutive Hardness or Microstructure Deviations: Occurrence of edge-to-center hardness scatter exceeding ±1.5 HRC across 3 consecutive coil lots.
- Unexplained Production Tooling Failures: Immediate joint root-cause review if field blades exhibit premature micro-chipping or rapid edge dulling despite “paper-compliant” MTCs.
When tooling failures trigger a root-cause review, the regrind decision framework provides the measurable inspection thresholds — chipping depth, remaining thickness, thermal burn criteria, and grinding economics — needed to determine whether a blade is recoverable or must be scrapped. See the Regrinding Industrial Strip Blades: Sharpening vs Scrap Guide for the full shop-floor protocol.
FAQs:
D: Come posso leggere rapidamente un MTC dell'acciaio per utensili per lame per nastri?
R: Inizia dall'intestazione: conferma il certificato EN 10204 3.1, il fornitore, il grado dell'acciaio e il numero di colata. Quindi, verifica che la tabella chimica corrisponda al tuo ordine d'acquisto/specifica e che il numero di colata sia collegato all'etichetta del coil. Infine, convalida l'uniformità della durezza con una semplice mappatura (testa/centro/coda × bordo/centro/bordo).
D: Qual è la differenza tra i certificati EN 10204 3.1 e 3.2?
R: Un certificato 3.1 viene rilasciato dal produttore con i risultati dei test ed è firmato da un rappresentante di ispezione autorizzato. Un certificato 3.2 aggiunge il coinvolgimento di un ente indipendente (terza parte o rappresentante dell'acquirente) in base ai requisiti contrattuali. Quando il rischio è più elevato o gli audit sono più rigidi, il certificato 3.2 viene utilizzato più di frequente.
D: Il PMI/XRF può verificare con precisione l'acciaio per utensili D2 o M2?
R: Il PMI/XRF è utile per confermare la famiglia di leghe e molti elementi leganti, ma presenta limiti per il carbonio. Se l'accettazione dipende da comportamenti sensibili al carbonio (risposta alla durezza, usura), utilizzare spark-OES o ICP-OES in base alle proprie SOP.
D: Quanti punti di prova di durezza Rockwell sono necessari su un coil in nastro d'acciaio?
R: Utilizzare una mappatura in grado di rilevare le variazioni sia in larghezza che in lunghezza: testa/centro/coda lungo il coil e bordo/centro/bordo attraverso la larghezza. Ciò fornisce nove punti come minimo pratico per il controllo dell'uniformità; aggiungere punti se la cronologia del processo mostra una dispersione localizzata.
D: Cosa causa la variazione di durezza dal bordo al centro sulle lame per nastri?
R: Le cause comuni includono differenze nelle condizioni superficiali, decarburazione vicino ai bordi e non uniformità di lavorazione. Il segnale tipico è spesso "bordi bassi, centro OK". Se si presenta questo schema, aggiungere un controllo della decarburazione e rendere più rigorosa la documentazione sulla localizzazione dei campionamenti.
D: A cosa serve la norma ASTM E1077 nel QA dell'acciaio per utensili?
R: La norma ASTM E1077 viene utilizzata per stimate la profondità di decarburazione nei campioni di acciaio. Nella pratica, supporta le decisioni di accettazione e le analisi delle cause radice quando la morbidezza superficiale compromette le prestazioni della lama, specialmente nei nastri sottili in cui la zona superficiale è più critica.
D: Cosa fare se la chimica del MTC è conforme ma la prova di durezza non supera il controllo?
R: Metti in fermo il lotto e verifica prima la validità del test (idoneità di scala e spessore, supporto, spaziatura e preparazione del campione). Se il test è valido, gestiscilo come una non conformità: preleva nuovi campioni con una catena di custodia documentata, confronta i dati con i requisiti del PO/specifica e stabilisci la destinazione del lotto (accettazione con riserva, declassamento o reso/scarto).
D: È necessario eseguire una nuova verifica dopo la taglio longitudinale (slitting) o la rettifica?
R: Sì, se tali fasi modificano la catena di tracciabilità (divisione del lotto) o alterano la superficie di lavoro. Riconfermare almeno la tracciabilità (dal numero di colata al lotto interno) e la durezza/condizione superficiale in base alla valutazione del rischio, in particolare dopo la rettifica o il trattamento termico.
Conclusione
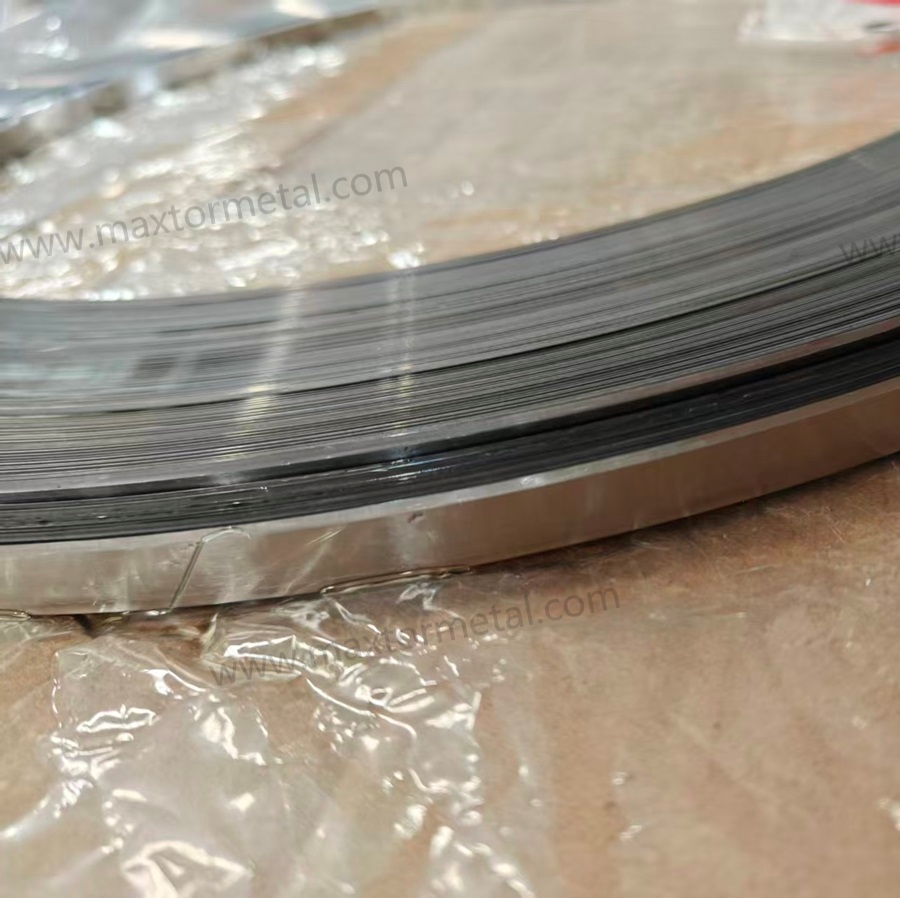
A clean checklist is only valuable if it reduces real waste: fewer retests, fewer surprises on the grinder, and fewer unplanned stops in production. The acceptance path covered in this guide comes down to four linked checks: confirm the EN 10204 3.1 certificate is correctly issued and signed; verify chemistry against PO/spec with the right method (PMI for screening, OES/ICP for carbon-critical decisions); map hardness at head/mid/tail × edge/center/edge and interpret the spread, not just the average; and verify decarburization depth when the application is edge-sensitive.
Traceability is what ties these checks together. If you can connect the MTC heat number to the coil tag, to your receiving log, and through to internal lot numbers after slitting or grinding—you have a defensible QA record. If any link in that chain is missing, you have paperwork, not traceability. Re-verify hardness and surface condition after any secondary process (slitting, grinding, heat treatment) that changes the working surface or splits the lot identity.
Consistent results require consistent identity. That’s the same internal discipline we apply at Maxtor Metal when aligning documentation and verification steps between supplier and buyer.
Author Bio
Jesse Xu
Senior Quality Engineer | Maxtor Metal (QA Department)
Jesse Xu is a Senior Quality Engineer at Maxtor Metal with over 15 years of hands-on experience in tool steel metallurgical quality assurance, material inspection, and failure analysis. Specializing in diagnosing complex blade performance issues—such as distinguishing heat treatment defects from material segregation in chipping and premature wear—he helps global equipment manufacturers ensure total quality from raw material receiving to finished precision cutting tools. Jesse holds prestigious industry credentials, including ASQ CQE (Certified Quality Engineer), Auditor capo ISO 9001, E ANT Livello II certifications.

 English
 Spanish
 Italian
 French
 Portuguese
 Russian
 German
 Arabic
 Hindi
 Vietnamese
 Indonesian
 Japanese
 Korean