スリット溝底におけるグリッド刃の折損防止策:R≥0.2 mm 設計に向けた溝底R半径、EDM放電加工面の健全性、および2回焼き戻し熱処理管理
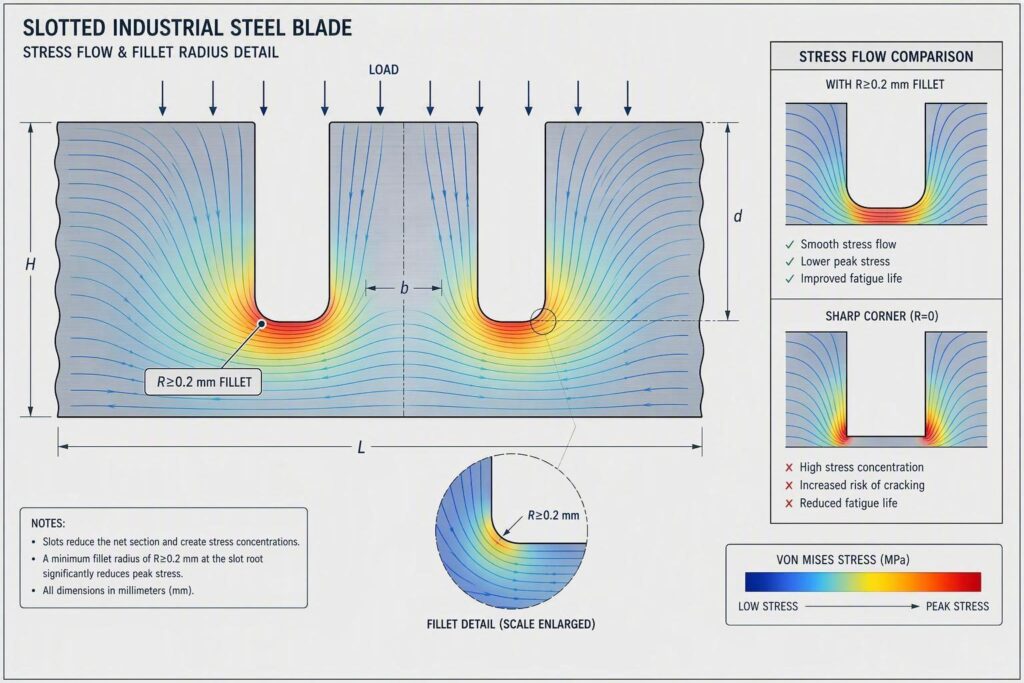
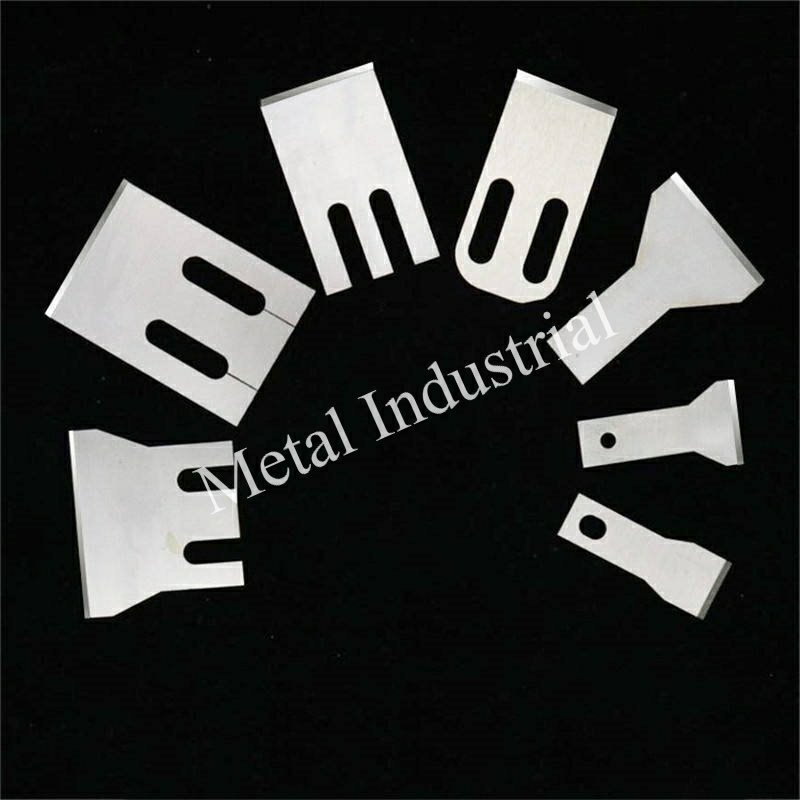
Quick Answer: Grid blade snapping at slot bottoms is caused by the coexistence of three factors: high elastic stress concentration (Kt 7–12 for sharp-cornered slots), surface defects that act as crack initiators (EDM recast layers, grinding burns), and insufficient toughness in the surrounding material. The primary engineering fix is to specify a slot fillet radius of R≥0.2 mm — which cuts Kt roughly in half compared to R0.05 mm geometry — combined with complete EDM recast removal via skim cuts and polishing, and a double-temper heat treatment matched to the specific steel grade. In a documented dicer grid blade case at HRC 56–58, controlling the slot-bottom radius to R0.20 mm […]
医療用ポリマー加工用ペレタイザーナイフの選定:420 vs 440Cステンレス、表面仕上げ、水循環制御の最適化
Quick answer: In medical-grade polymer pelletizing, 420 and 440C stainless are not interchangeable: 420 offers higher toughness, better polishability, and more corrosion tolerance in sanitization-intensive or variable-chemistry water loops; 440C delivers superior edge retention for abrasive polymers in stable, controlled-chemistry loops. Both grades require Ra ≤ 0.4 µm mirror finish and verified passivation per ASTM A967 — surface engineering, not alloy grade alone, is the primary contamination-prevention control. Black specks in medical pellets are most often a system problem: corrosion debris from the water loop and wear fragments from an underspecified knife acting together. Black specks in medical-grade polymer pellets rarely have a single source. Production teams often attribute them […]
シャーブレード刃こぼれの根本原因解析:破面解析(フラクトグラフィ)、意思決定ツリー、SOP 修正手順
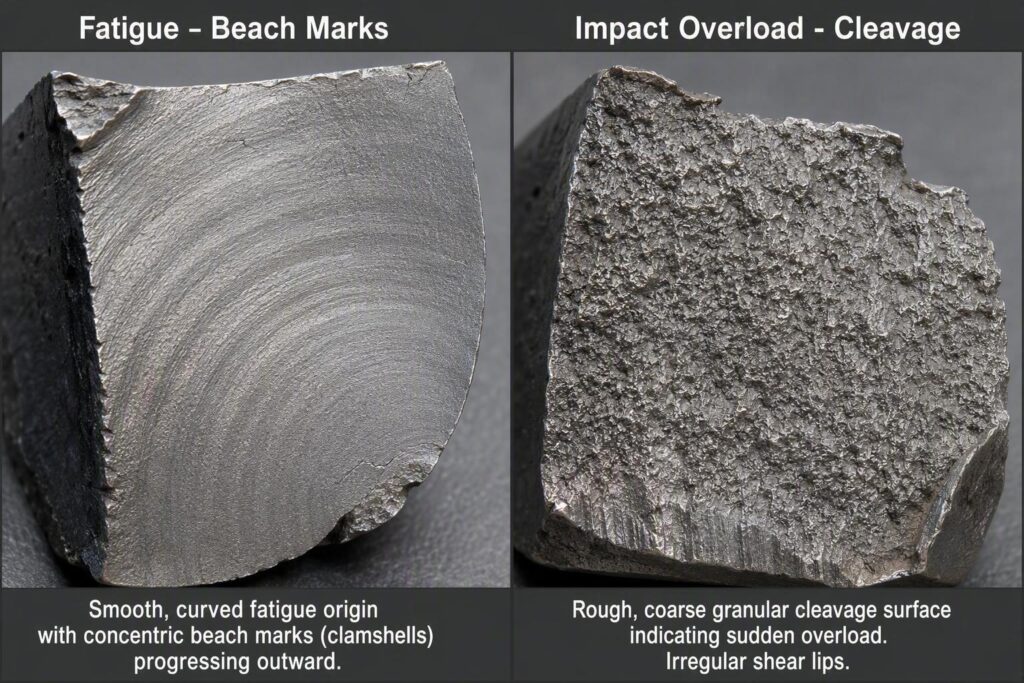
Quick Answer: Shear blade edge chipping root cause falls into two modes: fatigue (from cyclic stress — clearance errors, parallelism faults, or grinding burns) and impact (from sudden overload — foreign objects, excessive hardness, or geometry spikes). Read the fracture surface first: concentric arc-shaped beach marks mean fatigue; coarse granular cleavage with no arc pattern means impact. Each mode points to a different corrective action — fixing the wrong one guarantees repeat chipping. A recurring chip on a shear blade is not just a maintenance event. It is a fracture record — a physical diary of the stress history that produced it. When chips return after every resharpen cycle, the machine […]
丸ナイフのラップ量(オーバーラップ)設定:せん断力学、材質別適正値、およびアーバー精度制御

In continuous metal coil processing, achieving a clean, square, and burr-free edge is the primary benchmark of a well-calibrated slitting line. Behind every high-yield slitting run are two critical geometric parameters governing shear-cut quality: horizontal side clearance and vertical rotary knife overlap. While horizontal clearance dictates the stress concentration across the strip width, vertical knife overlap determines the exact depth of blade penetration required to transition the metal cleanly from plastic deformation into controlled fracture. The operational significance of rotary knife overlap cannot be overstated. Setting the correct vertical overlap minimizes burr height, preserves cut edge geometry, and dramatically extends blade working life. Conversely, incorrect overlap settings drive edge tearing, […]
廃タイヤ&ELVシュレッダー刃:トン当たり処理コスト(Cost Per Ton)を削減する硬度と靭性の最適バランス
Quick Answer: Balance hardness (wear resistance) against Charpy impact toughness rather than maximizing HRC alone—DC53 at 58–60 HRC delivers roughly double D2’s impact toughness for contaminated tire/ELV streams, while a documented real-world case shows that fracture at mounting-hole geometry, not material hardness, is often the true root cause. Scope: This guide focuses primarily on primary and pre-shredding applications for whole scrap tires and mixed ELV feedstocks, where steel reinforcement, tramp metal, impact loading, and abrasive contamination are significant. Secondary rubber granulation and clean wire-free crumb processing require a different wear-versus-toughness balance. Scrap tire recycling and end-of-life vehicle (ELV) size reduction represent two of the most mechanically demanding environments in industrial waste processing. […]
スリット粉じん(Slitting Dust)発生の根本原因解析:刃物側面Ra、炭化物組織&芯出し公差
これら4つの原則は、Maxtor Metalのアプリケーションチームが、軟包装、不織布、特殊紙ラインにおけるゼロダスト・コンバーティングプログラム向けに円形スリッターナイフを評価・選定する際に適用するエンジニアリングフレームワークを構成しています。高速軟包装、産業用テキスタイル、不織布、および特殊紙のコンバーティングにおいて、微粒子による汚染は、計画外のライン停止を引き起こす主な原因となっています。工場のオペレーターが「ウェブ張力の不足」や「原反ロールの欠陥」としばしば診断するトラブルは、多くの場合、シェアカットポイントで発生する「スリット粉の発生」という単一の根本原因に突き当たります。微細なポリマー片、繊維くず、または無機コーティング粒子がスリットされたウェブロールに蓄積すると、後工程で不具合が発生します。光学検査システムが誤った欠陥アラームをトリガーしたり、印刷インキに[…]
産業用ストリップナイフの再研磨:研削・再研磨の閾値、破棄(スクラップ)基準、およびライフサイクルコストモデル
Quick Answer: Regrinding industrial strip blades is economical when: chipping depth is under 0.5 mm, remaining thickness is above 60–70% of nominal, and the estimated regrind cost is below 50% of a new replacement blade. The minimum safe stock removal is 0.010–0.015 in (0.254–0.381 mm) to clear the subsurface micro-fractured fatigue layer. Blades with radial cracks, thermal burn below HRC 52, or thickness below the 60–70% threshold must be scrapped. A managed regrind program typically yields 3–5 precision cycles per blade and can reduce annual knife consumable costs by 45–60% compared to a disposable replacement strategy. In continuous coil processing and high-speed slitting operations, knife consumables represent one of the most […]
M390 vs CPM S90V 粉末冶金ペレタイザーナイフ:高ガラス繊維摩耗下における鋼種選定
Quick answer: For pelletizing blades under high glass-fiber wear, powder metallurgy stainless steels outperform conventional tool steels because their fine, uniform carbide distribution resists micro-ploughing without the toughness trade-offs of high-alloy ingot steels. Between M390 and CPM S90V: choose CPM S90V when abrasion load is the dominant failure mode (>30% GF, neutral water); choose M390 when corrosion resistance, thin blade geometry, or multi-resin flexibility is the priority. Both require cryogenic post-quench treatment and PM-specific grinding protocols to reach their rated HRC and edge geometry. Powder metallurgy (PM) stainless steel, in the context of pelletizer blade manufacturing, refers to steels produced by atomizing molten alloy into fine powder, then consolidating under heat […]
シャーブレード用 D2 vs SKD11 工具鋼:炭化物組織、破損モード解析、および鋼種選定フレームワーク
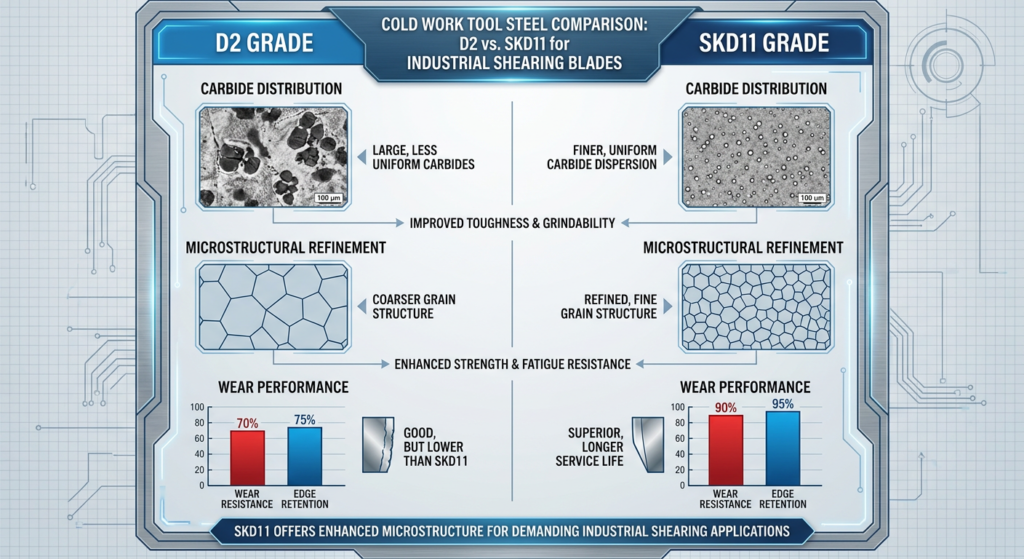
Quick Answer: D2 and SKD11 are compositionally near-identical high-carbon, high-chromium cold-work tool steels, but D2’s higher vanadium content (0.50–1.10%) delivers stronger abrasive wear resistance for clean, high-volume sub-6mm cutting, while SKD11’s finer carbide structure provides better impact toughness for stainless steel, variable feed, or chipping-prone operations. The decision turns on your dominant failure mode—wear or chipping—not the grade label alone. ESR refining quality from your supplier matters as much as the designation. Engineering Note: D2 vs SKD11 tool steel selection for shearing blades is a carbide microstructure decision, not a brand substitution. Both grades occupy the same ledeburitic cold-work steel family (high-C, high-Cr), and their nominal composition windows overlap substantially across ASTM […]
スリッターのカエリ(バリ)低減:根本原因マトリックス・設定条件・検査プロトコル
Slitting burr reduction is one of those “small edge” problems that becomes a big cost problem fast: burr drives customer complaints, creates downstream forming issues, and quietly shortens knife life. This handbook is compiled by Jerry Chu, Technical Support Specialist at Maxtor Metal, drawing on 10+ years of field troubleshooting experience across coil slitting lines processing carbon steel, AHSS, stainless, and aluminum. It is peer-reviewed by Maxtor Metal’s application engineering team and written in a practical, verification-first spirit where the winning approach is disciplined setup windows, fast root-cause isolation, and consistent measurement. If your line uses roller shearing blades (or equivalent slitter knife systems), the principles below still apply: treat the cut […]
 English
 Spanish
 Italian
 French
 Portuguese
 Russian
 German
 Arabic
 Hindi
 Vietnamese
 Indonesian
 Japanese
 Korean